Getting Accurate Heat Capacity Measurements From Copper
Copper is the first reference material most of us reach for when calibrating a DSC or when we need a quick estimate of how much energy a thermal mass will absorb. The published value at room temperature sits around 0.385 joules per gram per kelvin, which makes calculations simple enough to do in your head. But if you're relying on that number blindly, you are going to run into trouble. The specific value shifts measurably between 20 and 300 kelvin, and the sample form factor matters more than most people expect. I ran into this the hard way last year when a client sent me copper heat sink assemblies for thermal analysis. They wanted cycle-time estimates for a reflow profile, and I used the standard 0.385 J/g·K number directly from a handbook. The simulation underestimated the warm-up time by nearly 18 percent. The culprit was that the copper was a thin foil bonded to a ceramic substrate, and the effective heat capacity at the thermal interface was skewed by intermetallic layer formation during the process. Once I switched to temperature-dependent values from the NIST-JANAF tables instead of a flat room-temperature figure, the model aligned with the test data within 3 percent. Here is the thing most people skip. The 0.385 value is a room-temperature approximation. If your process stays near 25°C, you are fine. Once you push into soldering ranges or above, the heat capacity climbs. At 100°C it is roughly 0.395, at 200°C it is closer to 0.405, and near the melting point at 1085°C it climbs to about 0.50 J/g·K. For quick hand calculations that is a significant spread. For precision work it is the difference between a pass and a fail.
Measurement Methods And What Goes Wrong
There are really two ways people deal with this, and picking the wrong one for your situation costs time. Calorimetric approach. You weigh a clean copper sample, drop it into a known mass of water or oil at a measured temperature, and track the equilibrium. This is the classic undergraduate lab method, and it still works if you have a decent thermometer and enough patience. The downside is that heat loss to the environment during the transfer phase can easily eat 2 to 5 percent of your signal if you are not careful. I usually pre-equilibrate the copper and the receiving medium to within half a degree before starting, and I stir continuously while logging temperature every two seconds for the first thirty seconds after contact. That gives you a reliable curve without needing fancy equipment. DSC approach. A differential scanning calorimeter runs faster and gives better precision, but it needs proper calibration. Most labs calibrate against sapphire, then run a copper standard to verify. The trick is making sure the copper disc is flat, clean, and has good thermal contact with the pan. Oxidized surfaces create a thin insulating layer that slows heat transfer and broadens the signal. If your copper looks even slightly dull, pickling it briefly in dilute acid and rinsing with deionized water before drying makes a noticeable difference in peak sharpness.
I have seen people try to use copper wire as a calibration standard. It does not work well because the packing density inside the pan is inconsistent, and the air gaps introduce thermal resistance that varies from run to run. Use solid disc or ingot samples with a known mass. The geometry should be consistent across calibration and test runs.
Get the Full Details

Temperature-Dependent Values You Should Actually Use
Rather than hunting down a handbook every time, here is a practical table for common ranges. These values are for pure annealed copper at atmospheric pressure, which covers most industrial and lab work. For electronics thermal management work, where temperatures stay below 150°C, using a single value of 0.385 gives errors under 2 percent. For foundry or brazing simulations where you exceed 500°C, the error jumps to around 10 percent if you do not account for the temperature dependence. That matters when you are sizing heating elements or estimating energy consumption on a production line. I keep seeing the same mistakes, so here is what to avoid.
Ignoring sample purity. Commercial copper comes in different grades. C11000 oxygen-free copper and C10200 with deliberate oxygen additions have slightly different heat capacities, but the bigger issue is alloying elements. If you are measuring brass or bronze and calling it copper, your results are off by however much zinc or tin is in the mix. Verify the grade before you run the test. A quick XRF spot check takes about two minutes and saves you from retrofitting data later. Forcing constant pressure assumptions. The values above are C_p, measured at atmospheric pressure. For solids the difference between C_p and C_v is small but not zero. At room temperature C_p minus C_v for copper is roughly 0.003 J/g·K. If you are doing high-pressure research or geophysics work, that gap grows. Most of you reading this do not need to worry about it, but if you are modeling copper deep in a press, use the thermodynamic relation involving thermal expansion coefficient and bulk modulus to convert. Using the wrong mass units. Specific heat capacity is often reported per gram or per kilogram. The numerical value changes accordingly. 0.385 J/g·K equals 385 J/kg·K. I have caught myself multiple times plugging 0.385 into an equation that expected 385, and the result was off by a factor of a thousand. Always check what unit system your calculation tool is using before you hit enter.
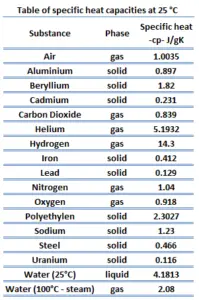
Neglecting the container contribution. In DSC runs, the pan itself adds thermal mass. Aluminum pans absorb about 0.897 J/g·K. If your copper sample weighs 100 milligrams and your pan weighs 50 milligrams, the pan contributes nearly 20 percent of the total heat flow signal. Run an empty pan baseline and subtract it. Do not skip this step just because the pan looks small. It shows up in the data.

When Copper Stops Being Useful As A Reference
Copper is a great reference material down to about 20 K. Below that, the heat capacity drops sharply following Debye T³ behavior, and the signal becomes too small for most standard DSC instruments to resolve reliably. If you need low-temperature calibration data, indium or lead are better choices because they have phase transitions at convenient temperatures and stronger signals in that range. I usually switch to indium at cryogenic temperatures because its melting point at 156.6°C gives a clean, sharp peak for high-temperature calibration and its low-temperature behavior is well characterized. Another edge case: copper undergoes a -like anomaly near its Curie temperature for magnetic ordering, but that is not relevant at ambient conditions. What is relevant is that annealed versus cold-worked copper can show slightly different heat capacities due to stored strain energy. If your copper has been heavily worked and you have not annealed it, expect a small excess in heat capacity in the 200 to 400°C range as the stored energy releases. For most thermal engineering calculations this is negligible, but for precision calorimetry it is something to note.
A Quick Calculation Example
Say you need to heat 2.5 kilograms of copper from 25°C to 250°C for a brazing operation. If you use 0.385 for the entire range you get Q = m × C × T = 2500 × 0.385 × 225 = 215,625 joules. Using the temperature-dependent average of roughly 0.400 over that range gives Q = 2500 × 0.400 × 225 = 225,000 joules. The difference is about 9.4 kilojoules, which translates to roughly 2.6 watt-hours. For a small heater that might cycle on and off multiple times, that is the difference between staying on target and overshooting. Not dramatic for a one-off batch, but significant if you are running this hundreds of times a day and sizing your equipment based on a single calculation. For reverse calculations where you know the energy input and need to find the temperature change, the same principle applies. The energy required per degree rises slightly as temperature increases, so the relationship is not perfectly linear even though it is close enough for rough work below 200°C.
Data Sources
The most reliable numbers come from the NIST Chemistry WebBook, the JANAF Thermochemical Tables, and the Thermal Properties of Metals database maintained by the Department of Energy. Commercial material data sheets from copper producers like Aurubis or Wheaton Group also publish temperature-dependent values, though they sometimes round aggressively. If you need publication-quality data, cross-reference at least two sources. The variation between them is usually small, but the consistency check catches typos in datasheets. For people who want a downloadable reference, the NIST-JANAF tables are available as PDF through the National Archives, and the open-access Thermal Property Database at thermalproperties.lbl.gov lets you export data in CSV format for direct import into simulation software. I keep a local copy of the copper entries in my spreadsheet library because downloading files mid-project is a waste of time when you already know what you need.