Why Your Steam System Keeps Crashing When You Change Load
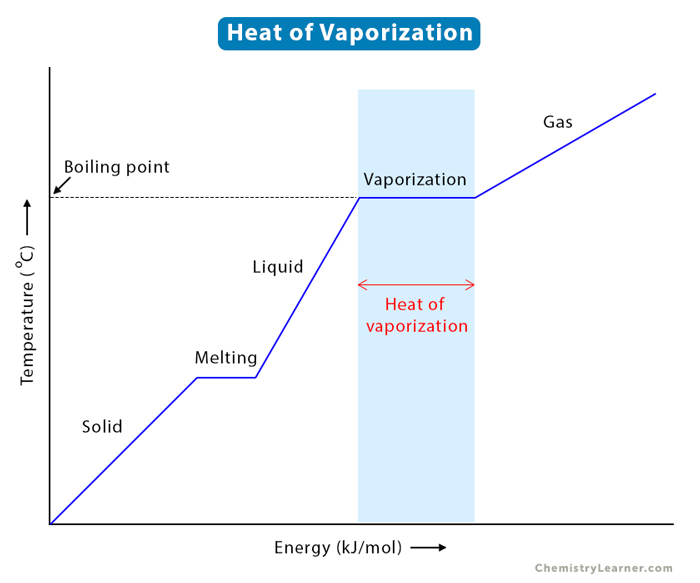
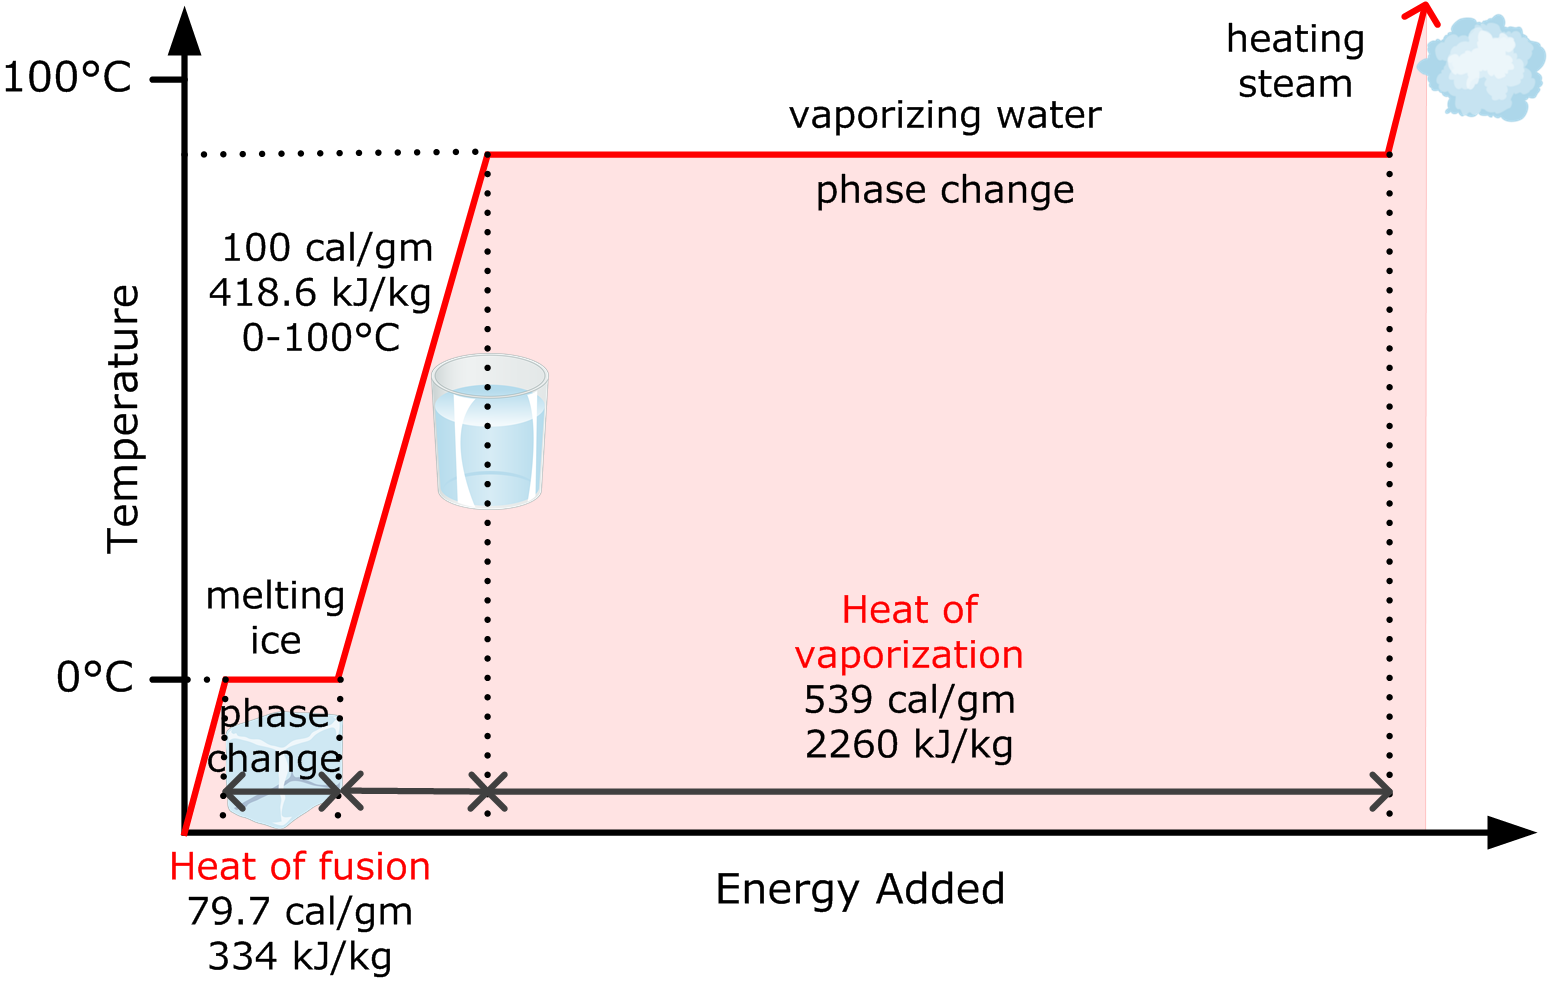
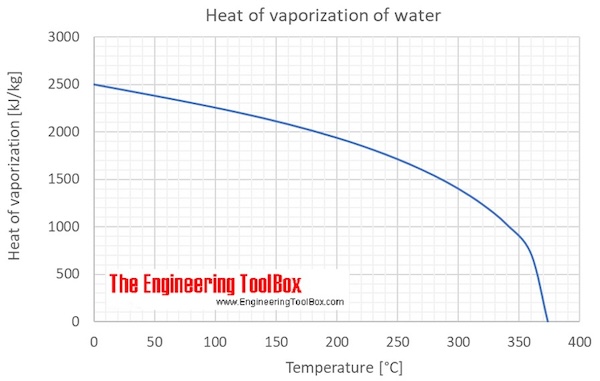
I spent three days last month trying to figure out why a small food-processing plant's steam jacket kept oscillating instead of holding temperature. The product spec called for a steady 120°C, and the control valve was hunting like crazy. We checked the PID tuning, replaced the pressure transducer, even rebuilt the control loop from scratch. Nothing fixed it. The real problem was that nobody had recalculated the heat of vaporization of water for the new operating pressure. At the original design pressure, the latent heat value they were using was off by about 8 percent, which threw off every mass-flow calculation downstream. Once we pulled the correct enthalpy values from the steam tables and updated the model, the oscillation stopped immediately. That's just how it is when you're working with phase-change systems. The number you will find on a standard chemistry textbook cover is 2260 kJ per kilogram at 100 degrees Celsius at sea level pressure. That is a single point on a curve, not a constant. The actual value drops as pressure increases, and it drops fast enough that using the textbook number at higher pressures will consistently overestimate your steam requirements. At 5 bar gauge, for example, the latent heat is closer to 2108 kJ/kg. At 10 bar gauge it is down to about 2015 kJ/kg. By the time you reach the critical point at 220.6 bar, the concept itself dissolves because there is no phase boundary left. I see people still use 2260 across the board in preliminary sizing, and the error is usually acceptable for rough estimates but becomes a real problem when you are specifying equipment or running a cost model. The practical way to get values is to use the IAPWS-IF97 formulation, which is the international standard for industrial steam properties. Most engineering calculators and property packages implement this. If you are doing hand calculations or building a spreadsheet, you can approximate from the steam tables published in most thermodynamics textbooks or from NIST Webbook data. I keep a small lookup table in my spreadsheet for pressures between 0.1 and 15 bar, which covers the vast majority of low-pressure industrial steam applications. For anything above that, you should pull the full property package because the curves change more rapidly near the critical region.
Here is the basic calculation you need for a steam heating application. You take the mass flow rate of the steam that condenses and multiply it by the latent heat at your operating pressure. That gives you the thermal power available from condensation alone. Add the sensible heat from desuperheating if your steam is superheated, and add the sensible cooling of the condensate if it leaves as subcooled liquid. In most jacketed vessel problems, the latent heat term dominates, usually 90 percent or more of the total heat transfer. The sensible terms are secondary but they matter when you are trying to hit a tight tolerance. I ran into a case where a pharmaceutical company was under-sizing their condensate removal system because they were only accounting for latent heat. The product being heated had a high specific heat and the process cycle was short, maybe four minutes from cold charge to target temperature. The sensible heat coming out of the superheated steam and the subcooled condensate actually accounted for about 12 percent of the total energy delivered. That 12 percent difference meant the steam trap was undersized, condensate was backing up in the jacket, and the effective heat transfer area was dropping over time. The fix was not just a bigger trap, it was redesigning the condensate drain to handle the full energy balance including sensible terms.
The Properties You Need to Know Beyond the Textbook Number
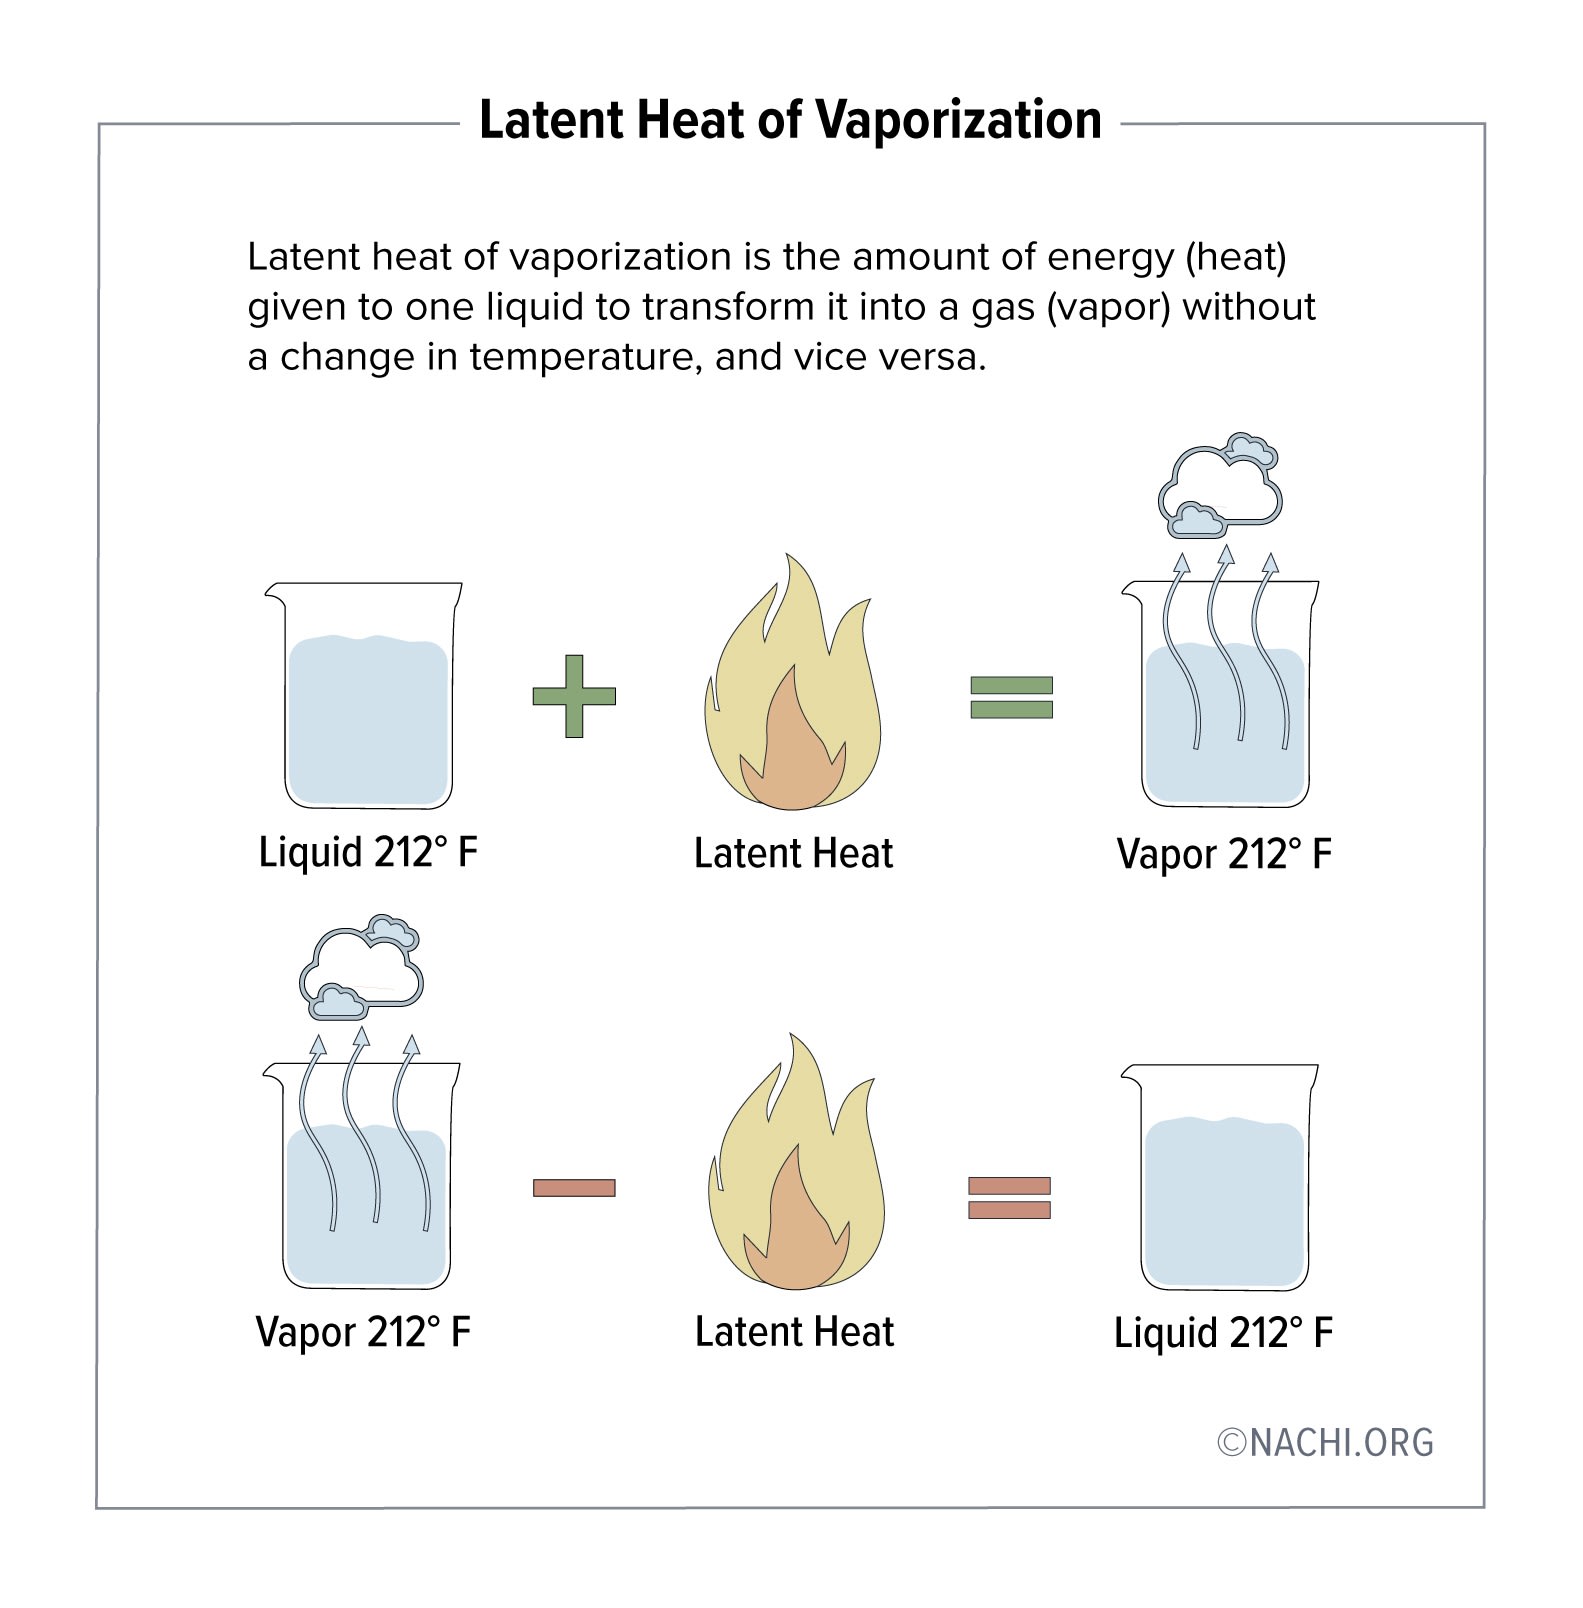
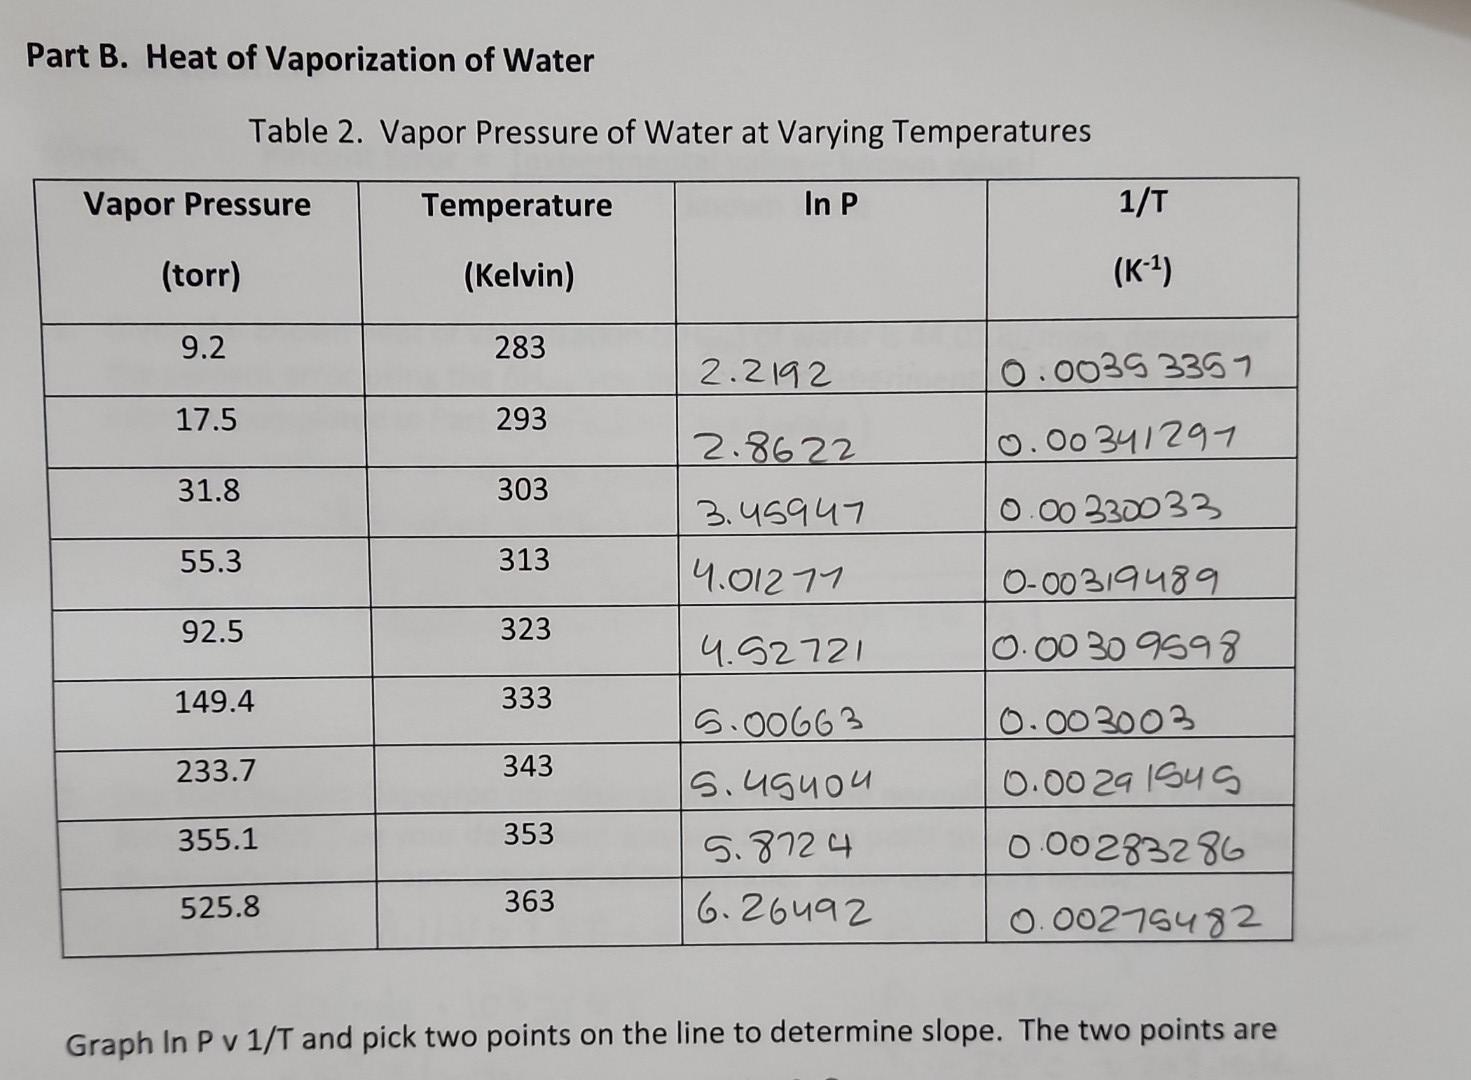
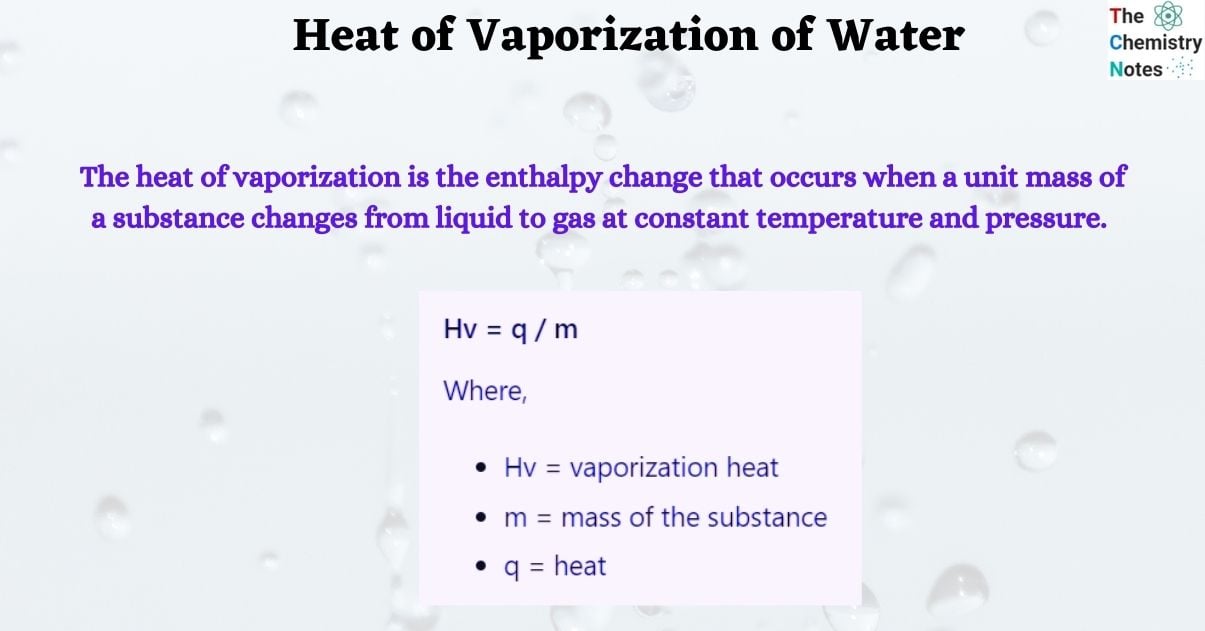
Enthalpy of saturated liquid is the energy content of water at the boiling point relative to the reference state. Enthalpy of saturated vapor is the energy content of steam at the same pressure. The difference between these two values is the latent heat or heat of vaporization at that pressure. These values are interdependent, so you cannot change one without the other shifting as pressure changes. Temperature and pressure are locked together along the saturation curve, which means you only need one independent variable to define the state. The Clausius-Clapeyron relation describes how the latent heat changes with temperature and pressure. The equation itself is straightforward, but the practical implication is that the latent heat is not linear with respect to either variable. It decreases roughly linearly at low pressures but then curves more sharply as you approach the critical point. This is why interpolation from a table is safer than assuming a straight-line relationship across a wide pressure range. A linear fit between 1 bar and 10 bar will give you errors in the 3 to 5 percent range at intermediate points. One thing that trips people up is assuming the heat of vaporization is the same as the total enthalpy of steam. They are different. The total enthalpy includes both the sensible heat to get the water to boiling and the latent heat to turn it into steam. If you are calculating how much energy is released when steam condenses and then cools as a liquid, you need both parts. Using only the latent heat term will under-predict the energy available by a significant margin if the condensate leaves hot. In many industrial condensate return systems, the condensate leaves at 80 to 90 degrees Celsius, carrying another 335 to 375 kJ per kilogram of sensible energy that never made it into the process. That is money leaving the plant in the drain line.
Get the Full Details
Common Pitfalls and Where the Method Falls Apart
The biggest mistake I see is using a single latent heat value for a system that operates across a wide pressure range. Some facilities have a central boiler at 10 bar that distributes steam through a header network, and by the time it reaches the point of use the pressure may have dropped to 3 or 4 bar due to line losses. The latent heat at those two pressures differs by roughly 100 kJ/kg. If your process model uses a single value, your steam consumption estimates will be wrong, and the error compounds over many cycles. The fix is to calculate at the actual point-of-use pressure, not the boiler pressure, and to include the pressure drop in your model. Another issue is non-condensable gases. Air or other gases trapped in a steam system do not condense and they occupy volume that should be filled by condensing steam. This reduces the effective heat transfer coefficient dramatically. I have seen heat exchangers that were rated for 500 kW perform at barely 200 kW because the air vent was clogged and the operator had not checked it in months. No amount of correcting your latent heat value will fix that problem. The workaround is regular venting and monitoring the condensate temperature, which should be very close to the saturation temperature at the operating pressure if the system is clean. The method breaks down completely near the critical point. Above about 200 bar, the distinction between liquid and vapor disappears, and the latent heat approaches zero. If you are working in supercritical water conditions, which some advanced power cycles do, you cannot use this approach at all. You need a full equation of state like IAPWS-95 and you need to treat the fluid as a single phase with continuously changing properties. Trying to force a latent heat calculation into that regime will give you nonsense numbers. I learned this the hard way when someone asked me to estimate the energy requirement for a supercritical water oxidation unit. My first draft was obviously wrong once I checked the property data.
There is also the issue of purity. The standard values assume pure water. If you have dissolved solids, the boiling point rises and the latent heat changes slightly. In most industrial steam systems the water is treated and the impurity level is low enough that the effect is negligible. In a boiler operating at high purity levels with repeated cycles, scaling can change the heat transfer characteristics even if the thermodynamic properties are unaffected. That is a maintenance problem, not a calculation problem, but it shows up in the same place in your data.
Practical Calculation Workflow
When I need to size a steam heating system or audit an existing one, my workflow is consistent. First, I identify the operating pressure at the point of use, not at the source. I measure it with a calibrated gauge if the documentation is old or missing. Second, I pull the saturation temperature and the latent heat from IAPWS-IF97 based on that pressure. Third, I calculate the required thermal duty from the process side, taking into account the mass and specific heat of the product, the temperature rise needed, and the cycle time. Fourth, I divide the duty by the latent heat to get the required steam mass flow. Fifth, I check the condensate conditions and add the sensible terms if they are significant for the application. This process usually takes me about 20 minutes for a standard jacketed vessel calculation. A preliminary estimate using rounded values and the textbook latent heat might take five minutes, but I do not trust those numbers for anything beyond an order-of-magnitude check. The extra time is worth it because the wrong steam flow rate leads to either wasted energy from oversizing or process failures from undersizing, and both are expensive to fix after installation. I have seen a project delayed by six weeks because the steam piping was undersized based on an incorrect latent heat assumption, and the replacement piping had to be ordered and fabricated from scratch. For quick reference, here are the key values at common industrial pressures. At atmospheric pressure, the latent heat is 2257 kJ/kg at a saturation temperature of 100°C. At 1 bar gauge, it is about 2201 kJ/kg at 120°C. At 5 bar gauge, it drops to 2108 kJ/kg at 152°C. At 10 bar gauge, it is 2015 kJ/kg at 184°C. At 15 bar gauge, it is 1947 kJ/kg at 201°C. These numbers are sufficient for most low-to-medium pressure industrial work. Keep them in a spreadsheet and reference them directly rather than recomputing from scratch each time.
What This Means for Your Design Decisions
If you are specifying steam traps, the flow rate you calculate depends directly on the latent heat value you use. An 8 percent error in latent heat translates to an 8 percent error in trap sizing, which can mean a trap that is too small and chokes under load or one that is wastefully oversized. Both are bad. If you are running a cost analysis, the steam consumption figure drives your operating cost estimate, and that figure is only as good as the latent heat input. A small error in the thermodynamic property propagates directly into a large error in the annual energy bill projection. The bottom line is that the heat of vaporization is a variable property, not a constant, and treating it as one will introduce systematic errors into any calculation that depends on it. The IAPWS-IF97 standard is the tool you should be using, and the steam tables are freely available online if you need them. The extra few minutes spent getting the right value at the right pressure saves you from a lot of downstream problems.