Why Heat Transfer Calculations Usually Fail on Paper
Most people start with Fourier's Law and assume everything works out linearly. It doesn't. I've sat in meetings where engineers stared at a perfectly solved textbook problem while the actual equipment blew a gasket because nobody accounted for contact resistance at the flange joint. The math was right. The application was wrong. Here's the thing about heat transfer problems and solutions that nobody tells you upfront: the boundary conditions matter more than the equation itself. Pick the wrong one and your solution converges beautifully to the wrong answer. I learned this the hard way in 2019 when we were modeling heat dissipation for a power electronics enclosure. The simulation showed a peak temperature of 78 degrees Celsius. Real world? 112. The missing variable was natural convection scaling. We'd used a forced convection coefficient because the datasheet value was cleaner to work with. It cost us three weeks of rework and a very uncomfortable conversation with the client.
Heat Transfer Problems And Solutions: Where to Start
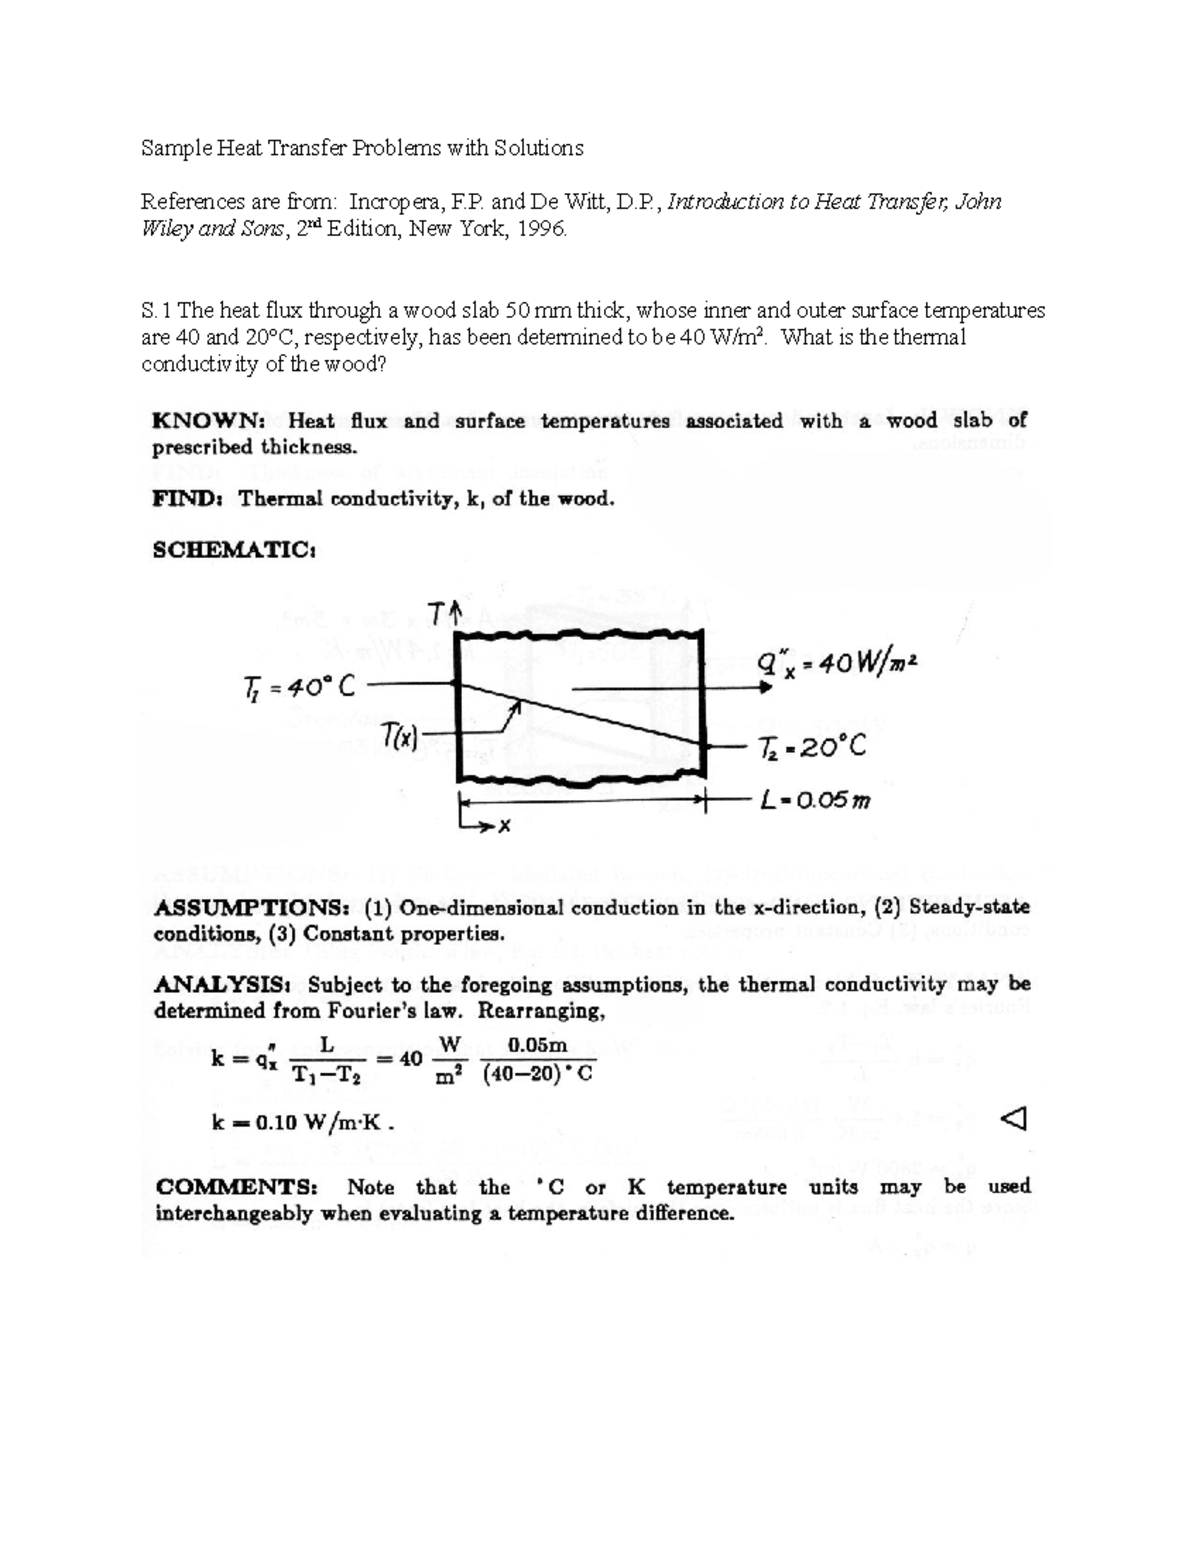
Don't reach for a numerical solver first. Write down what's actually happening at every interface. Conduction through solid material. Convection at surfaces exposed to fluid. Radiation if temperatures exceed roughly 150 Celsius above ambient. Most textbook problems hide radiation behind a "negligible" label. In practice, radiation becomes dominant around 300 to 400 degrees and above, and ignoring it will push your error margin into double digits. The standard approach breaks into three categories: conduction, convection, and radiation. You'll need thermal conductivity values, heat transfer coefficients, surface emissivities, and geometry details. Get any of these wrong and the whole calculation drifts. I keep a reference sheet with typical h-values for common scenarios — natural convection off a vertical plate runs about 5 to 10 W/m²K, forced convection in a duct can hit 25 to 250 depending on velocity. These ranges are where most beginners fumble because they treat them as constants instead of variables that shift with temperature and flow conditions. For steady-state conduction through a plane wall, the thermal resistance method is your baseline. It's just the electrical analogy: temperature difference equals heat flow times resistance. Resistance is thickness divided by conductivity times area. Stack resistances in series for composite walls. Parallel paths need their own treatment. This method works until geometry gets complicated, and then you switch to numerical approaches or simplified shape factors from handbooks like Incropera or Holman.
The Counter-Intuitive Stuff Nobody Teaches
First: adding insulation to a pipe doesn't always reduce heat loss. There's a critical radius of insulation where the trade-off between increased surface area and added resistance hits a tipping point. For small diameter pipes with low convection coefficients, adding insulation initially increases heat transfer. This matters in HVAC piping and electrical cable routing where wire diameters are tiny. Second: fin effectiveness isn't about making fins longer. Once a fin's length exceeds roughly three times the parameter sqrt(hP/kA), adding more length gives diminishing returns that taper off toward zero. I once saw an engineer specify fins on a heat sink that were 80 millimeters long for a application where 20 millimeters would have done the same job at a fraction of the weight and cost. The extra material didn't move any meaningful heat. Third, and this one trips people up constantly: transient heat transfer problems require the Biot number check before you apply the lumped capacitance method. If Bi is less than 0.1, the internal resistance is negligible compared to surface resistance and you can treat the object as a single temperature node. If it's greater, you need spatial temperature distribution — either analytical solutions with separation of variables or numerical methods. I've seen this mistake inflate errors by factors of three or four in casting and quenching applications where thermal gradients drive stress and distortion.
Get the Full Details

A Real Case From My Bench Work
We were troubleshooting a transformer cooling system where oil-driven natural convection was supposed to keep winding temperatures below 105 degrees. The design calculations said 92 degrees should be achievable. Measured values hovered around 118. The problem wasn't the oil flow rate or the radiator surface area. It was oxidation buildup on the internal fin surfaces that had been operating for four years without a flush. The effective emissivity and convection coefficient had dropped significantly because the surface roughness changed and a thin insulating layer formed. The workaround was brutal but simple: take the transformer offline, drain the oil, physically clean the fin surfaces with a solvent soak and soft brush, refill with fresh oil, and recalibrate the temperature sensors. The post-maintenance reading was 89 degrees. The lesson was that heat transfer coefficients degrade over time in real systems, and maintenance schedules need to account for that. Our original design assumed clean surfaces. Nobody revised that assumption during the annual review cycle.
Common Pitfalls When Solving These Problems
Using temperature-independent material properties when you have a 200-degree temperature swing. Thermal conductivity for metals drops as temperature rises. For insulators it often increases. If your delta T exceeds about 50 degrees, you should be iterating with temperature-dependent values or using an average evaluated at the mean film temperature. One degree of error in your conductivity input can translate to five to ten percent error in your heat transfer rate depending on the material. Assuming uniform heat flux at boundaries when your real setup has hot spots. A power resistor mounted to a heatsink doesn't distribute heat evenly across its base. The thermal spreader resistance inside the component creates a non-uniform flux profile. If you model it as uniform, your peak temperature prediction will be optimistic. The fix is to either use a conjugate heat transfer simulation or apply a correction factor based on the component's thermal spreading resistance data from the manufacturer. Neglecting the thermal contact resistance between joined surfaces. Two nominally flat metal surfaces in contact have actual contact at discrete asperity points. The rest is filled with air or thermal interface material. This contact resistance can dominate the total thermal resistance in bolted or clamped joints. I've measured contact resistances in the range of 0.01 to 0.1 m²K/W for machined aluminum surfaces with torque-spec bolts and no interface material. With a good thermal paste, you can get that down to 0.005 or so. Without it, your calculated temps will consistently run low.
When Analytical Methods Hit a Wall
Complex geometries, mixed boundary conditions, temperature-dependent properties, and multi-mode heat transfer all push you toward numerical methods. Finite difference, finite element, and finite volume approaches are the standard tools. ANSYS, COMSOL, and open-source options like OpenFOAM handle most industrial problems. For quick hand calculations, the method of superposition with shape factors from tables works surprisingly well for many practical geometries. There's a trap here though. Mesh dependency is real. Run a convergence study before trusting your results. I once reviewed a simulation where the temperature field looked reasonable at first glance, but refining the mesh changed the peak value by 15 percent. The original mesh had elements that were too coarse near the boundary layer. For convection-dominated problems, your first elements off a wall need to resolve the thermal boundary layer. That usually means y-plus values in the single digits for turbulent flow or at least enough layers within the laminar sublayer to capture the gradient.

What Actually Works in Practice
Start simple. Build an analytical or spreadsheet model first even if you plan to run a simulation later. It gives you a baseline to sanity-check the numerical results. If your FEA output looks nothing like your hand calculation, something is wrong and you'll catch it faster that way. This habit alone has saved me from chasing phantom bugs in simulation setups multiple times. Document every assumption. Every h-value you pick, every material property source, every boundary condition. When the numbers don't match reality, you need to be able to trace back and find which assumption cracked. I keep a log for every project with dates, sources, and rationale. Six months later when you're trying to figure out why your prediction was off, that log is the only thing that will save you from starting from scratch. Validate early and often. A single real-world data point beats a hundred simulated ones. Measure temperature at accessible points with thermocouples or IR cameras and compare against your model. Adjust your assumptions based on the discrepancy. This iterative calibration process is where the actual engineering happens, not in the initial calculation phase.
The bottom line is that heat transfer problems and solutions live in the gap between idealized theory and messy reality. The equations are reliable. The inputs are where things fall apart. Spend your time getting the boundary conditions, material properties, and surface conditions right and your predictions will land close to actual measurements. Miss those and no amount of numerical sophistication will save you.