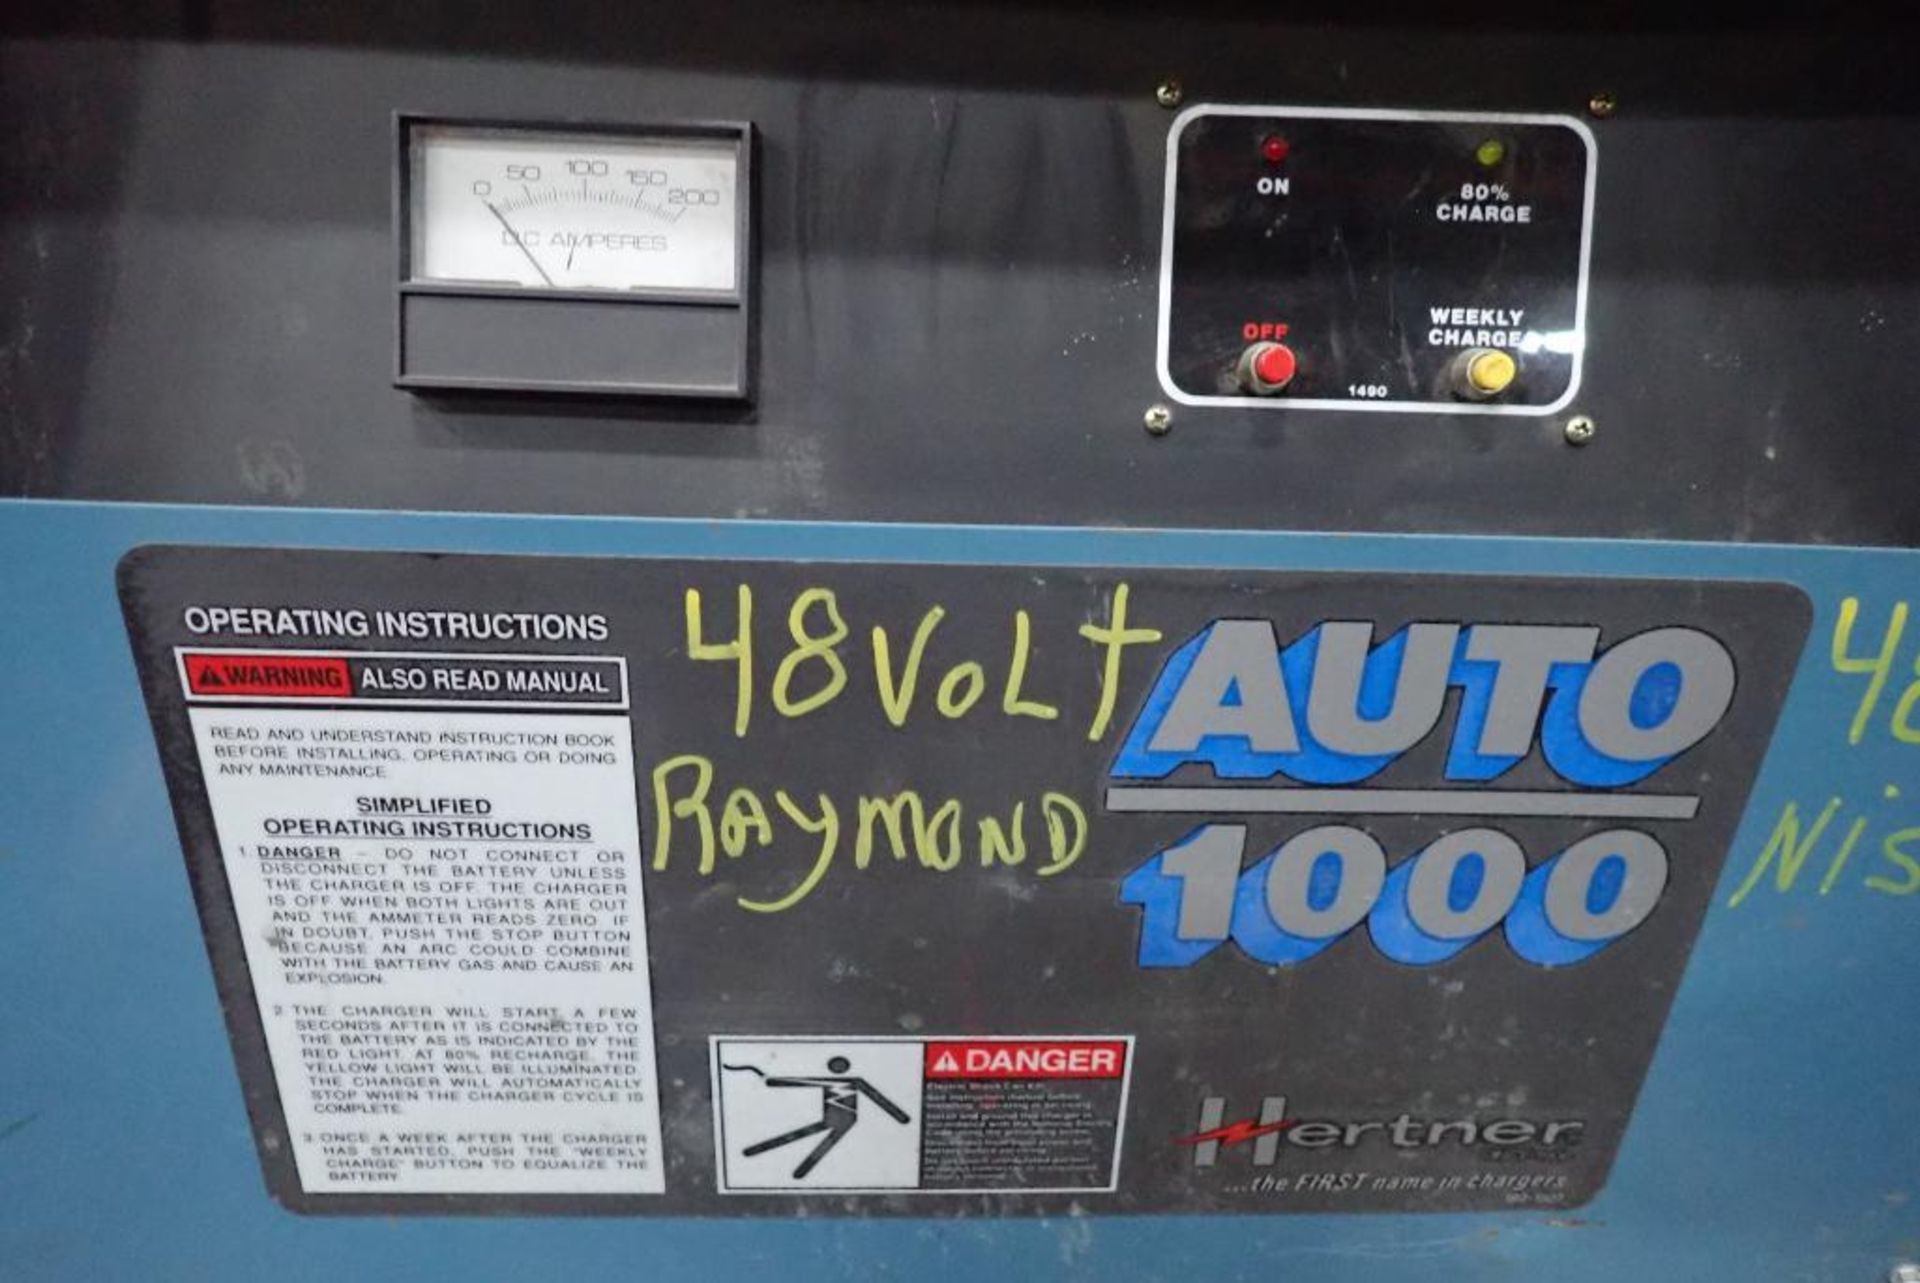
Getting the Hertner Auto 1000 Up and Running
The Hertner Auto 1000 is a benchtop precision drill press and milling hybrid from the late 1990s. It was built for small shops that needed both vertical drilling accuracy and light milling work without investing in two separate machines. The build quality is solid, but the manual that ships with it is sparse in places and occasionally contradictory. Most people who buy these used are working from a scanned copy or a PDF someone uploaded to a forum, and neither is always reliable. I spent about eight years running one of these in a machine shop before we retired it. It was one of the first pieces of equipment I ever got comfortable with, and I learned a lot of things the hard way because the documentation wasn't clear enough.
Hertner Auto 1000 Manual: What You Actually Need to Know
Before you touch anything, find the section on quill return spring tension. The manual tells you to adjust it so the quill returns smoothly, but it doesn't tell you what happens when it's set too tight. I learned this when my first Auto 1000's quill started binding after about six months of use. The spring was overtightened, and it was creating enough lateral pressure on the quill bushing to cause premature wear. The fix was loosening the spring retainer nut by about a quarter turn and testing the return with the spindle unloaded. If it still snaps back fast enough for your workflow, you're in the right range. If it lingers, tighten it incrementally. This adjustment alone usually makes the difference between a machine that runs quiet for years and one that develops play in the quill assembly within a year. The variable speed control is another area where the manual falls short. It says the motor runs at speeds from 250 to 3000 RPM, but the actual dial markings are approximate. I ran a tachometer check against the dial numbers on my unit, and the discrepancy ranged from about 8 percent at the low end to 15 percent at the high end. If you're doing work where RPM matters — like tapping or drilling hardened material — you need to calibrate the dial yourself or invest in a separate reflective tachometer. This adds maybe twenty minutes to your setup time the first time, but it pays off every time you need a precise speed afterward. The table adjustment mechanism uses a friction clamp combined with a lock screw. The manual describes this as straightforward, but in practice the friction element can slip under heavy cutting loads if it's not adjusted regularly. I found that checking and adjusting the table friction clamp every few weeks, especially if you're doing anything beyond light drilling, prevents the table from drifting during operation. A loose table during a milling pass can ruin a part and potentially damage the spindle. Tighten it just enough that the table moves with deliberate resistance but won't shift on its own under normal cutting forces.
One thing the manual doesn't emphasize enough is coolant compatibility. The Auto 1000 wasn't designed with a sealed coolant system, and the way the quill and spindle housing are constructed means that any liquid coolant you use will eventually find its way into areas it shouldn't be. I've seen machines where water-soluble coolant caused corrosion on the quill bearing surfaces because someone used it liberally without wiping down the exposed areas after each shift. The workaround I adopted was switching to a light cutting oil for most operations and only using water-soluble coolant for extended runs on aluminum, followed by a thorough wipe-down with a rag soaked in light machine oil. This approach keeps the internal surfaces protected and has kept the quill assembly clean and smooth on my unit for years. If you're looking for a full manual, the original paper version is hard to find new. There are scanned PDFs circulating on a few enthusiast forums and on one or two industrial equipment sites. They tend to be lower resolution than ideal, and pages can be misaligned or cut off. I'd recommend checking machinist forums like Practical Machinist or specific German industrial equipment groups, since Hertner was a German manufacturer. Some users have posted higher-quality scans there. You might also contact Hertner's current successor company or a dealer who still services their equipment — sometimes they'll provide a replacement manual for a nominal fee. There are real limitations to this machine that the manual glosses over. The spindle runout, even when new, tends to sit around 0.002 to 0.004 inches TIR, which is acceptable for general drilling but not for precision milling work that requires tight tolerances. Over time, as the bearings wear, this can increase. If you need sub-0.001 inch runout, you're looking at a bearing replacement and possible spindle rebuild, which costs more than the machine is typically worth on the used market. Also, the throat depth is limited to about 10 inches, which restricts the size of stock you can work with without fabricating an extension table. And the column diameter, while adequate for light work, can flex slightly under heavier side loads during milling, so don't expect it to perform like a dedicated milling machine.
Get the Full Details

For most people using this as a benchtop drill press with occasional light milling capability, it's a reasonable machine. If you're primarily doing precision milling or high-volume production drilling, you'd be better off looking at a dedicated mill or a modern CNC benchtop unit. The Auto 1000 occupies a middle ground that works well for hobbyists, small repair shops, and light production work, but it stretches past its limits if you push it into territory meant for heavier equipment.