Getting Started With HPP
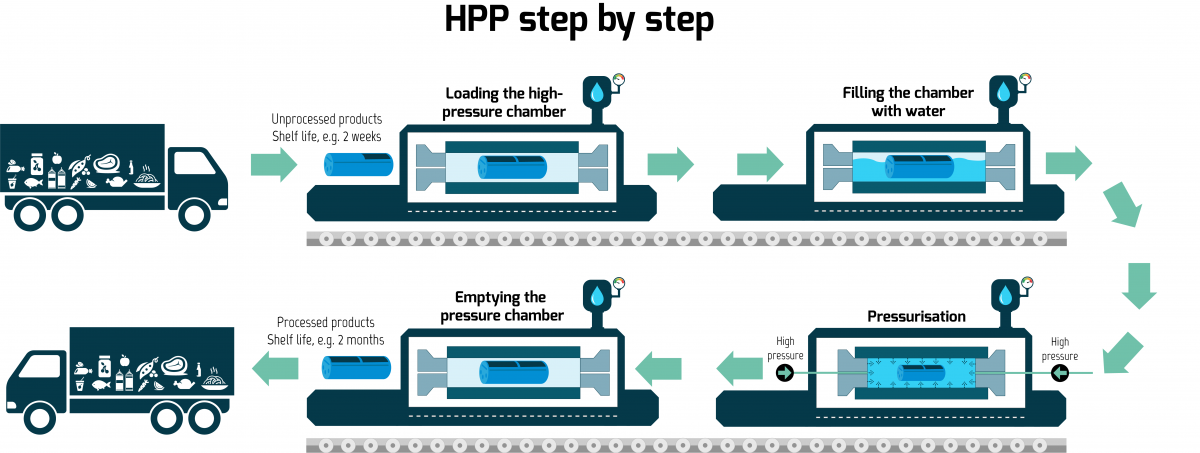
High Pressure Processing of Foods is one of those technologies that looks deceptively simple until you try to run a production batch. The concept itself is straightforward enough. You put sealed food in a vessel, pump water to roughly 400–600 MPa, hold it for somewhere between 60 and 300 seconds, then depressurize. That's the entire cycle on paper. The reality is a lot of fiddling around with parameters that never quite match the textbook. I should mention something about pressure units before going further. The industry talks in megapascals, but some of your suppliers will still quote in ksi or tons per square inch. 400 MPa is roughly 58 ksi. Getting this wrong on a spec sheet has ruined more orders than I care to count.
How High Pressure Processing Of Foods Actually Works
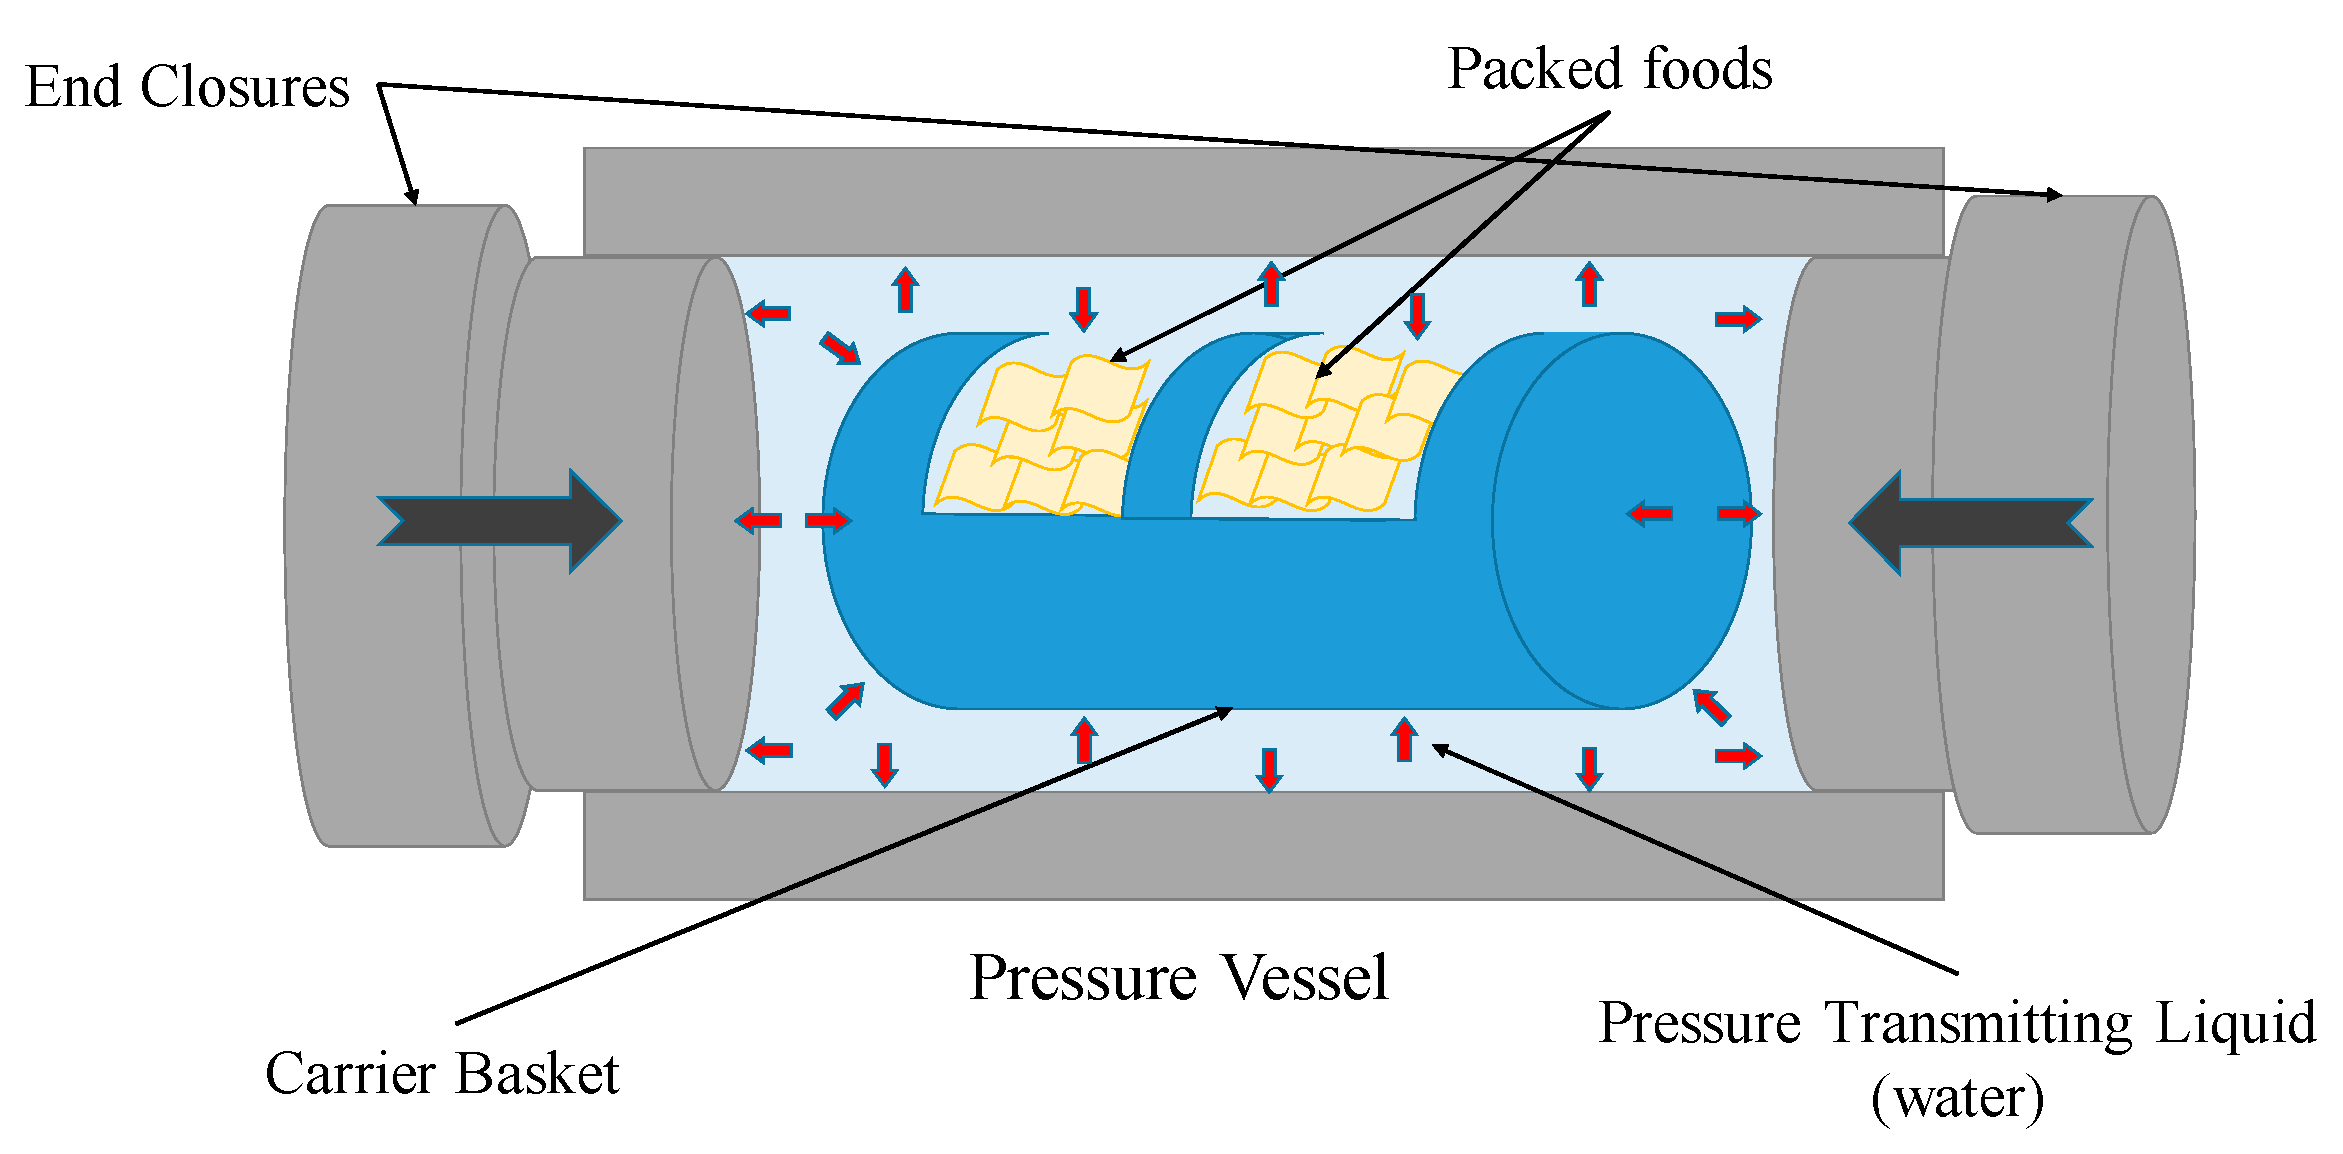
The mechanism is isostatic pressure. Water transmits it evenly in every direction, which is why HPP is fundamentally different from mechanical compression or heat treatment. Chemical bonds in proteins unfold at those pressure levels, microbial cell membranes lose integrity, and enzymatic activity slows or stops entirely. Pathogens like Listeria monocytogenes, E. coli O157:H7, and Salmonella are the main targets. Spoilage organisms get hit too, which is why shelf life extends dramatically without any thermal degradation of flavor or nutrients. One thing people consistently get wrong is assuming pressure does everything equally. It doesn't. Spores are remarkably resistant to pressure alone. Clostridium botulinum spores will survive a standard 600 MPa treatment with zero fuss. That's why HPP is almost always paired with a mild thermal step or a refrigerated distribution chain. If someone tells you HPP replaces all preservation methods, they're selling you something. Run. Here's the specific problem I ran into last year that took me three weeks to resolve. We were processing a ready-to-eat dip with a particulate phase — avocado and tomato bits suspended in a liquid matrix. The product passed microbial tests fine at 600 MPa for 180 seconds, but after four weeks of refrigerated storage, we started getting late-stage gas production. Turns out we had a barotolerant strain of Lactobacillus that wasn't being killed at our standard parameters. The pressure was reaching the liquid phase but not the particulate phase effectively enough due to density differences. The workaround was switching from a single 600 MPa hold to a two-stage treatment: 400 MPa for 60 seconds first to damage the cell walls, then ramp to 600 MPa for another 90 seconds. That broke the barotolerance and we got clean results for the rest of the trial. You can't solve this with a spreadsheet. You have to observe what's actually happening in the product.
Packaging selection is another area where beginners waste a lot of money. Flexible pouches and laminated trays work best. The material needs to be impermeable to oxygen and moisture, compatible with extreme pressure, and sealable without compromising the package integrity during compression. I've seen people try to reuse rigid containers from other processes and end up with seal failures or micro-cracks that let untreated water back in during the pressure cycle. EVOH barrier layers tend to hold up better than standard PET under repeated HPP cycles. It's worth testing your actual packaging material through at least 50 pressure cycles before committing to a production line.
Get the Full Details
Setting Up a Treatment Cycle
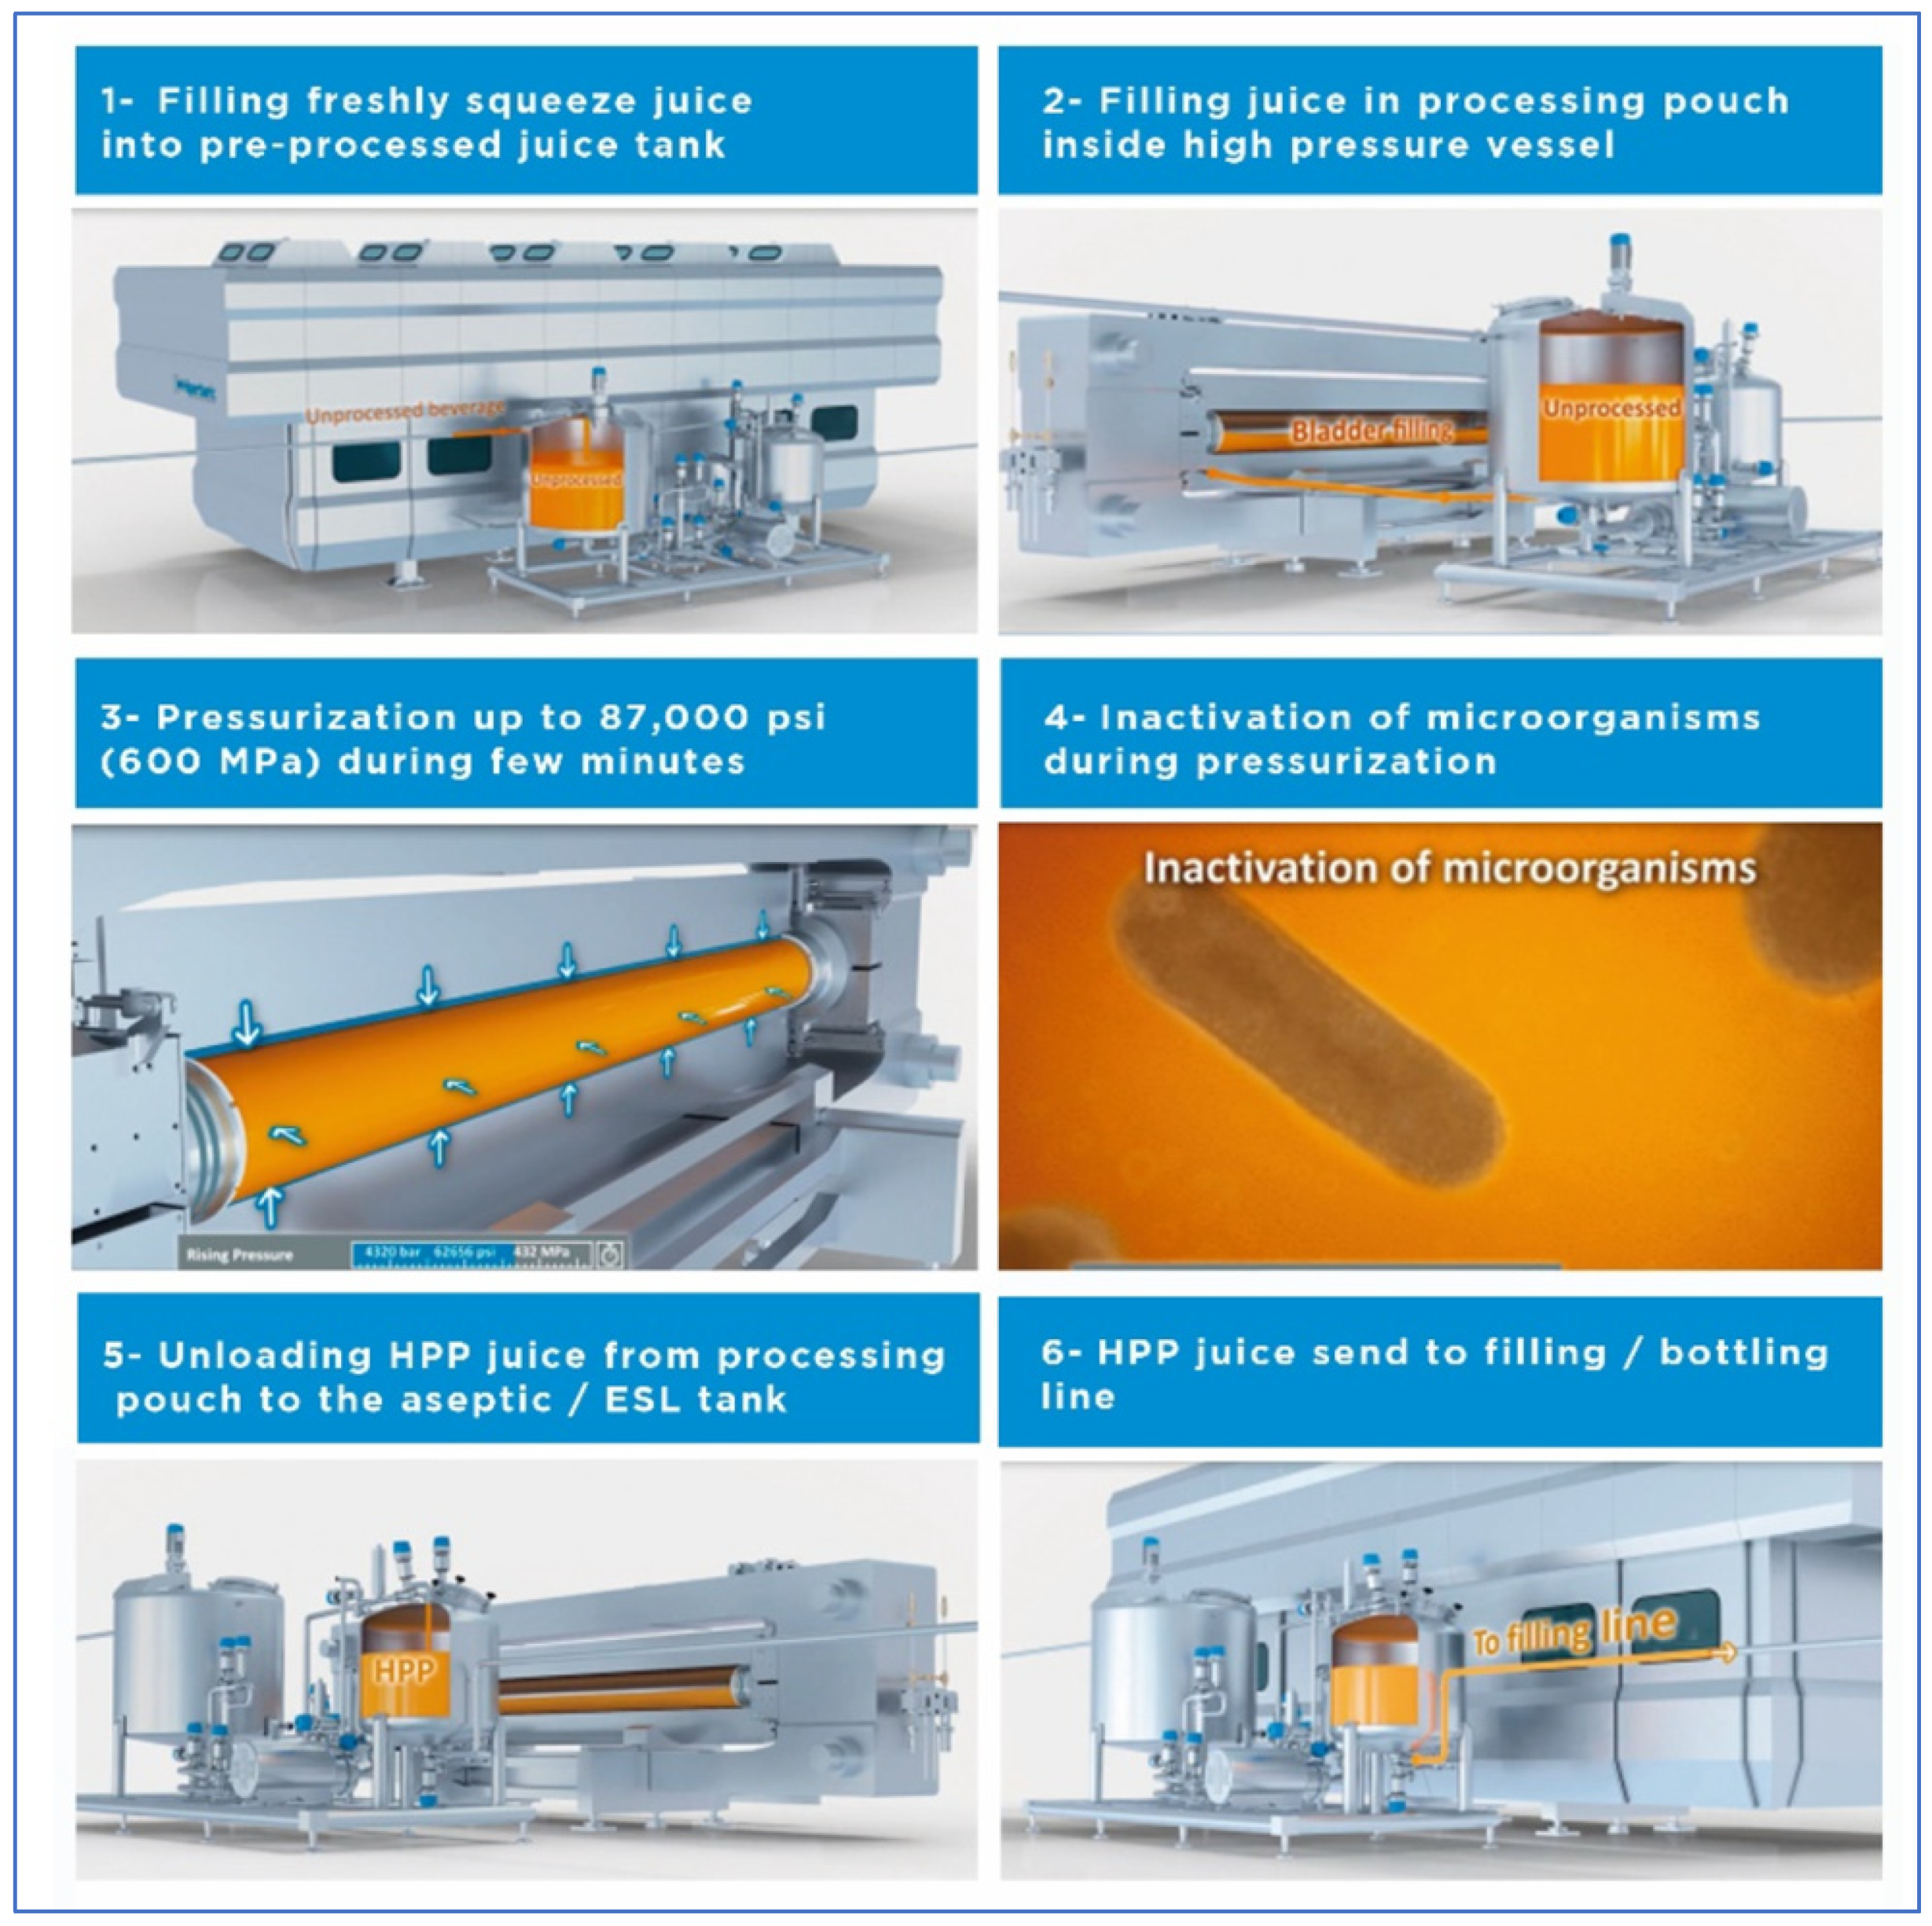
The parameters you choose depend entirely on your target organism and your product matrix. Here's a practical framework: Start by identifying your worst-case pathogen for the product. For acidic foods below pH 4.6, Clostridium botulinum isn't the concern — you're dealing with yeasts, molds, and acid-tolerant bacteria. For low-acid foods, you need a process that achieves a 5-log reduction of C. botulinum spores, which practically means combining HPP with mild heating to around 60–70°C during pressurization. Pressure level selection matters more than duration in most cases. 400 MPa handles many vegetative cells. 600 MPa is the workhorse for most ready-to-eat applications. Going above 800 MPa starts affecting texture and functional properties in ways that matter — proteins denature, gels can collapse, and emulsions may break. I typically recommend starting at 600 MPa and working downward only if you're getting negative sensory impacts.
Holding time is where the compromise happens. Longer holds increase microbial kill but also increase the chance of texture modification and color changes in sensitive products like fresh juices. A 180-second hold at 600 MPa is standard for many applications. Some juices benefit from a shorter 60-second hold at the same pressure because the acidity provides additional antimicrobial support. Your validation studies will tell you which combination works. Temperature control during the cycle is something most people treat as an afterthought but it genuinely matters. The compression of water generates heat — adiabatic heating. You can see temperature spikes of 15–20°C inside the vessel during pressurization depending on your pump speed and starting temperature. If you're processing a heat-sensitive product, you need a recirculating temperature control system on the pressure vessel. Running HPP at ambient temperature without temperature management is fine for some products and destructive for others. Cold water input, typically 5–10°C, is standard practice to offset the adiabatic rise.
Validation And Quality Control
You cannot ship an HPP-processed product without validated processes. This isn't optional. You need challenge studies that demonstrate your specific parameters achieve your stated log reductions in your actual product, not in a surrogate. Using a model organism in a buffer solution is not acceptable to any credible regulatory body or buyer. The big pitfall here is assuming that because a process works in your lab scale unit, it will work in production. The pressure distribution isn't perfectly uniform in larger vessels. Dead zones exist near the pressure relief ports and at the edges of bulky product configurations. When I design validation studies, I place thermocouples and chemical indicators at multiple points in the load — corners, center, and near the pressure transmission media interface. The worst-positioned point becomes your validation reference. If that point meets your microbial reduction criteria, the whole load is considered treated. Post-process testing should include both microbial confirmation and sensory evaluation at multiple time points. A product can pass all microbial tests and still be rejected by customers because the texture has changed. Gelation in protein-containing products is one of the more common issues. Casein micelles restructure under pressure. Meat products can become harder or develop a cooked-like texture even though no heat was applied. These are real problems, not theoretical concerns.
What HPP Doesn't Do Well
I want to be clear about the limitations because the industry marketing material tends to gloss over them. HPP cannot sterilize food in the commercial sense. If you need shelf-stable product at ambient temperature, you're looking at retorting or another thermal method, not HPP alone. The technology is designed for refrigerated or frozen distribution. Expect a cold chain from processing through retail. Products with free gas volumes are problematic. Headspace air compresses and can cause package deformation or, in worse cases, create localized pressure differentials that leave parts of the product under-processed. You need vacuum packaging or skin packaging for almost everything you process. Product design sometimes has to accommodate the packaging constraints rather than the other way around. Cost is the other real limitation. A production-scale HPP unit runs into the millions of dollars. Operating costs per batch are relatively low once you have the equipment, but the capital barrier is steep. Small producers often use co-packing services, which adds cost per unit but avoids the capital outlay. The breakeven depends heavily on throughput. Processing 200 batches per week makes the economics work much better than processing 20.
If you're working with a product that needs ambient shelf stability and can tolerate mild heat, there's no reason to force HPP into the process. Pasteurization or athermic methods might be simpler and cheaper. HPP is the right choice when you need to eliminate pathogens and extend shelf life while maintaining a fresh, uncooked flavor profile that heat simply cannot deliver.