The Unsexy Origin Story Of A Field Nobody Talks About Properly
Chemical engineering didn't start in a university lecture hall. It started because someone needed to make more soap, more explosives, or more ammonia faster than a batch process allowed. The earliest practical roots stretch back to the 1800s, when British engineer John Gorrie built a large-scale distillation unit for gas purification and others were building continuous acid plants. The Royal Society of Chemistry held its first proper lectures on unit operations in the late 1800s. That's the raw
History Of Chemical Engineering
before anyone gave it a textbook definition.
MIT established the first dedicated program in the United States in 1888. The UK followed roughly a decade later. But the discipline as we recognize it today really crystallized during World War I and again during World War II, when governments needed synthetic fuels, explosives, and pharmaceuticals produced at industrial scale. Lab chemistry and factory production are completely different problems. The gap between them is what chemical engineering exists to fill.
What The Word Actually Means In Practice
Unit operations is the framework most practicing engineers still use, even if they don't say it out loud. Distillation, absorption, evaporation, crystallization, filtration, drying, heat exchange — those are the building blocks. You break a complex process down into those chunks and size each one individually. The trick is realizing that a separation column in a textbook and a separation column on a plant floor behave very differently because real feeds contain impurities, foaming agents, and trace metals that don't appear in ideal equilibrium diagrams.
I spent a week troubleshooting a continuous extractor that kept choking. The manufacturer's specs said it handled 99.7 percent purity feed. Our feed was 94 percent and contained suspended particulates that the vendor had never considered. The workaround was installing a 5-micron cartridge filter upstream and switching to a pulsed sieve-tray column instead of the standard valve tray design. No one in the original process design had accounted for that.
Why Scale-Up Fails And What Nobody Warns You About
Scaling from a 500-milliliter flask to a 50,000-gallon reactor is not a linear multiplication. Heat transfer area scales with the square of the dimension but volume scales with the cube. Your exothermic reaction that took three minutes to cool in the lab might take four hours in the full-scale vessel, and if your cooling jacket can't remove the heat fast enough, you get thermal runaway. This is the single most common failure mode in pilot-to-production transitions.
During a project involving an exothermic polymerization last year, the pilot plant ran fine at five-kilogram batches. The production run at five hundred kilograms spiked to 140 degrees Celsius instead of holding at 110. The cooling system was adequate on paper. What we missed was that viscosity increased dramatically as conversion progressed, which killed the heat transfer coefficient inside the reactor. We solved it by switching to a semi-batch feed strategy where monomer was added gradually instead of all at once, keeping the reaction mixture thinner and more manageable thermally.
Thermodynamics Versus Kinetics — The Part Where Beginners Get Tripped Up
A reaction might be thermodynamically favorable at room temperature but kinetically frozen. That means it will never proceed at a meaningful rate without a catalyst or elevated temperature. Conversely, a kinetically fast reaction might produce unwanted byproducts because the thermodynamics favor them at higher temperatures. The equilibrium between these two forces determines everything about reactor design, and most junior engineers I've seen skip straight to kinetic data without checking whether the reaction is even thermodynamically viable under their proposed conditions.
The Le Chatelier principle is not just exam material. I once watched a team design a methanol synthesis loop that ignored the effect of inert buildup on partial pressures. After three weeks of operation, conversion dropped by 40 percent and they couldn't figure out why until someone calculated the actual mole fractions in the recycle stream.
The Computational Turn And Why It Didn't Solve Everything
Process simulation software like Aspen Plus and HYSYS changed the field dramatically starting in the 1980s. You can now model an entire refinery or petrochemical plant before pouring a single dollar of construction budget. The tradeoff is that these tools are only as good as the property packages and assumptions you feed them. A simulation will give you an answer with twelve significant figures even when your underlying thermodynamic model has an error margin of plus or minus 15 percent. Trusting the output blindly is a well-documented career mistake.
I've seen a complete ethylene cracker train designed around a simulation that underestimated coking rates by a factor of two because the vendor used a generic kinetic model instead of site-specific feedstock data. The plant shut down for decoking every six weeks instead of the projected sixteen. Retrofitting the furnace tubes with internal scalpers and adjusting the steam-to-hydrocarbon ratio brought the cycle time back to something operational.
Professional Structures And Where The Field Stands Now
The American Institute of Chemical Engineers formed in 1908. The Institution of Chemical Engineers in the UK came later in 1922. These organizations standardised curriculum, set examination pathways, and created the professional identity that let chemical engineering claim independence from chemistry and mechanical engineering departments. That separation still causes friction in some universities where the programs overlap heavily in the first two years.
Modern chemical engineering now extends into bioprocessing, pharmaceutical manufacturing, semiconductor fabrication, and environmental remediation. The core principles — mass balance, energy balance, transport phenomena, and reaction engineering — haven't changed materially since the 1950s. What changed is the scale, the regulatory environment, and the computational tools available for optimization.
The field is also currently dealing with the tension between legacy infrastructure and decarbonization targets. Carbon capture retrofits on existing plants require process integration skills that most engineers learned from textbooks written before climate policy became a design constraint. The theory is sound. The implementation is where the actual engineering work happens.
Gallery History Of Chemical Engineering
The History of Chemical Engineering - How it Changed the World! - YouTube
Your weekend read: History of chemical engineering at Berkeley | College of Chemistry
Chemical engineering for the Anthropocene - Horio - 2023 - The Canadian Journal of Chemical ...
Chemical and Biological Engineering History | Drexel Engineering
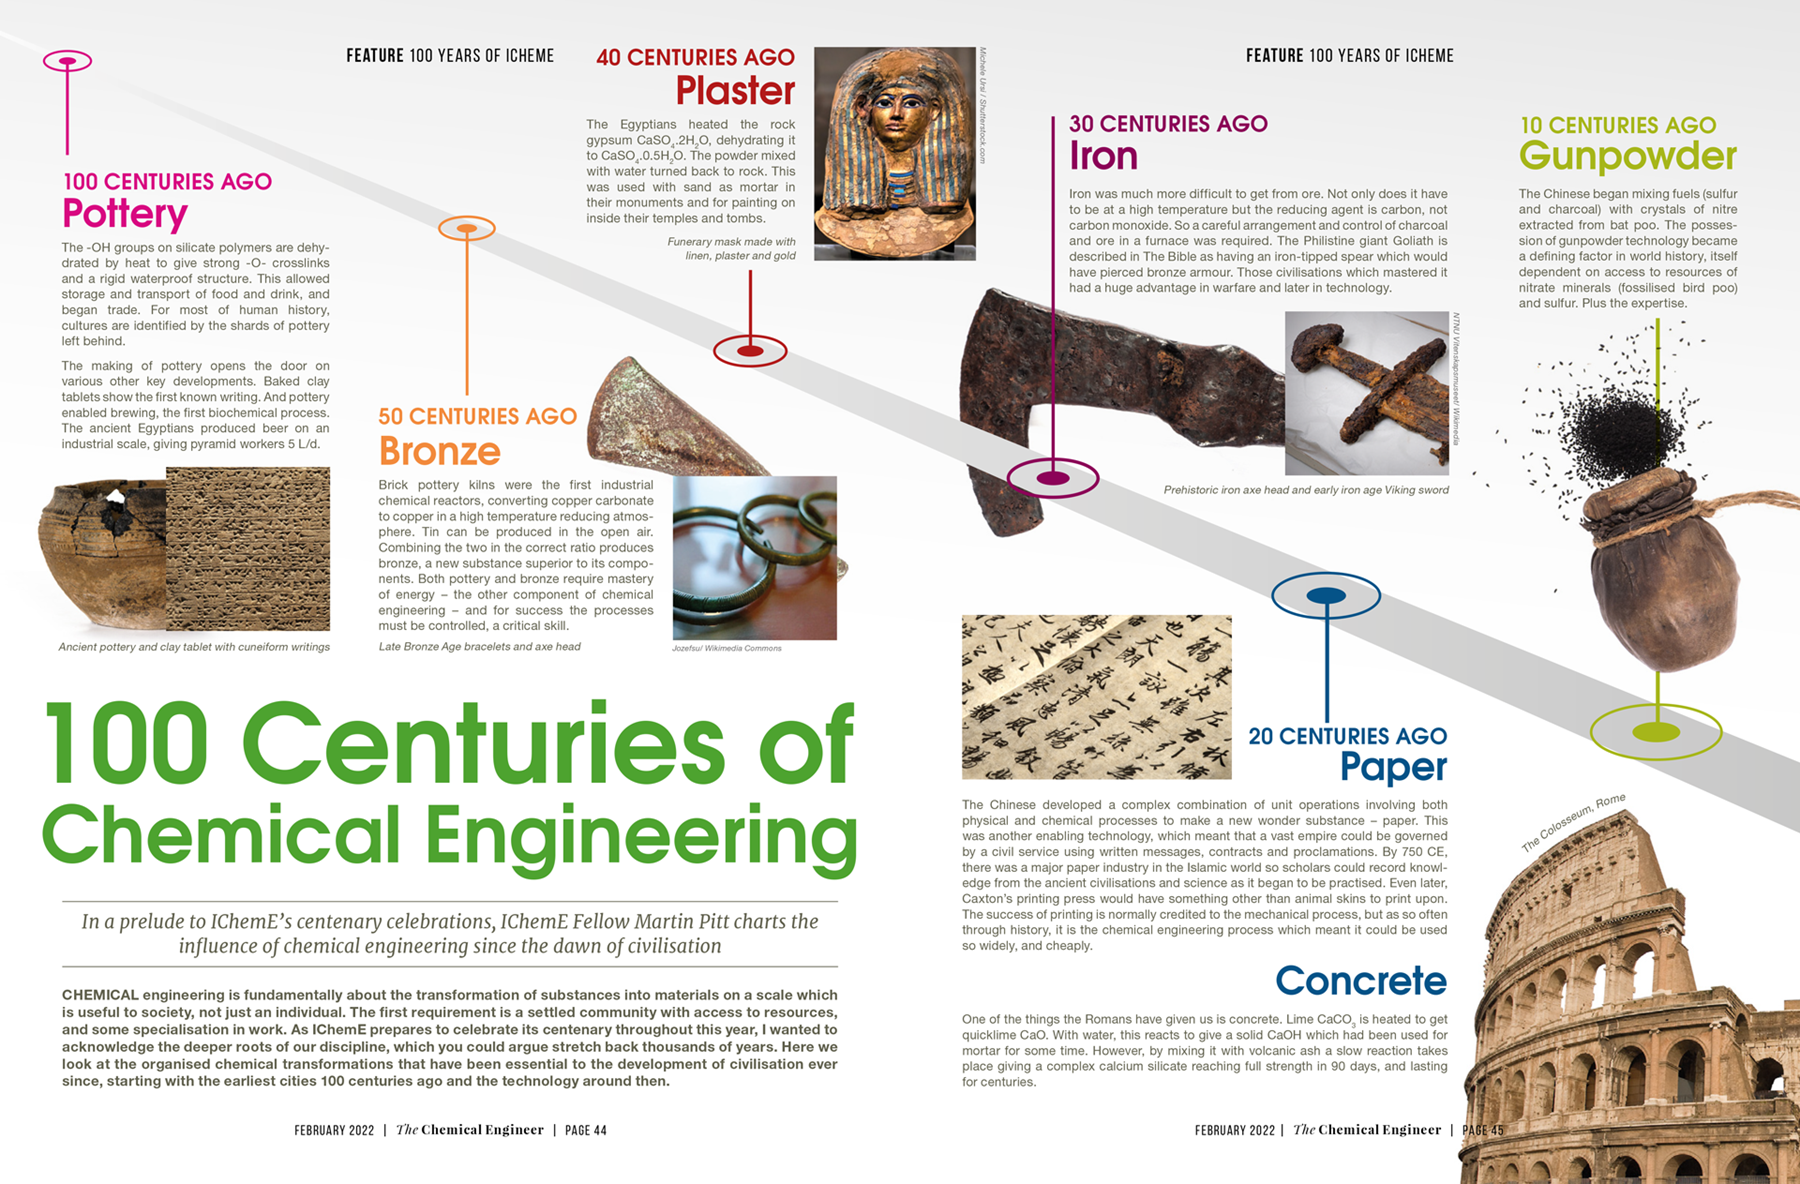
100 Centuries of Chemical Engineering - Features - The Chemical Engineer