Understanding Vase Mode in 3D Printing
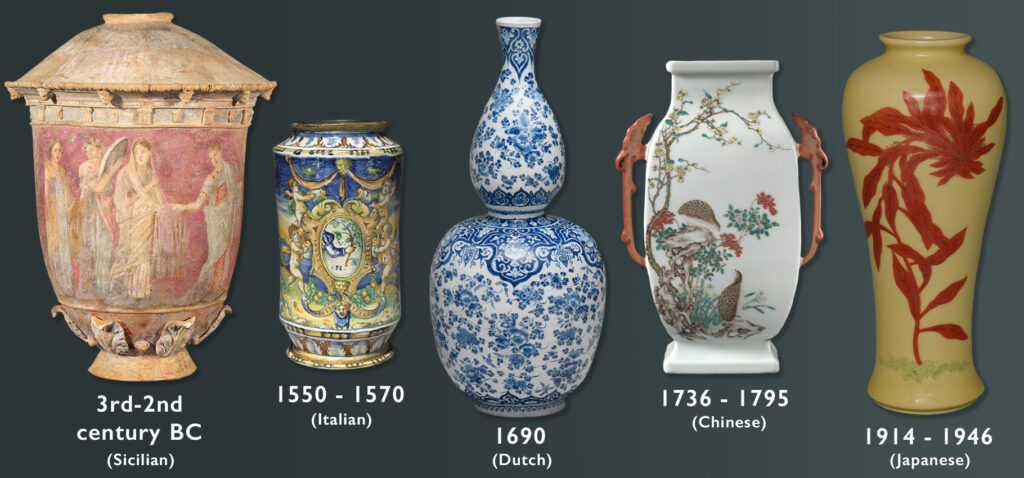
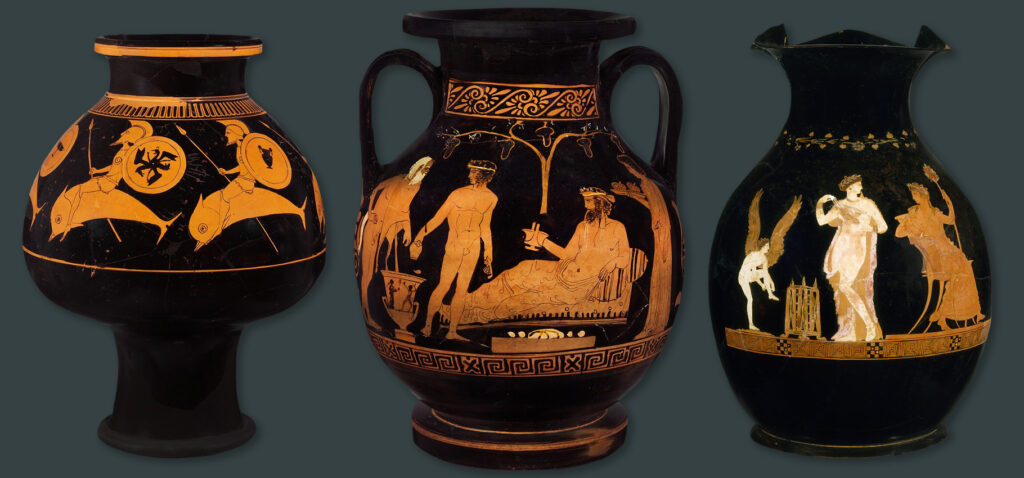
History Of The Vase
Vase mode is one of those slicer features that sounds obvious once you explain it but catches most people off guard when they first try it. The core idea is simple: instead of building a solid object with infill and multiple perimeters, the printer extrudes a single continuous spiral wall from bottom to top. No starting and stopping at layer boundaries. No visible seams. It turns out that for the right kinds of models, this cuts print time dramatically while also producing surfaces that look like they were machine-milled rather than FDM-printed. People started experimenting with spiral-only printing patterns early in the FDM era because the visual result was striking. What became known as "vase mode" in firmware and slicers was essentially a shortcut that disabled the Z-hop and retraction behavior between layers. Rather than lifting the nozzle, pausing, and restarting at the top of each new ring, the printer keeps the nozzle at a constant height relative to the build plate and maintains continuous extrusion. The result is a seamless outer shell. I spent a lot of time troubleshooting a batch of vases that had tiny vertical string lines appearing at regular intervals. It took me a few prints to realize the issue was not the nozzle or the filament. The problem was that my slicer was not actually running true spiral mode. I had enabled vase mode but left the "keep nozzle clean" option active, which caused intermittent pause-and-retract cycles that reintroduced visible artifacts. Disabling that option fixed the issue entirely.
How Vase Mode Actually Works
The slicing process for a vase-mode object works differently from a standard solid print. The slicer generates a single perimeter path that spirals upward continuously. There is no top or bottom solid layer. There is no infill. The model essentially becomes a hollow container defined entirely by the spiral wall thickness. In Cura, you enable this through the print settings by selecting the "Spiral Vase" option, sometimes listed as "Smooth Spiral vase" depending on the version. PrusaSlicer refers to it as "Spiralize outer contour." Both approaches do the same thing: they force the toolpath generator to treat the object as a single continuous loop with no vertical discontinuities. The thickness of the vase wall is determined by your nozzle diameter and the perimeter width setting. A standard 0.4 mm nozzle typically produces a wall close to 0.4 mm when set to 100% perimeter width. If you need a thicker wall, you can increase the perimeter width, but that also increases the chance of the spiral path bulging outward or the extruder struggling to maintain consistent flow. I usually keep vase prints at or near standard perimeter width settings unless I am using a larger nozzle.
When Vase Mode Makes Sense
This technique is useful for decorative objects, plant pots, lamp shades, and any geometry that does not require structural strength. Because there is no infill and only a single perimeter, vase-mode prints are inherently weak under lateral stress. A thin-walled vase printed this way will crack if you drop it or apply sideways pressure. The main advantage is speed. A vase that might take two hours in normal mode can print in twenty to thirty minutes depending on size and layer height. That speed gain comes from eliminating retracts, Z-hops, infill generation, and top/bottom layer passes. You also get a surface quality that would normally require extensive sanding or chemical smoothing. There are scenarios where vase mode simply does not work. Models with overhangs that exceed your printer's natural bridging capability will sag or collapse. Complex geometry with internal cavities that require multiple walls will not slice correctly. Objects that need a flat base for stability will have issues because vase mode leaves the bottom open by default.
Get the Full Details
Practical Settings to Consider
Layer height for vase prints should be chosen carefully. Taller layers create a more pronounced spiral texture, which can look deliberate and decorative or visually noisy depending on the context. I generally prefer 0.2 mm layer height for medium vases and 0.1 mm for smaller detailed pieces. Anything finer than 0.1 mm rarely improves appearance noticeably and slows the print without adding visible benefit. Print speed is another factor that matters more in vase mode than in standard printing. Since the extruder is moving continuously without pauses, the motor steps and extrusion consistency are under constant demand. I usually run vase-mode prints at about 50 to 60 mm/s. Going much faster tends to cause under-extrusion along the spiral because the stepper loses steps or the hotend cannot keep up with sustained flow. Retraction settings are largely irrelevant in true vase mode because retraction is disabled during the spiral. However, you still need reasonable retraction values for the initial and final extrusion passes. A small retraction distance of about 1 mm at a moderate speed is sufficient for most Bowden and direct-drive setups.
Common Pitfalls and Edge Cases
One issue that comes up frequently is the seam appearing as a visible ridge somewhere around the middle or upper portion of the print. This happens because the slicer must place a start point where the spiral begins, and that join can show up as a slight bump. The position of that join is controlled by the starting angle setting in your slicer. Moving the start angle to a less visible location on the model can help, but it will not eliminate the bump entirely. Another problem is uneven wall thickness. If the model has areas where the spiral path crosses itself or passes very close to another part of the same wall, the extruder may deposit extra material in that region. I ran into this with a cylindrical vase that had a decorative pattern sliced into the side. The pattern created localized areas where the spiral doubled back on itself, producing thick spots that ruined the smooth appearance. The workaround was to simplify the model geometry and remove the pattern before slicing. For decorative vases, it is better to post-process surface details rather than trying to encode them into the spiral path. There is also the matter of support structures. Vase mode generally does not support themselves overhangs, and adding supports is counterproductive because removing them would ruin the seamless wall. If your design requires an overhang, you need to redesign it or accept that vase mode is not the right approach for that particular geometry.
Alternatives When Vase Mode Fails
If vase mode cannot produce the result you want, there are other approaches. Printing a standard solid vase with a single perimeter and minimal infill can provide similar aesthetics with more structural integrity. Setting the infill to 5 to 10 percent and using a grid or cubic pattern adds a small amount of internal support without significantly increasing print time. This also gives you a sealed bottom and top, which vase mode lacks by default. For objects that require strength and a smooth exterior simultaneously, hybrid settings work better. You can enable standard perimeters and infill while also using a spiral first layer to create a strong base. Then print the rest of the model normally. This gives you the best of both approaches for certain geometries. Another option is post-processing. A vase printed in standard mode with 0.1 mm layer height and a high perimeter count can often be smoothed with a heat gun, sanding, or chemical treatments depending on the filament type. PLA responds reasonably well to sanding, while ABS can be smoothed with acetone vapor. This route takes more time upfront but produces stronger final parts.
The short version is that vase mode is a specialized tool. It works well for specific geometries and delivers fast prints with clean surfaces, but it has hard limitations around structural strength, overhangs, and seam visibility. Understanding those boundaries and knowing when to switch strategies is what separates a reliable workflow from a frustrating one.


