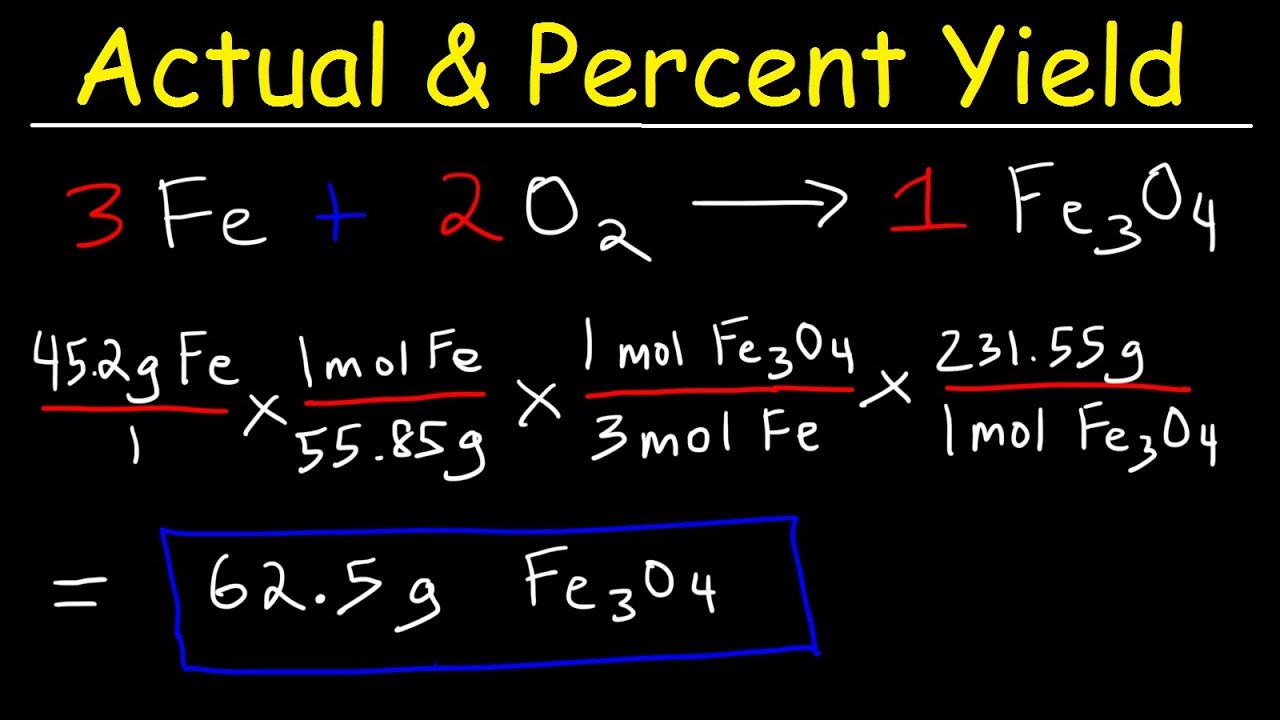
Calculating percent yield starts with knowing what you actually got, not what the textbook says you should get.
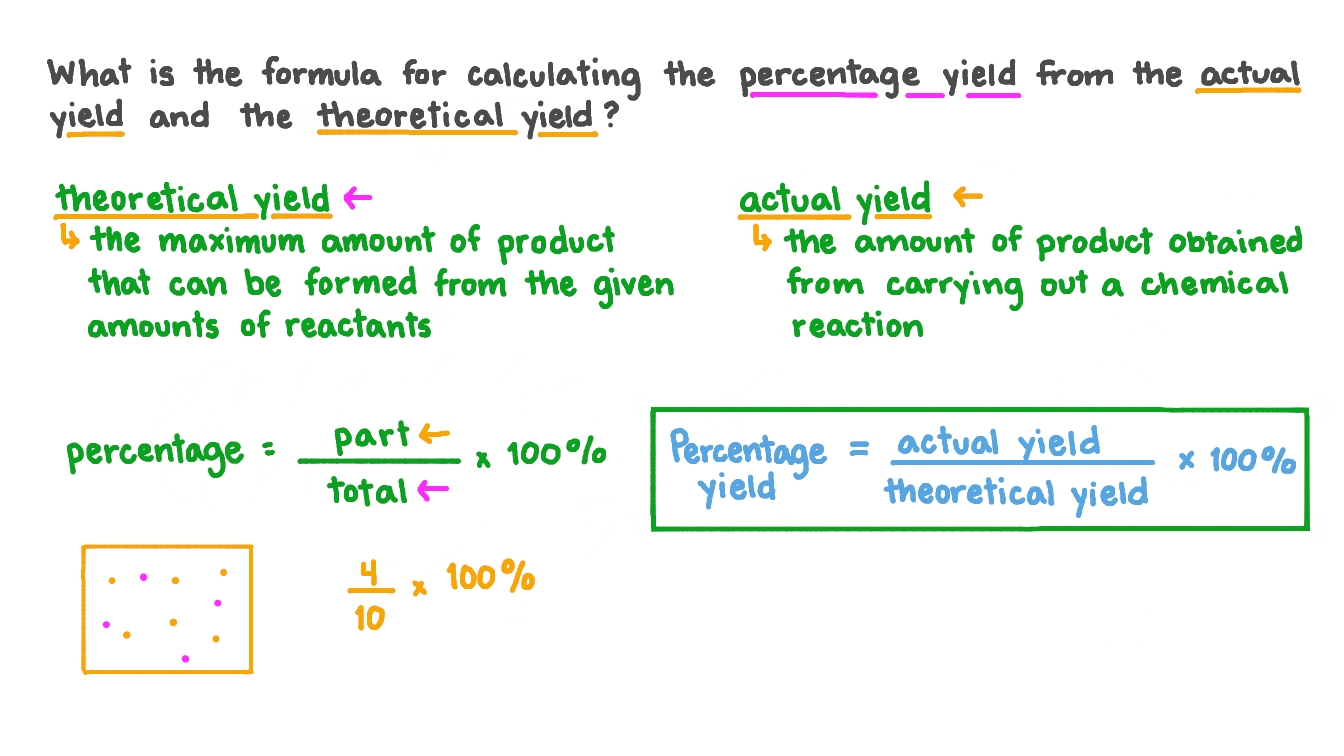
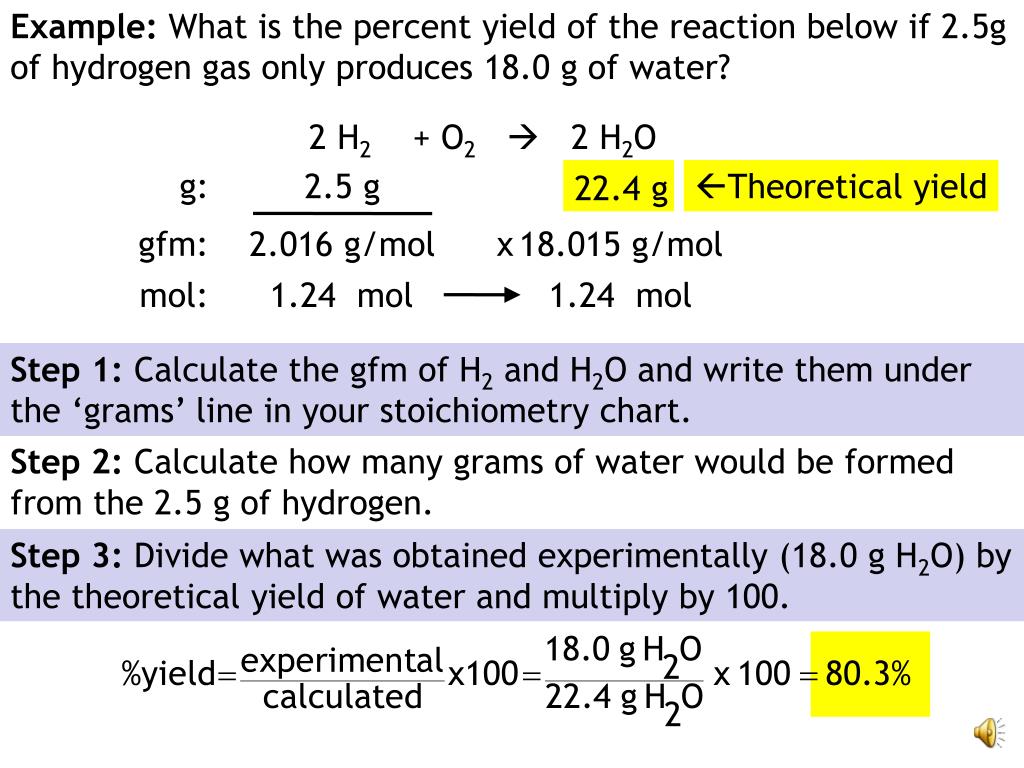
The method is straightforward if you keep track of your numbers. You run the reaction, isolate your product, weigh it. That's your actual yield. Then you calculate what the yield would be if every single molecule of your limiting reagent turned into product with zero losses. That's your theoretical yield. Divide actual by theoretical and multiply by 100. The result is your percent yield. Nothing complicated about the arithmetic. What makes it tricky is the chemistry between the two numbers. Write the balanced equation. Identify your limiting reagent by comparing moles. Use stoichiometry to calculate the maximum moles of product possible. Convert that to grams using the molar mass of your product. Weigh the dry product you collected. Plug into the formula. Percent Yield = (Actual Yield / Theoretical Yield) × 100
That's the definition, but definitions don't save you when you're holding a flask of wet powder. I learned that the hard way during a routine Grignard reaction. Theoretical yield came out to 4.2 grams based on the magnesium turnings I used. I dried the product under vacuum for three hours, weighed it, and got 4.8 grams. Eighty-six percent yield should be impossible unless something was wrong. It was. The product still contained ether and a trace of water from the workup. I dried it longer at higher vacuum and got 3.6 grams instead. Real percent yield was 86%, not 114%. The formula didn't change. My handling of the product did. This happens more often than people admit. Theoretical yield assumes perfect conditions: complete conversion, no side reactions, no material lost during transfer, no product left stuck to filter paper or glassware. None of that happens in practice. You will lose material. Filtration leaves product behind. Transferring between containers leaves residue. Recrystallization recovers only what's insoluble in cold solvent. These aren't failures of calculation. They're reality. A few things people miss when they calculate percent yield for the first time. First, percent yield has no upper limit in theory but practically anything over 100% means your product is impure or wet. That's usually the first warning sign. Second, percent yield and percent conversion are not the same thing. Conversion tells you how much starting material reacted. Yield tells you how much of the desired product you isolated. A reaction can have 95% conversion but only 40% yield if half the converted material went to a side product. Third, the limiting reagent determines theoretical yield, but sometimes you have excess reagent because the reaction is equilibrium-limited and you're driving it forward. In those cases, the "limiting" reagent isn't really limiting the yield anymore, and your theoretical calculation becomes less useful as a benchmark.
I worked with a Suzuki coupling once where the theoretical yield was based on the aryl halide. The palladium catalyst deactivated partway through and the reaction stalled at about 60% conversion. My percent yield was 52%, which looked mediocre on paper. The real issue wasn't isolation loss. It was catalyst death. Increasing the catalyst loading or switching to a more robust ligand fixed it. Percent yield told me something was wrong but not what was wrong. That's the limitation of the metric. It's a summary number, not a diagnostic tool. Another edge case that comes up: reactions where the product is a liquid and you measure volume instead of mass. Converting volume to mass requires knowing the density of your pure product, which you might not have on hand. You can look it up, but if your product isn't pure, the density won't match the literature value and your mass calculation will be off. Always weigh when you can. It removes a variable. When percent yield really breaks down is in polymer synthesis or reactions producing mixtures of isomers. If you're making a polymer, the molecular weight distribution affects how much you recover at different stages of precipitation. If you're producing a mixture of ortho, meta, and para isomers and only isolate one, your percent yield is relative to that specific isomer, not the total product formed. People sometimes report combined isomer yield without making that clear, which makes comparison across papers unreliable.
Get the Full Details
If you need a faster way to track yield across multiple runs without doing full stoichiometric calculations each time, some labs use an internal standard in the reaction mixture and analyze by NMR or HPLC. You get a relative yield quickly, then confirm with isolation and weighing later. It cuts down on characterization time for optimization screens. The tradeoff is that it only works if your internal standard doesn't interfere with the reaction and you have a clean spectrum or chromatogram to read. It's a practical shortcut, not a replacement for the standard method. The core problem with percent yield as a metric is that it rewards careful technique over smart chemistry. A student who carefully transfers every drop and scrubs their flask clean will often report a higher yield than someone who designed a better reaction but was sloppy with workup. Neither number fully captures how good the reaction actually is. That's why people in the field also look at isolated yield, crude yield, and reaction mass efficiency depending on what they're optimizing. Percent yield is one data point. It's useful, but it's not the whole picture. If you're just starting out, make sure your product is completely dry before weighing. Use a balance with at least 0.001 gram precision. Record the mass of your container before and after adding the product so you can account for any residue left behind. Write down your theoretical yield calculation alongside your actual yield so you can trace back where the gap came from. A 70% yield isn't inherently bad. A 70% yield you can't explain is the problem.