The Actual Process
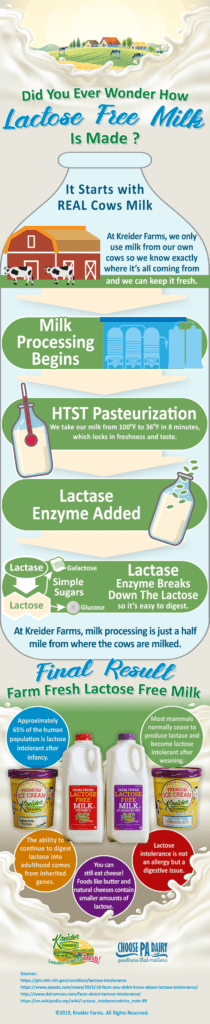
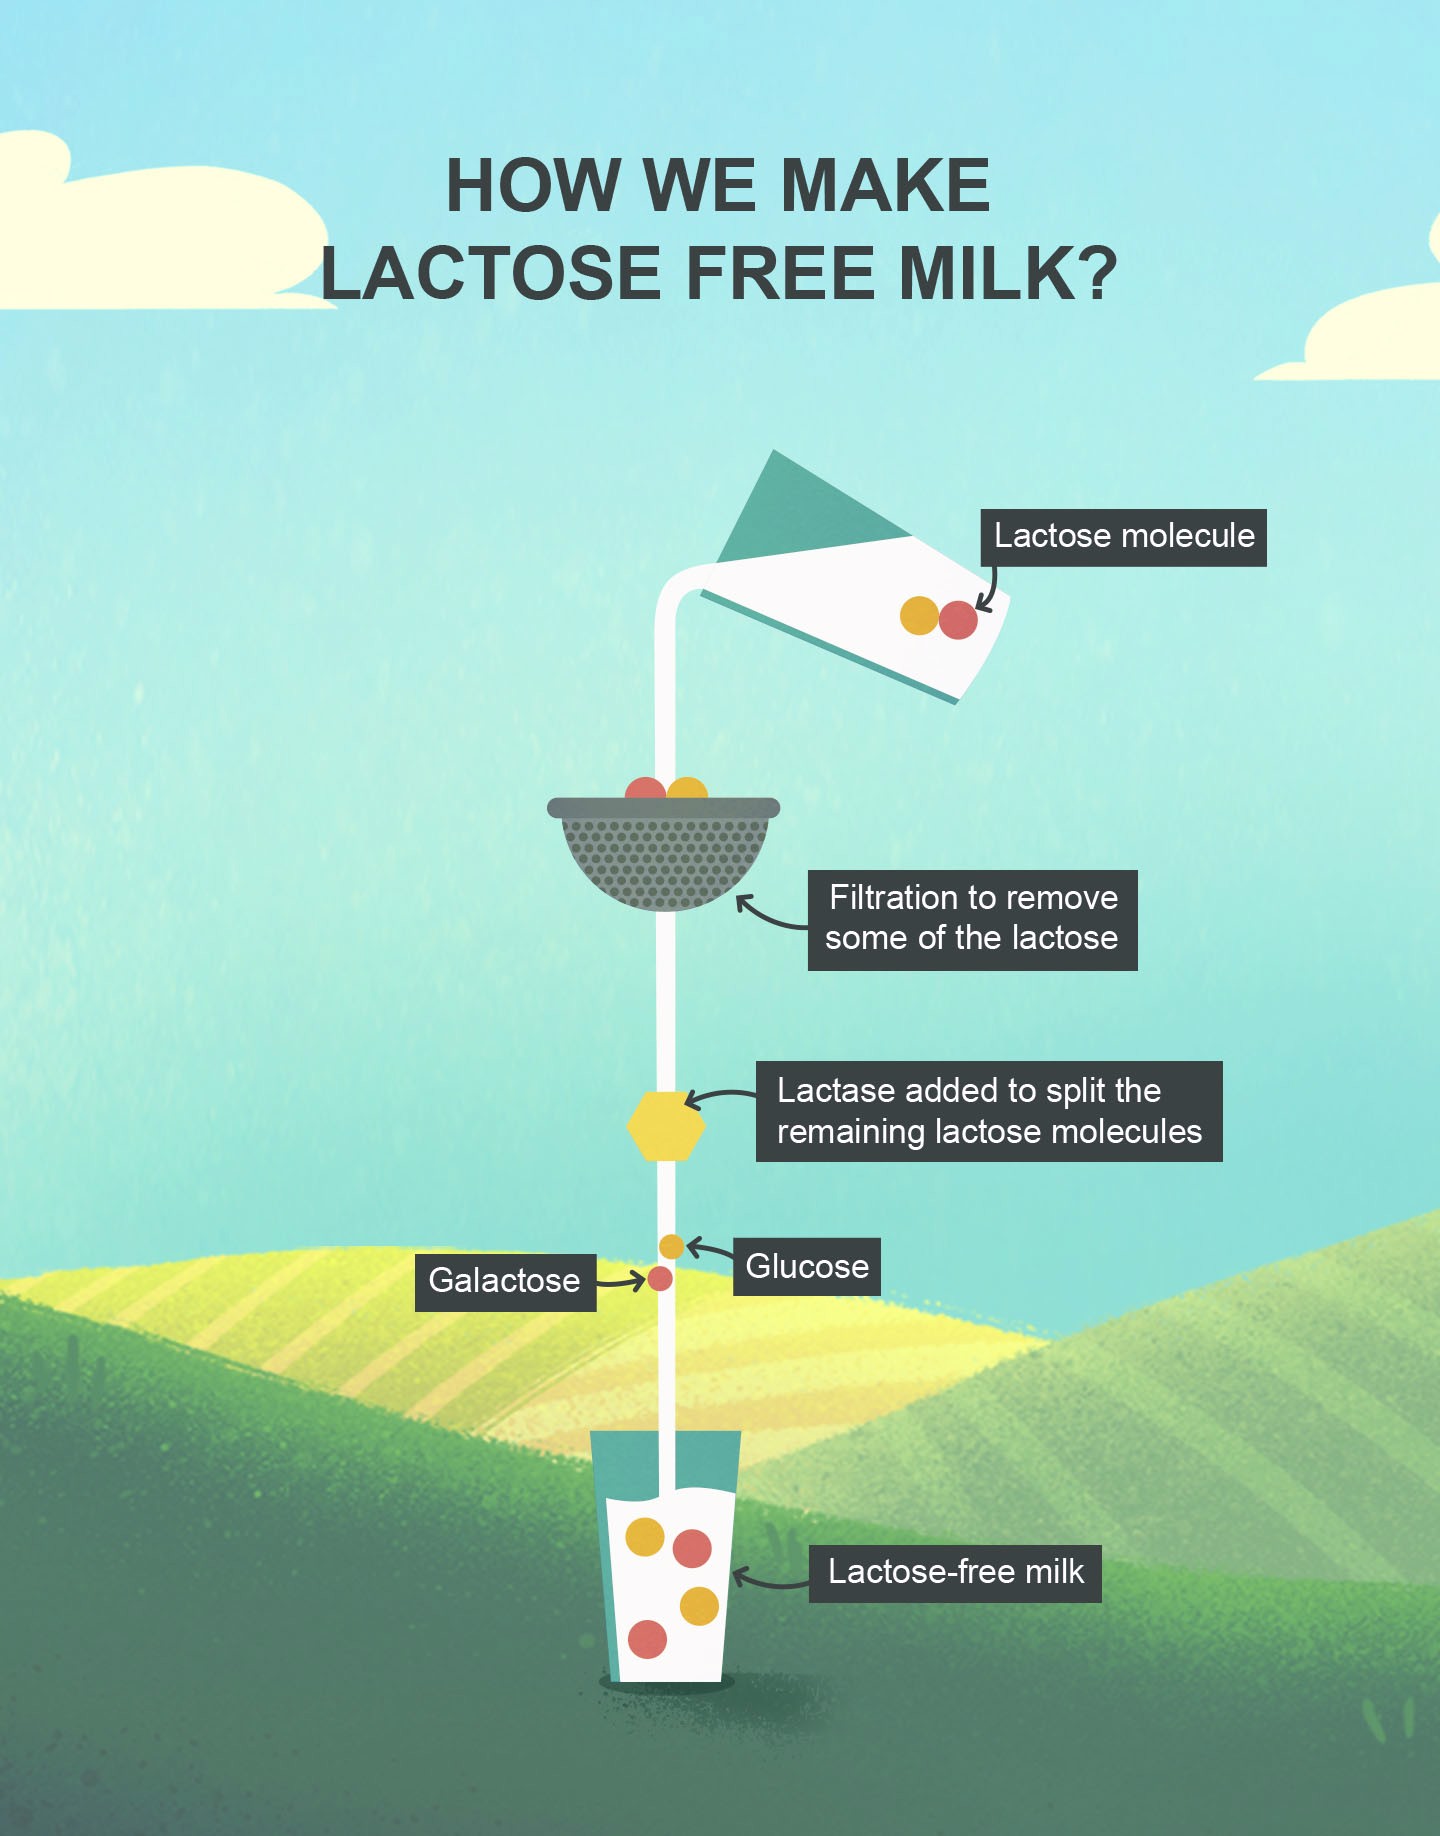
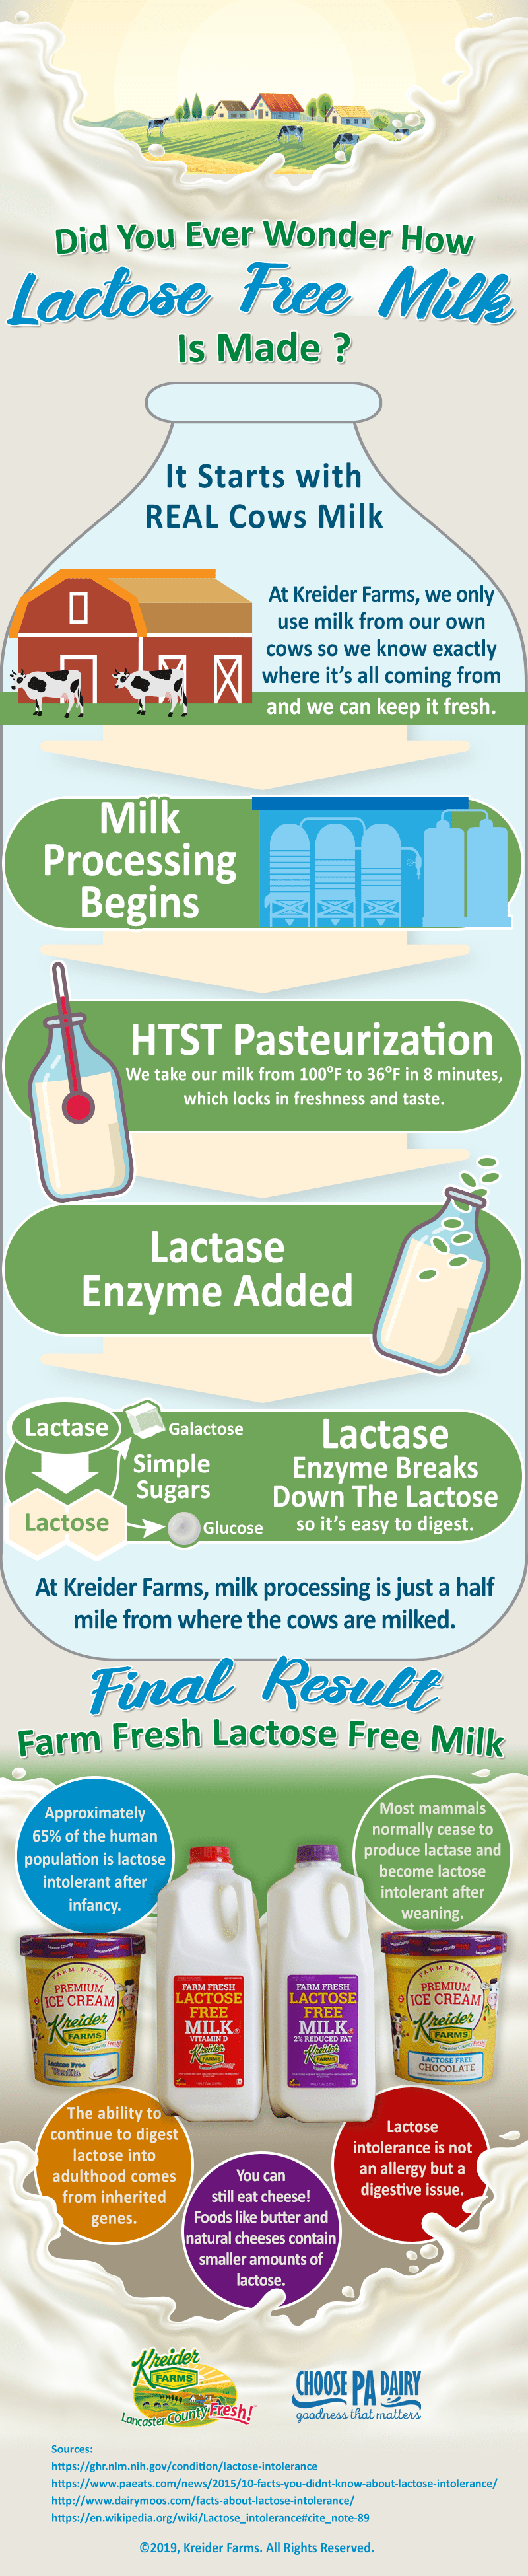
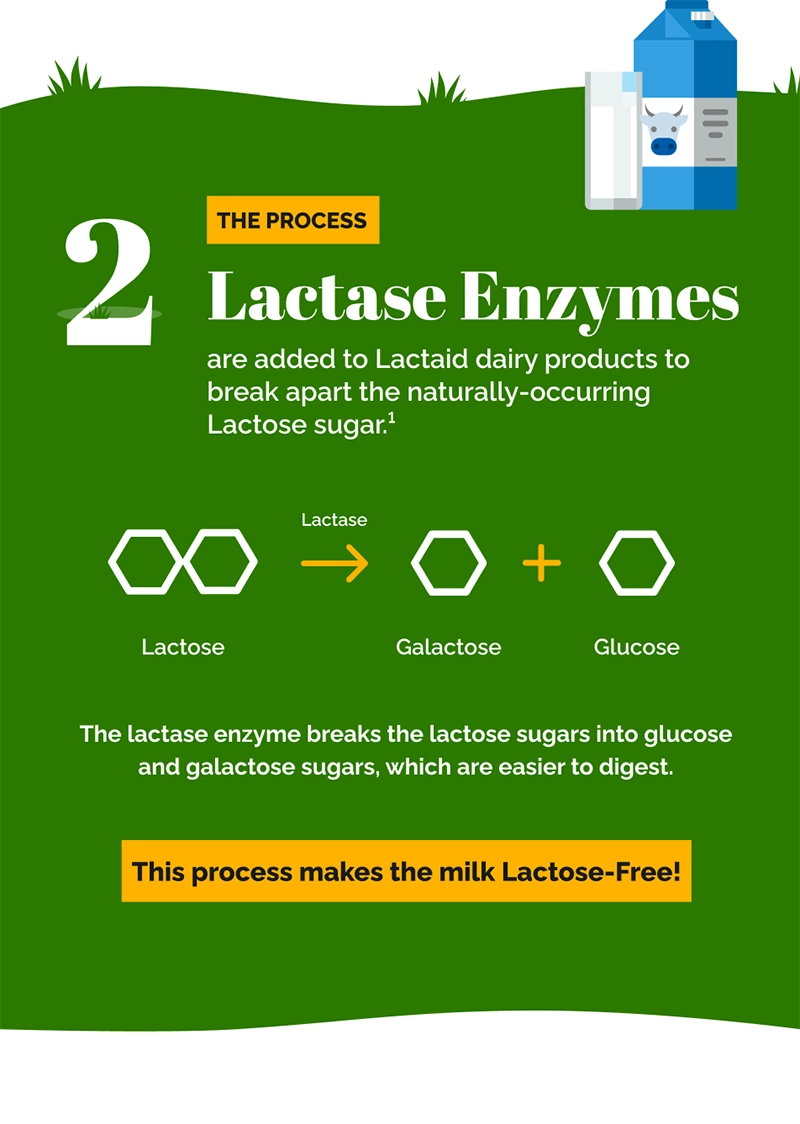
Lactose-free milk starts exactly the same as regular milk. You get the cow, you milk the cow, you pasteurize it. The only difference comes after that point, and it involves an enzyme you can buy from a biochemistry supplier if you ever need it. The enzyme is called lactase, sometimes referred to as beta-galactosidase. You add it to the milk, let it sit, and the lactose molecules get broken down into glucose and galactose. That's it. No magic. No chemical alteration of the protein structure. The milk still has casein, whey, fat, everything else exactly where it belongs. The reason lactose-free milk tastes sweeter is because glucose and galactose are individually sweeter than the disaccharide lactose. Your tongue registers that difference immediately, and it catches people off guard the first time they try it. Not because anything was added to the milk, but because you're literally tasting the products of the enzymatic reaction.
How Is Lactose Free Milk Made at Scale
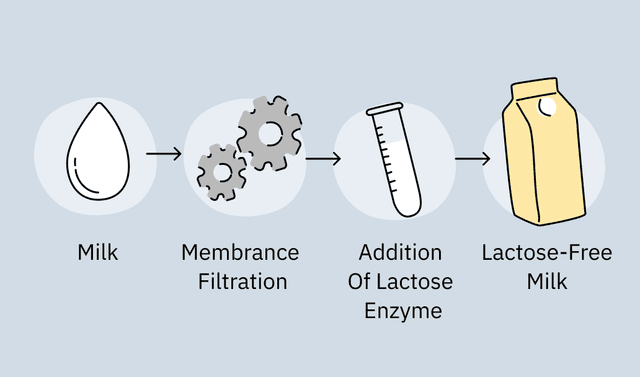
Industrial producers use a couple of approaches depending on their volume and equipment budget. The most common method is what they call batch hydrolysis. You take a tank of pasteurized milk, add a measured amount of lactase, stir it, and hold it at around 40 to 45 degrees Celsius for somewhere between four and twenty-four hours. The temperature window matters because lactase has an optimum range. Go too cold and the reaction crawls. Go too hot and the enzyme denatures and you've wasted both the enzyme and whatever you were doing to keep it warm. The alternative is continuous microfiltration with enzymatic treatment. Milk gets forced through a membrane that separates out the lactose-containing fraction, which then runs through a column packed with immobilized lactase enzymes. The product streams recombine at the end. This is faster, usually completing the hydrolysis in minutes rather than hours, and it gives you tighter control over the residual lactose level. It also costs significantly more in capital equipment. A mid-sized dairy line with this setup will run into the low millions for the filtration and enzyme columns alone. There's a third route that shows up occasionally, mostly with smaller or craft producers. They add the enzyme directly to the packaged milk and hold the finished product at fridge temperature until the hydrolysis completes. This works fine for small batches but introduces a problem: the longer the milk sits with active enzyme at any temperature above refrigeration, the more you risk microbial growth before pasteurization catches it. Most producers who do this method will pasteurize again after the reaction finishes, which adds a step and a quality control checkpoint that larger facilities skip entirely.
What People Get Wrong About It
The biggest misconception is that lactose-free milk is somehow chemically different from regular milk beyond the lactose breakdown. It isn't. The protein profile, the fat content, the vitamins and minerals all remain unchanged. If you're avoiding lactose for digestive reasons, this is good news. If you're avoiding dairy for any other reason, this is not a loophole. Another thing nobody explains clearly: lactose-free milk doesn't have zero lactose. The industry standard for labeling it as lactose-free in most jurisdictions is less than 0.1 grams of lactose per 100 milliliters. That's low enough that the vast majority of people with lactose intolerance can drink it without symptoms, but it's not the same as removing lactose entirely. There are still trace amounts. A sensitive person drinking a full liter could technically be consuming up to a gram of lactose spread across that volume, which adds up if they're already near their threshold. I ran into this exact problem a couple years ago working with a small batch producer who was getting complaints from apparently lactose-sensitive customers. Turns out the lactase addition rate was correct on paper, but the mixing wasn't thorough enough in the holding tank. You'd get pockets of fully hydrolyzed milk next to pockets where the enzyme barely touched anything. The lab test came back under the 0.1g threshold because the sampling was pulling from well-mixed sections, but the actual product leaving the tank was inconsistent. The fix was switching from a simple overhead stirrer to a turbulent inline mixer right before the holding tank, which eliminated the dead zones. Took about two hours to install and calibrate.
Get the Full Details
The pH Issue Nobody Talks About
Lactase works best in a slightly acidic to neutral environment, and milk's natural pH sits right around 6.5 to 6.7, which is fine. But here's the thing most people miss: as the lactose breaks down into glucose and galactose, the osmolarity of the milk changes. Higher osmolarity can actually slow the enzyme down over time because the substrate concentration drops while the product concentration rises, and lactase does exhibit product inhibition. The glucose produced can feed back on the enzyme and reduce its activity if left too long. That's why the time windows I mentioned earlier aren't arbitrary. Push the reaction too far past the point of complete hydrolysis and you start losing efficiency on the enzyme itself, which means you're paying for more lactase than you need without getting a cleaner product. This is also why some producers adjust the pH slightly downward during the process. Dropping it to around 6.0 can actually speed up the initial reaction rate, but go too far and you start affecting the milk proteins. Casein micelles get nervous around pH 4.6 and start coming out of solution, which is basically how you accidentally make cottage cheese. It's a narrow window and it requires monitoring that most small-scale operations don't have the equipment for.
Storage and Shelf Life
UHT-treated lactose-free milk behaves slightly differently than regular UHT milk. The extra glucose and galactose introduce more reducing sugars into the system, and reducing sugars participate in Maillard reactions during thermal processing. This is why lactose-free milk sometimes develops a very subtle caramel or cooked note after extended shelf storage, even when the packaging hasn't been opened. It's not spoilage. It's just chemistry happening slowly at room temperature over months. The shelf life numbers on the carton are still accurate because manufacturers account for this, but if you've ever noticed lactose-free UHT milk tasting ever so slightly different after six months compared to the same product at two months, that's the Maillard reaction doing its thing. Nothing wrong with it. Just a side effect of having simpler sugars floating around. Regular refrigerated lactose-free milk has essentially the same shelf life as regular milk, usually around two weeks past the sell-by date if unopened and properly stored. Once opened, it's the same rules apply. Keep it cold, seal it tight, drink it within the week or two window. The enzyme doesn't keep working once the milk is in your fridge at typical household temperatures. Lactase activity drops off sharply below 10 degrees Celsius, so the hydrolysis is effectively paused after pasteurization during distribution.
Cost Considerations
Lactose-free milk costs more to produce, and that shows up at the store. The enzyme itself isn't cheap, especially the immobilized form used in continuous systems. You also need the additional quality control steps to verify residual lactose levels, which means HPLC testing or at minimum enzymatic assay kits on each batch. Labor for monitoring, equipment for mixing and temperature control, longer holding times or capital investment in microfiltration systems — all of it adds up. Retail markup typically puts lactose-free milk at a 15 to 30 percent premium over comparable regular milk, though this varies by region and brand. If you're ever tempted to try making lactose-free milk at home with a lactase supplement, it's technically possible but the results won't match commercial product. The enzyme doses in over-the-counter supplements are calibrated for individual servings, not for a whole gallon of milk. You'd need to figure out the right dosage by trial and error, maintain the temperature precisely, and accept that you won't get the consistency or the guarantee of being under 0.1 grams per 100 milliliters. It's a fun experiment if you're curious. It's not a practical way to produce a usable quantity.