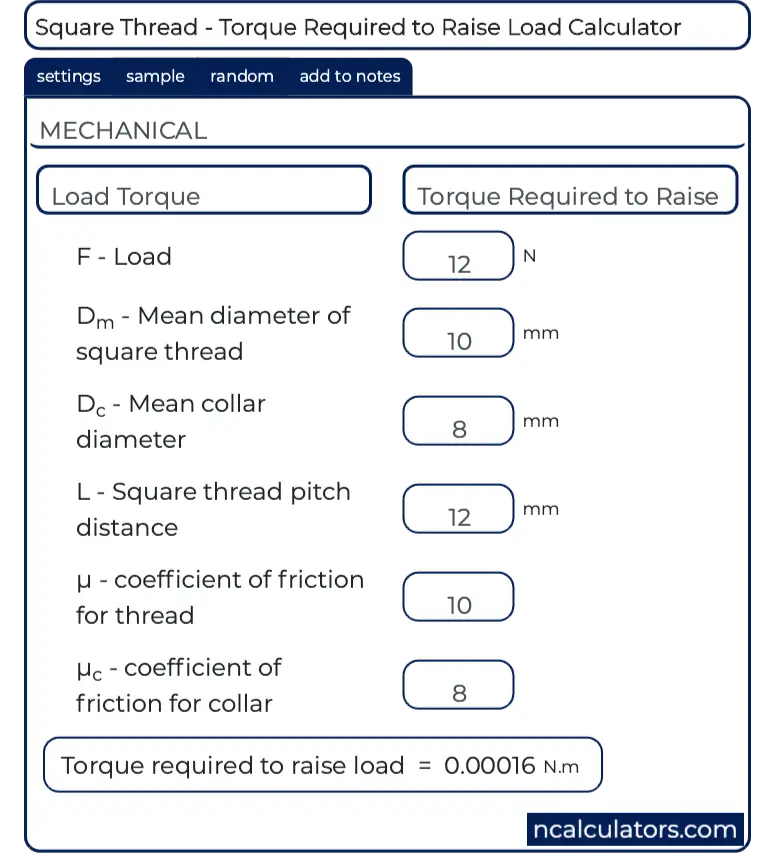
Understanding Screw Torque Calculations
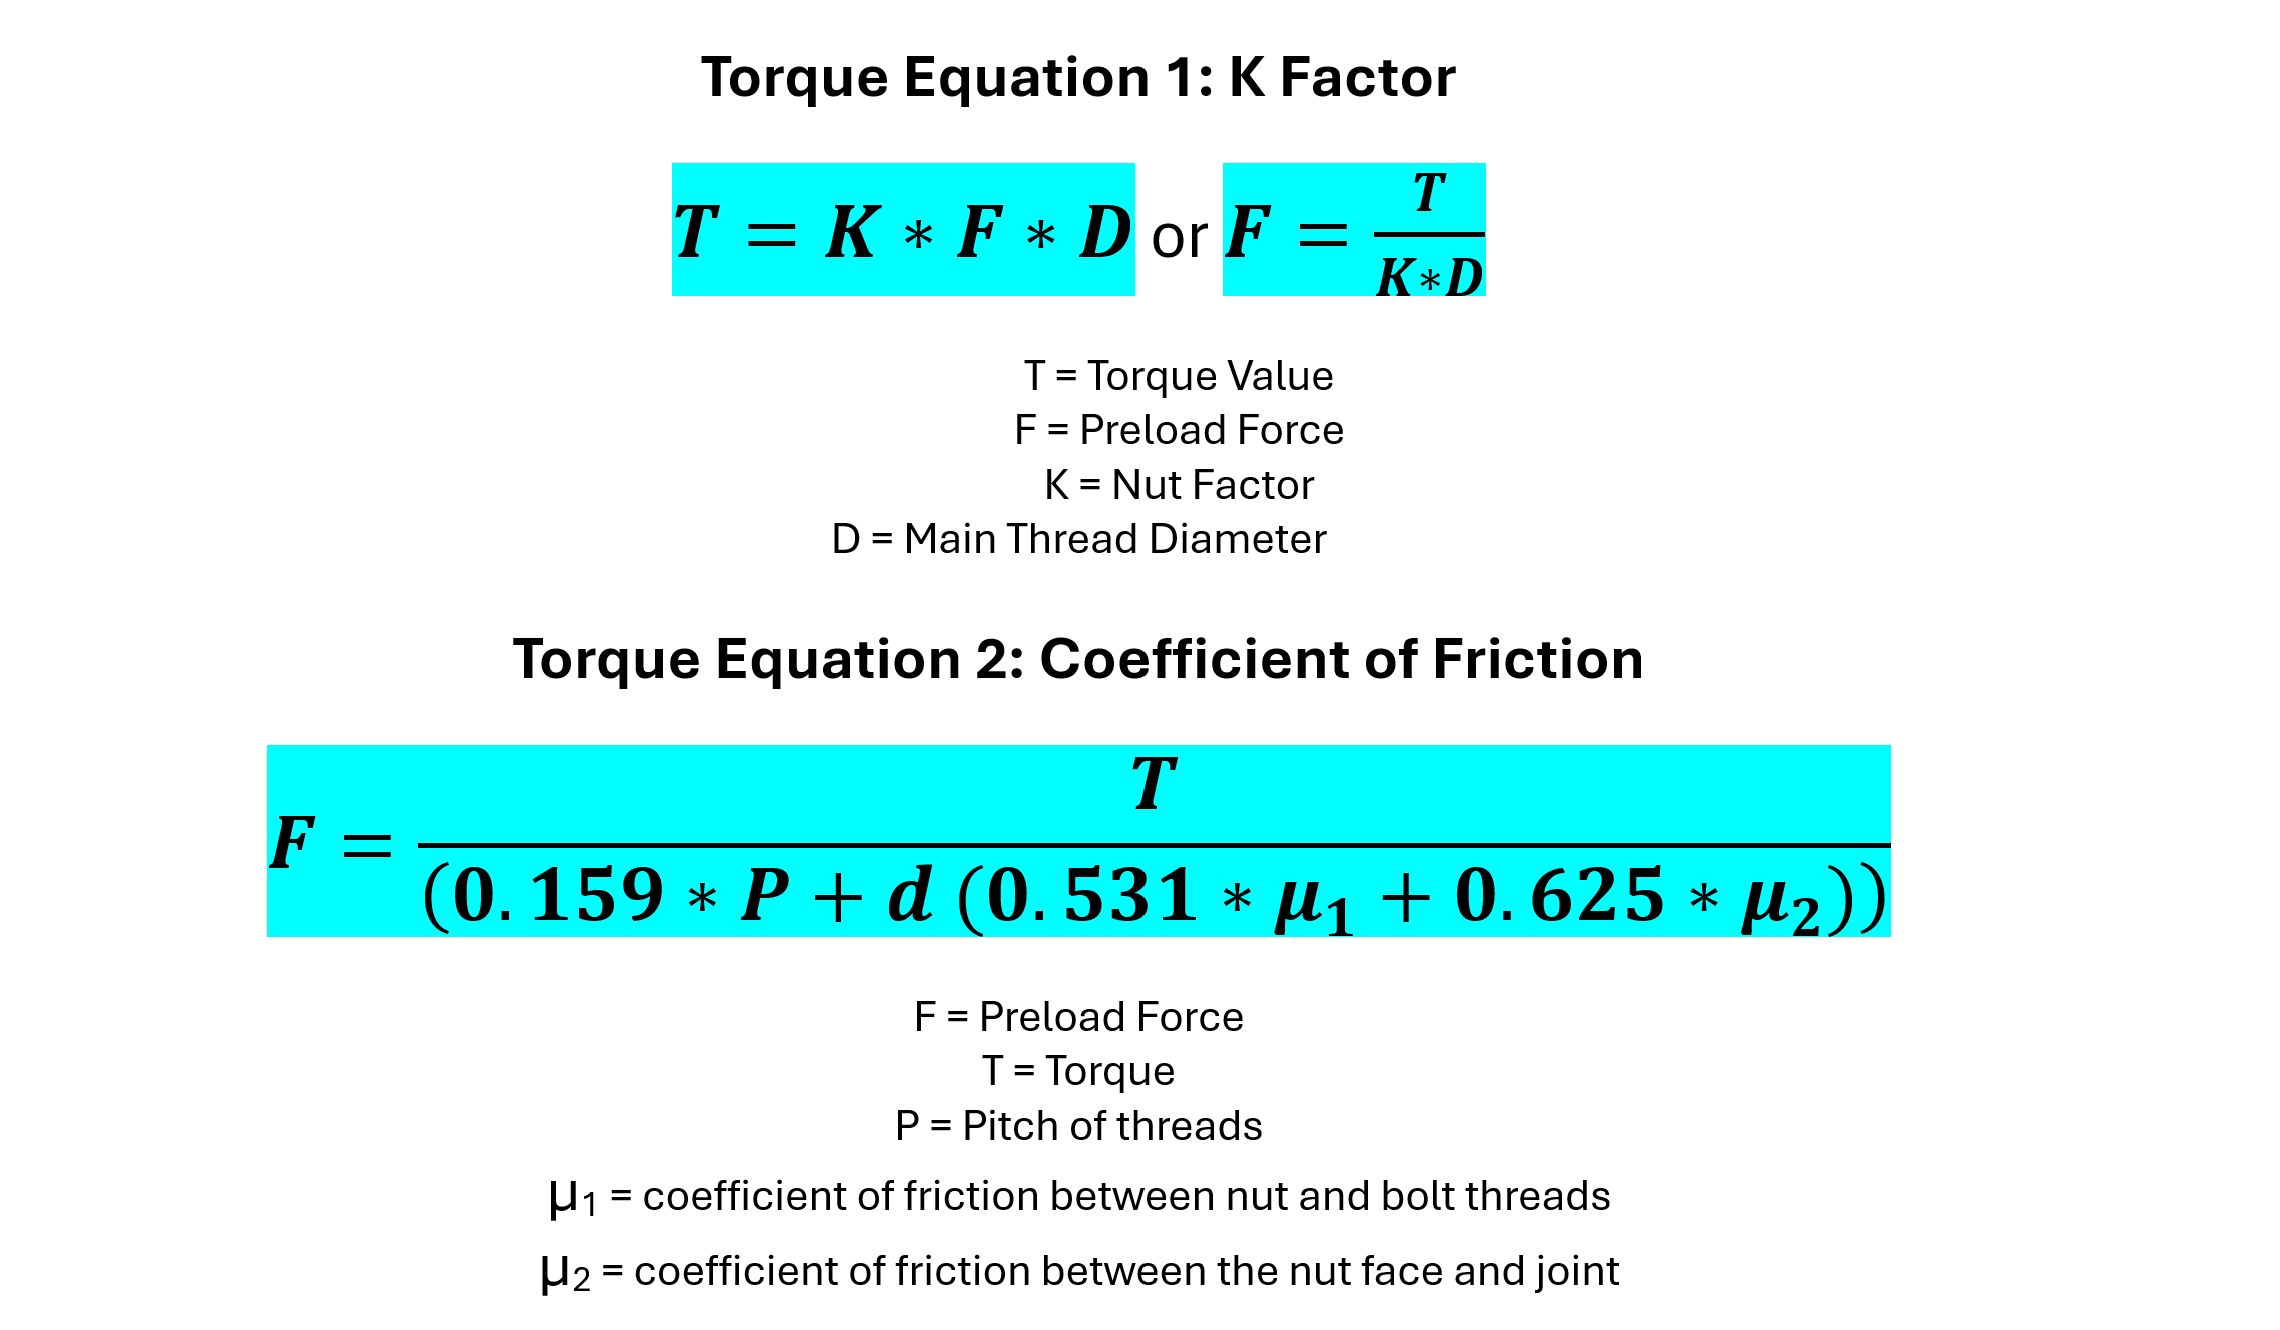
When you are tightening a screw or bolt, the torque you apply determines how much clamping force you get. Most people use a simple formula, but the reality is messier than what the textbooks show. The basic equation is T = K × D × P, where T is torque, K is the nut factor (or coefficient of friction), D is the nominal diameter, and P is the desired preload force. That is it. Everything else is just trying to figure out what K should be for your specific situation.
How To Calculate Torque Required From Screw Pitch
Here is what actually matters when you are doing this calculation. You need three things: the target preload, the screw diameter, and a realistic friction coefficient. The pitch comes into play when you are calculating the lead angle for the thread, but for most metric and UNF threads, the simplified approach works fine. I have seen engineers spend hours trying to get the perfect K value. They will measure friction with micrometers, test different lubricants, and run elaborate experiments. Then they apply it to an assembly where the actual conditions are completely different. The torque specification becomes meaningless within a few assemblies because the friction changes. Let me walk you through a practical example. Say you have an M8 bolt and you want to preload it to 80 percent of its yield strength. The tensile stress area for M8 is about 36.6 square millimeters. If the yield strength is 400 megapascals, that gives you a target force of roughly 11,700 newtons. With a friction coefficient of 0.15 for dry steel on steel, your K value would be approximately 0.2. Multiply that by the diameter (8 millimeters) and the force, and you get around 18.7 newton-meters of torque.
That number is useful as a starting point. But here is the thing that catches people out: torque and tension have a correlation coefficient of about 0.7 under normal conditions. That means 30 percent of the variation in your clamping force is just noise from friction, thread geometry, and surface conditions. If you need tighter control, you need a different approach.
Get the Full Details
The Friction Problem Nobody Talks About
The nut factor K is where everything falls apart. Manufacturers will give you a single value in their tables, but that value assumes perfect conditions. In practice, you might be dealing with zinc-plated bolts on galvanized nuts, or oil-contaminated threads from machining, or worst of all, rusty fasteners that nobody thought to clean. I worked on a project once where we specified 45 newton-meters for a set of M10 bolts. The first five assemblies felt right. By assembly twelve, the bolts were bottoming out before reaching torque, and the joint was loose. We traced it back to a batch of bolts that had been sitting in a humid warehouse for six months. The plating looked fine, but the friction had changed enough to make our torque specs completely unreliable. The workaround was straightforward. We stopped relying on torque alone and added a mark-and-wait system. Tighten to the target torque, then mark the bolt head and the mating surface. Wait ten minutes for any relaxation to occur, then check if the mark has moved. If it has, re-torque. This caught most of the issues before they became problems.
Advanced Methods When Torque Isn't Enough
If your application demands consistent clamping force, you have options beyond the standard torque calculation. Turn-of-nut method is probably the most practical. You snug the bolt, then rotate it by a specified angle, usually measured in fractions of a turn. This method is less sensitive to friction variations because you are controlling deformation rather than relying on friction coefficients. Ultrasonic measurement is the gold standard but requires expensive equipment. You measure the change in bolt length before and after tightening. The change correlates directly to the tension in the bolt. For high-value applications like pressure vessel flanges or engine head bolts, this is worth the investment. Load-indicating washers are another option. These have a calibrated spring that deflects under load. You can see exactly how much force is being applied without needing to calculate anything. They are reusable and relatively inexpensive, though not as accurate as ultrasonic methods.
Common Mistakes That Waste Time
Using the wrong friction coefficient is probably the most common error. People grab a value from a chart without considering their actual conditions. Dry steel on steel is around 0.2, but with molybdenum disulfide grease, you might drop to 0.12. With anti-seize compound, it could be as low as 0.08. That is a 40 percent difference in preload for the same torque. Another mistake is ignoring the thread pitch contribution for fine threads. The standard formula assumes coarse threads, but fine thread pitches change the lead angle enough to matter in precision applications. For an M8x1.0 fine thread compared to an M8x1.25 coarse, the torque difference can be 5 to 10 percent. People also forget about elastic interaction. When you tighten one bolt in a pattern, the adjacent bolts can lose preload as the joint settles. This is why torque sequences matter. Star patterns on flange bolts help distribute the load evenly and reduce this effect.
Quick Reference Values
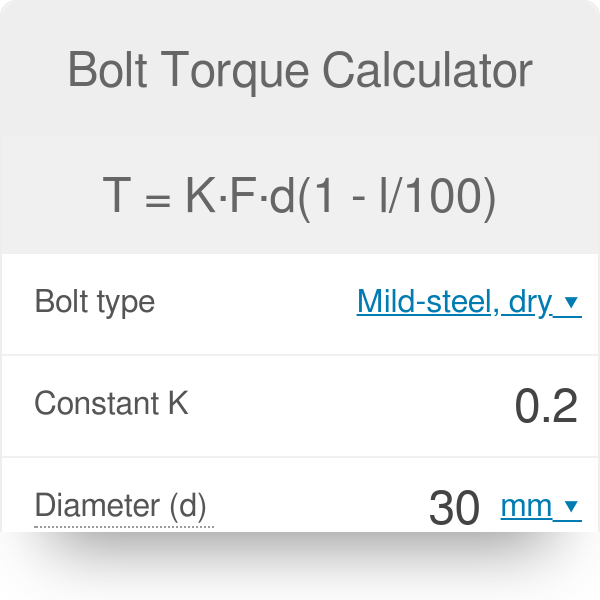
For general purpose work, a K value of 0.2 works for dry, unplated steel. Add 0.15 for lubricated steel. Use 0.12 for bolts with molybdenum disulfide grease. Drop to 0.08 only when you have proper anti-seize compound applied correctly. Here is a rough guide for common bolt sizes and their approximate torque values at 80 percent yield with dry conditions: M4: about 3 newton-meters
M6: about 9 newton-meters M8: about 23 newton-meters M10: about 53 newton-meters
M12: about 95 newton-meters M16: about 230 newton-meters These are starting points. Your actual values will vary based on material grade, thread condition, and lubrication. Always verify with your specific application requirements.
When to Use Which Method
For general machinery and structural work, standard torque calculation with a conservative friction factor is sufficient. Budget 10 to 15 percent extra torque to account for uncertainty, or use the turn-of-nut method for better consistency. For critical applications like aerospace, automotive engine components, or pressure systems, invest in ultrasonic measurement or calibrated load cells. The cost of a fastener failure in these applications far exceeds the cost of proper measurement equipment. For field service work where you do not have fancy equipment, the mark-and-wait method plus periodic verification is a practical compromise. It catches most problems without requiring significant additional tools or training.
The key takeaway is that torque is a means to an end, not the end itself. The goal is consistent clamping force. If your method does not achieve that consistently, you need a different approach. Start simple, verify when it matters, and do not pretend that a torque wrench specification guarantees anything without understanding the variables involved.