Getting Your Keycaps Made Without Losing Your Mind
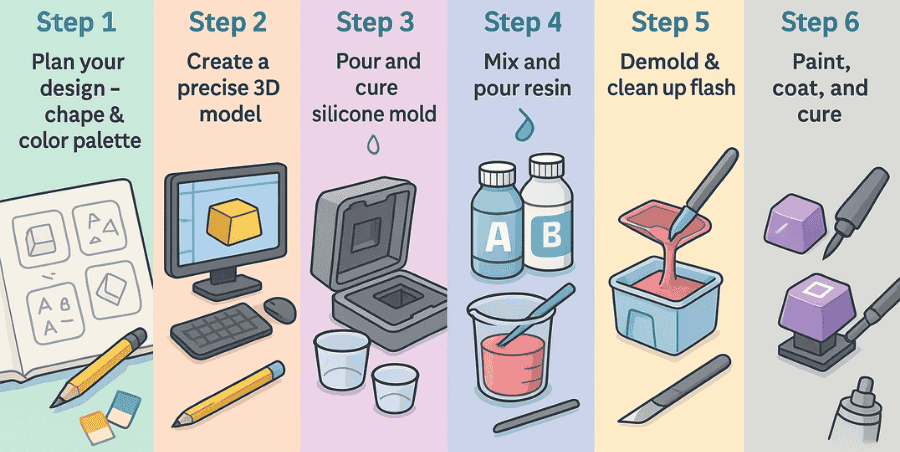
Custom keycap manufacturing is a long, grinding process that usually takes people three to six weeks from start to finish. I have been doing this for years, and the timeline never really changes no matter how much you optimize. The biggest variable is whether you use injection molding or 3D printing, because those two paths require completely different skill sets and budget levels. Most people come in thinking they can just design something in Fusion 360 and have a factory pump out ten thousand sets overnight. That does not happen. You start with a 3D model. This sounds obvious, but the quality of your base mesh determines everything downstream. If your profiles are off by even a fraction of a millimeter, the keycaps will wobble on the switches, and nobody wants that. I recommend using a parametric CAD program where you can lock your mount profiles to standard Cherry MX dimensions. You do not want to reinvent the stem geometry because it will not fit on anything except a custom board you also built yourself. That is a rabbit hole most people do not need to fall into. Once your model is solid, you need to decide on material. PBTABS and PA12 Nylon are the two industry standards. ABS is cheaper and easier to mold but shines quickly and develops that greasy feel within months. PBT lasts forever and has a nice texture, but it requires higher injection temperatures and can be trickier to produce cleanly. If you are prototyping at home, PETG is an acceptable middle ground for a few dozen copies before it starts warping on larger keys.
After the file is finalized, you send it to a manufacturer or run it through your own slicer if you are doing desktop production. For injection molding, someone needs to create a steel mold, which runs anywhere from two thousand to eight thousand dollars depending on cavity count. A single-cavity mold for a ten-key set might cost you around three thousand. A full 180-key production mold with four cavities pushes past six thousand. The per-unit cost after that drops dramatically, which is why custom sets always seem expensive until you crunch the actual numbers.
Where Things Actually Go Wrong
I learned this the hard way with a batch of 180 keys I had molded in-house. I was using a dual-color setup with a translucent top layer over a dark PBT base for backlighting. The issue was that the thermal contraction rates between the two materials were mismatched, and every single Spacebar came out with a visible seam running down the center about two millimeters wide. The keys were structurally sound but they looked defective, and I had to scrap roughly forty percent of the run. I solved it by switching to a single material with a separate sticker insert method instead, which eliminated the seam entirely and actually improved the light diffusion across the key surface. That experience taught me to always produce a small proof-of-concept batch before committing to a full run. Even a single test key from the actual production material will reveal problems that your CAD simulation cannot catch. Warping, sink marks, and incomplete fills show up immediately when you hold the physical object.
Get the Full Details
Practical Workflow for Small Batches
If you are trying to produce fewer than fifty sets without spending thousands on a steel mold, resin printing is your fastest route. SLA printers like the Elegoo Saturn or Anycubic Photon series can produce individual keycaps in about forty five minutes each after supports are removed. That is not fast for volume, but for a prototype run it is acceptable. The downside is that resin keycaps are brittle and will crack under heavy typing forces over time. They also yellow with UV exposure, so if your desk gets direct sunlight you are looking at a discoloration problem within a year. FDM printing works too but the layer lines on the key surface are a real issue. You need to sand and fill every cap, which takes maybe twenty minutes per key if you are efficient. A full set takes me about four hours of post-processing labor. I stopped doing that for anything beyond ten keys because the time investment started making the per-unit cost higher than just paying a manufacturer directly.
The Injection Molding Route That Actually Works
When you go the industrial route, you should not shop based on price alone. Some factories in Shenzhen quote you low per-unit prices but use recycled PBT that is contaminated with previous batches of different colors. The result is keycaps that look slightly off in saturation and feel rough or chalky. I had this happen with my first order and ended up sending everything back. The replacement batch from a different supplier cost ten percent more but had consistent coloring and a proper matte finish that did not flake when you ran your thumb across it. Minimum order quantities are another trap. Most credible manufacturers require a minimum of three hundred to five hundred pieces per color. For a standard 104-key layout with two colors that is twelve hundred keys minimum. If you do not have the capital to cover that, your options narrow significantly to either 3D printing or working with a group buy coordinator who can pool orders from other enthusiasts. Group buys are a legitimate path, but they carry their own risk of delays. The keyboard space runs on group buy timelines because manufacturers often deliver late, and there is nothing you can do about it once you have paid upfront. Surface finishing matters more than people realize. A standard matte finish feels good out of the box but picks up oils and shows shine patterns within weeks. A texture like skin coating or bead-blasted PBT hides fingerprints much better. I switched my personal builds to bead-blasted and have not looked back. The texture is consistent, the keycaps feel dry under your fingers, and they maintain their appearance indefinitely.
If you are serious about producing custom keycaps, the manual route through a machine shop or small-scale injection molder is viable but it demands patience and realistic expectations around both timeline and cost. Budget six weeks minimum for a clean first production run. Factor in a ten to fifteen percent rejection rate for your first batch regardless of how careful you are. And always, always order a single sample before committing to volume. The money you save by catching a mistake early pays for itself many times over.