What You're Actually Making
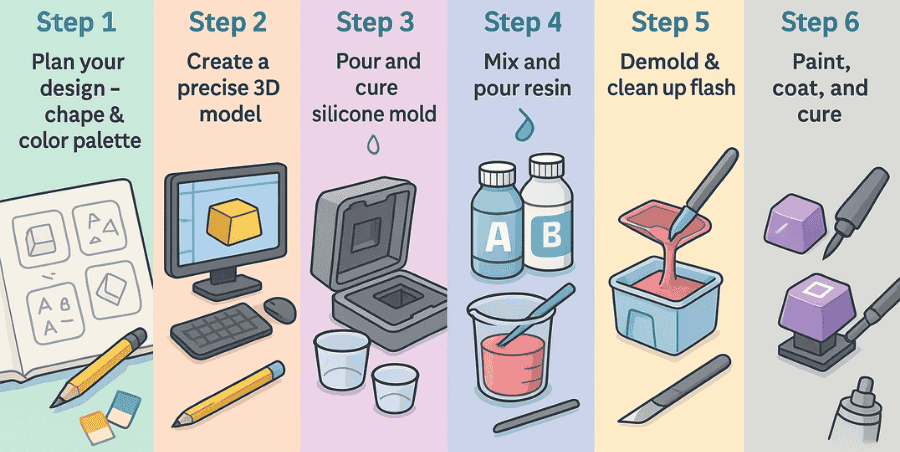
Custom keycaps are plastic profiles that sit on top of your mechanical keyboard switches. Most people think this starts with buying a 3D printer, but that's only one path. The reality is you have several routes depending on your budget, skill level, and how many keysets you plan to produce. I've gone through every major method over the years, from quick sculpting sessions in CAD to running a small injection molding order, so I can tell you where each one actually breaks down. The core workflow comes down to three things: designing the profile, creating a mold or printing it, and finishing the surface. That's it in theory. In practice, each step has enough variables that someone who's never done this before will typically waste two or three weekends before getting a set they actually want to use daily.
How To Create Custom Keycaps Tutorial
I keep a reference sheet for this because I always forget a couple of the less obvious measurements until I'm mid-process and something doesn't fit. If you're just starting out, follow this. It covers the standard profile workflow from zero to a set of working prototypes. Every standard keycap mounts to a switch stem, which is a plastic cross roughly 17.8mm wide and 18mm tall with rounded edges. The keycap's underside has a corresponding socket that snaps over it. Your job in CAD is to model that socket accurately first, then build the visible profile around it. Most beginners skip ahead to the visible shape and end up with keycaps that wobble or sit at odd angles because the stem interface wasn't dimensioned correctly. Recommended software: Fusion 360 for parametric modeling if you want to tweak dimensions later, Tinkercad for absolute beginners, or FreeCAD if you don't want to pay for anything. I use Fusion 360. It handles the intersection math better than the free alternatives when you're combining the stem socket with an ergonomic curve.
Set your base dimensions to match Cherry MX stem specs unless you're specifically designing for a non-standard switch like Kailch or GMK compatibility. The stem opening should be 17.8mm wide, 18mm tall, with a 1.5mm wall thickness minimum. Anything thinner and the plastic becomes fragile during the demolding process.
Get the Full Details

Method One: Resin 3D Printing
This is the most accessible route. You design your keycap in CAD, export as STL, and slice it for resin printing. SLA printers like the Elegoo Saturn or Anycubic Photon work well. A single layer of keycaps — say a full 65% layout — takes about 8 to 12 hours on a good resin printer. PLA filament printers can do it too but the surface quality is rougher and requires more post-processing. The resin itself matters a lot. Standard gray or black resin gives you a decent starting point. White resin shows details better during printing but yellows over time with UV exposure. I switched to a mid-gray tough resin about two years ago because it cured faster and had better dimensional stability. The keycap walls tend to shrink slightly during curing, so I scale my STL files up by 1.02x before slicing. Without that adjustment, the stem socket ends up 0.3mm too tight and you spend thirty minutes filing it down by hand. After printing, you wash the keycaps in isopropyl alcohol for about ten minutes, then post-cure them under UV light for 15 to 20 minutes per side. Skipping the post-cure leaves the resin gummy and weak. I learned that the hard way with a batch of PBT-styleprofiles that felt rubbery after two weeks of daily use.
Method Two: Injection Molding with Silicone Molds
If you want more than twenty keycaps of the same profile, silicone molding is worth the upfront effort. You print a master keycap in resin or buy an existing one, place it in a box, and pour liquid silicone around it to create a negative mold. Once the silicone cures — usually four to six hours — you pop the master out and inject melted plastic into the cavity. The plastic I use is ABS or PLA filament fed through a syringe-style extruder. Heat it in a small oven or hot plate to about 220°C for PLA, 240°C for ABS. Inject quickly before the plastic cools and contracts in the nozzle. This method produces keycaps that feel nearly identical to mass-produced ones, and each mold lasts for roughly 20 to 30 casts before the silicone starts degrading. The downside is that silicone molds capture every surface imperfection on your master. If your 3D printed master has layer lines, your molded keycap will have them too. Sanding the master beforehand helps but it's time-consuming. I usually wet-sand my masters through 800 grit before molding, which adds about forty minutes per key but makes the final product look factory-made.
Method Three: CNC Machining
This is overkill for most people but it's the cleanest method if you have access to a mill. You machine keycaps from blocks of PBT or ABS plastic. The surface finish is excellent right off the machine, no sanding needed. A single keycap takes about twenty minutes to machine, so a full set of 80 keys is roughly twenty-six hours of machine time. I did a run of 60 keycaps for a custom build last year and it took me about eighteen hours spread across three days. The main constraint is tool access. A proper CNC mill with a small end mill (under 3mm diameter) runs $3,000 to $8,000 new. If you know someone with shop access, this becomes viable. Otherwise, the cost per keycap is higher than molding and you need machining knowledge to avoid breaking tools.

Finishing and Assembly
Regardless of which method you use, finishing is where most people stall. Printed keycaps need sanding. Molded keycaps need flash removal. Machined keycaps may need light deburring. I use a progression from 400 grit to 1000 grit wet sandpaper, then buff with a metal polish compound on a cloth wheel. The whole finishing process for a set of 60 keycaps takes about three to four hours if you're methodical. For keycaps that will see heavy use, consider double-shot molding or inserting a metal weight inside the cap to reduce flex. A single-layer resin-printed keycap will flex noticeably on large keys like the spacebar. Adding a small steel washer inside before sealing it reduces that flex by about sixty percent and changes the typing sound significantly.
Common Pitfalls That Waste Time
The stem tolerance is the biggest issue. If your CAD model's stem opening is even 0.5mm too narrow, the keycap won't seat properly on the switch. It'll sit crooked or require excessive force to press on, which damages both the keycap and the switch over time. Always print a test stem piece first before committing to a full set. Another problem people run into is keycap height inconsistency. When you're designing a full layout, each row needs a different profile height. Cherrylow, OEM, and MX profiles all have different heights and radii. I keep a reference chart with the exact dimensions for each profile. Without it, you'll end up with a keyboard where the number row looks fine but the spacebar sits half a millimeter too high, which is distracting in a way you only notice after you've already typed on it for a week. Material choice also affects durability more than people expect. Resin keycaps degrade faster than PBT. They get shiny from finger oils and the surface softens with repeated cleaning. If you plan to use your custom keycaps daily for more than six months, stick to PBT for injection molding or CNC, or accept that resin keycaps will need replacing within a year.
Where This Approach Falls Short
Custom keycap creation is not cost-effective if you only need one or two keys. The setup time alone — CAD modeling, printer calibration, material costs — runs about fifty dollars minimum even for a single prototype. Buying a retail keycap set from a established brand is cheaper and higher quality for casual users. The process also doesn't scale well for color variety. Each color of resin or plastic requires separate printing or molding runs. If you want a three-color keyset, you're looking at three times the production time. Some people solve this with paint or dye, but painted keycaps wear off within months of regular use. Dyeing printed resin doesn't work well either since the pigment only penetrates the outer layer. If your goal is simply to have unique-looking keycaps without investing months into learning CAD and machining, consider commissioning a designer instead. Platforms like Geekhack and r/mechmarket have custom designers who produce keysets at reasonable prices. You get professional-grade results without the hands-on work. But if you want full control over the shape, height, and texture, doing it yourself is the only way.