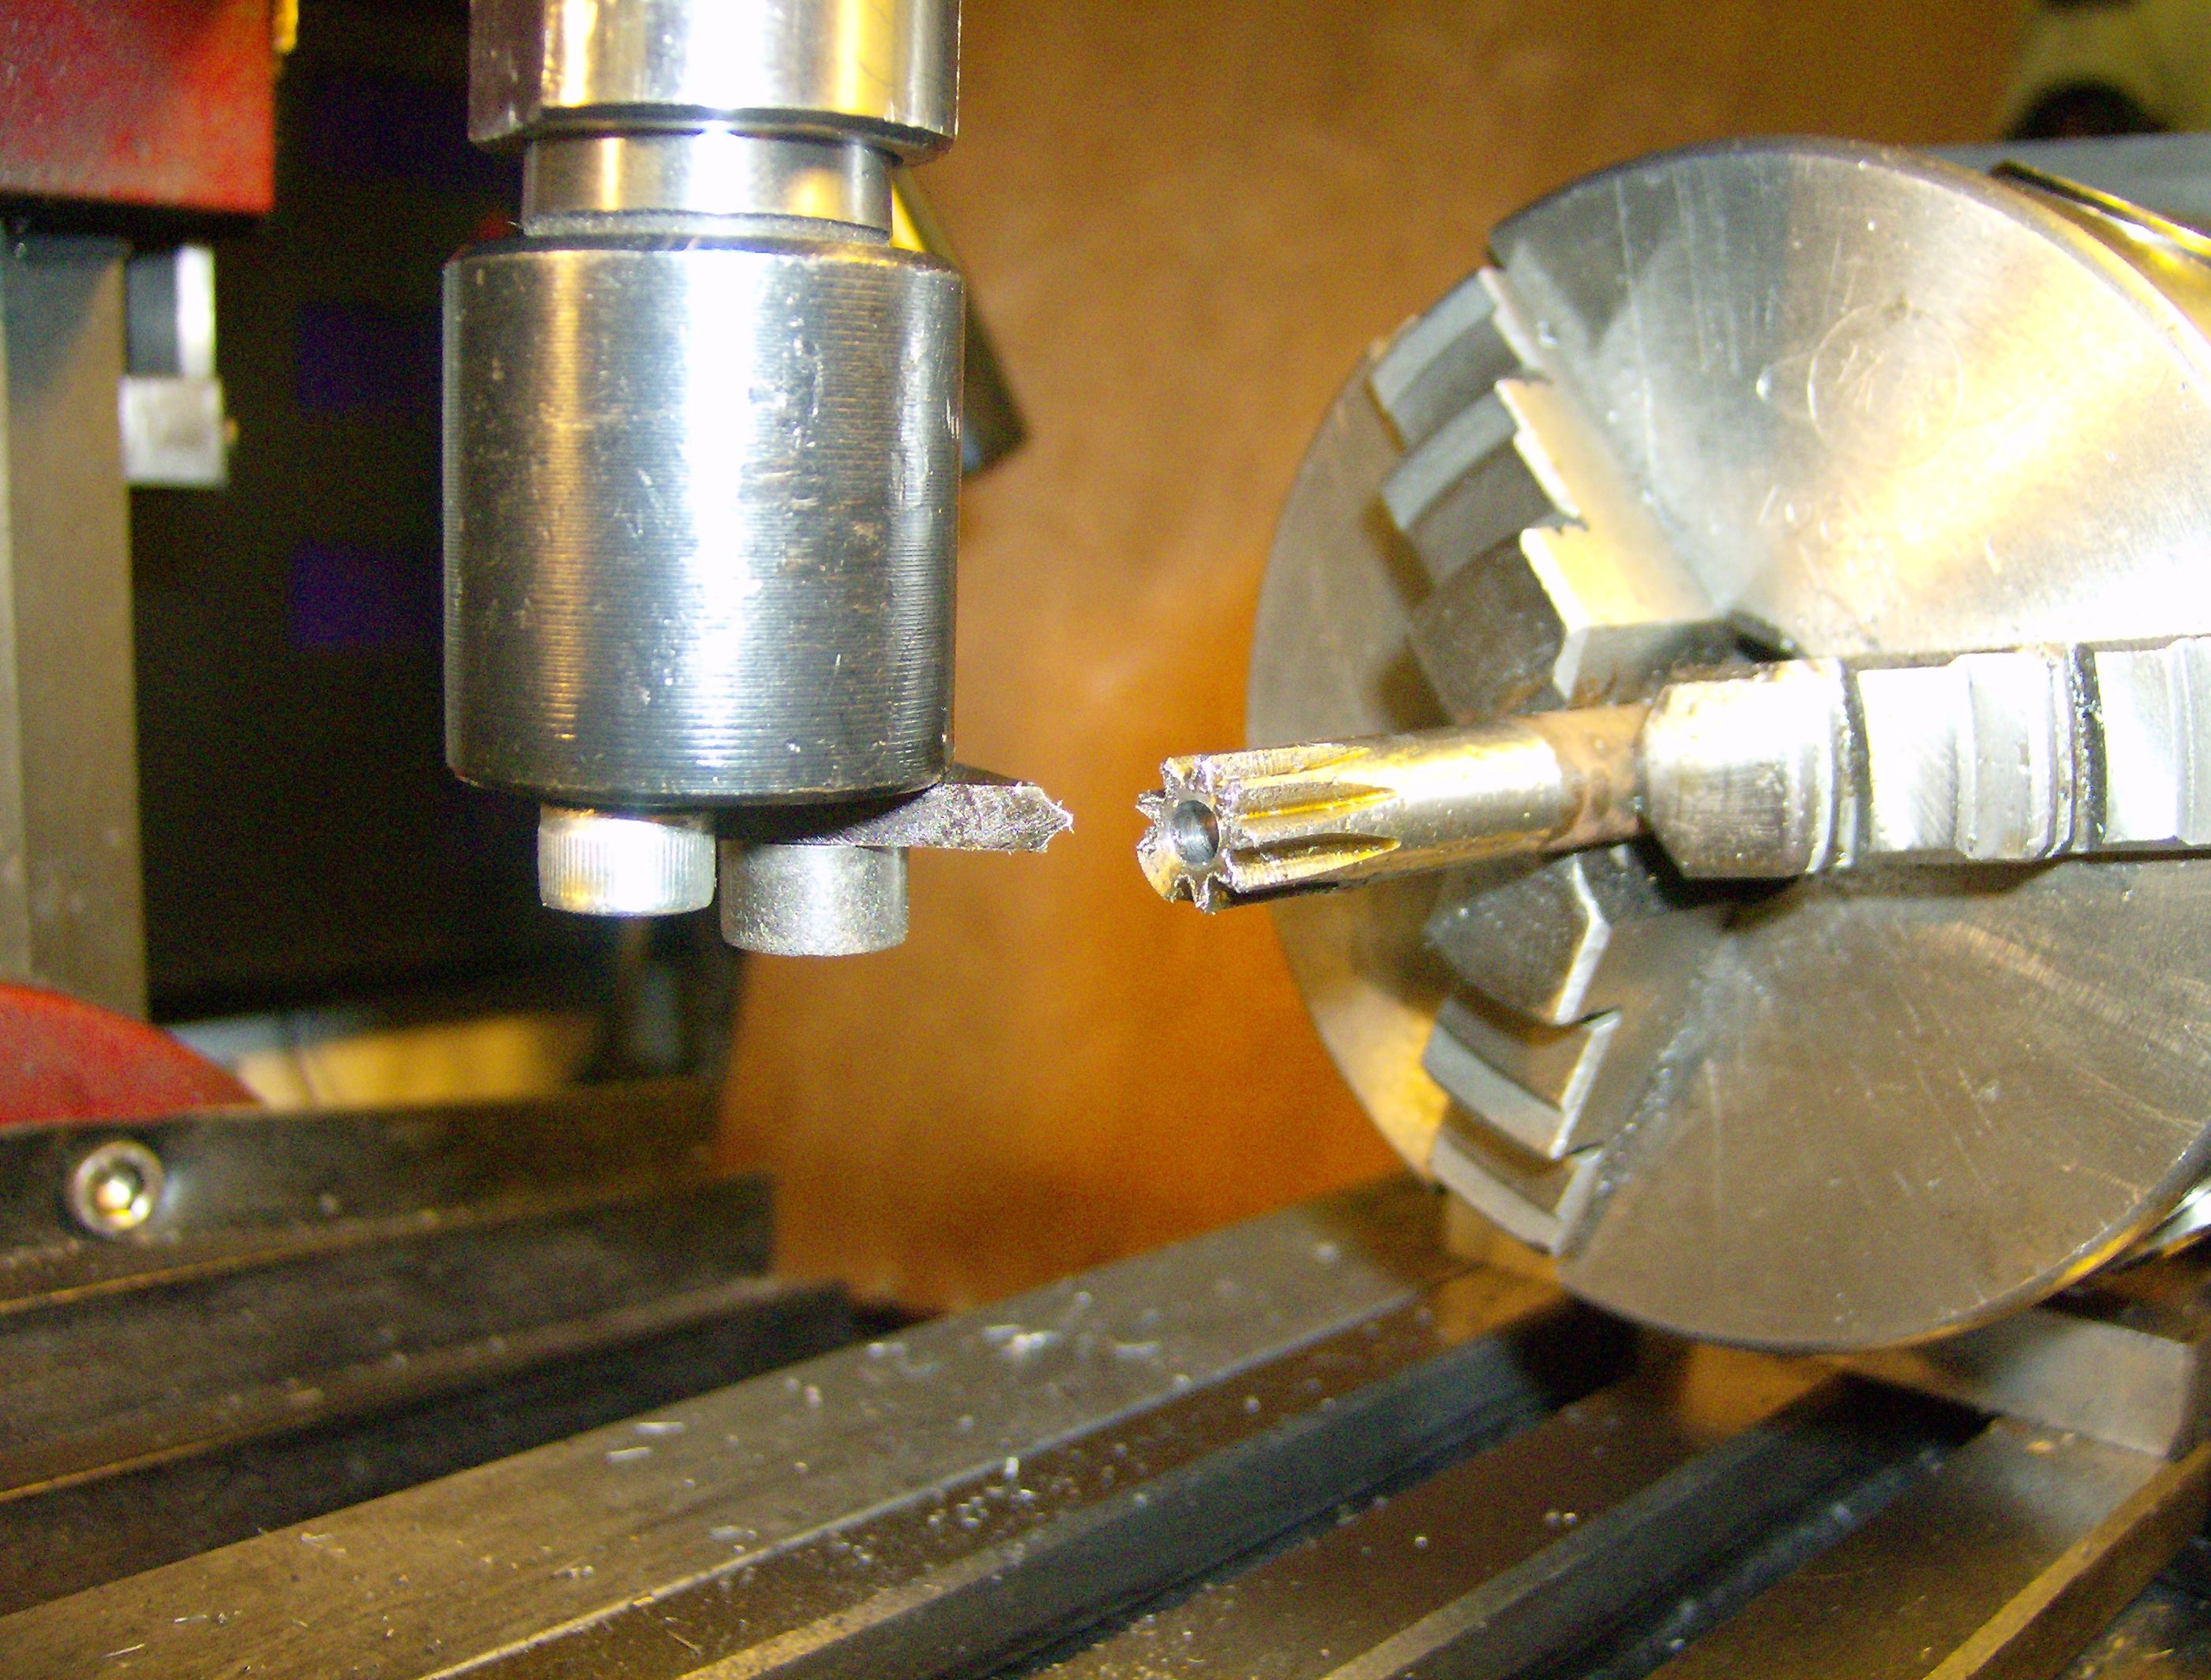
Setting Up the Change Gears
The first thing most people get wrong is the gear ratio. You're not guessing here. If you're cutting metric threads on an imperial lathe, or vice versa, you need to know the lead screw pitch. Write it down. Keep a notebook with your common ratios so you aren't recalculating at 11 PM when the shop is quiet and everyone else has gone home. I spent a good three hours once chasing a thread that wouldn't engage because I used the wrong compound gear ratio in my head. Turns out I was off by one tooth on the idler. The part was already cut to length and there was no way to salvage it. Now I write every calculation on a whiteboard before I touch the machine. Takes ten seconds and saves a lot of headaches.
How To Cut Threads On Lathe for Beginners
Let's walk through the actual process. First, determine your thread pitch. If you're cutting a 1/4-20 thread, that's 20 threads per inch, which means the lead is 0.05 inches per revolution. Your lathe's lead screw needs to turn exactly that much for each revolution of the workpiece. That's why the gear ratio matters so much. Install your change gears. Most lathes come with a gear set - 40, 48, 56, and 64 tooth gears are common. Mount them on the stud and leadscrew spindles according to your ratio calculation. Slide the back gears into place if you're cutting fine threads and need reduced speed. Tighten everything, but don't overtighten the gear mounting screws. Stripped threads on the spindle are not a fun problem to solve. Set the compound rest. Angle it to roughly half your thread form angle - about 29.5 degrees for a 60-degree ACME or V-thread. This lets you advance the tool into the cut with the compound slide instead of the cross slide, which gives you a cleaner finish and reduces the chance of the tool digging in too deep on each pass.
Using the Apron and Thread Dial
The thread dial on the apron is your friend, but only if you understand it. For even-numbered TPI threads, you can close the half-nuts at any time. For odd-numbered TPI, you need to open the dial at a specific mark each time - usually every second or fourth line depending on your dial. Check your lathe manual. Some dials have markings that indicate which quarter to engage for different thread types. Here's something nobody tells you: the thread dial can lie to you under certain conditions. If you're cutting a thread where the lead screw revolutions don't divide evenly into the workpiece revolutions, the half-nutes will re-engage at the wrong point on the previous pass. You'll hear a clunk, the tool will dive into the existing thread path, and you'll ruin the part. Test the engagement before you commit. Run the carriage back, disengage the half-nuts, move the tool clear, then try engaging at one of the dial marks. If the tool follows the existing thread groove smoothly on a test cut, you're good. If it bumps or skips, switch to the split-nut method instead. I ran into this on a batch of 13 TPI Acme threads. The dial said I could engage anywhere, but every third pass the tool would skip a ridge and chatter like hell. Stopped the machine, did the math, and realized the lead screw completed three full revolutions per workpiece revolution - an odd number. Had to engage at the same dial mark every single pass. Slowed the batch down considerably but saved a bunch of material from scrap.
Get the Full Details
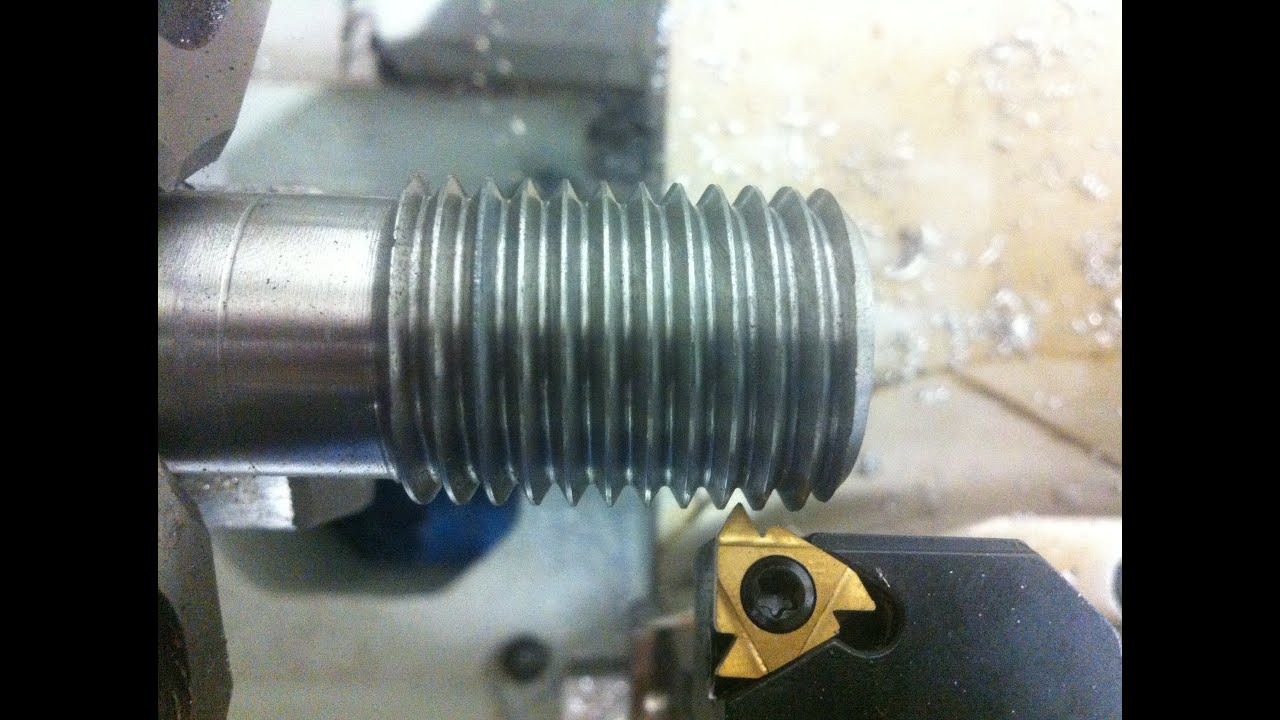
Cutting the Thread Itself
Start with a roughing pass at about 0.020 inches of depth. Go lighter on the finish passes - 0.005 inches for the final cut, maybe 0.003 for the last one. The exact amount depends on your tool geometry, the material, and how rigid your setup is. Soft aluminum lets you take more material. Hardened steel means you're lucky to get 0.003 per pass without burning up the insert. Use cutting fluid appropriate for the material. Oil for steel. Soap solution or light oil for aluminum. Don't run dry unless you're cutting a material that specifically doesn't want coolant - like some cast irons where thermal shock could crack the workpiece. Check your depth with a thread mic or a set of thread wires if you have them. A caliper won't cut it for accuracy. Thread wires give you the over-wire measurement which tells you exactly where your pitch diameter is. Without them you're guessing, and guessing is how you end up with a half-tone thread that won't fit its nut.
For external threads, start the tool slightly ahead of the workpiece and back off before reaching the end. Leave a small unthreaded section at the bottom of the thread runout. This prevents the tool from crashing into the shoulder and chipping the insert. Internal threads are worse because you can't see the bottom. Use a pilot hole that's close to but not exactly the minor diameter. A #7 drill for a 1/4-20 thread is about right - gives you clearance without taking too much out before you start threading.
Common Problems and Fixes
Rough threads usually mean one of three things: your tool isn't sharp, your compound angle is wrong, or you're feeding too aggressive for the material. Check the tool first. A worn insert on steel will tear the thread form instead of shearing it cleanly. Replace it. Then verify the compound is set to 29.5 degrees, not just a rough guess. And slow down your feed rate if you're hogging material on the first few passes. Pitch errors often come from backlash in the leadscrew or loose gibs. Take up the slack on the cross slide before each pass by always approaching from the same direction. If you're cutting a long thread and notice the pitch varies along the length, check that the tool post isn't vibrating. A loose tool post is probably the single most common cause of pitch variation on older lathes. Tighten it down and test again. Chatter during threading creates a wavy surface finish that ruins the thread. This is usually a rigidity problem. Shorten the tool overhang, use the largest tool bit your setup will accept, and make sure the workpiece is supported. Long thin shafts need a steady rest or a center support. I learned this the hard way on a 3/4 inch by 12 inch bar of cold-rolled steel. Chattered so bad I couldn't hear myself think over the noise. Bought a small steady rest from eBay for forty bucks and the problem disappeared instantly.

Advanced: Single-Point vs. Die Heads
Single-point threading gives you control but takes time. For production work, a die head or thread turning insert can speed things up significantly. The problem is that die heads can't handle non-standard pitches or special thread forms without swapping out the dies. If you're cutting custom threads or low-volume work, stick with single-point. You'll learn more about the machine and the process too. Thread turning inserts with the correct form radius exist for standard pitches. They're convenient but expensive and you'll go through several before you figure out the right feed rate and depth for your specific setup. A properly ground HSS tool costs about two dollars in material and fifteen minutes of your time. It cuts just as well once you get the geometry right. The learning curve is steeper but the long-term cost is lower. If you're cutting Acme threads, remember that the thread form is wider than a standard V-thread. Your tool needs a 29-degree included angle, not 60. Using a standard threading insert on Acme will give you a sloppy form that doesn't mesh properly with the nut. I've seen this mistake multiple times. People grab the first threading tool they find without checking the angle.


