The actual process
Building a double bass from scratch is one of those projects that eats weekends for months. The instrument is massive, the tonewood has to be dead flat, and every brace needs to be carved by hand while you're standing on a stool. I started this as something to fill a long winter. It turned into about fourteen months of work, including the time I spent waiting for wood to stabilize and the time I spent fixing mistakes. Let's start with the wood. You need spruce for the top and maple for the back, ribs, and neck. The spruce should be quarter-sawn, meaning the growth rings run perpendicular to the face of the board. That gives you the stiffness and the acoustic response you need. Flat-sawn spruce will work for a cheap project bass, but it won't carry the same projection. The maple back is typically bookmatched, which means you take one slab and slice it in half so the grain patterns mirror each other. Look for figuring, that swirling grain that makes the instrument look expensive, but don't get obsessed with it. A plain back plays just fine. What matters more is that the maple is well-seasoned, at least three to five years of air drying. Green wood will crack as it dries inside the instrument cavity and you won't be able to fix it once the bass is assembled. I got my spruce from a local mill in Colorado, specifically Engelmann spruce that had been dried for about six years. The grain spacing came in around twelve lines per inch, which is about average for bass tone wood. Not super tight, not loose. I'd recommend somewhere between ten and fourteen lines per inch as a workable range. Anything tighter than fifteen lines per inch and the wood gets stiff and bright. Anything below eight and it gets flabby and weak.
Carving the plates
This is the part that takes the most skill and the most time. The top plate and back plate both need to be arched. A flat plate sounds thin and dead. The arch gives the wood flexibility in the right directions while maintaining enough rigidity to handle the string tension, which on a double bass is roughly one hundred and fifty to two hundred pounds total across all four strings. The arching profile is typically a low dome, maybe half an inch to three quarters of an inch at the center, tapering down to nearly flat at the edges. You remove the wood in stages. Start with a block plane or a scraping plane to get the rough curve, then move to cabinet scrapers and finally 3-inch Bailey-style planes with curved blades for the final tuning. The goal is to hit specific frequencies at specific points on the plate. Most luthiers use a tap tone method where they hang the plate from strings and strike it gently, listening for a clear ring. The target frequencies vary depending on the wood and the size of the instrument, but a typical spruce top might ring around Cor D around the center block area and somewhere around For G near the edges. These numbers are starting points, not laws. If your wood is stiffer than average, the frequencies will read higher and that's fine. Bracing is what actually controls the plate vibration. The bass bar is the big one, a strip of seasoned maple that runs lengthwise under the treble side of the top plate, glued in place before the plates are assembled into the rim. It usually measures about three millimeters thick, twenty millimeters wide at its widest point, and runs from just below the treble foot of the bridge to near the lower bout. The bass bar transfers energy from the treble string contact point into the body. A poorly fitted bass bar makes the top sound choked and the instrument feels sluggish to play. I learned this the hard way on my first attempt. The bass bar I carved was slightly too thick in the middle section and the D string side of the top wouldn't vibrate freely. I had to remove the bar, re-carve it, and reglue it, which meant taking the entire instrument apart after it was already assembled and varnished. That added about three weeks of delay. The fix was making the bar thinner toward the center and ensuring the contact surface was perfectly flat against the underside of the top plate. A good test before gluing is to flex the top plate with your thumb where the bar will sit. It should give slightly and snap back. If it feels rigid, the bar is too thick or the plate is too thin in that area.
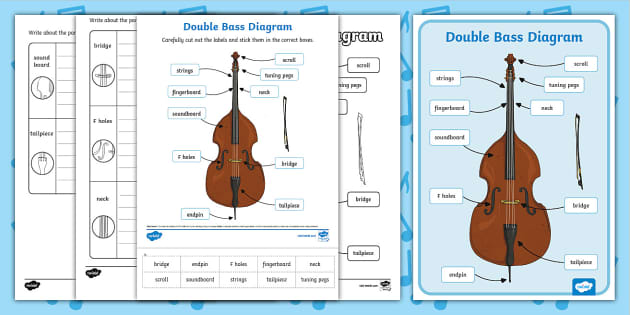
The f-holes come next. They're cut into the top plate after the arching and bracing are done. The standard shape is a long elegant slit with curled ends, but the exact profile matters less than the thickness of the wood around them. The bridges must remain. The area between the two f-holes at the center needs to be sturdy enough to support the bridge pressure, which can exceed forty pounds of downward force. I typically leave about five to six millimeters of wood there. The lower part of the f-holes, near the bass bar, should also have adequate material. If you cut the holes too aggressively, the top plate can crack along the grain line during assembly or later under string tension.
Get the Full Details

Bending the ribs
The ribs are the strips of maple that form the sides of the instrument. They're bent using heat and pressure, usually over a form or mold that matches the bass's outline. A rib bending iron, which is essentially a curved metal plate heated by an element, works well. You place the thin maple strip against the hot surface and slowly form it around the mold. The wood needs to be fairly thin, about four to five millimeters, and it should be slightly dampened to make it pliable. Dry maple cracks when you try to bend it. Soaked or steam-treated wood bends easier but can delaminate if overdone. The compromise is using a rib bending iron at around two hundred degrees Fahrenheit with the wood at normal moisture content, maybe ten to twelve percent. It takes patience and a few practice pieces before you get consistent results. There are internal corner blocks and end blocks that anchor the ribs. The bass has more blocks than a violin because the body is larger and the string tension is much higher. Typically you'll have two corner blocks at each end, plus a neck block and a tail block. The tail block is where the endpin attaches, and it needs to be substantial. I made mine from a solid piece of maple about three inches wide and two inches tall, glued into the bottom of the rib assembly. The endpin sits into a threaded insert screwed into this block. If this block isn't solid and well-glued, the whole back of the instrument can pull apart over time from the downward force of the strings and the weight of the instrument hanging from the pin. Here's a specific problem I ran into during rib assembly. One of the lower bass-side ribs didn't seat flush against the corner block because the block had a slight imperfection in its mating surface. The rib had a gap of maybe a millimeter at one end. I couldn't just force it because that would warp the rib. The workaround was to carve a small recess into the rib itself where the block imperfection was, using a sharp chisel and a scraper. I test-fitted repeatedly, removing tiny amounts of material until the rib sat flush all along the joint. This took about two hours of careful work. It's the kind of detail that doesn't show up in any guide but makes a real difference in the strength and sound transmission of the instrument. A gap between rib and block is a weak point that can propagate into a crack under stress.
Assembly
Once the ribs are bent and the blocks are in place, you glue the top and back plates to the rib assembly. The joints need to be clean and tight. I use hide glue for this because it's reversible, which matters if you ever need to open the instrument for repair. Hide glue sets faster than PVA glue, which gives you less time to adjust things, but it creates a bond that's acoustically superior and easier to break apart later. The mixing ratio for hide glue is roughly one part glue granules to ten parts water by volume, let it bloom for about twenty minutes, then heat it to around one hundred sixty degrees Fahrenheit. Keep it warm in a glue pot during assembly. The scroll and neck are carved from a single piece of maple, ideally with the grain running straight from the scroll down through the fingerboard area. A broken or wavy grain in the neck is a structural risk. The pegbox holds four tuning pegs, each under significant tension. A weak neck will twist over time. I carve the neck to about fifty millimeters wide at the nut for a standard four-string bass in E string tuning. The fingerboard is usually ebony, glued to the neck, and slightly cambered to match the hand position of a player who is stopping the strings with their fingertips. The bridge is separate, not carved from the same piece as the neck. It stands on the top plate between the f-holes and transfers string vibration into the body. A typical double bass bridge is about forty-five millimeters wide and seventy-five millimeters tall. It needs to be carved from well-seasoned maple, preferably radial or half-radial cut, and it should be shaped to allow freedom of vibration for the top plate underneath. Many beginners make bridges that are too thick and heavy, which deadens the tone. A good bridge weighs between eighty and one hundred grams for a bass. File the feet to match the curvature of the top plate exactly. Even a small gap between the bridge foot and the top will muffle the sound noticeably.
The finish
Varnish is another area where there's more opinion than there is science. Alcohol-based spirit varnish dries fast and is easy to repair but is less durable. Oil varnish is slower to dry, harder to repair, but more resilient. I used an oil varnish recipe based on linseed oil and amber varnish, applied in thin layers over a sanding sealer. About six to eight coats, with light sanding between each one. The varnish shouldn't be thick. A heavy coat acts like a skin that restricts the wood's ability to vibrate. The instrument will sound better with a thin, hard finish than with a thick soft one. This is one of those things that's hard to verify precisely, but experienced luthiers will tell you the same thing after enough iterations. The f-holes, the purfling, the inlay work, the endpin, the pegs, the strings, the mute, the case. All of those are details. The core of the instrument is the relationship between the top plate, the back plate, the bass bar, and the ribs. Get those right and the rest is mostly craftsmanship. Get them wrong and no amount of decoration will save the sound. One more thing that surprised me about the whole process. The interior of the bass is almost completely dark inside. You can't see what you're doing once the plates are closed in. This means any glue squeeze-out, any misaligned block, any air bubble in a joint is now trapped inside the instrument. I made a habit of checking every internal joint with a small mirror and a flashlight before closing up the next layer. It adds maybe ten minutes to each assembly step but prevents problems that would require disassembly later. On my second bass, I skipped this on one rib joint because I was tired and confident. Six months later, I noticed a slight rattle when playing at high volume. It turned out the rib had shifted slightly at the block joint and was vibrating against the wood. Fixing it required removing the back plate entirely. I wish I had caught it during construction instead of after the instrument was fully finished and played for half a year with a flaw in it.

If you're considering building one, start with the plans, get the wood right, and expect the project to take significantly longer than you think. The margins for error are wider than with a guitar but the consequences of getting things wrong are also larger because you can't easily hide acoustic defects in an instrument this size. There's no paint thick enough to cover a poorly voiced top plate.