Reading a micrometre is mostly about not screwing up the thimble
A micrometre is a precision measuring tool that uses a calibrated screw to measure distances down to thousandths of an inch or hundredths of a millimetre. The main components are the frame, the anvil, the spindle, the sleeve (or barrel), and the thimble. When you close the jaws, you should get a clean zero reading. If you don't, the tool is either worn or it was stored improperly. There is no fixing that except sending it for calibration or replacing it. I have a $120 Starrett that I bought in 2008. The thimble has a slight drag when it gets past 0.500 inches on the metric side. It reads consistently off by about 0.0002 inches in that range. I just subtract that from my readings and move on. These little offsets happen. Cheap micrometres drift more. Expensive ones drift less but still drift. That is just reality.
How To Read A Micrometre Step By Step
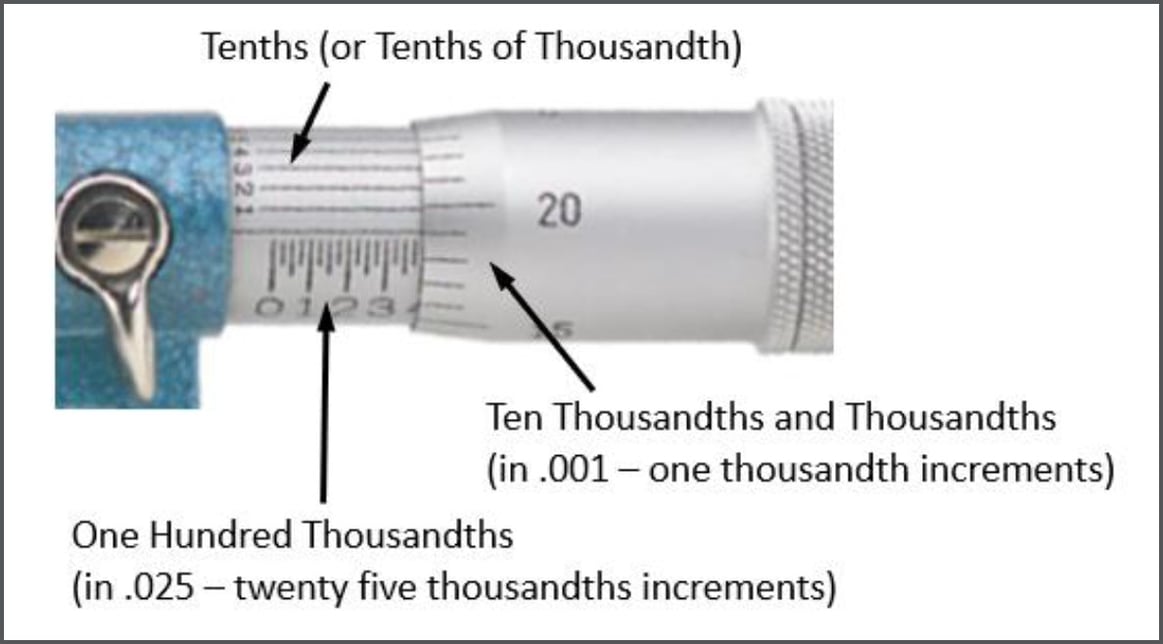
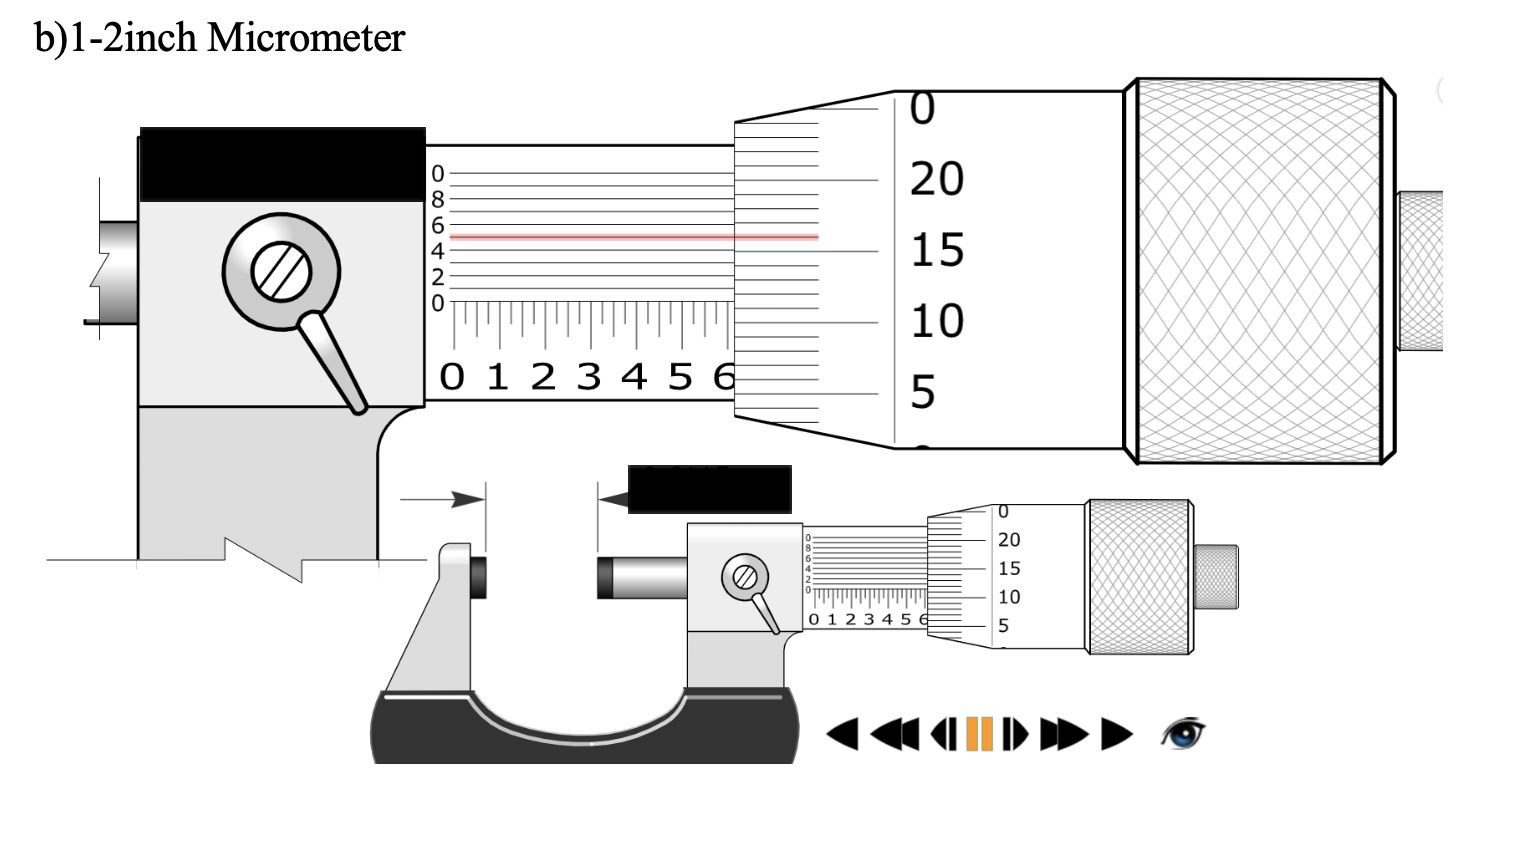
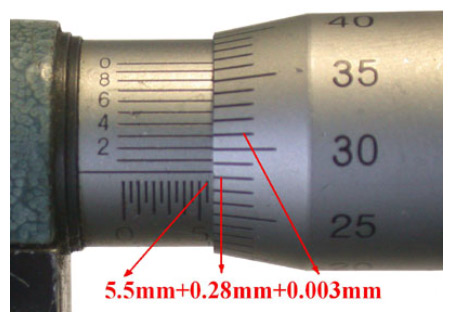
First, clean the measuring faces. I mean actually clean them. Wipe the anvil and spindle with a lint-free cloth. Even a tiny speck of metal shavings or oil will throw off your measurement by several thousandths. This is the most common mistake beginners make and the one that costs people the most in scrap parts. Open the micrometre wider than your target measurement. Place the object between the anvil and spindle. Close it using the ratchet stop or friction thimble. Do not overtighten. The ratchet should click two or three times. If you are using the regular thimble without a ratchet, apply consistent light pressure. Over-tightening will compress the measurement and give you a reading that is too small. Now look at the sleeve. The numbers on the sleeve represent whole units. On an imperial micrometre, each number is 0.100 inches. On a metric micrometre, each number is 1 millimetre. Below the numbers on the sleeve you will see smaller graduations. On an imperial micrometre each small line between the numbered lines is 0.025 inches. On a metric micrometre each small line below the numbers represents 0.5 millimetres.
Next look at the thimble. The thimble has 25 graduations around its edge. On an imperial micrometre each thimble graduation equals 0.001 inches. On a metric micrometre each thimble graduation equals 0.01 millimetres. The edge of the thimble should align with one of these lines to give you the final decimal place. Here is how the math works. On an imperial 0-1 inch micrometre if the sleeve shows the number 3 and two small lines past it, that is 0.350. If the thimble aligns at the 12th graduation, add 0.012. Your total reading is 0.362 inches. On a metric micrometre if the sleeve shows 8 and one small line past it, that is 8.5mm. If the thimble aligns at the 18th graduation, add 0.18mm. Your total is 8.68mm. There is a trick people miss. When the thimble edge falls between two lines, you need to estimate. If it looks closer to the lower line, round down. Closer to the upper line, round up. If it is right in the middle, take the average. This estimation is where most reading errors come from, especially under poor lighting.
Get the Full Details
I had a job once where a machinist was measuring a shaft that came out to 24.52mm. He thought it was 24.50 and rejected it. Turned out he was reading the thimble upside down because he was looking from the wrong angle. The parallax error on that particular micrometre was enough to throw off three hundredths of a millimetre. Always look straight at the scale. Tilt your head slightly and check. If the reading changes, you had parallax error.
The parts you need to actually understand
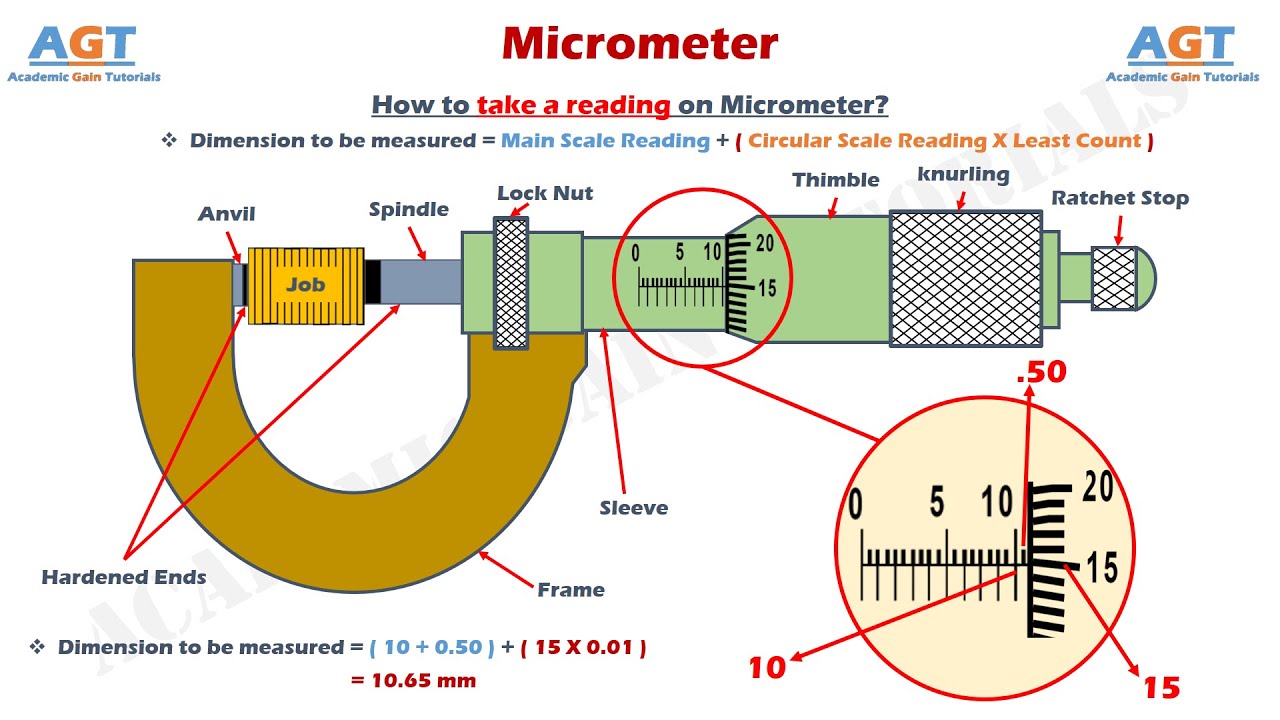
The frame is the C-shaped body that holds everything together. It is usually made of steel or sometimes cast iron in cheaper models. The frame should feel solid. If it flexes when you apply pressure, the micrometre is garbage and you should not trust it for anything above rough measurements. The anvil is the fixed measuring face. It is hardened and ground flat. The spindle is the moving face that advances when you turn the thimble. Both faces should be perfectly parallel when closed. You can check this by closing the micrometre gently and sighting across the faces. If light shows through evenly, they are parallel. If light shows through more on one side, the faces are and the micrometre needs service. The sleeve is the stationary barrel that has the main scale engraved on it. The thimble rotates around the sleeve and carries the minor scale. The ratchet stop is at the very end of the thimble. Its purpose is to apply a consistent measuring force every time. Without a ratchet, different operators will get different readings on the same part because everyone tightens differently. This is why ratchets exist and why you should use them.
Common mistakes and what to do about them
Reading the wrong side of the scale. On imperial micrometres the sleeve has two sets of graduations. The top set counts in 0.100 increments and the bottom set counts in 0.025 increments. If you read both sets as if they are the same thing, your number will be wildly wrong. Make sure you are only reading one set of lines from the sleeve and then adding the thimble reading to it. Not accounting for the pitch. Most micrometres have a 0.025 inch pitch on imperial models and a 0.5mm pitch on metric models. This means one full rotation of the thimble moves the spindle 0.025 or 0.5mm respectively. Understanding this is critical because it explains why the sleeve has those extra half-lines. Each half-line represents half a rotation of the thimble, which is exactly half the pitch. If you ignore the half-lines you will be off by 0.0125 inches or 0.25mm every time you cross a numbered line. Temperature is a real factor. Micrometres and the parts they measure should be at approximately the same temperature. If you take a micrometre from a cold office into a warm shop and immediately start measuring, the metal will expand differently. Give it 10 to 15 minutes to acclimate. I learned this the hard way when I was measuring aluminium parts with a steel micrometre and getting readings that varied by 0.001 inches depending on when I grabbed the tool.
Wear patterns matter more than you think. After years of use, the anvil and spindle faces develop wear. This wear is rarely uniform. It usually creates a low spot in the center of the face. When measuring soft materials like aluminium or copper, the spindle can settle into that low spot and give a reading that is too low. Hard materials like tool steel will bridge the wear spot and give a reading closer to actual size. If you frequently measure soft metals with an old micrometre, check the faces for wear with a dial indicator before trusting a reading.
When a micrometre is not the right tool
A micrometre typically measures between 0 and 1 inch or 0 and 25mm per tool. If you need to measure a 4 inch shaft, you need a 3-4 inch micrometre, not a 0-1. Using the wrong range micrometre will give you a loose fit and inaccurate results. Some shops use a single micrometre for multiple ranges by swapping anvils and spindle tips, but this introduces more potential for error. Micrometres also struggle with internal measurements. If you need to measure a bore diameter, use an inside micrometre or a caliper instead. External micrometres are for external dimensions only. Trying to force an external micrometre into an internal measurement will damage the tool and give you a useless reading. The biggest limitation is operator skill. Two people measuring the same part with the same micrometre can get different readings if they apply different torque. Even with a ratchet, hand position and grip strength vary. For production work where consistency matters more than absolute accuracy, a go/no-go gauge or a CMM will outperform any hand-held micrometre every time. The micrometre is fine for checking individual parts or verifying tool settings, but it is not a replacement for proper inspection infrastructure.
If you need to get better at reading one, the only way is practice. Measure known standards. Buy a set of gauge blocks if you can. Measure the same part five times in a row. If your readings vary by more than one thimble graduation, something is wrong with your technique or the tool. Check your cleaning process, your closing torque, and your reading angle. Fix the biggest issue first and retest.