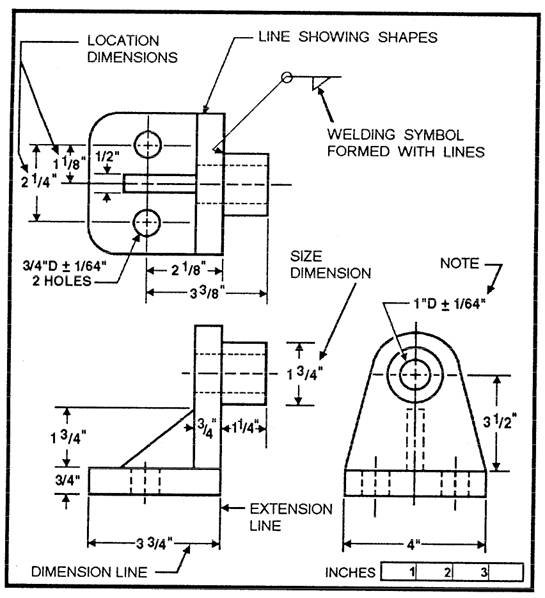
Reading dimensions off a drawing is something most people overcomplicate until they've made a mistake.
I spent about three years making cheap errors on shop floor prints before I stopped second-guessing myself every five seconds. The process is straightforward, but the details matter. Here's how I actually approach it now. Start with the title block. Every blueprint or CAD extraction needs you to check the scale, units, and revision date first. You'd be surprised how often I've caught someone measuring off a 1:50 scale print like it was full size, or assuming metric when the drawing said inches. Grab that info before you touch a single dimension line. Once the basics are locked in, scan for the overall envelope dimensions. These give you the bounding box of the part or assembly. From there, work inward toward the detailed features. It sounds minor, but reading from the outside in prevents you from getting lost in a forest of toleranced holes and fillets before you understand the general layout.
Dimension lines carry the actual measurements. They're the thin lines with arrows or tick marks that point from one feature to another. The number sitting on or above that line is the nominal size. That's your starting reference. Everything else branches off from it. Here's where things get tricky for people who don't do this daily: chain dimensions versus baseline dimensions. Chain dimensions stack measurements end-to-end, which means any error at the first dimension compounds as you move down the line. Baseline dimensions measure everything from a single reference edge, so each measurement stands on its own. On tight-tolerance assemblies, chain dimensions are a recipe for accumulated stack-up failure. I once had a supplier send me a bracket with four holes spaced using chain dimensions, and the total length came out 0.8 millimeters short because each individual spacing was at the low end of tolerance. Took me an hour to realize the drawing wasn't wrong—the manufacturing was just summing the wrong way.
Tolerances are where most people skip ahead and regret it later
A dimension without a tolerance is just a suggestion. Look for the ± notation next to a value, or check the general tolerances box usually printed in the title block area. ISO standard tolerance grades like h7, P9, or IT6 tell you exactly how much variation is allowed without writing it out next to every single dimension. If the drawing uses geometric dimensioning and tolerancing (GD&T), those symbols live in feature control frames—rectangular boxes divided into compartments that spell out form, orientation, and location requirements. A common pitfall is ignoring datums. Datums are the reference surfaces or axes that everything else measures from. If a dimension says a hole is 25mm from Datum A, you need to know what Datum A is before you can verify anything. I've seen machinists measure from the nearest flat surface instead of the specified datum, producing parts that are technically within individual dimension tolerances but completely non-functional when assembled. Angular dimensions follow the same logic but add a layer of confusion because some drawings use degrees-minutes-seconds while others use decimal degrees or slope ratios. Always confirm which system the drawing uses before cutting material. I learned this the hard way on a steel fabrication job where the architectural team specified a 5-degree rake and the structural shop interpreted it as a 1-in-5 slope, which is roughly 11.3 degrees. The fabricated members didn't fit the connection plates by about two centimeters along the top edge.
Get the Full Details
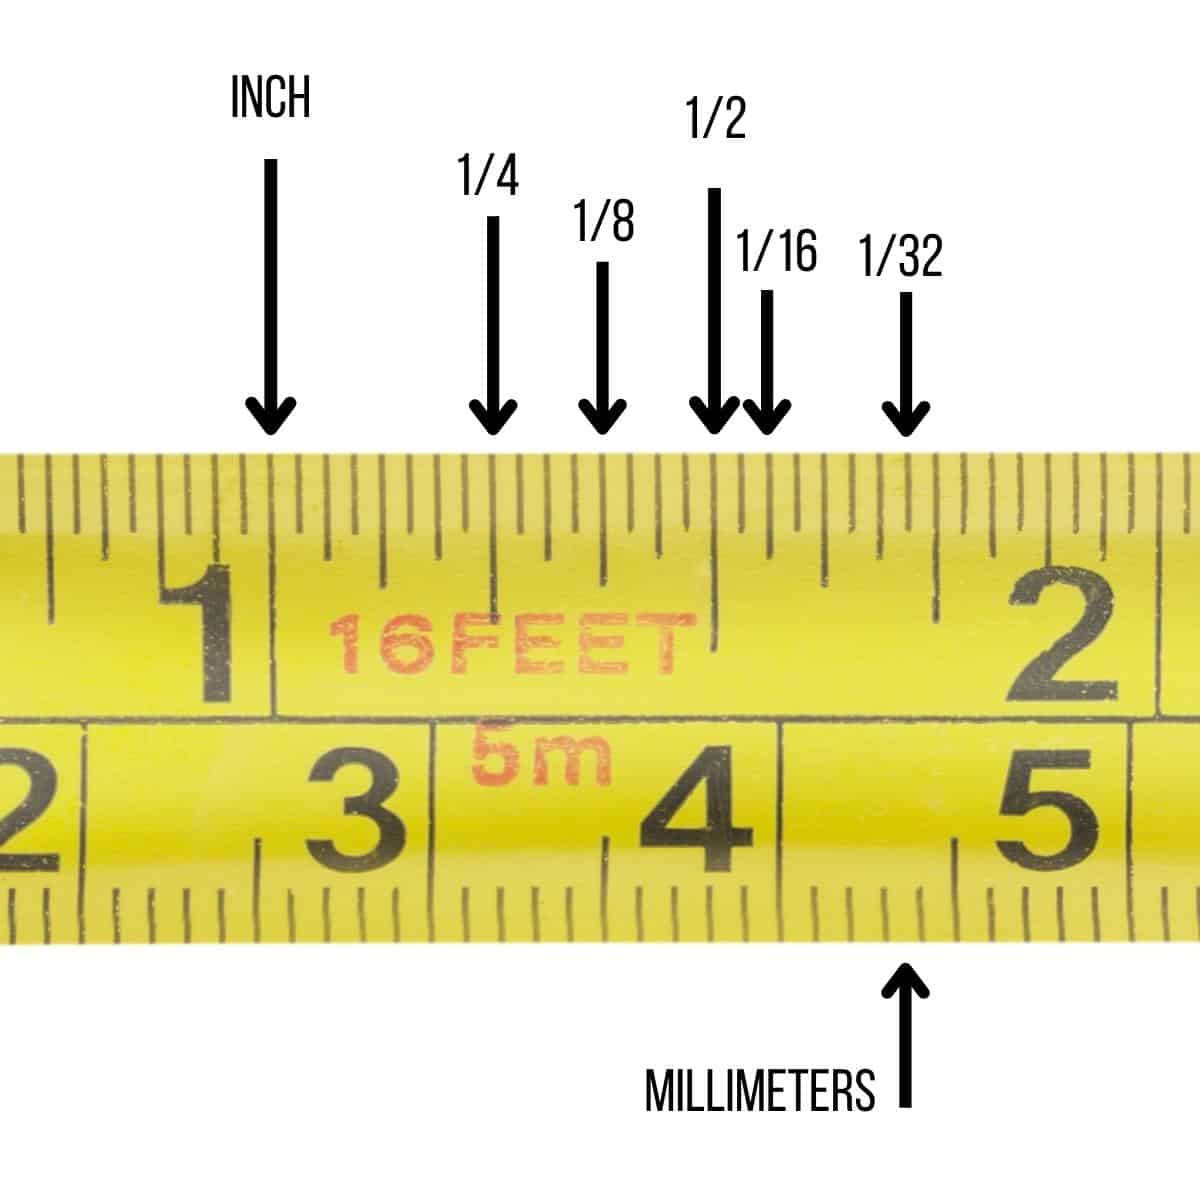
When the drawing doesn't have what you need
Missing dimensions happen. It's not drama, it's just reality. When you encounter a gap, don't guess. Draw a note on your markups or send a formal RFIs (Requests for Information) to the design team. Never fill in a missing value yourself and assume it's fine—that's how you get personally responsible for a $4,000 rework. Advanced cases involve unlimited free state tolerancing where feature controls aren't specified. In those situations, the default tolerance from the drawing's general tolerance table applies. Read that table carefully. Some shops use ASME Y14.5, others use ISO 2768, and the default tolerances between them differ significantly. ISO 2768-mK for medium precision, for example, allows ±0.1mm on dimensions between 30 and 120mm, while the equivalent ASME rule might specify ±0.050 inches for a similar range. Mixing up the standard is a real problem when drawings come from different regions. The practical workaround I use is simple: before any fabrication or inspection, print the drawing with the general tolerances clearly visible, circle the ones that affect my operations, and flag any dimensions that fall outside comfortable machining or measuring capability. This usually saves about 30 to 45 minutes of back-and-forth that would otherwise eat into a production day.
Tools that actually help
Physical calipers and micrometers are fine for basic checks, but if you're reading dimensions from PDFs or CAD exports regularly, CAD measurement tools save serious time. Most modern platforms—Fusion, SolidWorks, even free viewers like Autodesk Viewer—let you click two points and get the exact distance, angle, or diameter. Pair that with a good monitor at 1920x1080 minimum, and you'll catch dimension inconsistencies that get lost on a small laptop screen. For physical part inspection, a coordinate measuring machine or at least a digital caliper with data output will let you log measurements directly instead of handwriting values and risking transcription errors. I switched to logged measurements a couple years ago and cut my inspection documentation time roughly in half. The initial learning curve was about two days of awkward clicking, then it became routine.
What this approach doesn't cover well
Reading dimensions off 2D drawings is relatively straightforward. Reading them off complex 3D models or scanned point-cloud data is a different problem entirely. With point-cloud scans from laser scanners or photogrammetry, the dimensions aren't clean lines with clear numbers—they're noisy data clouds that require interpretation software to extract meaningful measurements. In my experience, the accuracy drops noticeably below 0.5mm resolution unless you're working with a high-end scanner and proper calibration targets. For most shop-floor applications, a good caliper and a clear drawing beat a handheld scanner every time. Also, dimension reading assumes the drawing is current. Revision control matters. If someone marked up a field change on paper and never updated the master file, everyone measuring from that outdated PDF is working from false information. Always confirm the revision number against the latest transmittal or PLM system check-out.