Getting Chips Away From Steel
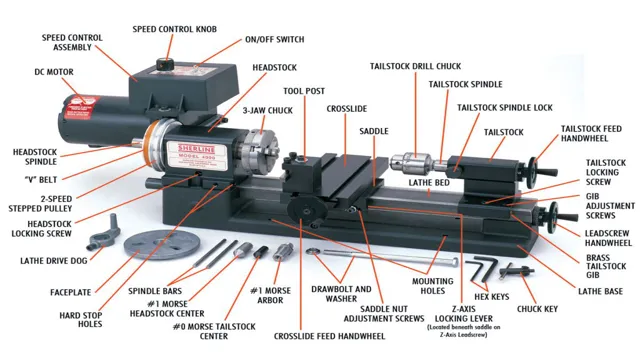
A metal lathe turns a workpiece on its axis. That's essentially what it does. You mount something between centers or in a chuck, spin it, and press a tool against it to remove material. Sounds simple enough until you're standing in front of a 1978 South Bend with a chip buildup problem and the spindle won't engage without you hitting it at exactly the right angle. Before you even think about cutting metal, you need to understand the three axes. The cross slide moves left and right across the bed. The compound rest angles at whatever you set it to. The carriage travels along the length of the bed. When you're doing a facing cut, you're moving the cross slide. When you're turning diameter, you're moving the carriage. Get those directions wrong and you'll be scratching the bed ways instead of cutting anything useful. The first real decision is how you're mounting the work. Chuck jaws are fine for round stock under three inches, but once you go larger or irregular, you need faceplates or four-jaw chucks. I learned that the hard way on a piece of aluminum plate about a foot wide. Centrifugal force does not care about your good intentions.
Tool height matters more than people admit. If your cutting tool isn't running dead center to the spindle axis, you're either pushing the tool into the work or pulling it away. At center height, the cutting edge properly engages the material. Below center and you get digging. Above center and the tool skims rather than cuts. Set it by bringing the point up to touch the tip of a live center in the tailstock. That's it. No laser levels. No fancy gauges.
Speeds, Feeds, and Not Ruining Your Tooling
Surface speed is what you're really working with here, not just RPM. Cutting carbon steel at 120 surface feet per minute with a high-speed steel tool on a half-inch rod looks wildly different from doing the same calculation on two-inch bar. The RPM numbers jump around enough that beginners punch them in without thinking and end up burning through inserts or glazing the workpiece. Use a speeds and feeds chart, then adjust based on what you actually hear and see. If the chips look like ribbons and are warm to the touch, you're probably running too slow. If they're powder or blue, you're going too fast. Here's something that always trips people up: roughing and finishing often want completely different feed rates, not just different depths of cut. A heavy roughing pass at 0.015 inches per revolution on a 12-inch swing lathe eating 4140 steel will chew through material like nothing. But try that same feed on a finishing pass and you'll be hunting for the part with a micrometer because it's sitting somewhere past your tolerance. Finish cuts usually live between 0.003 and 0.008 inches per revolution depending on your setup rigidity. I spent about forty-five minutes last November fighting a chatter problem on a long, slender shaft. The material was 416 stainless, four inches long and three-quarters inch in diameter. Standard approach would be a slow feed, light cut, maybe a different tool angle. Nothing helped until I loosened the tool post clamp just enough that the tool could self-oscillate at a slightly different frequency, then tightened it back down. That's not something you find in the manual. It worked because the chatter was resonating at the tool-post interface, and the slight compliance broke the feedback loop. Took another run at a proper finish cut after that and the surface came out at around 125 microinches.
Get the Full Details
Common Mistakes That Cost Money
People forget about thermal expansion. Machine tools and workpieces both expand when they run. If you zero out your micrometer on a cold 4140 bar and then turn it for twenty minutes without stopping, that part is going to grow. On a tight tolerance job like a bearing seat, you might measure it .001 under and then wonder why it didn't fit the shaft you just measured it against. Let the part and the machine warm up for fifteen to twenty minutes before you start calling dimensions final. Keep a steady supply of coolant going if you can. Even a basic jet on a roughing pass makes a measurable difference in thermal drift. Another thing nobody warns you about is backlash. On any lathe with worn gibs, the cross slide and carriage will have play. If you're approaching a dimension and hit it from above, you're probably within tolerance. If you overshot and are coming back up to it, that backlash is eating into your accuracy. I compensate by always approaching from the same direction. Overshot? Back off a thousand and come back up slowly. It adds time to the process but it keeps you honest. Some people install backlash compensators. Those work until the threads wear out, which they do. Digging in too deep is the classic rookie move. A half-inch depth of cut on steel with a worn tool isn't going to happen in one pass. The tool will deflect, the cut will grab, and you'll either break the insert or take a chunk out of the part. Start with around a tenth of an inch on roughing passes for most steels. Move up from there as the tool and setup allow. The lathe isn't going anywhere. Your first instinct to remove material fast will cost you more time than a methodical approach ever would.
What This Machine Can't Do For You
Lathes are fantastic for cylindrical work. They're not going to make flat faces with perpendicularity better than a thousandth or so unless you've invested in a proper faceplate setup and know how to indicate it. They're not cutting centers or threading multi-start leadscrews without some serious setup. And don't expect to run a lathe at high RPM on a piece of material that's unbalanced. Even a quarter-inch of offset on a six-inch disc is going to shake the whole machine apart. Static balance before you spin anything above 500 RPM. If you need to machine complex geometries or multiple features in one setup, a mill or a CNC machine is probably the better call. A manual lathe rewards patience and linear thinking. It punishes shortcuts and assumptions. That's not a complaint. That's just how it works. You learn the machine, you respect the materials, and you pay attention to what's happening at the cutting edge instead of staring at the tachometer.