Setting Up and Running a Metal Lathe
A metal lathe is a machine tool that spins a workpiece around an axis of rotation while a cutting tool is brought into contact with it. That spinning is what lets you turn cylinders, face flats, cut threads, and make boring operations. The machine itself is straightforward. Getting the setup right is where people waste time. The first thing you do is clamp the workpiece. If you are using a three-jaw chuck, insert the key and tighten until the jaws bite into the bar evenly. Don't crank it like you are strapping a tire. Snug, then a little more. If the jaw faces are worn, you will get runout, and your part will be out of round by ten thousandths or worse before you know it. I once machined a batch of 4140 shafts and every single one was .003 oversize on diameter. Turned out the chuck jaws had been trued on a different machine years ago, and the calibration had drifted. I ran a test bar at low RPM, measured it, realized the concentricity was off, and re-trued the jaws in place. Took me twenty minutes. The parts were fine after that. I stopped trusting pre-set chucks after that incident.
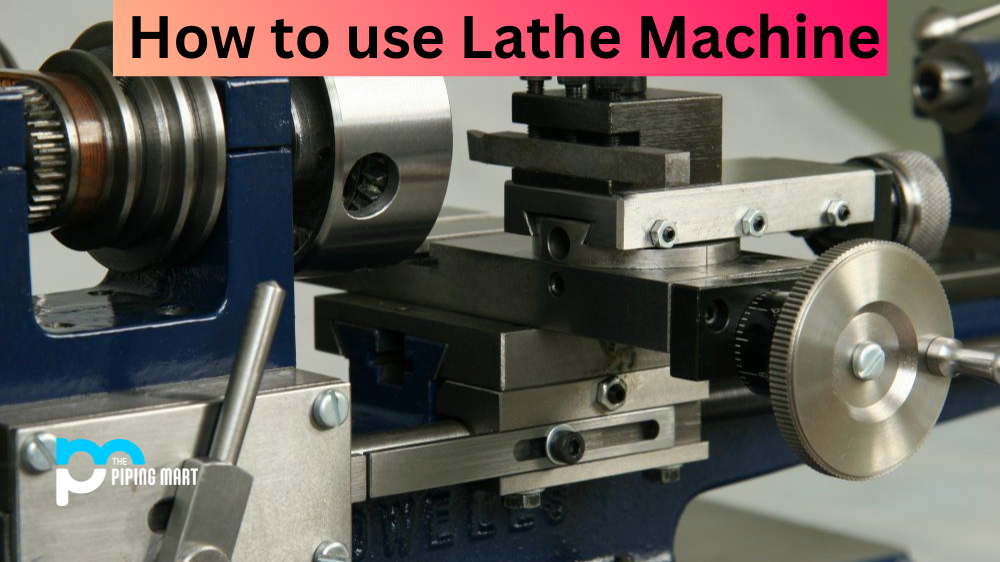
Once the stock is secured, position the tool post. Slide the compound rest to where you need it and lock it down. Set your cutting tool height so the tip aligns with the center of the workpiece. This matters more than beginners think. If the tool sits too low, it digs in and grabs. Too high and it rubs instead of cutting. You want the tip just at centerline, maybe a hair above for steel. Select your speeds and feeds. For mild steel with a HSS tool at .010 depth of cut, you are looking at roughly 120 to 150 surface feet per minute. That works out to about 600 RPM for a two-inch diameter bar. Cast iron runs slower, maybe 80 to 100 SFM. Carbide can handle more, but you are not necessarily running at maximum recommended speed just because you can. Chip formation and tool life matter. Start the lathe and take a light pass. You want to remove material, not fight it. For a roughing pass, .020 to .030 inches of depth is reasonable. Feed rate on the cross slide should be slow and steady. Let the tool do the work. If you hear a screaming sound, something is wrong. If you see long continuous chips rolling off the tool, you are in the right range. Broken, powdery chips mean too much speed or a dull tool.
When facing, you move the tool from the outside edge toward the center. Don't start at the center and push outward. The tool will jam and the workpiece can launch. I learned that one the hard way on a piece of free-machining aluminum with no shoulder to catch it. The bar came out of the chuck at about 800 RPM. It took a chunk out of the tool rest and made a mess that took an hour to clean up. For turning operations, you move along the length of the workpiece using the carriage. The cross slide handles diameter changes and facing. The compound rest is for taper cuts and fine adjustments. Most of the action happens with the carriage handwheel. Turn it smoothly, watch your measurement, and stop before you hit the dimension. Take a test cut, measure, adjust, and pass again. A micrometer costs about forty dollars. A scrapped part costs your time and frustration. Thread cutting is where people get tripped up. You need to set the correct thread pitch using the change gears or the leadscrew mechanism, depending on your lathe. Engage the half-nut at the right moment, usually when the indexing mark on theApron aligns with the dial. If your lathe has a split-nut, disengaging it mid-cut will ruin the thread. I once dropped a half-nut while finishing a metric thread on a vintage South Bend and had to start the pass over. Took me another thirty minutes to re-establish the entry point.
Get the Full Details
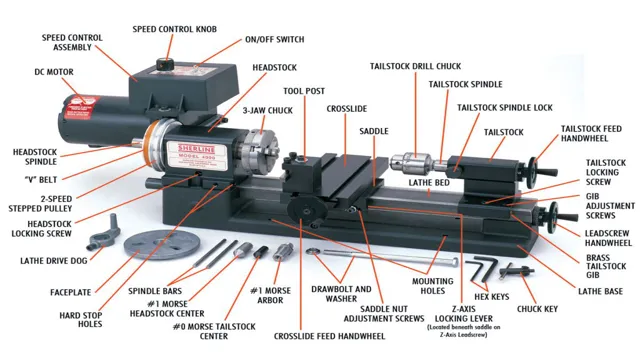
Drilling and boring require the tailstock. Center the drill bit or boring bar in the tailstock spindle, pull it tight, and advance it slowly into the rotating workpiece. For deeper holes, you need to retract frequently to clear chips. A cobalt bit in hardened stock without proper peck drilling will break before you get halfway through. Don't skip the peck cycle. There are limitations you need to accept. A standard metal lathe will not hold better than about .001 to .002 inches TIR on a typical setup unless you invest in precision collets, a steady rest, or a four-jaw independent chuck and spend time indicator-setting each piece. If you need sub-thousandth consistency across multiple parts, you are either going to spend more time setting up or you should look at a CNC lathe. A manual lathe is capable, but it demands patience and skill that most people underestimate coming in. Coolant is optional but recommended for anything beyond soft aluminum or brass. For steel, a straight oil or synthetic soluble coolant will extend tool life significantly and improve surface finish. I run wet on most steel work and dry on cast iron and aluminum. Cast iron dust is a lung irritant and coolant turns it into a grinding paste that ruins ways. Aluminum gums up tools with heat and adhesion, so a mist or just compressed air works fine for most operations.
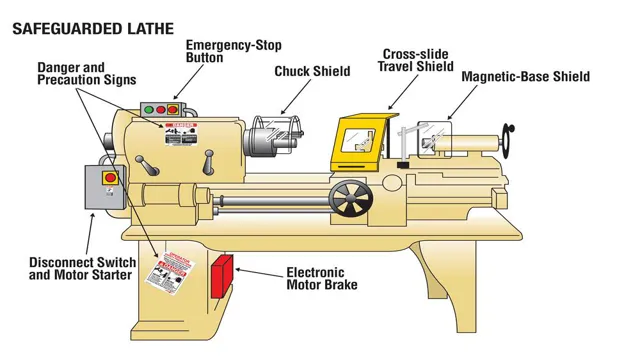
Safety gear is non-negotiable. Safety glasses with side shields at minimum. No gloves near a rotating chuck. No loose clothing, no jewelry, hair tied back. The lathe will grab anything it touches. I have seen people get away with cuts and bruises from flying chips and spinning stock, but the ones who ignored basic precautions usually ended up with injuries that required medical attention. It is not worth the risk. Maintenance is simple but easy to neglect. Wipe down the ways after every shift. Apply a light coat of way oil to the exposed surfaces. Check the chuck jaws for wear periodically. Lubricate the gearbox according to the manual. If your lathe has a grease zerk, give it a pump or two. A dry ways will drag and cause inconsistent feed, which ruins accuracy faster than anything else. The machine itself does not care about your schedule. It will wait. But the material you are cutting will tell you exactly how you are doing if you listen to it. Bad sound, poor chip formation, excessive vibration, or a tool that glazes over are all signals. Adjust speed, feed, or depth of cut and try again. You do not need expensive instrumentation to run a metal lathe competently. You need a micrometer, a reasonable understanding of what the machine is doing, and the willingness to slow down and verify your setup before you start removing material.