
Getting It Right From The Start
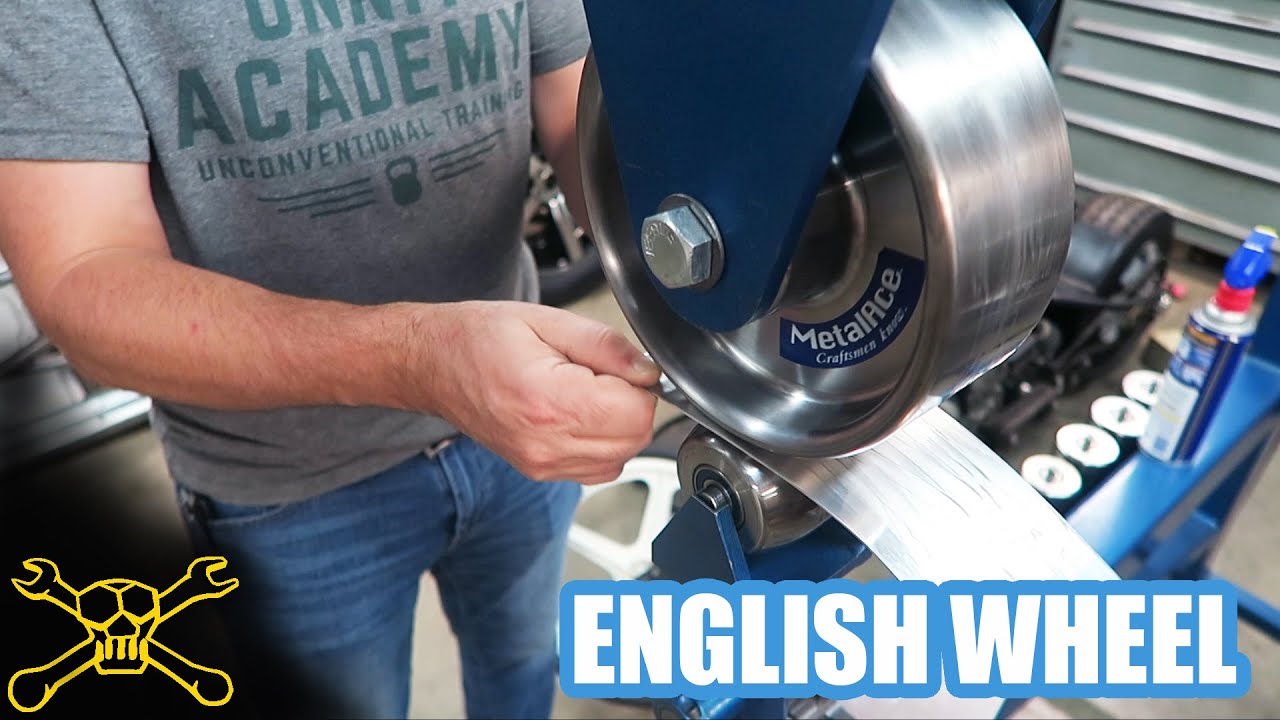
The English wheel is just two wheels rolling against each other with sheet metal sandwiched in between. You push, you roll, the metal stretches and curves. That is basically it. The thing that trips people up is assuming it is simple, because it is not. Getting smooth compound curves without ripple marks or uneven spots takes practice, and if you skip the fundamentals you will spend hours trying to fix bad work later. I once spent three days on a hood panel for a '67 truck. The client wanted a subtle belly swell. I started going too aggressive on one section, and the metal stretched faster than I could redistribute it. Ended up with a wave running across the entire panel that I could see when light hit it at the right angle. Sanded it all back down and started the affected area over. Took me another six hours. Lesson learned: go slow, make multiple light passes instead of one heavy one.
How To Use English Wheel Properly
Here is what actually matters. First, your setup. You want a solid base, either a floor stand or a heavy bench. Wobble kills accuracy. The anvil and formed wheel should be matched for your material thickness. Thinner gauges need smaller diameter wheels. If you are working with 18-gauge steel, those big formed wheels designed for thicker stock will just make ripples you cannot get out. Your technique is everything. You are not hammering. You are rolling. The motion is a continuous feeding pattern where you advance the sheet in overlapping passes. Start from the center of the area you want to curve and work outward. Cross-hatch pattern helps you build compound curves evenly. Roll diagonal, then perpendicular, then diagonal again. This distributes the stretch rather than concentrating it in one direction. Pressure matters more than speed. Light, consistent pressure gives you control. Squeeze too hard and you thin the metal unpredictably. I usually work at about fifty to sixty percent of what feels like maximum pressure. You can always add more passes. You cannot add metal back once you have stretched it too far.
Material Considerations
Aluminum behaves differently than steel. It work-hardens slower but it also springs back more. When you take aluminum off the wheel it will continue to relax for maybe fifteen to thirty minutes after you stop. If you are checking fitment right away, it might look tight and then develop a gap later. Steel is more predictable but it requires more force. Cold-rolled steel is your best bet for panels. Hot-rolled will have scale and inconsistencies that transfer into your finish. The thickness range is roughly 24-gauge down to about 16-gauge for most standard English wheels. Going thinner than 24 gets tricky because the material bridges between the wheels instead of rolling properly. Going thicker than 16 requires a much heavier-duty machine and still pushes the limits. For anything over that you are better off with a shrinker or a bead roller depending on what you are trying to do.
Get the Full Details
Common Mistakes That Cost Time
People tend to focus too much on the lower wheel and not enough on their foot placement and body position. Your feet should be shoulder-width apart, your body leaning slightly forward so your weight goes through your hands naturally. If you are standing straight up and just pushing with your arms, you will fatigue fast and your passes will be uneven. The power comes from your legs and core, not your wrists. Another issue is not annealing at the right time. With aluminum especially, you will notice the metal getting harder and harder to roll as you work it. The wheel starts to slip instead of bite. At that point you need to anneal. For aluminum you heat it to about 650 degrees Fahrenheit and let it air cool. For mild steel you heat it to a cherry red and quench in water. Do it before the metal becomes nearly impossible to work, not after. Checking your work is critical. Hold the panel up to a bright light source at an angle. Any high or low spots will show up as shadows. This is how I find imperfections before they become problems. Running your hand across the surface works too but light is more honest, especially for large panels where your hand cannot cover the whole area at once.
When The Wheel Is Not The Answer
There are situations where the English wheel is the wrong tool. If you need sharp creases or defined edges, you are looking at a shrinker stretcher or a English wheel with a hammer setup depending on the profile. If you are trying to make a perfect sphere or a complex organic shape that requires exact duplication, you would be better served by a slapper or a sanding drum on a lathe for certain applications. The English wheel excels at smooth, gradual curves on relatively flat panels. That is its sweet spot. Going beyond that usually means you are fighting the tool. I also recommend having a secondary finishing step ready. After the wheel work, most panels need some level of filing, sanding, or hammering on a sandbag to refine the surface. The English wheel leaves a texture that is workable but not final. Think of it as the shaping stage, not the finishing stage. Budget accordingly for the follow-up work because skipping it almost always shows in the final result. The investment in a decent English wheel is worth it if you plan to do this regularly. Cheap Chinese-made units from online marketplaces often have mismatched wheels, wobbly axes, and poor finish that transfer into your panels. A used American-made wheel from the seventies or eighties in good condition will outperform most new budget options. Look at brands like Eastwood, Classic Metal Works, or even older Harris units. Check that the wheels spin freely without play and that the surface finish on the wheels themselves is smooth. Rough wheels mean rough panels.


