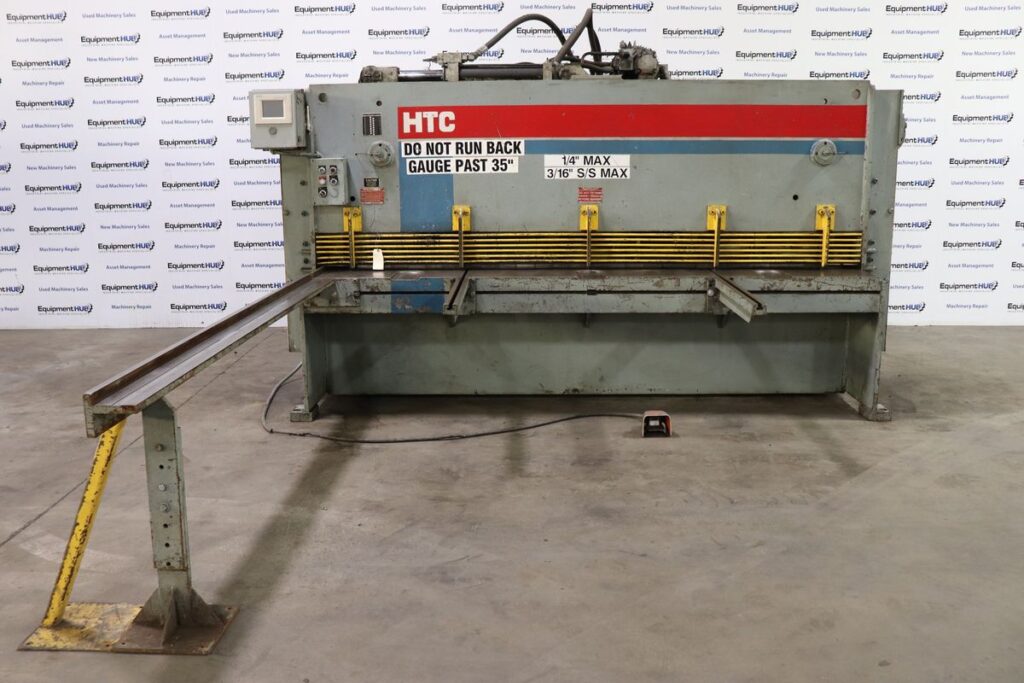
Getting Started With the Htc Hydraulic Shear Manual
I pulled out the Htc Hydraulic Shear Manual a few years back when a unit on my floor started losing pressure mid-cut. The problem wasn't the pump or the blades — it was the relief valve setting, and I spent two hours trying to find the torque spec before realizing it was on page 47 in the appendix. That manual is not well organized. It jumps between hydraulic schematics, maintenance checklists, and error codes without clear separation. But it is the only source that covers the H120 through the H320 series in one document. The shear uses a tandem pump setup — a high-flow stage for rapid stroke and a high-pressure stage for the cut itself. Understanding which circuit feeds which function saves you from replacing parts that are not broken. I have seen too many shops swap the main cylinder seal when the real issue was the pilot-operated check valve sticking open due to contaminated fluid. The manual covers this in section 3.2 but buries it under a generic troubleshooting table. Common setup sequence:
First, verify the hydraulic fluid level with the shear in the fully retracted position. Running it low causes cavitation noise that sounds like a bad pump bearing but actually damages the high-pressure stage within minutes. Second, cycle the shear through its full stroke range three times with no load to purge air from the cylinder. Third, set the relief valve to the manufacturer specification listed in the data plate — usually around 210 bar for the H160 model. Do not exceed this value to increase cutting force. The frame is rated for a specific maximum pressure, and exceeding it causes hairline cracks near the pivot pins that are nearly impossible to inspect without breaking the shear apart. The manual lists approximate cycle times for each model at various PSI settings. These are useful for planning production but do not account for fluid temperature effects. Cold fluid at 10°C increases cycle time by roughly 30% compared to the rated 40°C operating temperature. If your shop does not have conditioned hydraulics, factor that into your throughput calculations. A real problem I ran into:
The H200 model has a known issue where the rod seal on the main cylinder fails prematurely when cutting high-tensile rebar repeatedly. The manual mentions seal part numbers but does not call out this specific failure mode. I learned the hard way after three seal replacements in eight months. The workaround is switching to a polyurethane seal kit from a third-party supplier instead of the standard NBR seals the OEM lists. The kit costs about 40% more but lasts four to five times longer when cutting #5 rebar at maximum shear capacity. The manual does not reference aftermarket seal options, so you have to know to look elsewhere.
Get the Full Details

Maintenance Schedule and Critical Checks
The manufacturer recommends inspection every 250 operating hours, which translates to roughly two weeks on a busy job site. The checklist includes pin lubrication, hose condition inspection, and hydraulic fluid sampling. I treat the fluid sample as the most important item. A basic particle count tells you whether the filtration is holding or if there is internal wear starting in the pump or valve bank. Key maintenance intervals from the manual: Pin bushings require greasing every 50 hours. I grease them daily because I run mine hard and the pins wear faster than the manual suggests. The manual gives a generic grease specification but does not differentiate between EP and non-EP compounds. EP grease holds up better under high pressure at the cutting head. Using the wrong type accelerates wear on the moving contact surfaces.
The hydraulic filter should be replaced at 500 hours. The manual shows the filter location on a diagram but the actual removal requires dropping the return line pressure first. If you remove the filter housing under pressure, hot fluid sprays out and can cause burns. The procedure is in section 5.1 but is written in a way that assumes familiarity with this shear model. A new operator might miss the pressure bleed step. Hydraulic fluid recommendations: The manual specifies ISO VG 46 hydraulic oil for temperatures between -10°C and 40°C. For colder environments, ISO VG 32 is acceptable but the shear cycles slower and the pump may cavitate if the reservoir is not heated before startup. For hotter environments, ISO VG 68 works but increases internal leakage across valve clearances, which reduces cutting speed without increasing force. The manual does not discuss viscosity-temperature tradeoffs in detail. You figure that out through experience.
One thing the manual gets wrong is the torque specification for the cylinder head bolts. The printed value in the appendix does not match the actual requirement for the H250 and H320 models. The correct spec is higher than listed. I discovered this when a cylinder head bolt backed out during normal operation and damaged the manifold surface. The fix involved resurfacing the manifold and replacing three bolts. Had I torqued the bolts correctly per the actual spec instead of the manual's printed value, the failure would not have happened.

Troubleshooting the Htc System
The manual includes an error code chart but some codes are model-specific and not all models share the same diagnostic display. The H120 uses analog gauges with no digital readout, so error interpretation relies on symptom observation rather than code reading. This makes the troubleshooting section less useful for older units. Symptom-based diagnosis approach: If the shear loses pressure during the cut stroke, the most likely causes are: worn piston seals in the main cylinder, a leaking pilot-operated check valve, or contamination fouling the relief valve. The manual lists these but puts them in alphabetical order rather than probability order. Start with the cheapest and most accessible component first. Check the fluid for contamination before tearing into the valve bank. A magnet passed through the suction strainer will pick up ferrous particles if the pump is wearing internally.
Slow cycling with normal cutting force usually points to pump wear in the high-flow stage. The high-pressure stage may still be fine. You can confirm this by measuring flow at the pump outlet with a flow meter while running the shear through a cycle. The manual provides baseline flow values for each model but does not explain how to measure them if you do not have the proper test ports installed. Some dealers add auxiliary test ports during overhauls. If your unit does not have them, you may need to install them or work without precise flow data. A common complaint from operators is that the shear drifts down when held at full extension. This is normal to a small degree due to internal valve leakage. The manual states acceptable drift is less than 5mm per minute. Anything beyond that indicates a problem. In my experience, drift is most often caused by a dirty pilot-operated check valve rather than worn cylinder seals. Cleaning the valve with fresh fluid and a soft brush resolves the issue 90% of the time without replacement parts. The manual suggests seal replacement first, which is unnecessary in most cases.
Parts Ordering and Compatibility Notes
The manual includes a parts breakdown with explosion diagrams. The part numbers are model-specific, and some components are shared across the H160 to H280 range while others are unique. Cross-referencing between models requires checking the serial number against the manual's revision date. Manufacturing changes occurred frequently, so the same model number from different production years may have incompatible parts. The hydraulic hose assembly part numbers in the manual are sometimes outdated. I have ordered replacement hoses based on the diagram only to find the fittings were updated mid-production without a manual revision. Always verify the actual fittings on the machine against the diagram before ordering. Taking a photo of the existing hose assembly and sending it to the supplier prevents most ordering mistakes. Seal kit compatibility:

The manual lists individual seal part numbers but selling them as complete kit packages is often more practical. Third-party seal suppliers map their kits to the Htc model numbers accurately. Using a quality aftermarket kit for routine maintenance reduces downtime compared to waiting on OEM parts, especially for less common models like the H320 where OEM lead time can exceed two weeks. The manual does not cover electrical system diagnostics for the powered units. If your shear has a motor-driven hydraulic power pack, you need a separate electrical schematic that is not included in this document. Contact the dealer for the electrical manual or check whether the power pack manufacturer provided one with the initial purchase. Running the shear without understanding the motor starter circuit and overload protection settings is a safety risk.
Operating Best Practices
The manual's operating instructions are thorough but assume the operator understands basic hydraulic system behavior. I recommend new operators spend time with a mechanic watching a full cycle before running the unit independently. The sound of normal operation is distinctive — a smooth pressurization ramp followed by a clean cut stroke. Abnormal sounds include knocking from the cylinder (rod misalignment or loose pins), whining from the pump (cavitation or low fluid), and chatter from the relief valve (contamination or incorrect setting). Cutting capacity varies with material grade. The manual lists maximum capacities for mild steel rebar. High-strength rebar reduces effective capacity significantly. Do not attempt to cut material rated above the shear's specification even if it appears to fit between the blades. The frame can flex under overload conditions, and permanent deformation is not covered under warranty. The manual recommends a break-in procedure for new or rebuilt shears: run through 50 full cycles at 50% of maximum pressure before normal operation. This seats the piston seals gradually and prevents premature seal failure from sharp initial pressurization. Skipping this step is a common mistake that leads to early seal leakage.
One operational detail the manual omits: the shear performs best when the material being cut is supported on both sides of the cutting point. Unsupported material vibrates and causes uneven blade wear and increased cutting force requirements. A simple workstand or even a second piece of scrap rebar placed against the cut piece on the far side of the shear makes a measurable difference in cut quality and blade life. The Htc Hydraulic Shear Manual serves its purpose as a reference but is not written for quick comprehension. It assumes the reader will cross-reference diagrams, tables, and procedural text during actual maintenance work. Keep a pen and highlighter handy when reading it on the job site. The information is there, but finding it requires patience and familiarity with the document structure, which comes only after repeated use.


