The Real Way Lean Actually Works on a Shop Floor
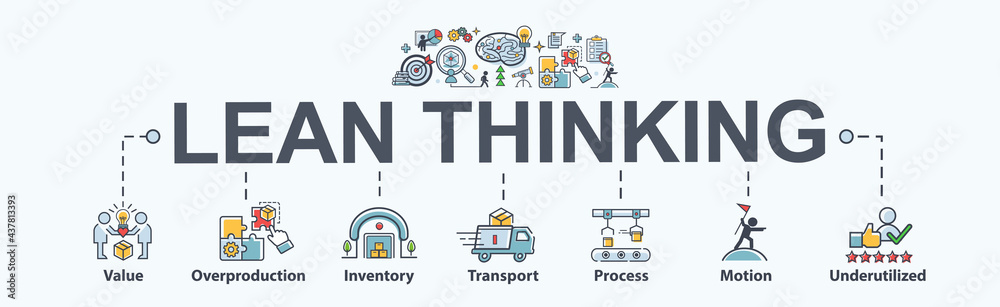
Lean isn't a philosophy. It's a set of very specific, very boring operational habits that most factories are terrible at implementing because they skip straight to the flashy stuff. I spent about eight years in manufacturing before moving into process consulting, and the ones that actually got results weren't the ones with the prettiest value stream maps. They were the ones where someone spent three weeks just standing at a workbench with a stopwatch watching people pick up the same box in slightly different ways. Lean thinking is fundamentally about identifying and eliminating the seven wastes: overproduction, waiting, transportation, overprocessing, inventory, motion, and defects. The problem is that every textbook explains this in the same sanitized way, and then real production environments are a mess of variables that no diagram covers. The first thing you need to understand is that Lean isn't about cutting costs. It's about making problems visible. When you reduce inventory buffers, things break faster. That's the whole point. You're trading comfort for information. The most common mistake I see is companies trying to implement Lean tools without first understanding their own process flow. They'll bring in a consultant, do a two-day Gemba walk, and come back with a 40-page presentation full of kanban cards and 5S color-coded floors. Six months later, nothing has changed except the floor is really shiny. The waste is still there, it's just hiding behind new visual management.
Here's how you actually start. Pick one product family. Not the entire line, not your top five sellers - one product family. Map the current state with actual data, not estimates. Walk the process from raw material to shipping and time every single step. I've seen this take anywhere from two days to six weeks depending on how messy the operation was. The key detail everyone misses is that you need to distinguish between value-added time and non-value-added time. Most processes are 5-15% value-added. The rest is movement, waiting, or rework disguised as productivity. Once you have the map, you identify the bottleneck. This isn't always obvious. The slowest machine isn't necessarily the constraint. In one case I dealt with, we had a welding station that was technically the slowest process, but the real bottleneck was a quality inspection step three stations downstream that had a backlog of four hours. Fixing the welder would have done nothing. We reorganized the inspection workflow and reduced total lead time by 62% in three weeks. That's the kind of insight you only get by being physically present and measuring actual flow, not theoretical capacity. After identifying constraints, you implement pull systems. Kanban is the most well-known tool here, but don't treat it as a silver bullet. A kanban card is just a signal. If your underlying process is unstable, a pull system will just make the instability more obvious and more painful. I had a case where we introduced a two-bin kanban system and within two weeks, both bins were empty every afternoon because the supplier couldn't keep up with the revealed demand rate. The solution wasn't better kanbans. It was negotiating a daily delivery schedule with the supplier and reducing order quantities. The kanban was never the problem. The supply chain was.
One thing that beginners consistently overlook is the role of standard work. You can't improve what isn't standardized, and you can't standardize what you don't understand. Standard work documents are often treated as bureaucratic exercises - a form to fill out so management feels like they're doing something. Real standard work is different. It's a living document that captures the best known method at a given time, and it gets updated constantly as improvements are made. If your standard work hasn't changed in six months, you're not improving. You're just maintaining the status quo with better paperwork. Another counter-intuitive point: single-minute exchange of die (SMED) isn't just for high-mix environments. We applied a simplified SMED approach to a food processing plant that ran a single product for six months at a time. The changeovers between products took four hours because the cleaning procedure wasn't broken down systematically. By separating internal and external setup activities and converting as much as possible to external work, we reduced changeover to 47 minutes. That allowed us to run smaller batches and cut work-in-process inventory by 35% without any equipment changes. Just better changeover discipline. There's also the question of JIT (just-in-time) and when it completely fails. JIT assumes predictable demand and reliable supply. If your demand fluctuates by more than 30% month-over-month or your suppliers have lead times longer than your consumption rate, JIT will just create stockouts and angry customers. In those situations, a hybrid approach works better. Keep strategic buffer inventory for critical components while implementing pull systems on stable, high-volume items. Don't try to be theoretically pure. Be practically effective.
Get the Full Details
Continuous improvement, or kaizen, is the engine that keeps Lean going, but it's also where most organizations lose momentum. The problem isn't that people don't want to improve things. It's that improvement efforts aren't connected to daily work. When kaizen events are scheduled as special occasions - a week off the floor, a team retreat, a contest with prizes - they become disconnected from the actual process. Sustainable improvement happens when every person on the floor spends 10-15 minutes each day identifying and addressing small problems. Not big projects. Small problems. A tool that's always in the wrong place. A step that requires awkward body positioning. A measurement that's always inaccurate. I once worked with a team that implemented a daily 15-minute problem-solving huddle at the cell level. They used a simple three-question format: what happened yesterday, what's different today, what could go wrong. No PowerPoint. No reports. Just five people standing around a whiteboard talking about their actual work. Within four months, the team had identified and resolved 127 small issues that were collectively causing maybe 20% downtime. Individually, each one was too small to justify a formal project. Together, they were massive. The trick was making it habitual, not heroic. The biggest limitation of Lean that nobody likes to admit is that it requires a certain level of organizational maturity. If you have no baseline data, no trust between management and workers, no willingness to confront problems openly, Lean tools will look like theater. A and B cards won't fix a broken culture. A value stream map won't help if people are still working in silos and protecting their own metrics. In these cases, the work before Lean is building basic management discipline - regular communication, shared goals, honest reporting. Skip that and you're decorating a sinking ship.
Another hard truth: Lean doesn't scale well without delegation. When I've seen Lean programs fail at the enterprise level, it's usually because everything flows through a central team of Lean experts. They become the bottleneck for improvement itself. The organizations that succeed treat Lean as a operating system that every manager runs, not a project that a special team delivers. This means training supervisors, not just engineers. It means giving people the authority to stop the line, not just the responsibility to meet output targets. If you're starting from scratch and your operation is fairly simple - low product variety, stable demand, mostly manual processes - you can get meaningful results in 90 days with focused effort on one product family. More complex environments with high mix and variable demand might take 6-12 months before you see sustained improvement. The timeline depends entirely on how much hidden waste you're dealing with and how quickly people learn to see it. The fundamental insight that separates successful Lean implementations from unsuccessful ones isn't the tools. It's the willingness to let the organization feel uncomfortable. Lean removes the cushions that hide problems. Reduced inventory means no buffer when something goes wrong. Takt time means the pace is set by the customer, not by management's monthly targets. Standard work means everyone knows exactly what's supposed to happen, so deviations are immediately visible. This creates friction. Good friction. But it's still friction, and people resist it. The organizations that push through that resistance are the ones that benefit.