Working with Koh Young AOI Systems
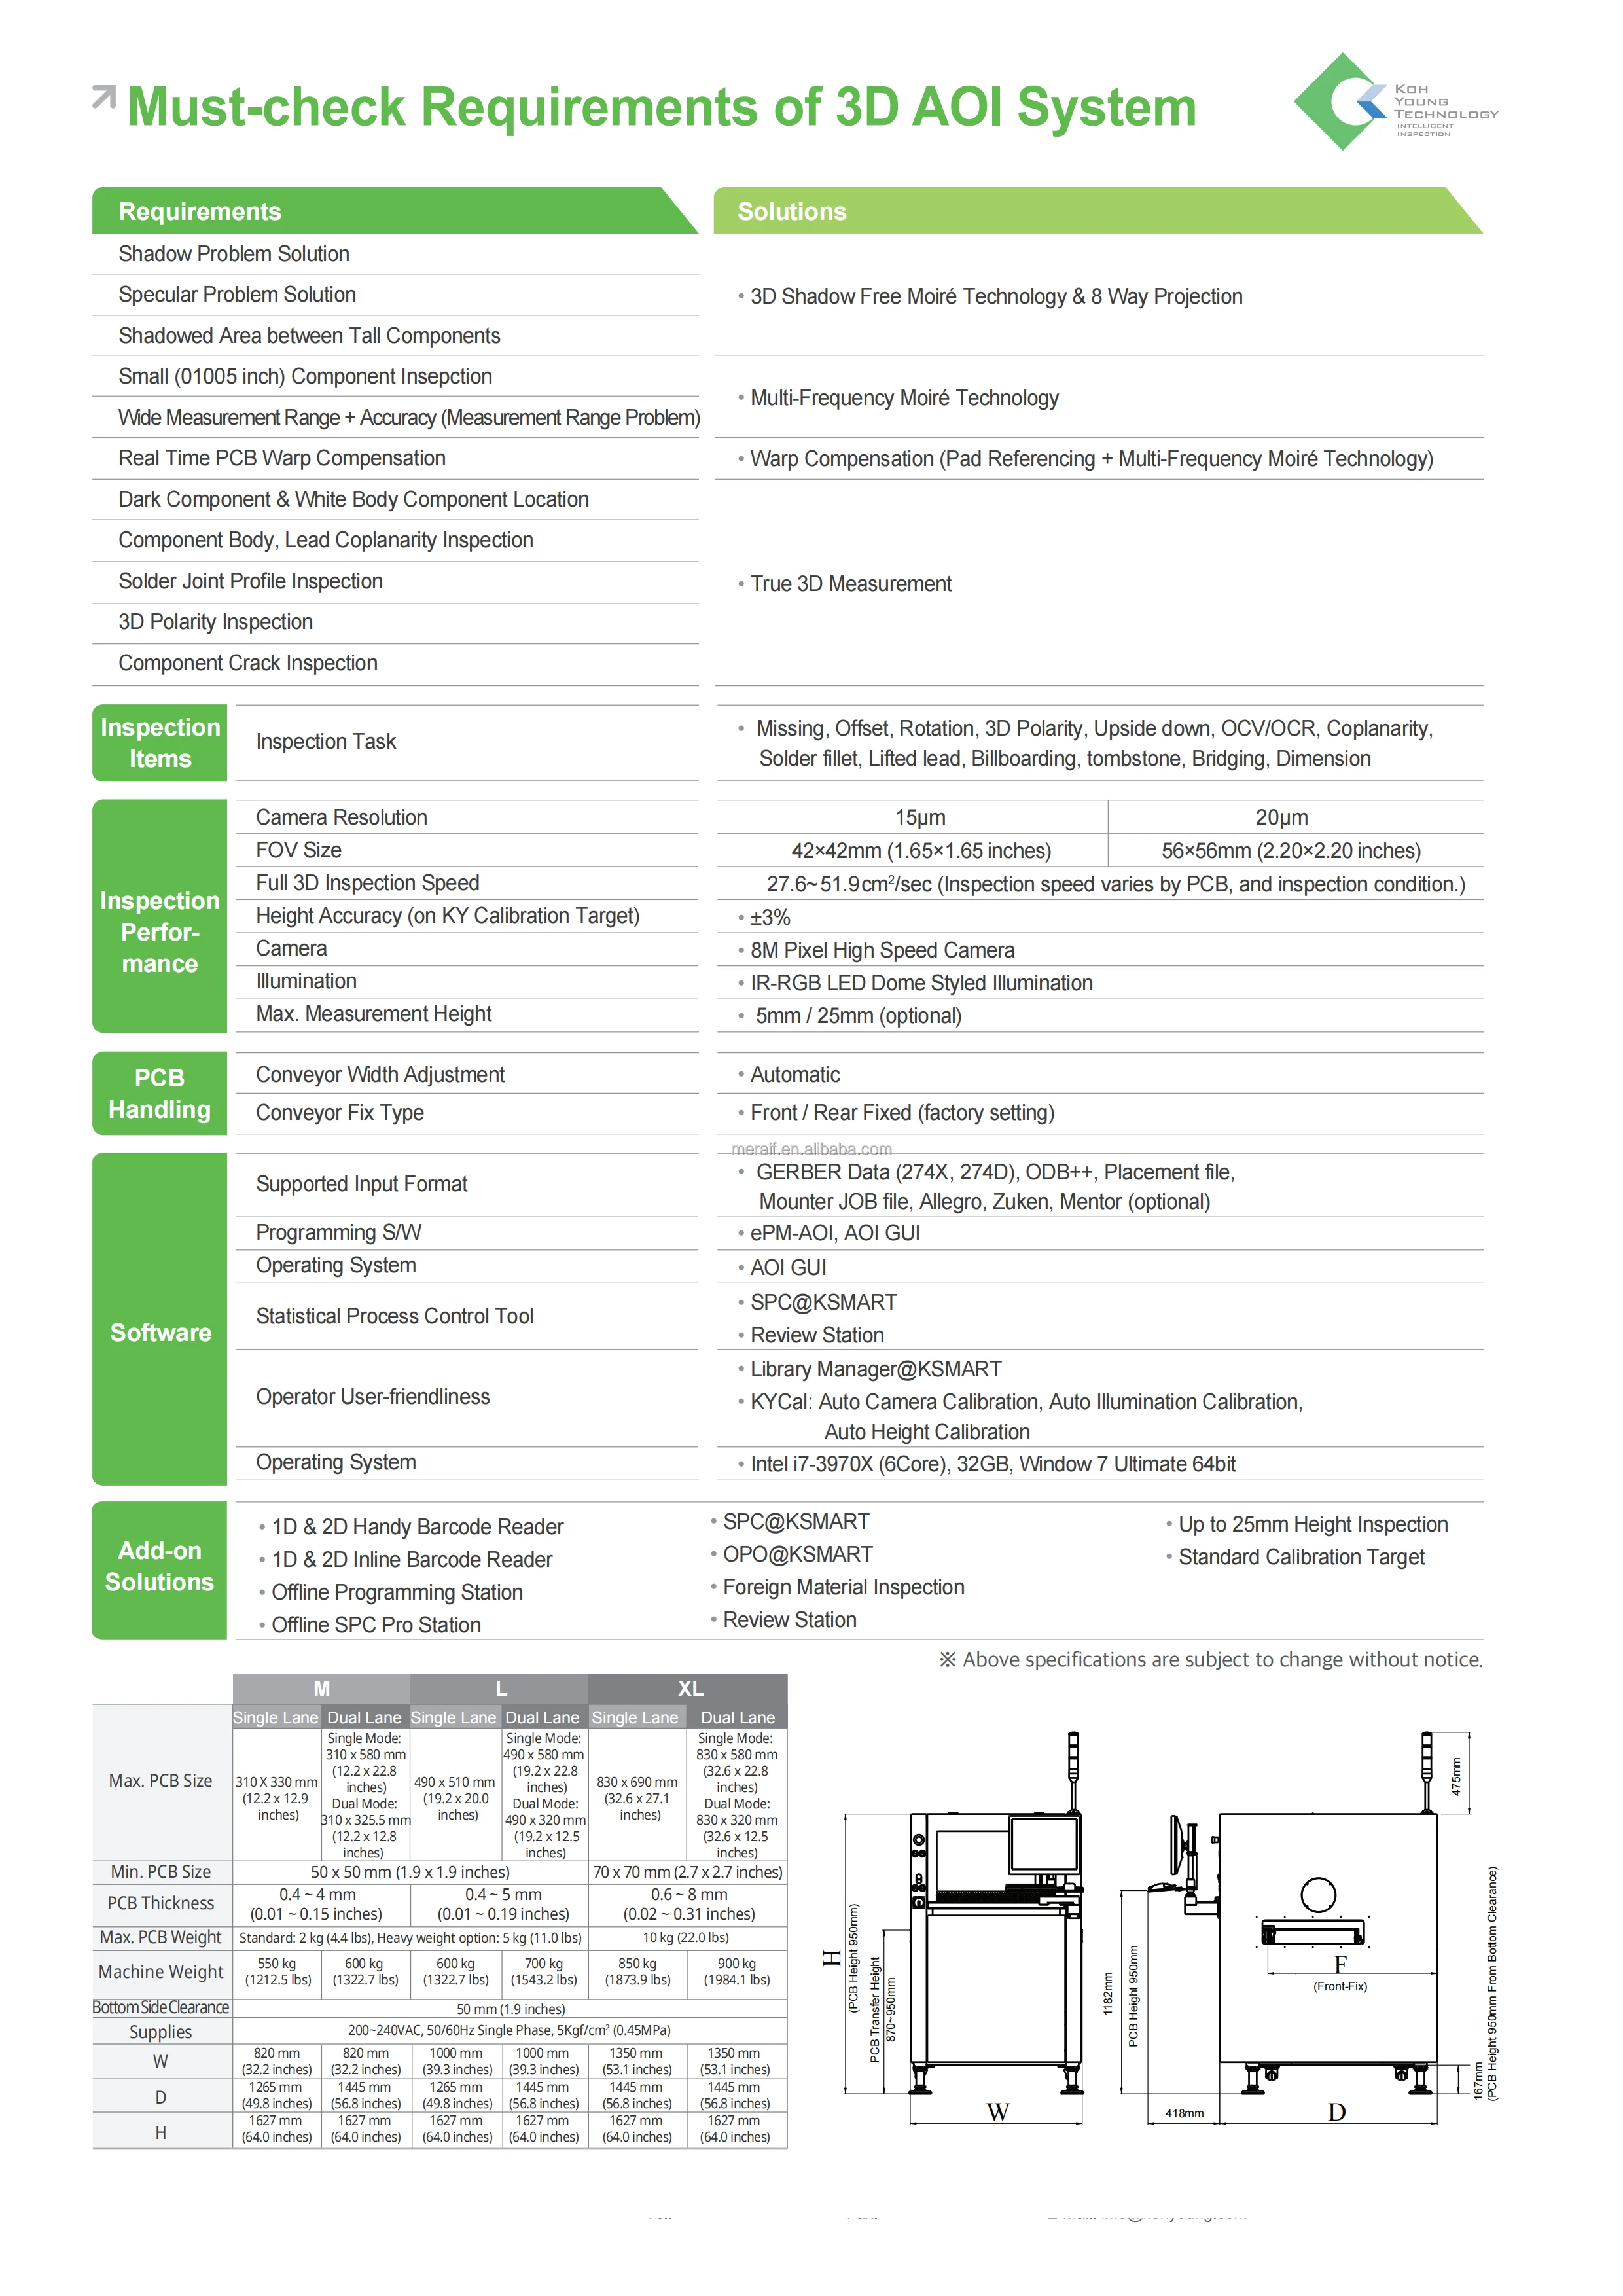
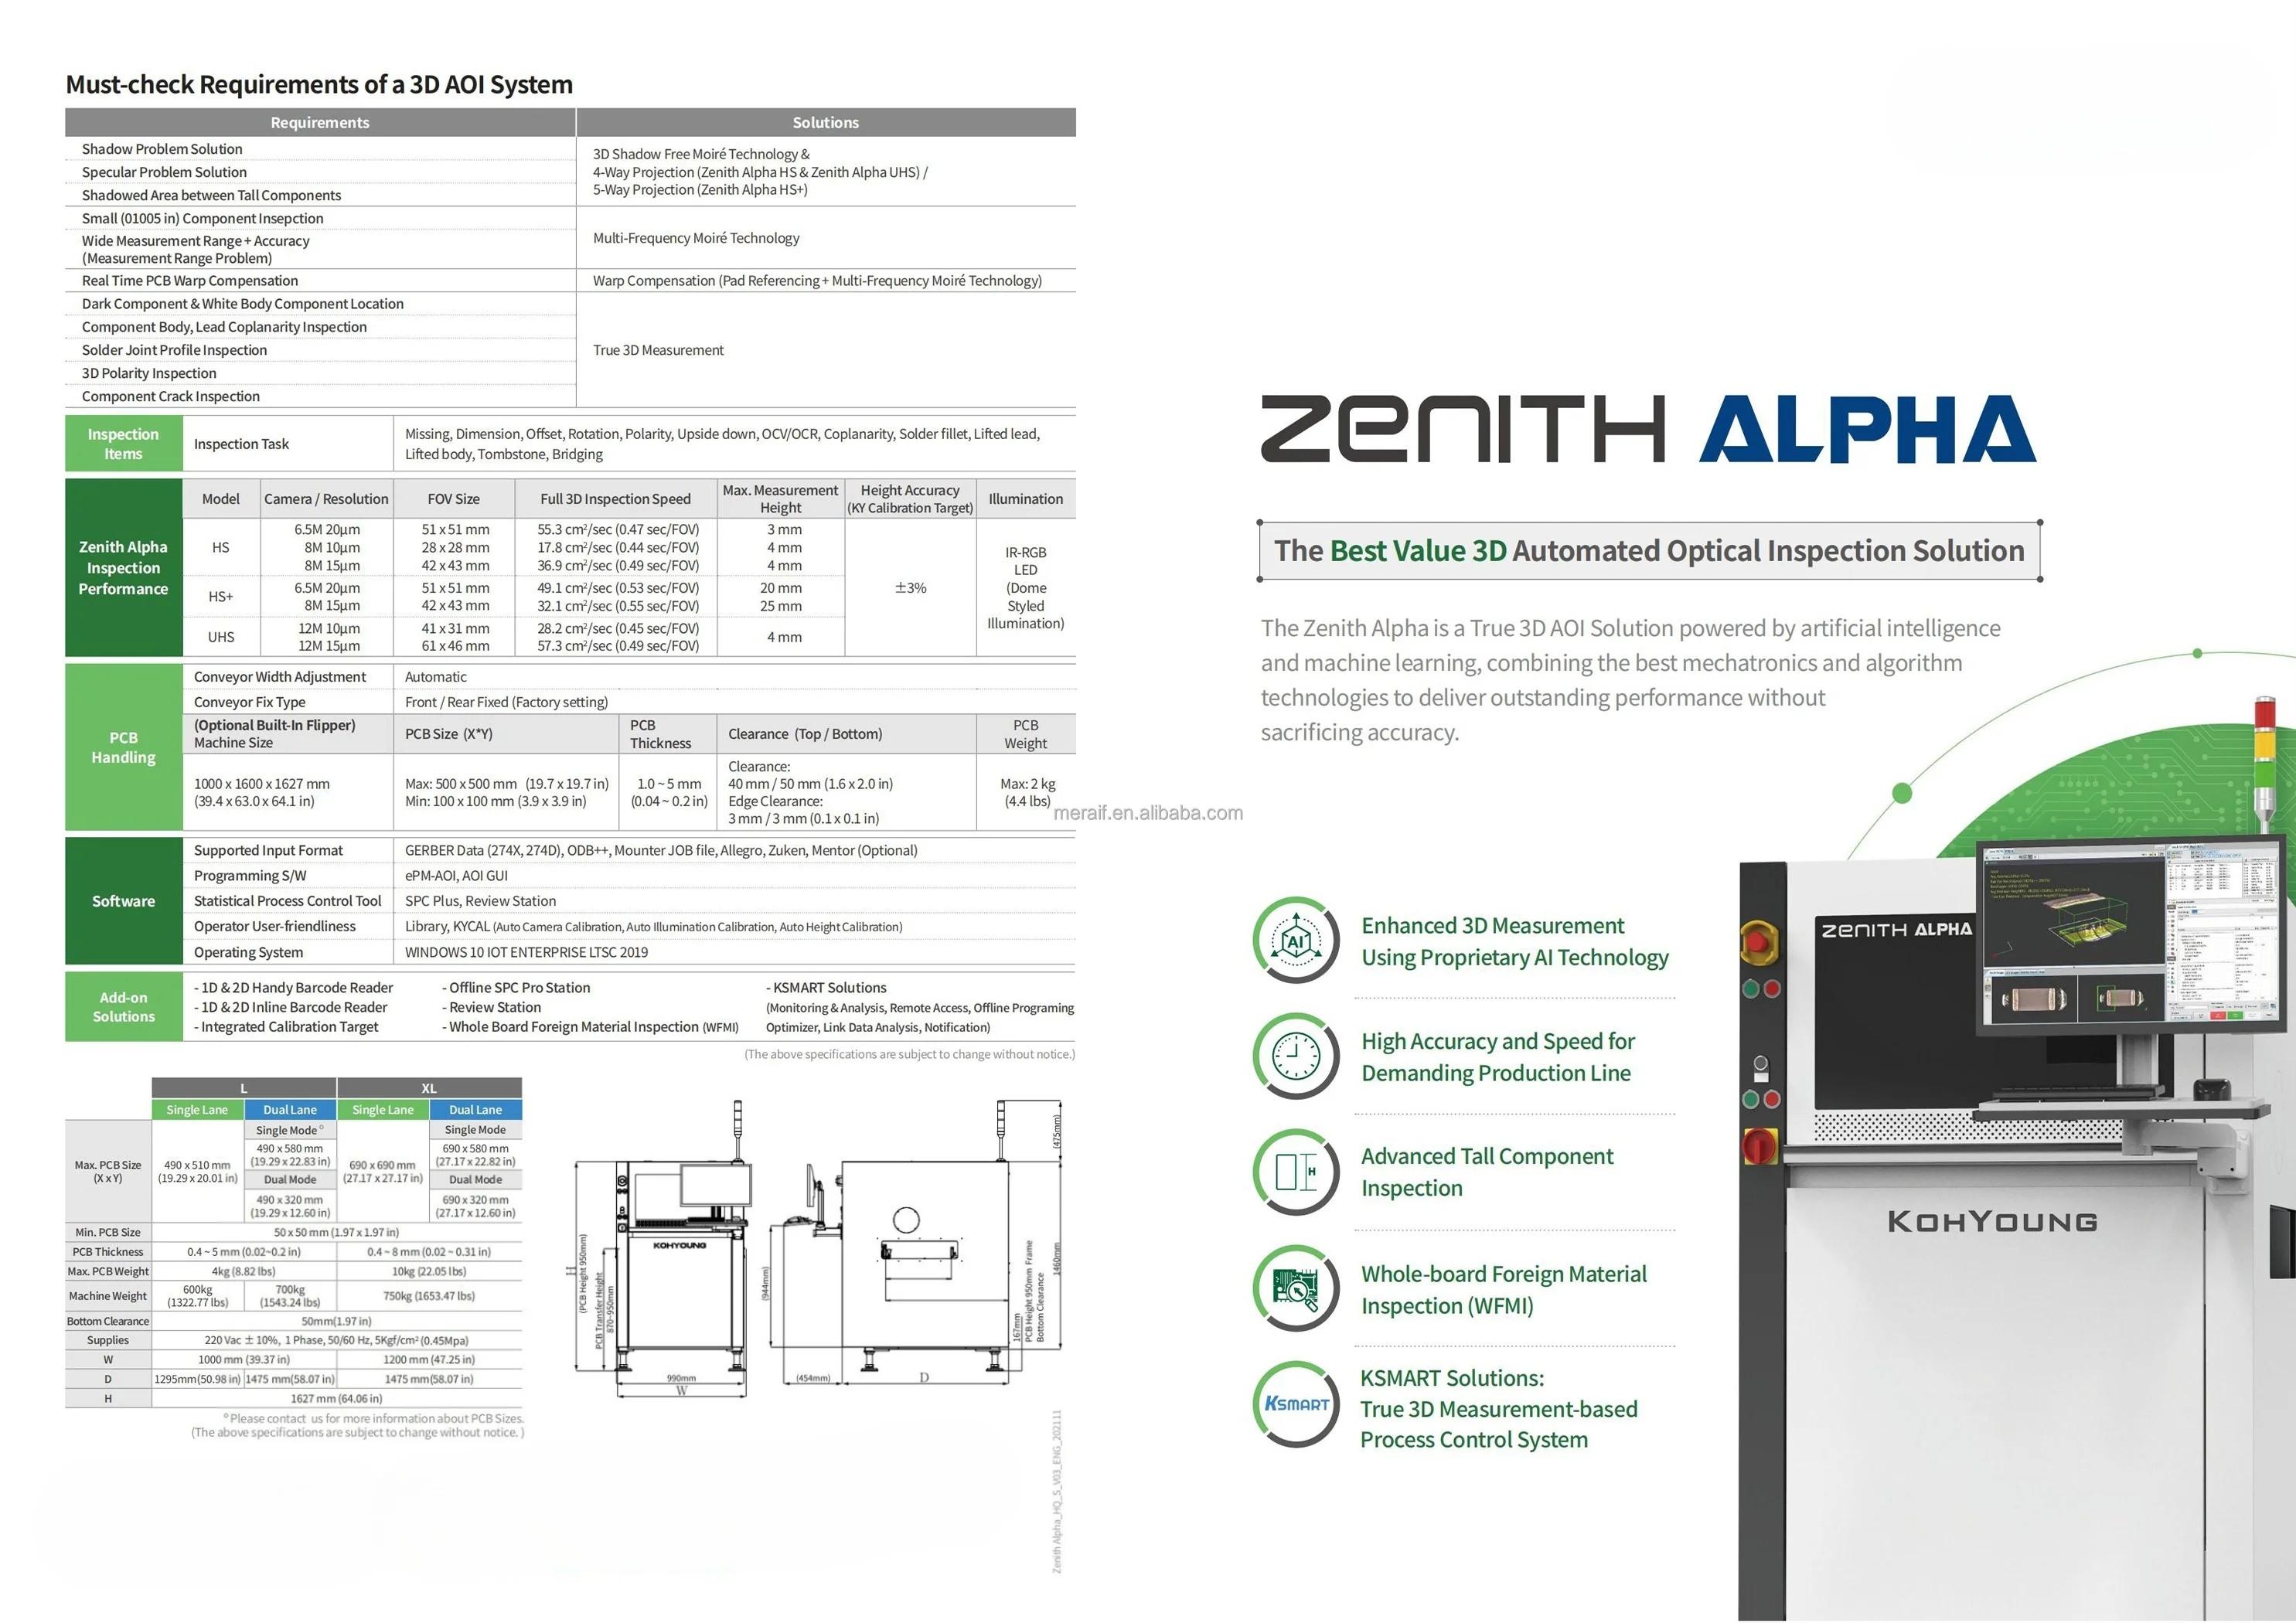
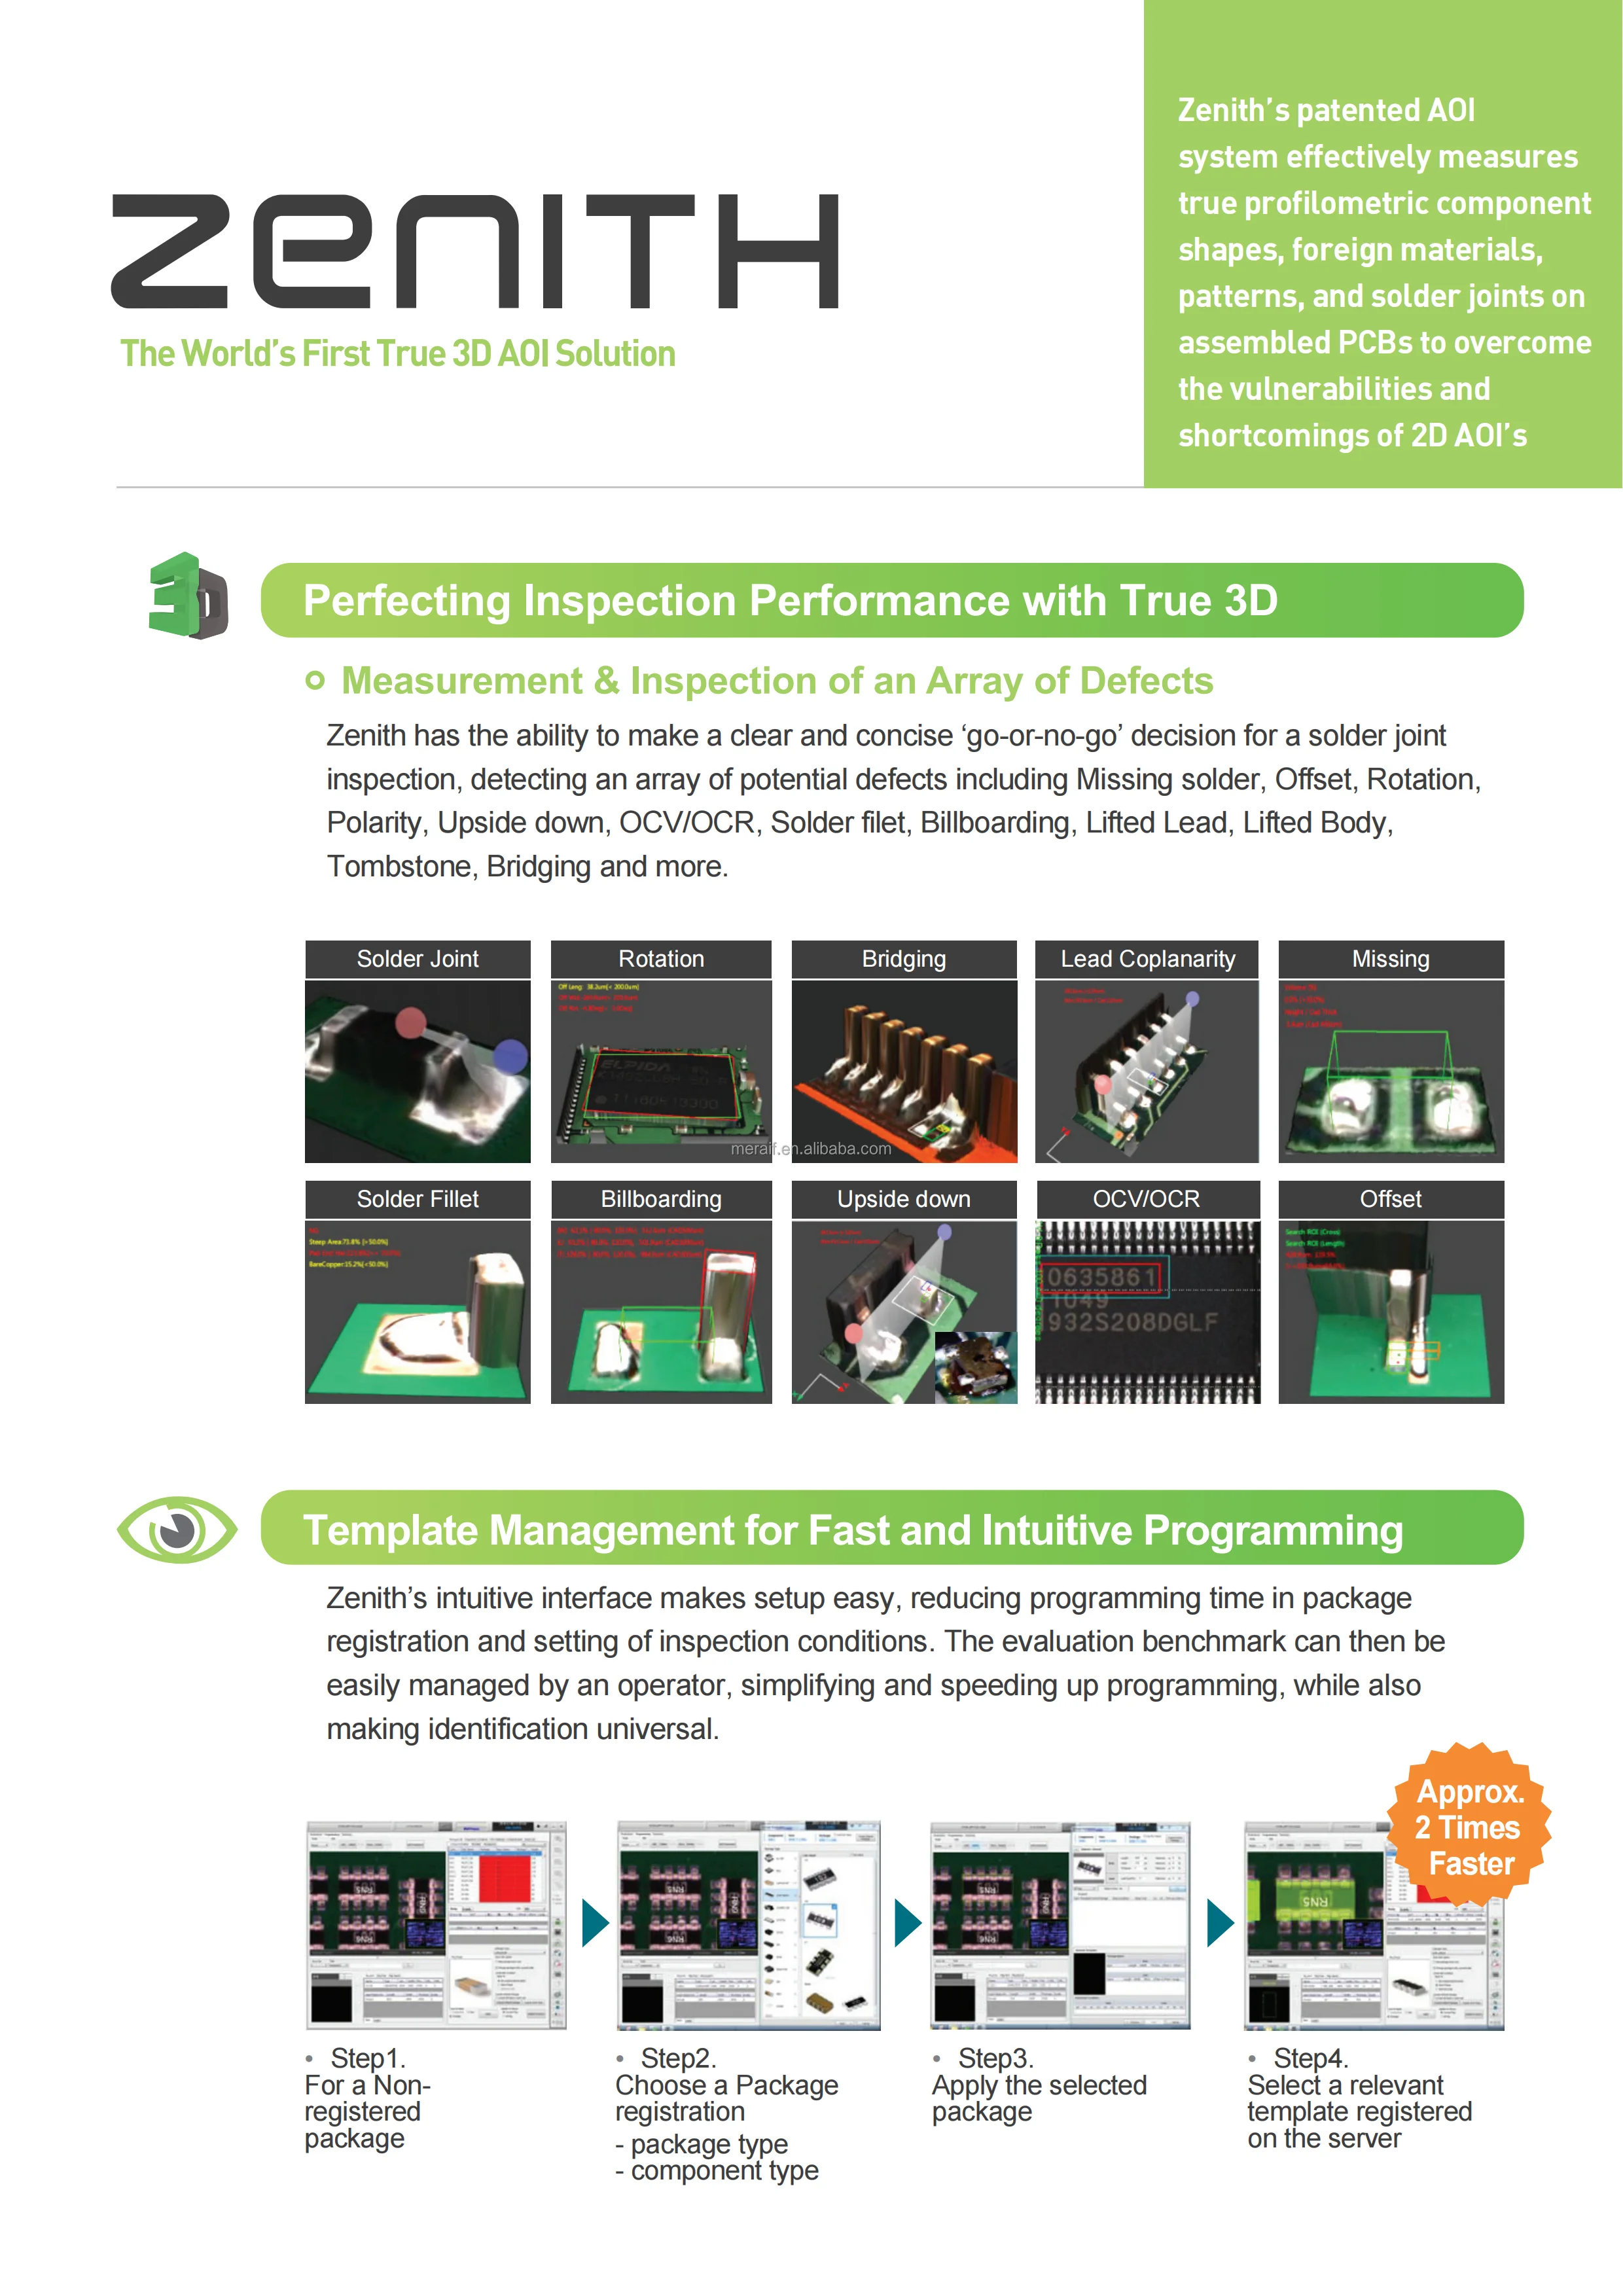
The Koh Young Aoi Manual documents a lot of edge cases that the help menu doesn't really cover. Most people looking at this stuff are SMT line engineers dealing with false calls or missing defects on high-mix boards. I've spent more years than I care to count troubleshooting these units across different fabs. Here's the practical breakdown. The interface isn't intuitive for first-time users. You'll want to focus on the inspection recipe builder first, not the reporting module. The recipe system controls everything downstream, and getting confused there leads to garbage data no matter how clean your imaging is. Start by mapping your board outline in the stage coordinates, then move to component library setup. One thing that trips people up constantly is the camera calibration sequence. The manual glosses over the fact that environmental temperature swings of just 3 degrees Celsius can throw off your pixel-perfect alignment. I had a whole production run of 01005 passive components called false opens because the lab AC kicked on during a noon shift change. The workaround was scheduling all calibrations during the morning warmup window when the room was most stable.
Common Pitfalls and Workarounds
Solder paste inspection mode has a notorious issue with dark solder paste formulations. The standard algorithm assumes a certain reflectivity profile, and when you switch to lead-free paste with higher tin content, your IPC class 2 readings drift consistently false. The fix isn't in the manual's basic settings. You need to adjust the brightness compensation table manually for your specific paste vendor. I keep a reference spreadsheet with compensation values for each paste type we run. Another thing nobody warns you about: the component height measurement function is highly sensitive to board warpage. If your substrate exceeds 0.75 millimeters of bow and twist, your Z-axis readings on tall components become unreliable. I found that running the inspection with the board vacuumed to exactly 45 kPa and allowing a 90-second stabilization period reduced our height measurement variability by about 60 percent.
Recipe Transfer Between Units
You can migrate inspection recipes between machines, but only if they're the same hardware generation. A recipe built on a Volition series won't fully carry over to a different chassis without manual tweaking. I've lost about half a day to this before remembering to check the firmware version match first. The transfer process uses the File menu export function, but verify your component libraries are synchronized on the destination machine before importing. The software also has a ghost in the maintenance logs. If you've been running extended inspection cycles above 8 minutes per board, the system accumulates optical housing dust faster than the auto-wipe routine can handle. You'll see rising false call rates without any obvious pattern. The maintenance schedule in the manual suggests 30-day intervals, but in a high-production environment with heavy solder flux usage, I've found biweekly cleaning of the illumination ring and top cameras is necessary to maintain consistent defect detection rates.
Get the Full Details

Reporting and Data Export
For traceability requirements, you'll want to configure the JEDEC-compliant output format rather than relying on the default CSV. The built-in report generator has a template section that's poorly documented. Go to the Report Designer module and enable the expanded component parameter export. This gives you full XY coordinates, rotation angles, and height deltas for every inspected device, which matters when you're doing root cause analysis on intermittent defects. The network share setup for centralized data collection works but has a quirk with folder permissions. The software expects write access to a specific subdirectory structure on the server, and if any parent folder has restrictive ACLs, it silently fails to log new inspection data. I spent two weeks chasing phantom missing reports before realizing the file system permissions were the bottleneck. Mapping a dedicated shared folder with explicit write permissions for the inspection service account resolved it immediately.
Limits of the System
To be straight about the downsides, this equipment struggles with matte-finish black components. The absorption rate of those surfaces defeats the standard lighting strategies, and you'll get elevated miss rates on capacitor and resistor bodies regardless of how you tune the algorithm. For those materials, switching to the oblique lighting mode with reduced exposure helps, but you're still working with physical limitations of optical inspection. In those cases, consider supplementing with X-ray or manual verification on critical components. Another hard limit is the minimum feature size for older firmware versions. Early Volition models can't reliably inspect anything below 0201 dimensions without firmware updates that change the image interpolation method. If you're running legacy software and trying to catch 01005 defects, you'll have acceptance gaps. Check your firmware level and update if possible before committing to a tight-tolerance inspection program.