The Real Problem With LOTO Training
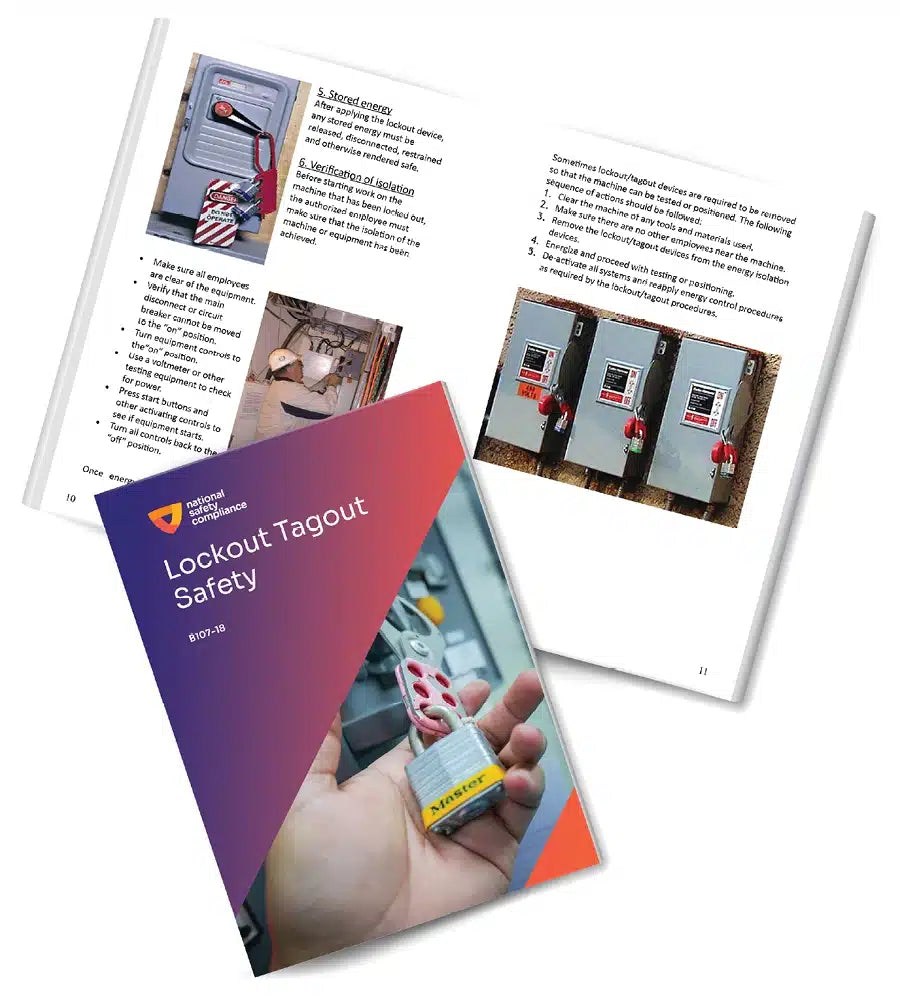
Most companies treat Lockout Tagout Training Material as a checkbox exercise. They print out a PDF, hand it to someone during onboarding, and call it compliance. Three months later, when an auditor asks about it, nobody can actually explain what happened. The gap between what the paperwork says and what happens on the shop floor is where injuries occur. I have seen it repeatedly. OSHA 1910.147 is the governing standard, but the regulation itself is thin on implementation details. It tells you the requirements but not how to meet them in a way that sticks. Effective training material has to address three distinct layers: the regulatory requirements themselves, the physical procedures for each piece of equipment, and the decision-making process workers use when something doesn't match the written procedure. Here is the thing most people miss. The six-step sequence — notify affected employees, shut down, isolate, apply lockout/tagout devices, release stored energy, and verify isolation — is simple in theory. In practice, the verification step is where everything falls apart. A machine can appear off. The main breaker can be in the open position. Yet a secondary circuit or a residual charge keeps energy present. I spent two days tracking down an intermittent fault on a packaging line where the verification step was technically followed but done wrong. The pressure accumulator on the pneumatic system had a check valve that held residual pressure even after the main supply was shut off. The lockout procedure on paper didn't mention bleeding that accumulator. Nobody had caught it during the initial procedure development because the machine had never been opened for maintenance in over a decade. The workaround was straightforward — I required every compressed air line entering the machine to have a bleed valve within three feet of the point of connection, and I added a second verification step requiring a pressure gauge reading below 5 PSI before any work begins.
Building Procedures That Actually Work
Energy source identification is the foundation, and it is also where most programs fail. A typical industrial machine can have electrical, pneumatic, hydraulic, gravitational, thermal, and chemical energy sources. Electrical is obvious. The others are not always obvious to the person filling out a form from a template. I reviewed a lockout program for a food processing plant once where the freeze system had zero thermal energy isolation steps. The ammonia refrigeration circuit could hold enough thermal energy to cause severe frostbite if a line was opened while pressurized. It wasn't in their procedure at all. They just listed "electrical disconnect" and moved on. The correct approach requires a walkthrough with the procedure writer standing next to the equipment, tracing every energy path from its source to the point of work. This is not something you do from a desk. You cannot read a manual and figure out that a servo motor will continue to rotate under load for approximately four seconds after power is removed, or that a spring-loaded clamp stores enough energy to snap shut with considerable force. You need to see it, understand the mechanism, and document the specific method to control it. Group lockout is another area where training material is routinely inadequate. The standard allows multiple workers to be covered under a single lockout device through a group lockout procedure, but the details matter. There must be a primary authorized employee who maintains control of the energy isolation. Every other worker applies their own personal lock to a group lockbox or has an individual lock directly on the isolation point. The procedure needs to specify exactly how the group leader verifies that all workers are clear before re-energization. I worked at a facility where the group lockout procedure simply said "the supervisor will ensure everyone is clear." That is not a procedure. It is a hope. We rewrote it to require a headcount at the lockbox before the group leader removes their lock, with each worker individually unlocking and removing their own device. No exceptions.
Lockout Tagout Training Material for Different Audiences
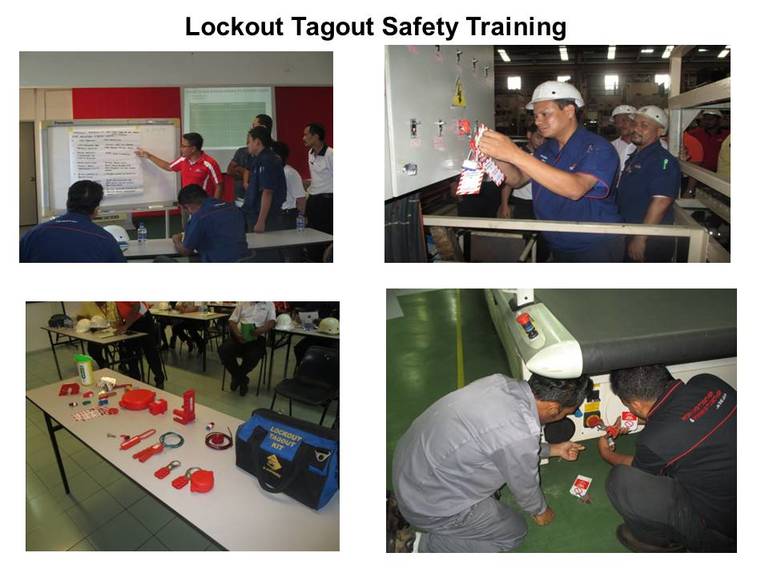
Authorized employees, affected employees, and other employees outside the immediate area all need different training. This is required by the standard and it is also just good practice. An authorized employee who opens a machine needs detailed, equipment-specific instruction. An affected employee who walks past the machine during maintenance needs to understand why they cannot operate controls they normally would. A warehouse worker who happens to walk through the area needs a completely different level of awareness. One training document that covers everyone is a compliance failure. Refresher training is another common gap. The standard requires it when there is a change in job assignments, machines, or procedures, and whenever there is reason to believe an employee's knowledge or compliance has declined. That last condition is subjective, which means it is frequently ignored. I recommend scheduling annual refreshers regardless, because after a year without real practice, most workers will skip steps they learned during initial training. The steps they skip are usually the verification step and the stored energy release step. These are the steps that prevent deaths. Periodic inspection of the energy control procedure is required at least annually. This is not the same as refresher training. It is a review of the written procedure itself to make sure it still accurately reflects the machine's current configuration and energy sources. Machines get modified. Controls get added. Circuits get re-routed. If the procedure wasn't updated after those changes, the annual inspection won't catch it unless the inspector physically walks through the lockout sequence on the actual equipment. I made it a rule that the annual inspection requires one full simulated lockout by the authorized employee performing the inspection, with the procedure document in hand, marking off each step as it is performed. Any deviation from the written procedure is immediately documented and the procedure is corrected. This catches about 80 percent of the drift that happens over time.
Get the Full Details

What Lockout Tagout Training Material Cannot Fix
Training material has real limitations. It cannot compensate for a culture that prioritizes production speed over safety procedure. I have seen lockout procedures take forty-five minutes to complete on machines that only needed twenty minutes of actual maintenance work. When supervisors are implicitly or explicitly pressuring workers to finish faster, the lockout gets shortened. No amount of training material changes that dynamic. The intervention has to come from management, and it has to be visible. The person who can get away with skipping lockout steps sets the tone for everyone else in that area. Lockout tagout also cannot address every scenario. Portable tools with double insulation that are plugged into receptacles rather than hardwired are generally exempt from lockout requirements under OSHA guidelines, but the line between portable and fixed equipment can be blurry. A permanently mounted grinder that is cord-and-plug connected exists in a gray area. Some interpreters consider it portable equipment. Others require lockout. You need to make a determination and document it consistently across your facility. Contractor coordination is another area where training material alone is insufficient. When a third-party vendor comes in to perform maintenance on your equipment, both your team and theirs need to understand each other's lockout procedures. The standard requires the hosting employer to inform contract employers about the lockout procedures in use at the facility. This usually means a brief conversation at the start of the job, not a comprehensive training session. But that brief conversation needs to cover the specific energy isolation points, the lockout devices in use, and the notification process for re-energization. I have seen contractor lockout failures happen because the host facility assumed the contractor already knew the procedure, and the contractor assumed the host would handle it.
Store energy release is a concept that trained workers often underestimate. A large capacitor bank in a variable frequency drive can hold a lethal charge for hours after power is removed. A pressurized hydraulic system can release enough energy to inject fluid through skin. A suspended load held only by a mechanical lock can drop if that lock fails. Training material needs to address these scenarios with specific, equipment-level detail, not generic statements about "releasing stored energy." The worker needs to know exactly what to do, where to find the bleed valve or discharge resistor, and how to verify that the energy is actually gone.