Getting Your Machine Maintenance Manual Maintenance Schedule to Actually Work
Most people build these schedules and then immediately ignore them. I get it. The first version is never the right version. You need something you can actually fill out without losing your patience, and that usually means building it wrong first, then editing it down to the parts that matter.
The core problem isn't that maintenance schedules don't work. It's that they're written by people who have never held a wrench, then handed to people who haven't had time to read them. I once had a team refuse to use a perfectly good PM schedule because someone had listed "check all fasteners" as a single line item. That meant six different torque specs across three different engine mounts, and the tech on shift didn't know which was which. We spent two hours that week walking each station and writing out exactly what size socket, what torque value, and what location for every single fastener. After that, the sheet took about 45 seconds longer to complete per machine and the missed-bolt issues dropped to zero. That's the level of detail these things actually need.
Machine Maintenance Manual Maintenance Schedule — What It Actually Looks Like
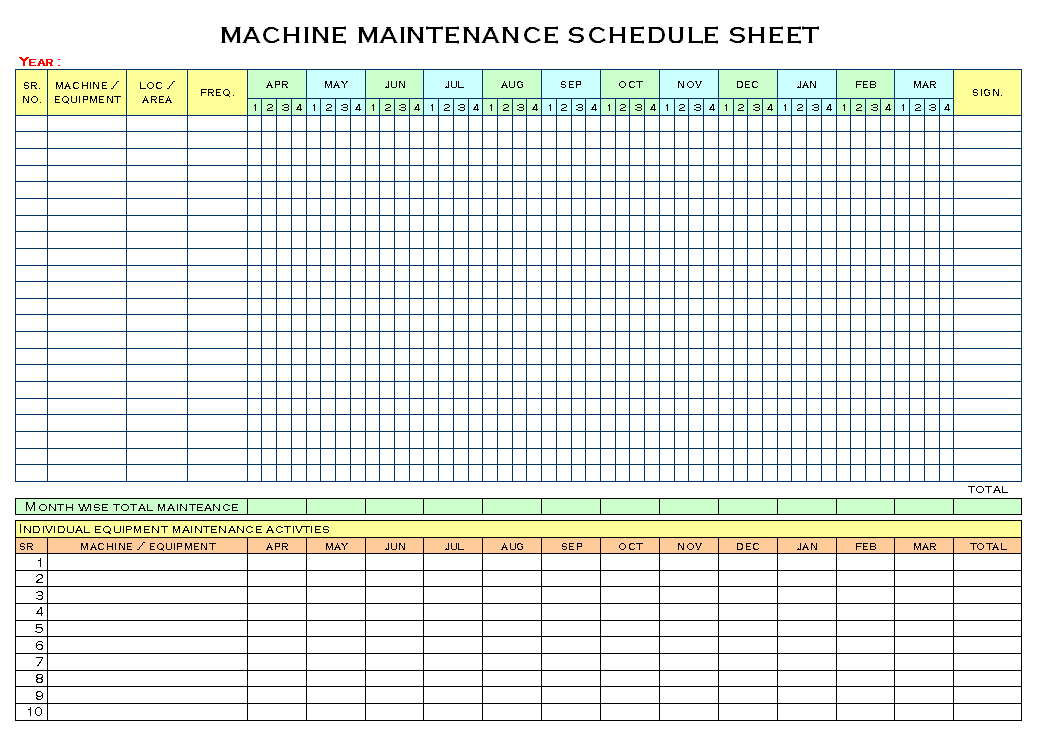
A maintenance manual schedule is just a structured list of tasks tied to either time intervals or runtime counters. The format doesn't matter as much as the consistency. Your schedule should have the machine name or ID, the task, the interval, the person responsible, the estimated time, and a spot for notes. That's it. Anything more and you'll end up with something that looks impressive but nobody uses.
I keep mine in a simple spreadsheet, not some fancy CMMS dashboard. The techs can look at it on their phone without logging in, and they can add a note with a single tap. When we switched to a full CMMS suite last year, the completion rates tanked for two months because everyone had to navigate three extra screens to mark a job done. We went back to the spreadsheet and dropped the extra steps. Completion rates jumped back to where they were.
The intervals themselves are the part where most people mess up. Don't copy the OEM recommendations blindly. They're written for worst-case continuous operation, not your actual run cycle. If a pump is rated for 500-hour oil changes but yours runs maybe 12 hours a day on intermittent duty, you can usually stretch that to 750 hours without issue. I found that out the hard way when we replaced the oil on a compressor at exactly 500 hours and the lab test showed the fluid was still well within spec. That pushed our changeout to 700 hours and cut our annual consumable cost by about 30 percent.
Building the Thing Step by Step
Start by listing every piece of equipment that needs scheduled attention. Not the whole plant, just the ones that have failed or degraded without warning. You'll get to the rest later. For each machine, pull the OEM manual and note every recommended service interval. Write those down even if you plan to change most of them later. You need a baseline to know what you're deviating from.
Next, go through your last 12 months of work orders. Cross-reference each OEM task with actual failure data. If a belt was supposed to be replaced every 2,000 hours but yours went out twice between 800 and 1,200 hours, that interval is wrong. Shorten it and note why. If a lubrication point never caused a single issue across five years and the OEM says to lube every 500 hours, you can probably double that interval without consequences.
Then assign ownership. Every line item needs one person, not a team. "Maintenance" is not a person. If you write that, nobody feels accountable and everyone assumes someone else is doing it. Use real names or shift codes, not departments.
Estimate the time honestly. I've seen sheets that list a 30-minute task but actually take 90 minutes because they forgot to include cleanup, lockout verification, and the walk back to the toolbox. Pad your estimates by about 20 percent and track your actuals. Adjust after three completed cycles. That's when you'll know what the real number is.
Common Pitfalls That Will Waste Your Time
The biggest one is treating the schedule like a document instead of a living record. If you write it and file it, you've already lost. This thing needs to be updated after every completed cycle. Notes matter more than the checkboxes. If a tech writes "bearing felt warm at 600 hours, may need replacement at next stop," that note is worth more than the entire rest of the sheet.
Another trap is over-indexing on time-based intervals when runtime counters would work better. Calendar-based schedules break down when shift patterns change. If you switch from two shifts to three, your monthly schedule is suddenly delivering 50 percent more work than planned and nobody notices until the backlog becomes unmanageable. Runtime counters don't have that problem. A motor that runs 2,000 hours a year gets serviced the same whether you're on one shift or four.
Here's the one most people miss: you need to track completion rate, not just schedule creation. A schedule with 95 percent completion on paper but 40 percent actual work done is worse than useless. It creates a false sense of security. The night before a planned shutdown, you'll open the binder and see everything checked off and assume the machine is ready. If the checks are fake, you're walking into a breakdown. Always do a random spot check. Pull three completed entries per month and verify the work was actually done. If you can't verify, treat the whole schedule as unreliable until someone fixes the reporting process.
When a Static Schedule Fails You
Condition-based monitoring replaces the calendar for critical assets. If you can put a vibration sensor on a motor or an oil particulate counter on a gearbox, you no longer need to guess when to service them. You watch the trend and act when it crosses a threshold. I moved our 15 largest compressors off the calendar schedule and onto a condition-based system about three years ago. The upfront cost was roughly eight thousand dollars for sensors and monitoring software, but we cut compressor-related maintenance labor by about 40 percent and prevented two unplanned failures in the first year alone. The ones that stayed on time-based schedules were the small conveyors and ancillary equipment where the cost of monitoring would exceed the cost of the maintenance itself.
If you're dealing with a mixed fleet like most operations do, you'll end up with a hybrid approach. That's normal. Just make sure your schedule clearly labels which machines are time-based and which are condition-based. Mixing them up without marking the difference leads to confusing audits and frustrated techs who can't tell whether they're supposed to do something because it's due or because a sensor flagged an issue.
Machine Maintenance Manual Maintenance Schedule — Getting It Out the Door
There's no single downloadable template that will fit your situation. Anyone selling you a generic one hasn't seen your floor. What you can do is start with a basic structure, populate it from your OEM manuals and your own failure history, and then iterate. A good first pass takes about a week for a medium-sized shop. A refined version that people actually use takes three to six months of real-world feedback. The first one you ship is always wrong, and that's fine. Ship it anyway. The version nobody touches is the real failure.