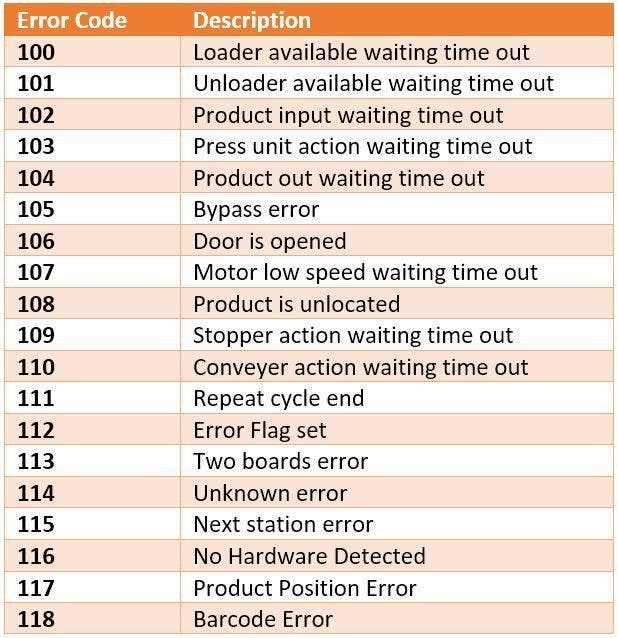
Working with machine error codes is mostly about not panicking when the display lights up.
You walk up to a CNC mill and the control screen is flashing E-47 with a red bar across the bottom. Your first instinct is to restart it. Don't. I spent three weeks last year troubleshooting a Haas VF-2 that kept throwing a spindle overload code after every two-hour run. Every time someone power-cycled it, the code went away and we called it fixed. It came back at 2:14 AM on a Thursday, of course. The real issue was a cooling fan on the spindle motor controller that had been slowly clogged with coolant residue. The controller wasn't actually failing — it was overheating and throwing a false overload flag. A simple compressed air blast and a replacement fan ($18 part) fixed it permanently. Restarting the machine would have masked the problem for days or weeks at a time. That's the thing about error codes. They're diagnostic tools, not verdicts. The manual code tells you which subsystem the machine flagged, but it rarely tells you what actually caused the flag. Understanding that gap is where most people waste time and money.
Reading Machine Operating Manual Error Codes
The most useful section in any machine manual is the error code appendix, usually near the end and often the most dog-eared part of the book because people only flip to it when something breaks. Here's how to actually use it instead of skimming and guessing. Start by noting the exact code format your machine uses. Some systems use alphanumeric codes like FANUC's A-series alarms (A001, A2xx, etc.), others use purely numeric formats like Mitsubishi's MELDAS system with four-digit codes, and some, like older HAAS controls, mix both. The format matters because different families of codes often share the same number across different subsystems. An E-47 on a lathe means something entirely different from an E-47 on a machining center. Always confirm you're looking at the right manual for your specific model and control revision. I learned this the hard way with an older OKK machining center where the error code list in the operator's manual didn't match the actual control firmware. The service manual had the corrected version, but only because I called the dealer and asked for the latest revision update. When you find the code entry, read the full description, not just the one-line summary. Most manuals list the cause, the likely symptoms, and the recommended corrective action. Some also include a "related codes" section that points to upstream failures. A coolant pressure alarm might actually be caused by a failed pump relay, but the manual might also note that a clogged filter or air lock in the lines can trigger the same code. Cross-referencing related codes before you start replacing parts will save you hours.
The practical workflow when a code appears
Here's the sequence I follow now, which usually cuts diagnosis time from an afternoon to something more like thirty minutes depending on the machine age and documentation quality. First, record the code exactly as displayed, including any sub-codes or accompanying messages. Modern controls often nest secondary information. A Fanuc alarm might show the main code on line one and a detail code like " servo amplifier channel 3" on line two. Write both down. Then check the machine history log if it has one. Many newer controls store a running log of past alarms with timestamps and operational conditions at the time. That log entry from last Tuesday when the same code appeared during a heavy cutting operation tells you something a current-state snapshot never will. Next, verify the code isn't a ghost alarm. This sounds obvious but it's surprisingly common. Loose wiring, marginal sensor signals, and ground loops can all cause intermittent codes that clear on their own. If the machine has been running fine for twenty minutes after clearing the alarm, don't assume it's resolved. Run a test cycle that stresses the affected subsystem. For a spindle overload code, run the spindle at 80% load for five minutes. If the code returns under load, you've confirmed a real fault. If it doesn't, you're dealing with an intermittent electrical issue and the diagnostic path changes completely.
Get the Full Details

After that, move from simple to complex. Check the easy things first: fluid levels, air pressure, filter status, belt tension, lubrication lines. I once spent two hours chasing a recurring axis position error on a Mori Seiki before realizing the linear scale was covered in a thin film of chips. The scale wasn't faulty. The debris was reflecting light incorrectly and the readout was losing position feedback. A quick cleaning with isopropyl alcohol and a lint-free wipe fixed it. The manual listed scale replacement as the primary corrective action for that code, which would have cost us a day of downtime and several hundred dollars in parts.
Things the manuals don't always tell you
Error code interpretation has several nuances that barely get mentioned in documentation. One is that some codes are advisory, not fault-based. A "tool wear limit approaching" message on a modern control is a reminder, not an alarm that stops the machine. Confusing advisory messages with hard alarms leads to unnecessary and resets. Another is that manufacturers sometimes change code meanings between control software revisions without updating the printed manual. If you're working with a machine that's had control upgrades, always check whether your physical manual matches the installed firmware version. The error code for a particular alarm can shift between revisions, and a mismatched manual will send you down the wrong path. A more counter-intuitive point is that some of the most destructive failures start with codes that look minor. A low-lubrication alarm on a linear guide system might seem like a nuisance, but running a machine with insufficient lubrication for even an hour can destroy guideways and ballscrews that cost thousands to replace. Treat every code seriously, even the ones labeled as warnings. The hierarchy of severity varies by manufacturer, but erring on the side of caution is cheaper than erasing a mistake.
Limitations and when to call someone else
No amount of manual-reading skill replaces actual experience with a specific machine, and there are hard limits to what you can diagnose from the error code alone. Systems-level failures involving PCB-level faults, encoder feedback loops, and servo tuning issues often require specialized test equipment and schematic access that only the manufacturer or an authorized service provider has. If the error code points to a servo amplifier fault or a communication bus error and basic checks don't resolve it, the most practical move is to contact support with your recorded code, history log, and a description of what was happening when it occurred. Going further without the right tools usually means swapping parts randomly until something sticks, which is expensive and unreliable. Similarly, error code interpretation becomes much less reliable on machines that are twenty-five years old or have been through multiple unofficial repair cycles. Modification history, replaced components with non-OEM equivalents, and rewired interfaces all create scenarios where the manual's error code descriptions no longer accurately reflect the machine's actual behavior. In those cases, the manual is a starting reference, not a definitive guide.

Keeping your reference materials current
Maintain a digital copy of the relevant error code section for each machine you work with. Photocopies get lost, margins get filled with notes that become illegible, and the version in the machine cabinet is rarely the latest revision. Take a photo or scan the error code appendix every time you receive an updated manual, and keep a simple log of codes you've encountered and how you resolved them. That log becomes more valuable than the manual itself over time because it captures the actual failure patterns of your specific machines in your specific operating conditions. Two identical models from the same year can throw the same code for completely different reasons if they've been in different environments — one in a temperature-controlled room, the other next to a welding station with voltage fluctuations and conductive dust. The error code is a starting point, not an answer. The manual gives you the map, but you still have to do the walking.