Getting Machine Safety Schematics Right on the First Draw
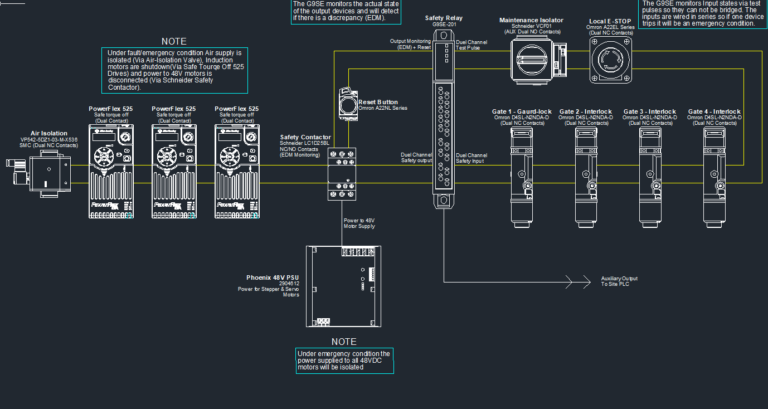
Most safety schematics I've reviewed over the years fail the same way. The designer puts together a clean block diagram, it looks fine on paper, then the field technician arrives and realizes two relays share a terminal block that can't handle the combined current draw, or the wiring path crosses an E-stop circuit in a way that violates ISO 13849-1 routing requirements. I've fixed this kind of thing three times in the last eighteen months alone. It's not glamorous work. When I say Machine Safety Manual Schematics, I'm talking about the documented electrical layout that shows every safety-related component in a machine — light curtains, interlock switches, safety relays, hazardous energy isolation points, and the logic that ties them together. This isn't the general control schematic. This is the safety subsystem drawn separately, with wire numbers, terminal designations, and fault states clearly marked so anyone can trace a single channel failure from sensor to actuator. There's a difference between a safety schematic and a regular one. Regular schematics show how the machine operates under normal conditions. Safety schematics show how the machine behaves when something goes wrong, and more importantly, they prove that a single fault won't prevent the safety function from operating. That distinction matters when you're trying to achieve PLd or PL e per ISO 13849.
How I Actually Build These Diagrams
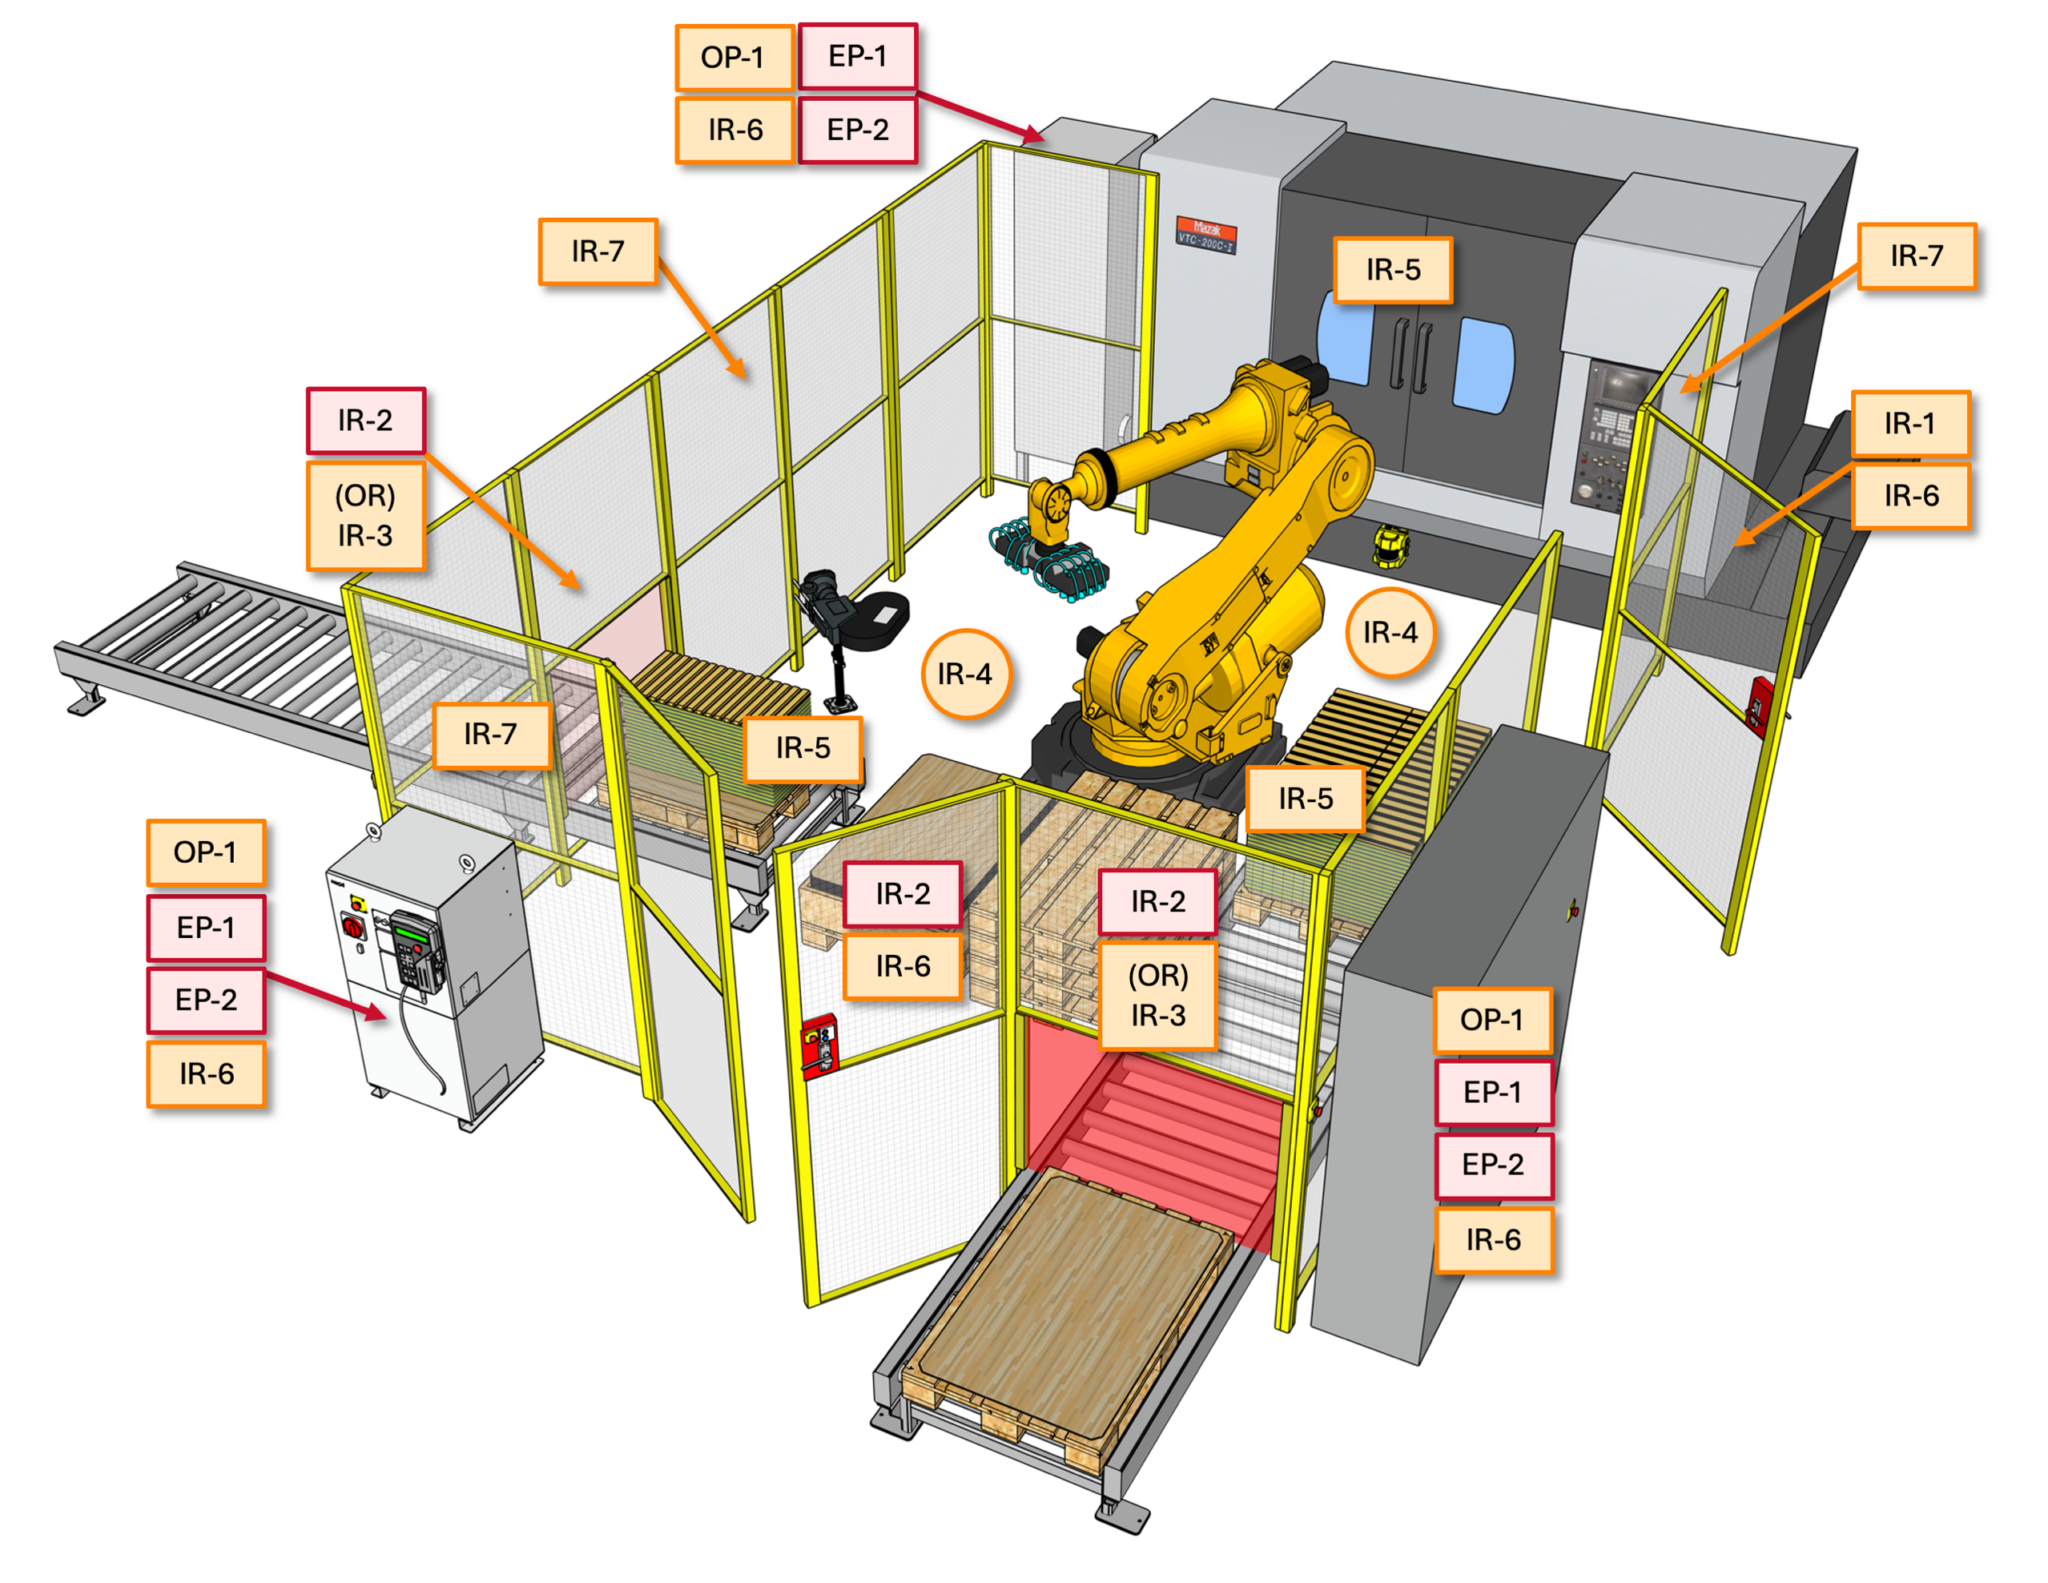
I start from the hazard analysis. Not from a template. Not from a previous machine's drawing. From the actual risk assessment for the specific piece of equipment. If you haven't done a proper risk assessment, your safety schematic is going to be missing something you didn't think to look for. I've seen this happen with robotic welding cells where the engineer copied a cutting machine's safety diagram and missed the retraction requirement on the torch head. That omission alone drops your category assignment by a full level. Once I have the hazard analysis, I map every safeguard to its input device, then trace the signal path through the safety logic controller or relay, and finally to the power stage that actually stops motion. Each path gets its own layer in the drawing. I use different line weights or colors for each independent channel — channel A, channel B, monitoring channel if applicable. When you're dealing with dual-channel safety circuits, merging them onto one visual plane makes it nearly impossible for a service technician to verify correctness during a routine inspection. Wire numbering follows IEC 61346. That's not a preference, it's a compliance expectation in most jurisdictions now. Every wire gets a unique identifier that matches across all related documents — the schematic, the bill of materials, and the I/O table. I learned this the hard way on a packaging line audit where three separate components shared the same wire number because the original engineer never checked for conflicts. The auditor flagged it as a documentation deficiency. Fixing that took two days of re-labeling and re-verifying every connection point.
The Problem I Run Into Most Often
Here's a specific case that comes up repeatedly. You're designing a dual-channel safety circuit for a press brake with two-hand control stations. The manual says you need redundancy with cross-monitoring. So you wire two contactor coils, each on its own channel, and you cross-connect the monitoring inputs. Everything checks out in simulation. Then you build it and the safety relay throws a channel imbalance fault every time the machine cycles. The issue is cable capacitance. When you run dual-channel signals parallel to high-current motor cables over any meaningful distance — say, more than five meters — the induced capacitance between channels creates enough current leakage to trip the monitoring circuit. The schematic looks correct. The component ratings are right. The fault is purely environmental. My workaround is to specify shielded twisted pair for all safety signal runs and route them in separate conduit from power conductors. It adds maybe eighty dollars in material cost per machine and saves you from spending a weekend troubleshooting an intermittent fault that doesn't show up in simulation.
Get the Full Details

Common Pitfalls That Beginners Miss
One thing nobody warns you about is the dormant fault. A safety circuit can fail in a way that doesn't immediately prevent the safety function from working. A welded contact on a safety relay, for instance, might not cause any visible alarm until you actually need to stop the machine. Your schematic shows the relay as functional. Your diagnostic coverage calculations look good on paper. But the physical component has a single-point failure that your architecture hasn't accounted for. This is why diagnostic coverage figures from component manufacturers matter more than you'd think. A safety relay with 90 percent diagonal diagnostic coverage versus one at 60 percent can be the difference between achieving PL d and falling back to PL c. Another oversight is assuming that all versions of a standard safety component behave identically. They don't. A type 4 safe torque off module from Manufacturer A has different response time characteristics and different fault detection capabilities than an equivalent module from Manufacturer B. When you specify components in your schematic, you're committing to a specific part number, not a generic function. If you leave it vague, the procurement team will source the cheapest option, and your safety integrity calculations are now invalid.
What These Schematics Don't Solve
A safety schematic is a documentation tool, not a safety system. Drawing a perfect diagram won't compensate for poor component selection, incorrect installation, or inadequate maintenance. I've walked through facilities where the schematics were beautifully produced in CAD, laminated and hung at every station, and the actual wiring had been modified six times without any update to the drawing. The schematic was technically accurate for a machine that no longer existed. The revision control process is where most organizations fail. A safety schematic needs the same version management as any other engineering document. Change date, change description, who approved it, what previous revision it supersedes. If you're using a shared network folder and someone edits the master file without renaming it, you've just created a situation where two technicians could be working from different versions simultaneously. I recommend a dedicated document management system with mandatory check-out functionality. The cost is roughly fifteen hundred dollars per year for a small shop, and it eliminates an entire class of documentation errors.
Where to Find Reference Materials
The best starting point is your local certification body's published guidelines. VDE in Germany, UL in the United States, and SGS globally all publish application notes on safety circuit design that include example schematics at various performance levels. These are more useful than manufacturer datasheets because they show complete systems, not individual components. I keep a folder of these on my workstation and reference them whenever I'm designing a safety circuit above Category 2. For Machine Safety Manual Schematics templates, the EN 1050 standard provides the framework for what documentation should exist, though it doesn't specify drawing formats. Most German machinery manufacturers follow VDE 0113 for safety-related electrical design, which gives you a concrete reference for symbol usage and layout conventions. If you're working with North American clients, NFPA 79 and CSA Z432 are the relevant standards, though they're less prescriptive about schematic formatting than their European counterparts. I use EPLAN Electric P8 for creating these drawings. It has built-in safety circuit symbols, automatic wire numbering, and it can generate the I/O list and component list directly from the schematic. The learning curve is about two weeks of focused practice, and it pays for itself after the first three machines because it eliminates the manual cross-referencing that normally takes up most of the drafting time. If budget is tight, OpenSCADA or even a well-organized AutoCAD Electrical setup will work, but you'll spend more time on documentation tasks and less on actual safety analysis.

The Bottom Line
A safety schematic is only as good as the hazard analysis it's based on and the revision control that keeps it accurate. Get those two things right and the rest follows. Get them wrong and no amount of drawing polish will save you during an audit. I've seen competent engineers waste weeks producing elaborate schematics for machines that never got properly risk-assessed. The result was always the same — the auditor asked a single question about a specific hazard, and the entire document fell apart because it was drawn to a template rather than to the actual machine. If you're just starting out, pick one existing machine, tear apart its safety circuit in the field, and redraw it from scratch matching what you actually find. Then compare your drawing to the as-built schematic. The gaps you find between the drawing and reality will teach you more than any tutorial. I did that with my first twenty machines and it was the only reason I stopped making the same documentation errors other people keep repeating.