Router Maintenance Manuals and Replacement Parts — Where to Find Them and What Actually Works
Most people looking for a Maintenance Manual Router Setup Replacement Parts guide end up on forums because the official documentation from the machine builder either doesn't exist anymore or is locked behind a service portal you can't access without an active contract. I spent about three years dealing with this exact problem when our facility's three vertical machining centers started needing spindle replacements, servo motor swaps, and way block refurbishment without the OEM handbook handy. Here is the practical breakdown of how to get setup right and parts sourced without wasting weeks on dead ends.
Where Maintenance Manual Router Setup Replacement Parts Information Actually Lives
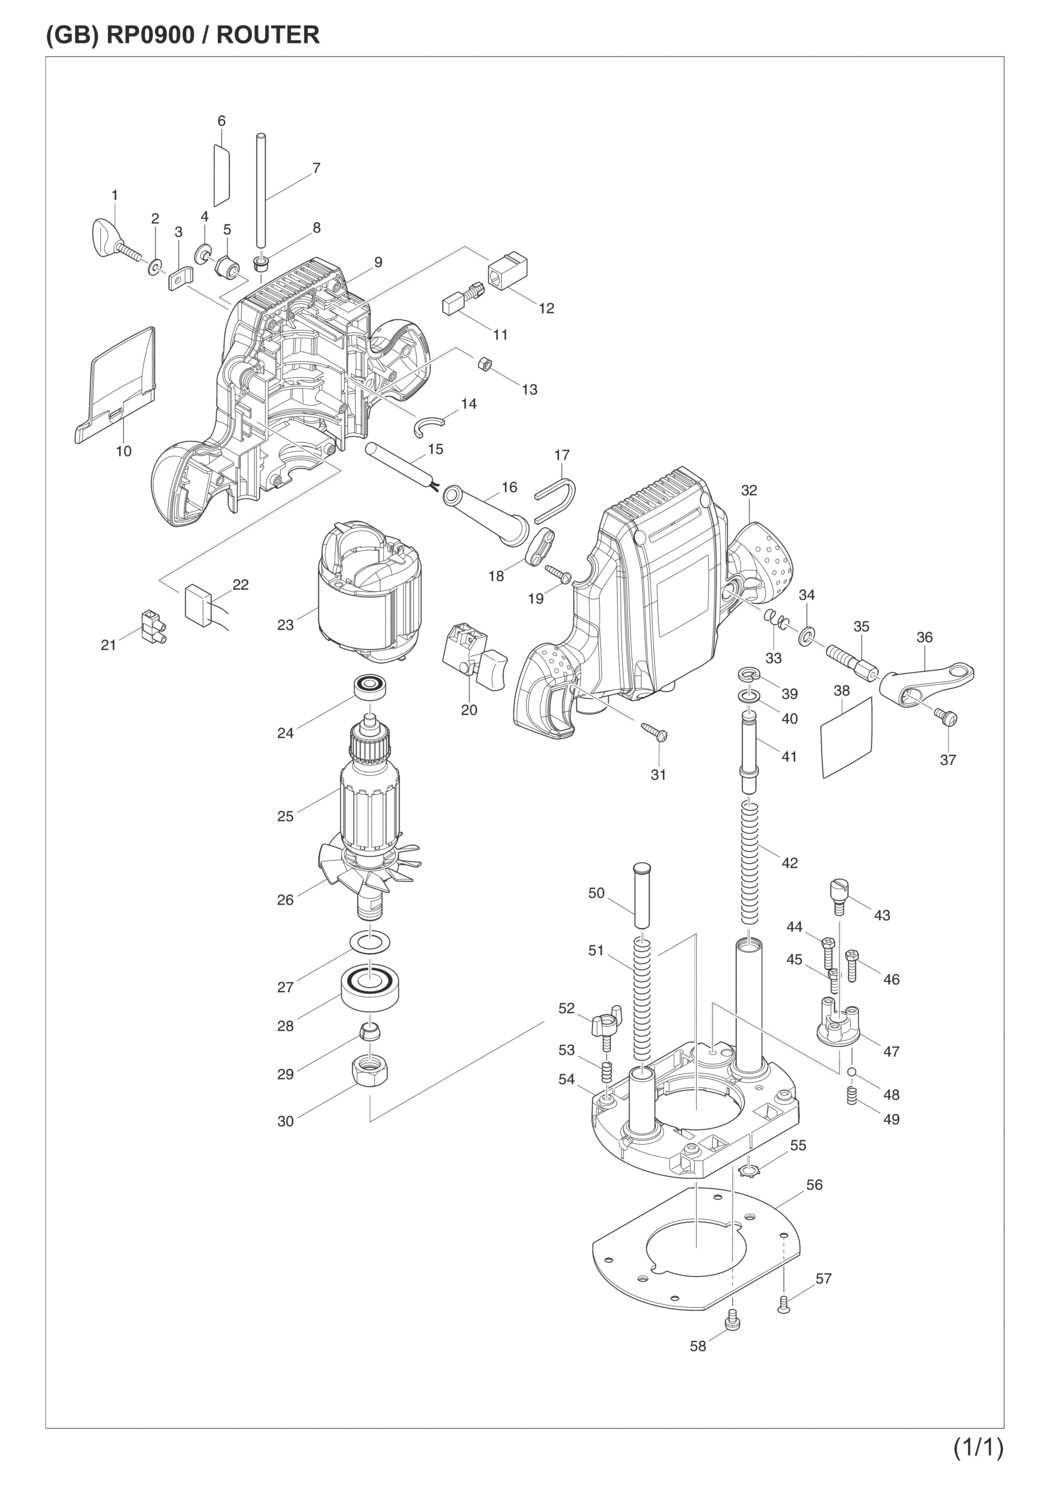
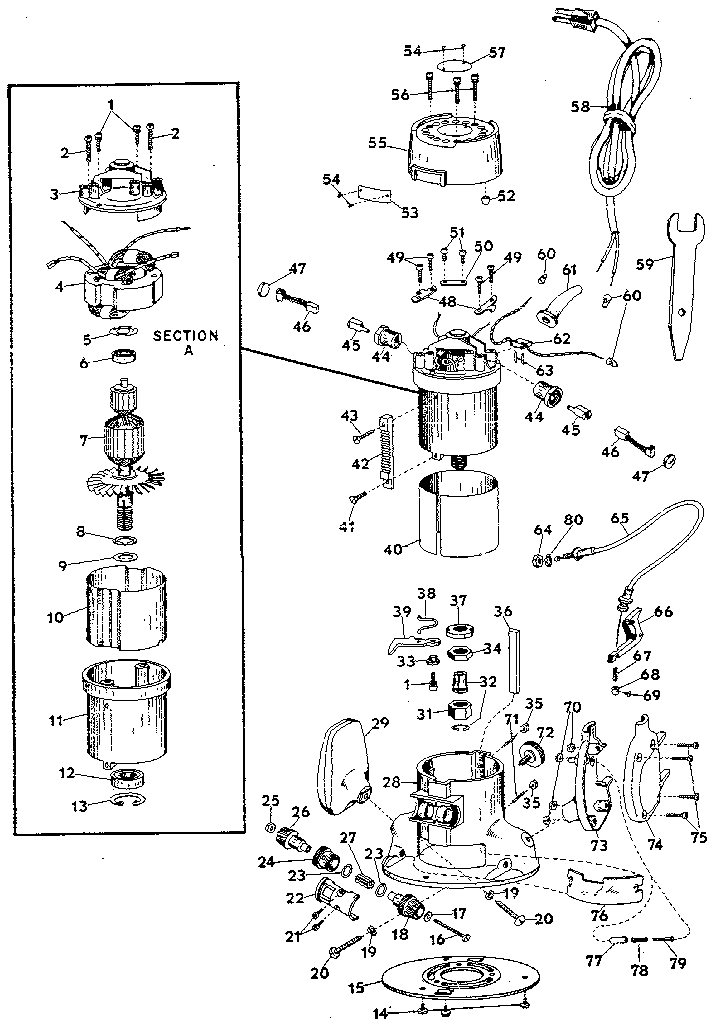
The first thing to understand is that most router and CNC machine documentation follows a hierarchy. The base layer is the general operation manual, which covers safe startup, emergency stops, and basic parameter entry. The maintenance layer covers lubrication schedules, belt tension checks, and filter replacement intervals. The deepest layer is the parts breakdown with exploded diagrams and cross-reference numbers. Most people who tell you they found a complete guide have only seen the first layer and don't realize what they're missing until a controller fault forces them into level two. I keep a folder system on our shop network organized by machine serial number, not by model name. Serial number matters because a 2018 unit and a 2021 unit with the same model designation can have completely different spindle assemblies, different servo drive revisions, and different safety interlock configurations. When we went through a controller board replacement on one of our older routers, I pulled the serial-number-specific wiring diagram and caught that the aux relay configuration had been updated in the 2020 revision. Had I used the generic parts list, I would have installed the wrong relay and spent another half day tracing why the coolant pump wouldn't engage.
How to Source Replacement Parts Without Getting Duplicated or Stopped On obsolete Hardware
When you are ordering replacement parts for a router that is three or more generations old, the part numbers in the original manual are often superseded. The manufacturer may have replaced a component with an updated version that has a different part number but the same physical envelope. Here is how I handle that without ordering the wrong thing and waiting six weeks for a return. First, photograph the existing part before you remove it. Not a quick snapshot — a clear, well-lit photo of the nameplate, any molded numbers, and the mounting configuration. Then cross-reference using the servo drive manufacturer or spindle builder's independent catalog rather than relying solely on the machine tool builder's part number. We found that one of our linear guide rail replacements was being sold as a proprietary part at a 3x markup when the underlying component was a standard THK HK series carrier that we could get for a fraction of the price by going directly to the bearing distributor. Second, always confirm the revision level. I once ordered a replacement end-cap assembly for a router spoilboard system based on the part number in the manual. The part arrived and bolted right up, but the air seal geometry was off by about two millimeters because the build had been updated mid-year and the manual hadn't caught up. The workaround was to machine a simple adapter plate from 6061 aluminum, about three millimeters thick, that compensated for the offset. It ran fine for two years until we replaced the entire assembly with the newer revised part number, which the supplier eventually started carrying after we pushed them to match their own published revisions.
Get the Full Details
What Most People Miss About Router Setup Before Running Replacement Parts
Replacing a part is straightforward. Setting the machine back up after the replacement is where things go sideways. I see this repeatedly in shop environments. A belt gets replaced, a spindle bearing gets swapped, a servo motor goes in — and nobody bothers to re-run the backlash compensation or verify the axis squareness before committing to production. When you replace a timing belt on a router axis, you need to tension it to spec, run a full homing cycle, then check the position error using a dial indicator or laser interferometer if your machine has one. The positional accuracy will drift for the first few cycles as the belt seats. Give it thirty to forty full travel cycles before you consider the axis stable. I learned this after cutting a batch of plexiglass panels and finding that the Y-axis repeat error was pushing 0.005 inches on the last three passes. The belt was just settling. Once it stabilized, the error dropped to under 0.001 inches across the full travel. Another thing that catches people off guard is the firmware or parameter correlation. Some replacement parts require a parameter change in the CNC controller to recognize the new hardware. A servo motor with a different encoder resolution, for example, will run fine mechanically but will cause the controller to report position mismatch alarms if the pulse equivalent value isn't updated. Check the controller manual section on hardware parameter tables before you power anything back up. It takes about ten minutes and saves you from spending an hour troubleshooting phantom alarms.
The Real Limitations of Maintenance Manuals and Parts Guides
I should be straightforward about where these documents fall short. Most maintenance manuals assume a certain level of technical literacy. They will tell you to check bearing preload but not how to measure it without specialized equipment. They will list lubrication intervals but not what happens when your shop runs hot or dirty, which is the majority of cases. If your environment has significant airborne particulate or temperature variation, the standard maintenance schedule underestimates wear by roughly 30 to 40 percent. I adjust our intervals accordingly — filter changes go from every 500 hours to every 300, and bearing inspections from every 1000 hours to every 600. Another limitation is that parts availability is unpredictable. Even when a part is listed as available in the manual, the lead time can swing from two weeks to twelve weeks depending on the component's supply chain. Generic components like ball screws and linear bearings tend to have better availability. Proprietary interface boards, custom spindles, and OEM-specific touch probes are the ones that stall production. I keep a small buffer stock of the top five most likely failure points for each router in our shop. Belt assemblies, limit switch sensors, lubrication pump seals, fan filters, and fuse sets. That buffer typically prevents a full machine shutdown from lasting more than a single shift. If your router is a high-usage production unit running twenty-four hours a day, the manual-based maintenance schedule won't keep up. You need to move toward condition-based monitoring — vibration analysis on the spindle bearings, thermal growth tracking on the machine frame, and power draw profiling on the servo drives. Those methods catch failures days or weeks before a manual inspection schedule would, and they require instrumentation that most standard maintenance manuals never mention.


