Setting Up Manual 3D Printer Factory Specs for Production Runs
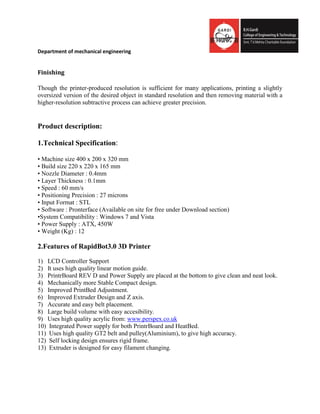
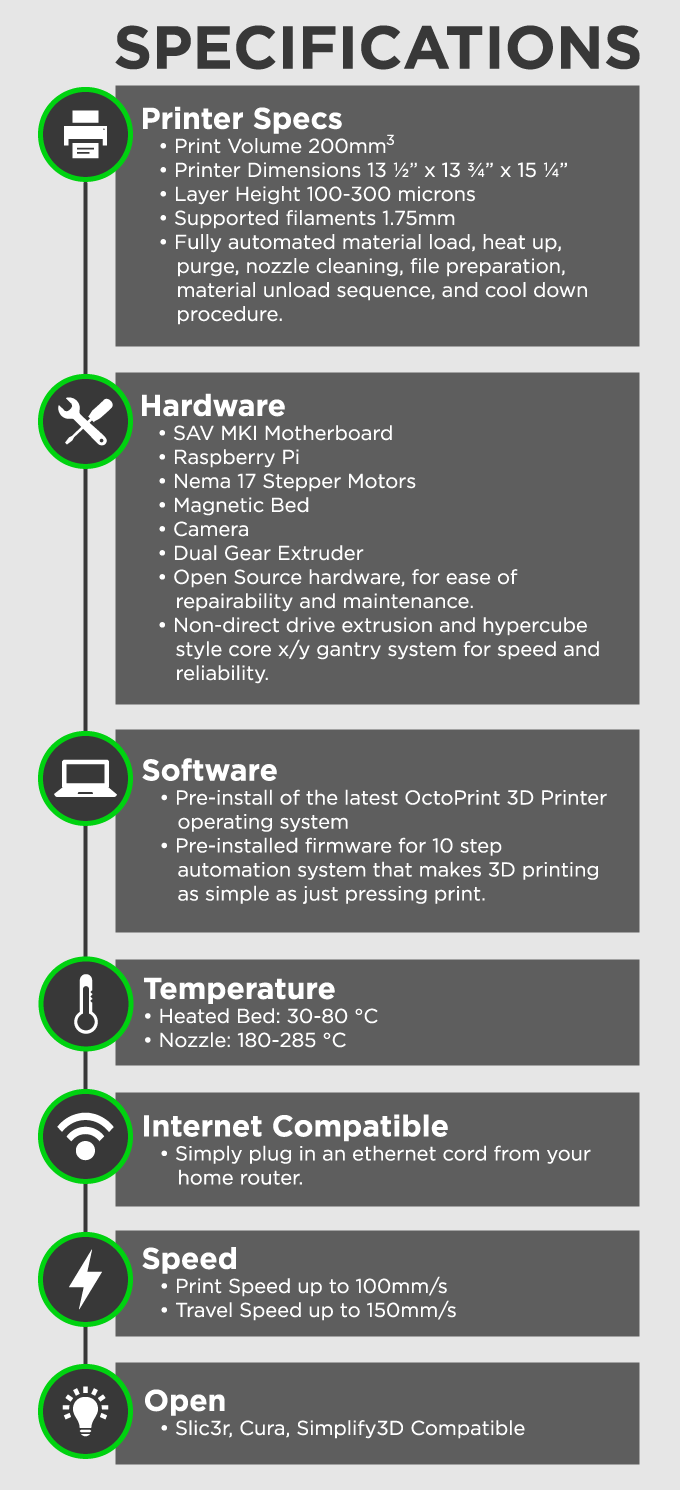
I have spent more years than I care to count wrestling with FDM printers that claim they are "factory calibrated" right out of the box. The reality is almost never what the manual says. Factory specs are basically a starting point, not an endpoint. If you want repeatability across multiple machines or consistency over a long print run, you need to understand what those specs actually mean and how to adjust them. Factory specifications typically include nozzle diameter, maximum print volume, build plate temperature range, extruder step values, and default layer height recommendations. These numbers come from the manufacturer and assume ideal conditions. They do not account for your specific filament batch, ambient temperature, or the wear pattern on your particular printer's hardware. I learned this the hard way when my first batch of production prints had consistent dimensional drift on the Z axis after about fifty hours of operation. The factory spec sheet said nothing about this because it is a wear issue, not a specification issue. The step values for your extruder are probably the most important number in that document, even though most people ignore them. If your extruder steps are off by even three percent, every dimension in your print will be wrong. You can verify this by measuring a 100mm calibration cube and comparing the actual measurement to the expected measurement. If the cube comes out 97mm, your extruder steps need adjustment. Most firmware handles this through a simple M92 command or via the printer settings menu, depending on whether you are running Marlin, Klipper, or Repetier.
Getting Your Nozzle and Temperature Right
Nozzle diameter matters more than people realize when you are working within tight tolerances. A 0.4mm nozzle does not print at exactly 0.4mm. The actual extrusion width depends on your flow rate, line height, and how much the filament compresses as it comes out. I had a situation where a client needed parts with a 0.5mm clearance and the default factory temperature settings were causing stringing that made the parts too wide. Dropping the temperature by ten degrees and increasing the retraction distance solved it without affecting layer adhesion. Bed temperature is another area where factory specs mislead. The recommended temperatures assume standard PLA and PETG. If you switch to ABS or ASA, you need to adjust both the bed temperature and the chamber temperature if your printer has one. The factory spec sheet rarely mentions chamber temperature because most consumer printers do not have one. I learned that when printing larger ABS parts, the warping was not just a bed adhesion problem but a cooling gradient problem. Placing a simple clear plastic cover around the build area raised the ambient temperature enough to stop the warping without any firmware changes.
The Layer Height Debate
Factory specs usually recommend a layer height between 0.1 and 0.3mm depending on nozzle size. The common advice is to keep layer height below 80 percent of your nozzle diameter for reliable adhesion. This is mostly correct but does not tell the whole story. I once ran a test printing the same model at 0.08mm, 0.12mm, and 0.20mm layer heights using the same nozzle and filament. The 0.08mm print took three times longer but showed a visible difference in surface quality that mattered for a presentation part. The 0.20mm print looked rough but was actually stronger in the Z direction because each layer had more material to bond with. If you are printing functional parts that will see stress, higher layer heights are often better than you expect. The vertical strength of an FDM print is always weaker than the horizontal strength because the layers bond imperfectly. Using a thicker layer reduces the number of layer interfaces and can actually improve overall strength. This is counter-intuitive for most people who equate thin layers with quality, but the relationship is not linear and depends entirely on what the part will do.
Get the Full Details

Calibrating Manual 3D Printer Factory Specs for Your Setup
The real work starts when you take those factory numbers and adjust them for your specific printer. Begin with the extruder steps calibration. Print a calibration cube, measure it with digital calipers, and calculate the correction factor. Then move to temperature tuning. Most filaments have a recommended range but the optimal temperature depends on your nozzle size and cooling setup. A 0.4mm nozzle with good part cooling might run better at 205°C for PLA while the same filament needs 215°C through a 0.6mm nozzle. Flow rate calibration is where most people give up and go back to slicing with defaults. It is worth the effort because incorrect flow rate causes visible defects that no amount of post processing fixes. Print a flow calibration test and measure the overlap between layers. You want the layers to merge smoothly without bulging or gaps. Adjust the flow percentage in your slicer until the test looks uniform. One thing factory specs never mention is filament drying. Moisture in your filament changes the effective viscosity and causes bubbling in the extrusion. This is especially problematic with PETG and Nylon. I started drying all my filament before long prints and noticed an immediate improvement in surface quality. A simple filament dryer at 45°C for four hours solves most moisture related issues. Without this step, your temperature and flow calibrations will be wrong every time the humidity changes.
Build Plate Adhesion Beyond the Basics
The factory recommendations for build plate adhesion usually suggest using PEI sheets, glass with glue stick, or build tape. These work well for standard geometries but fail on more challenging prints. I had a project where a large flat base kept delaminating during the first few layers despite perfect bed leveling and correct temperature. The issue was not adhesion but thermal contraction. The part was cooling faster than it could relax into the bed. Adding a simple enclosure around the print area and reducing the fan speed for the first ten layers solved the problem completely. Bed leveling deserves more attention than it gets. Automatic bed leveling helps but is not always accurate enough for precision work. The probe locations matter and probe drift over time is common. I check my bed leveling manually every week by placing a piece of paper between the nozzle and bed at multiple points and adjusting until the drag feels consistent. This takes about fifteen minutes and prevents hours of failed prints later. The factory spec sheet mentions bed leveling but does not explain that probe accuracy degrades with use.
When Factory Specs Fail You
There are scenarios where following factory specifications will produce poor results. High speed printing is one of them. Most factory recommendations assume moderate print speeds. If you run your printer at 150mm/s or faster, the extrusion dynamics change and you need to adjust acceleration values, jerk settings, and sometimes even temperature. I found that increasing the nozzle temperature by five degrees when printing at high speed reduced under extrusion without affecting layer adhesion. Anisotropic materials expose the limitations of standard factory settings. Printing with wood filled or metal filled filament requires different temperatures and slower speeds than standard PLA. The factory specs on these filaments are usually more accurate than the printer specs but you still need to tune based on your nozzle wear. Tungsten steel nozzles handle abrasive materials better than brass but they have different thermal characteristics. I switched to a hardened steel nozzle for carbon fiber filled filament and had to increase the printing temperature by about eight degrees to get proper flow. Multi material printing is another area where factory specs break down. Switching between filaments with different melting points requires careful temperature management. I used to get ooze and stringing when switching from PLA to TPU on a dual extruder setup. The solution was not just raising the temperature of the PLA side but also increasing the travel speed and adding a wipe tower with higher retraction. Each material combination is different and you need to test it specifically.
Documenting Your Adjustments
Keep records of every adjustment you make. Write down the temperature, flow rate, layer height, and speed settings for each filament batch. Filament properties vary between batches even from the same manufacturer. I lost two days of work once because I switched to a new spool of PETG without adjusting the drying time and temperature settings. The old settings worked for the previous spool but the new one was slightly more hygroscopic and needed a higher printing temperature. Photograph your successful prints and note the conditions. This becomes useful when you need to reproduce a part months later or troubleshoot a problem with a similar print. I have a simple spreadsheet with columns for filament type, batch number, drying time, nozzle temperature, bed temperature, flow rate, and any anomalies I noticed. It takes two minutes to fill out after each print and saves hours when something goes wrong later. Start with the factory specifications as a baseline. Do not treat them as gospel. Test each parameter, document what works, and adjust based on your specific situation. The time you spend calibrating pays for itself in reduced failures and better part quality. Most people skip this step and wonder why their prints look different from one session to the next.