Material flow in a shop floor is where most people screw up
I spent three years watching a mid-size aerospace components operation try to justify a half-million-dollar automated guided vehicle system to replace forklifts that were working fine. The problem wasn't the equipment. The problem was they designed the material handling network around the old facility layout instead of designing the layout around the actual flow patterns. They ended up with AGVs that spent more time waiting at intersections than moving product. That project got scaled back to three manual carts and a schedule board. Here's how to actually do Manufacturing Facilities Design And Material Handling without wasting capital on solutions that look good in a rendering but fail on Tuesday morning when production hits 110%.
Manufacturing Facilities Design And Material Handling fundamentals
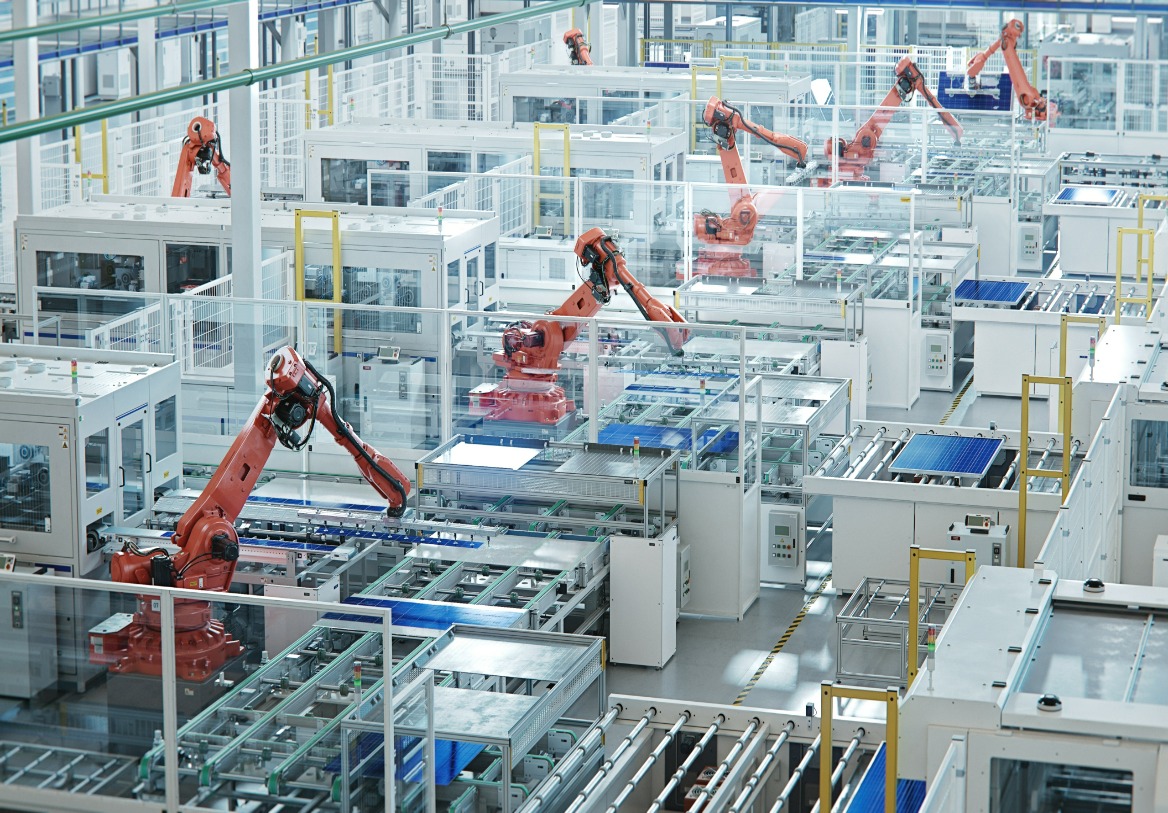
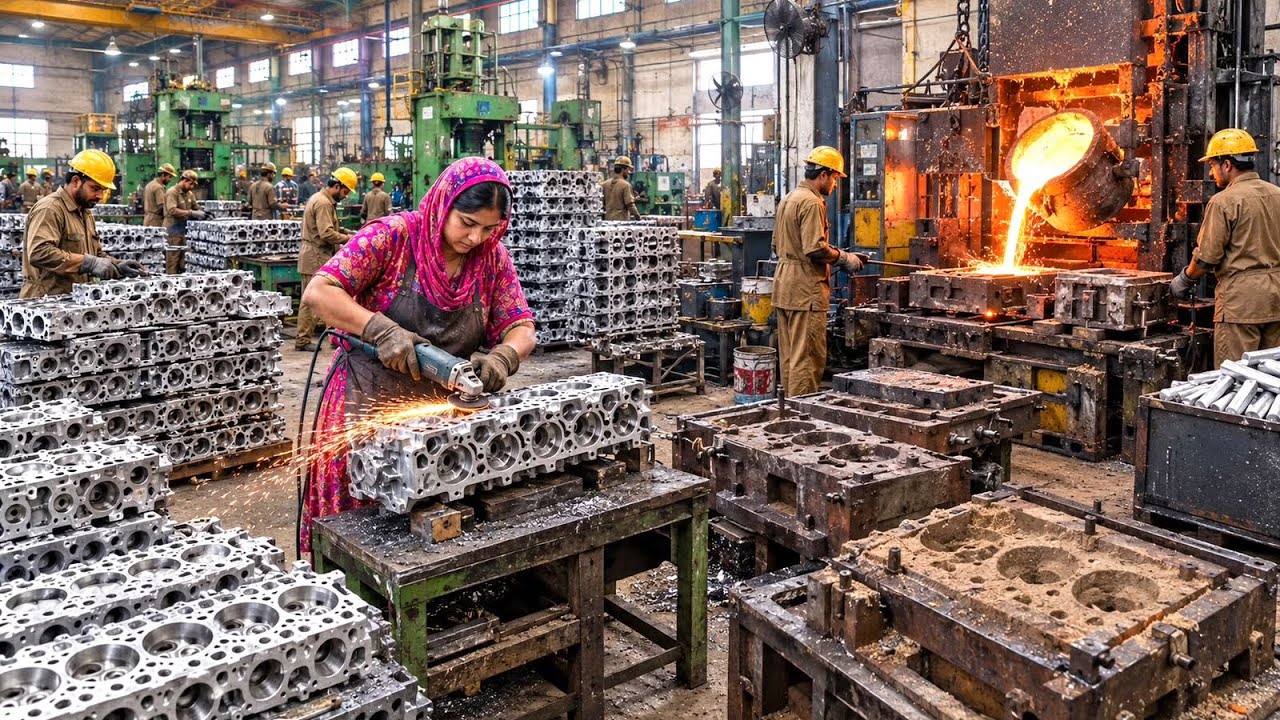
There are four basic layout types and each one creates completely different material handling requirements. Process layout groups similar equipment together - lathes in one area, mills in another. This creates maximum flexibility but terrible flow efficiency because parts travel long distances across the floor in unpredictable patterns. Product layout arranges equipment in sequence following the manufacturing path. Parts move linearly from station to station with minimal handling. This is what you see on automotive assembly lines. Cellular layout groups dissimilar processes into cells that produce complete families of parts. Each cell handles most of its own material movement internally. Fixed-position layout keeps the product stationary while resources come to it. Shipbuilding and large turbine manufacturing work this way because moving the product would be catastrophic. The material handling decisions follow directly from whichever layout type you choose. They're not separate decisions. Every conveyor placement, every forklift route, every stockroom location is a consequence of your layout choice and your volume assumptions.
Start with the data, not the equipment
Before you draw a single wall or order any conveyors, you need three datasets. First, the part routing matrix showing which operations follow which sequence across your entire product line. Second, the volume profile for each part family by week, month, and season. Third, the physical constraints - column spacing, floor load capacity, door sizes, ceiling height, and where the utilities actually are. I've seen too many facility redesigns fail because someone assumed uniform volume across all parts. Your top twenty percent of SKUs will likely represent eighty percent of material handling movements. Design your primary flow paths for those parts. The low-volume specialty items can take the secondary routes. Don't size your infrastructure for the long tail. For material handling equipment selection, the decision tree is straightforward but people ignore it. Bulk materials like steel plate and castings usually need overhead cranes or forklifts. Unit loads on pallets or in bins work well with conveyors, automated guided vehicles, or cart systems. Small parts in trays or totes typically use horizontal conveyors, roller systems, or carton flow rack. You match the handling method to the physical characteristics of what you're moving, not to what looks impressive in a vendor catalog.
Get the Full Details
Flow design rules that actually matter
The golden rule of facility material handling is minimizing the sum of distance multiplied by weight multiplied by frequency. A thousand pounds moved ten feet once per hour costs the same as ten pounds moved one hundred feet once per hour. People always optimize for distance and forget about weight and frequency. Your heaviest items should travel the shortest distance. Your most frequent movements should use the simplest handling method. Backtracking is the enemy. If your floor plan forces parts to travel past their next destination to reach it, you've made a layout mistake. Draw the material flow first. Place the walls after. I had a case where a stamping operation kept having crashes between the press feed and the deburring station because the deburr area was positioned downstream from the press exit. We moved the deburr station adjacent to the press and eliminated thirty percent of the forklift traffic. The building columns stayed where they were. We didn't rebuild anything structural. Buffer zones need specific sizing, not guesswork. A buffer between two processes should hold roughly fifteen minutes of upstream output at peak rate. Too small and you starve the downstream process during normal variations. Too large and you hide problems that should be fixed. WIP accumulation in buffers is usually a symptom, not a solution.
Common equipment choices and when they fail
Conveyor systems look efficient until you understand their failure modes. Roller conveyors handle rigid unit loads well but jam constantly with flexible packaging or irregular shapes. Belt conveyors tolerate messy loads but require regular tensioning and tracking adjustments. Chain conveyors are workhorses but create noise and vibration that affects precision machining nearby. You select based on load characteristics, not throughput numbers alone. Automated guided vehicles generate excitement in management meetings and deliver disappointing results in practice. They work well on smooth, flat floors with clear overhead clearance and predictable traffic patterns. They struggle with temperature variations that affect wheel traction, dynamic obstacles from human workers, and any floor surface degradation. Our AGV installation required resurfacing forty percent of the travel lanes within six months because the original concrete couldn't handle the point loads from the vehicle wheels during frequent stops and starts. Forklifts remain the most flexible material handling solution despite their reputation for inefficiency. They handle variable loads, navigate temporary obstacles, and adapt to layout changes without infrastructure modifications. The tradeoff is operator training, maintenance requirements, and safety infrastructure like pedestrian barriers and mirror systems. A well-managed forklift operation with dedicated aisles and pedestrian separation typically achieves ninety percent of the throughput of an automated system at thirty percent of the capital cost.
Integration points where everything breaks
The most expensive mistakes happen at transfer points between material handling systems. A conveyor feeding into a storage rack needs precise positioning, accumulation control, and usually a lift or tilt mechanism. An AGV docking with a workcell requires repeatable positioning, interface protocols, and fallback procedures when the automated handoff fails. These integration points typically account for sixty percent of material handling system downtime. Dock and yard management deserves more attention than it receives. Shipping and receiving areas create the highest concentration of material handling activity in any facility. Trailer position uncertainty, loading sequence dependencies, and yard truck congestion can eat two to four hours of productive time daily in a medium-volume operation. GPS-based yard management systems combined with appointment scheduling typically reduce trailer wait times from ninety minutes to under thirty minutes.
Lean material handling principles
The concept originates from manufacturing efficiency work but applies directly to facility design. Move materials only when needed, in the quantity needed, using the simplest method possible. Superfluous handling steps multiply costs faster than superfluous equipment purchases. A part that gets picked up three times before reaching its destination has absorbed three times the handling cost without gaining three times the value. Standardized work cell layouts with predetermined material delivery schedules eliminate the decision-making that slows down production. When operators spend time deciding where to put incoming components or how to route outgoing parts, they're not producing. Fixed location marking, standardized container sizes, and predetermined pickup schedules create the constraints that enable consistent performance. Visual management reduces material handling errors without adding technology. Floor marking for storage zones, color-coded containers for different part families, and shadow boards for handling tools create immediate visual feedback when something is out of place. The human eye catches deviations faster than any sensor system can detect them.
Capacity planning mistakes
Most facility designs assume current volume indefinitely. Material handling systems sized for today's production won't handle tomorrow's growth without modification. The correction factor is typically 1.5 to 2.0 times current peak demand for the first expansion cycle. Building in concrete pad capacity for additional conveyor supports or power distribution is dramatically cheaper than retrofitting after occupancy. Peak versus average demand creates different sizing requirements for different systems. Conveyors and automated systems need peak sizing because they can't accelerate quickly during surges. Manual handling systems like carts and forklifts can absorb peak demand through temporary labor increases. Match the sizing philosophy to the flexibility of the handling method.
Specific implementation checklist
Before finalizing any facility design for Manufacturing Facilities Design And Material Handling, verify these items. The part routing matrix is complete and validated against actual production data. The volume forecast covers five years minimum with identified growth triggers. Floor load capacity is confirmed at every proposed equipment location including point loads from heavy machinery. Ceiling height accommodates the tallest handling equipment plus maintenance clearance. Utility access points align with equipment power and compressed air requirements. Emergency egress paths maintain minimum width after equipment installation. Pedestrian walkways are separated from vehicle traffic by physical barriers, not paint markings. Fire suppression coverage extends to all storage heights including racked storage. Loading dock capacity matches the sum of simultaneous inbound and outbound trailer positions. After implementation, track these metrics monthly. Lines traveled per part per shift. Average handling time from pickup to delivery. Equipment utilization by system type. Incident rates by handling method. Buffer overflow frequency at each integration point. These measurements identify problems before they become capital projects requiring solutions. The cheapest material handling improvement is usually moving a machine three feet closer to the next operation. The most expensive is replacing an entire handling system because you sized it for the wrong demand profile. Design for the flow. The equipment follows.