How We Actually Run a Risk Assessment on the Floor
Most companies treat their manufacturing risk assessment example like a checkbox exercise. They fill out a standard FMEA template, assign a low to medium score to everything that vaguely looks dangerous, and call it a day. That approach works fine until something actually blows up. I learned this the hard way back in 2018 when we had a casting line at a mid-sized foundry in Ohio that kept failing quality checks without any clear root cause.
We ended up building a proper process hazard and operability study from scratch instead of relying on the generic risk matrix our safety team usually pushed. What I found was that the biggest risks were never the ones flagged by the standard scoring system. They were the interactions between variables that no single department owned. Temperature swings during cooling combined with operator fatigue during the night shift created a window where rejected parts slipped through inspection. Nobody was tracking both factors at the same time.
Building Your Manufacturing Risk Assessment Example
Start by mapping every step in your actual production process. Not the one on the wall chart. The one where things actually happen. Walk the floor during a full shift cycle and note where workstations, materials, and people overlap. You need to understand the real flow before you can identify where it breaks.
Then identify failure modes for each step. A failure mode is simply any way a process can go wrong. For a CNC machining line this might be tool wear exceeding tolerance, coolant concentration dropping below spec, or a fixture not seating properly. Write each one down. Do not assign severity, occurrence, or detection scores yet. Just list them.
Once you have your inventory of failure modes, bring in the people who actually run the equipment. Not the engineers. The operators. They know which machines behave strangely when the ambient humidity shifts. They know which batch of raw material from a certain supplier causes chatter marks without any other change to the process. This is where the assessment gets useful. The spreadsheet alone will never capture this.
I recommend using a modified FMEA format with an additional column for cross-process dependencies. Most standard templates have columns for potential causes and current controls. Add a column for what other processes are affected when this failure occurs. This single addition caught the casting line issue I mentioned earlier because we could see that a defect in the pouring stage was only visible three steps downstream after assembly had already started.
Scoring Without Bullshit
When you assign severity, occurrence, and detection ratings, use actual data from your facility. Not industry averages. Not textbook numbers. Pull your scrap rates from the last six months. Look at your mean time between failures from the maintenance logs. Check your inspection catch rates from quality reports. If you do not have this data, collect it first. A risk assessment built on guesses is just a waste of time.
The detection score is where most people get it wrong. They rate detection based on whether their current controls exist on paper. They should rate it based on whether those controls actually catch the failure in practice. I had a facility where they scored detection as 2 out of 10 for a visual inspection station because they had a checklist at that station. Two months later an audit revealed that the checklist was never actually filled out. The detection score should have been 8 or 9 because the failure was slipping through completely.
Common Pitfalls That Cost Money
The biggest mistake I see is treating risk assessment as a periodic event instead of a living process. You complete it once, file it in a binder, and update it only when something goes wrong. By then the assessment is already obsolete. Change orders, new suppliers, equipment modifications, and shifts in production volume all alter your risk landscape. I recommend reviewing and updating your manufacturing risk assessment example quarterly at minimum, and after any significant process change within forty-eight hours.
Another problem is isolating risk assessment from your continuous improvement program. If you identify a high severity failure mode but have no budget or timeline to address it, the assessment becomes frustration rather than a tool. Pair every high priority finding with an owner and a target completion date. If you cannot assign an owner, that means nobody cares enough to fix it, and you need to escalate it to management before something happens.
What This Method Does Not Do Well
A manufacturing risk assessment example will not predict failures that have never occurred before. It is backward looking by design. It uses historical data and process knowledge to identify likely problems. It cannot account for novel failure mechanisms from new technologies or unproven materials. When introducing something truly new, combine your assessment with a pilot run and tighter monitoring during the early production phases.
It also tends to underrate human factors. Operators make mistakes. Fatigue, distraction, and procedural drift are real. But they are hard to score numerically. I usually add a separate risk register for human error scenarios and review it monthly alongside the main FMEA. This keeps human factors from getting buried under mechanical failure modes that get more attention.
Practical Tips from the Floor
Keep your assessments portable. If they live only in a shared drive, nobody will use them during an actual problem. Print the top twenty risk items and post them at each workstation. Update them weekly. Make sure the people working the line can see what matters most right now.
When you identify a high risk item, test your controls before declaring them effective. Do not just trust the paperwork. Run a controlled trial where you simulate the failure mode and verify that your detection and mitigation controls actually work as designed. I once had a company that rated their emergency stop system as highly effective because it existed and passed inspection. During a live test, we found that the guard interlock on one station had been miswired during a recent maintenance job. The emergency stop would have done nothing. A five minute physical check caught it.
Tools and Templates
You can build your manufacturing risk assessment example in Excel if you want. It works for smaller operations with straightforward processes. For more complex environments, dedicated software like Reliasoft FMEA or AxysRisk gives you better traceability and reporting features. The software costs more but saves time on data entry and makes trend analysis easier. Both approaches are valid. Pick what fits your scale and budget.
If you want a free starting template, I have used a modified AIAG FMEA workbook adapted for discrete manufacturing. It includes the cross-process dependency column I mentioned earlier. You can find similar versions online from industry associations and engineering forums. Customize it for your process rather than using it as is. A template that does not match your actual workflow is worse than nothing because it gives a false sense of structure.
The Bottom Line
A good risk assessment in manufacturing is not about scoring every possible failure perfectly. It is about focusing your limited resources on the failures that will actually hurt your operation the most. Identify the top ten risks by risk priority number. Address those first. Then move down the list. Do not try to eliminate everything at once. You will burn out and get nothing done.
The best assessments are the ones that get used. If your team is not referencing it during daily meetings, shift handovers, and root cause analyses, it is not helping anyone. Build something practical and keep it current. That is how you avoid costly surprises.
Gallery Manufacturing Risk Assessment Example
Must-Have Manufacturing Risk Assessment Templates withSamples and Examples
Must-Have Manufacturing Risk Assessment Templates withSamples and Examples
7.1.3.1 - Manufacturing Risk Assessment | PDF | Evaluation | Economies
Manufacturing Risk Assessment Form from Frontline Data Solutions
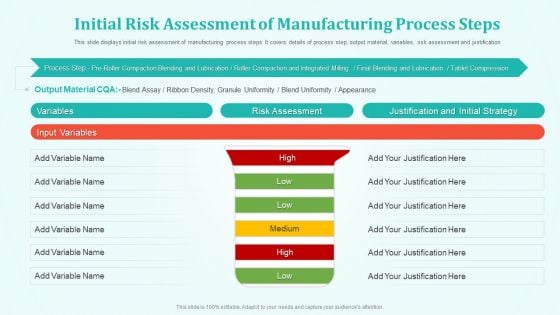
Initial Risk Assessment Of Manufacturing Process Steps Template PDF