Why Your FEA Results Look Like Garbage
The biggest mistake I see in material modeling isn't about choosing the wrong model. It's about trusting output that looks plausible when the input was fundamentally wrong. I've sat through enough project reviews where someone ran a nonlinear analysis, got reasonable-looking deformation contours, and declared victory, only to find out the stress values were off by a factor of three because they didn't account for rate-dependent behavior. Let me walk through how this actually works in practice, not the textbook version.
Material Modeling In Finite Element Analysis
At its core, material modeling is about defining how a substance responds to load. You give the solver a set of equations, and it uses them at every integration point across every element throughout the simulation. The equations are called constitutive models. Engineers have built dozens of them over the last century, and most of them are approximations of things we don't fully understand anyway. The basic categories run like this. Elastic models describe reversible deformation. Linear elasticity uses two parameters, Young's modulus and Poisson's ratio. It works fine for metals under small strains, up to maybe one or two percent elongation. Hyperelastic models handle large reversible strains, mostly for rubbers and elastomers. You feed them experimental data from tension, compression, and shear tests, and they fit parameters like the Mooney-Rivlin or Ogden coefficients. Plastic models capture permanent deformation. Von Mises with isotropic hardening is the workhorse for ductile metals. Crystal plasticity exists for when grain-level behavior actually matters, which is almost never in a standard engineering analysis. Viscoplastic and viscoelastic models add time dependence. Polymers, biological tissues, and metals at high temperature all need these. Creep models handle slow time-dependent deformation under sustained load. Damage and failure models predict when and how a material breaks. Lemaitre damage mechanics, Johnson-Cook failure, and cohesive zone models are common choices depending on what you're studying.
Here's the part most people skip. You need actual test data for whatever model you're using. I've seen engineers pull Young's modulus and yield strength from a handbook and call it good for a crash simulation. That's not how this works. A handbook value is a single point. Your material might have a lot more behavior between that point and fracture, and if your model doesn't include it, your results are just wrong with confidence. When I was working on a bracket failure investigation a few years back, the initial simulation showed no issues. The physical part had cracked after 50,000 cycles at a stress level the simulation said was well below yield. We went back and found the material supplier had switched from a cold-drawn to a hot-rolled condition without updating the documentation. The yield strength was about 15 percent lower, and the fatigue properties were completely different. The simulation wasn't wrong. The material definition was. This is the kind of thing that happens constantly. Material data sheets get copied from older designs, substitutions happen on the supply chain side without notification, and nobody catches it until physical testing fails.
Get the Full Details
Setting Up a Material Model Step by Step
Start with the physics of what you're trying to simulate. This determines everything that follows. If you're doing a static structural analysis of a steel bracket at room temperature with expected strains under two percent, linear elastic is probably sufficient. Don't add plasticity because you read it's more realistic. It's more accurate, sure, but it also adds nonlinearity, which means more iterations, more chances for convergence problems, and more time spent debugging instead of designing. Once you know the physics, pick the model class. For metals under monotonic loading, elastic-plastic with von Mises yield criterion and isotropic hardening is the default. MostFEA packages have this built in. You need the stress-strain curve. Not the engineering stress-strain curve from the test report, the true stress-strain curve. Engineering stress divides force by original area. True stress divides by the instantaneous area. They diverge once necking starts, and if you're analyzing large plastic deformation, using engineering values will give you incorrect results. Convert it yourself rather than trusting the software to do it. Some packages handle this conversion. Most don't do it well. For hyperelastic materials, you need at least three test modes. Uniaxial tension alone is not enough to calibrate an Ogden model. The fitting algorithm can find parameters that match tension data perfectly while predicting nonsense for equibiaxial or plane strain. I had a project where we used only uniaxial data for a silicone sealant model. The simulation predicted the seal would hold under compression loading. The physical prototype extruded out of place under a quarter of the expected load. Adding compression and shear test data fixed the prediction immediately.
When you enter the data into your solver, check the units. This sounds obvious and it isn't. I've seen models where the modulus was entered in MPa but the geometry was in millimeters while forces were in kilonewtons. The resulting strains were three orders of magnitude too small. The part looked nearly rigid. Set up a unit system and stick to it. Write it down in your model notes so the next person doesn't have to figure it out from the output files. Validation is the step everyone rushes. Run a simple test case before you apply the material model to your actual geometry. A uniaxial tension specimen modeled with the same elements and boundary conditions you'll use later. Compare the reaction force versus displacement output against the experimental curve. If they don't match within a few percent, your material definition is wrong or your numerical setup is introducing errors. Fix it here where it's cheap to investigate, not after you've spent six hours meshing a full assembly.
Common Pitfalls That Waste Days
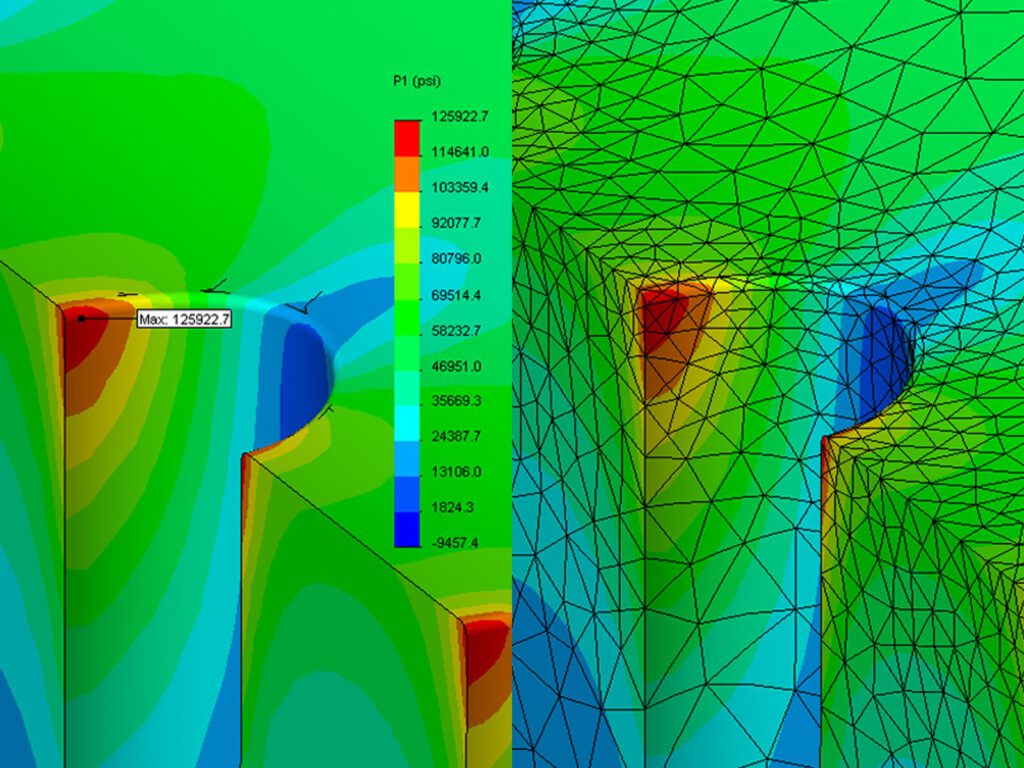
Numerical integration points are where material models actually live. Each element has a set of points where stress and strain are computed, and the results are interpolated across the element. If your mesh is too coarse, you're not resolving the strain gradient properly. Plastic zones develop at stress concentrations. In a beam with a hole under tension, the plastic zone might be three or four element widths wide. If you model it with only one or two elements across that zone, your predicted failure load will be significantly wrong. Refine the mesh locally around high-gradient regions. Don't refine the whole model. That just makes the analysis slower without necessarily making it more accurate. Convergence problems with plasticity are extremely common. The Newton-Raphson solver struggles when the material stiffness matrix changes rapidly during plastic yielding. If your analysis is bouncing between iterations without converging, check your load stepping. Automatic time stepping usually handles this, but sometimes you need to manually reduce the load increment size in regions where plasticity initiates. I once spent two days troubleshooting a convergence issue on a metal forming simulation. The problem turned out to be a single element with a severely distorted mesh at the start of the analysis. The solver was trying to compute stresses in an element that was essentially zero volume. Removing that element and remeshing the region fixed it in an hour. Regularly check your initial mesh quality before you invest time in solving. Temperature dependence is another area where models break down quietly. Most material definitions are given at room temperature. If your analysis involves any temperature variation, you need temperature-dependent properties. Young's modulus drops as temperature rises for nearly all materials. Yield strength drops faster. If you're simulating a brake rotor or an exhaust manifold and you use room-temperature properties throughout, your predictions will be non-conservative. Get the temperature-dependent data from the material supplier or from published databases. If you can't find it, you need to test it. Running a simulation with guessed temperature dependencies is worse than running one with constant properties because it gives false confidence.
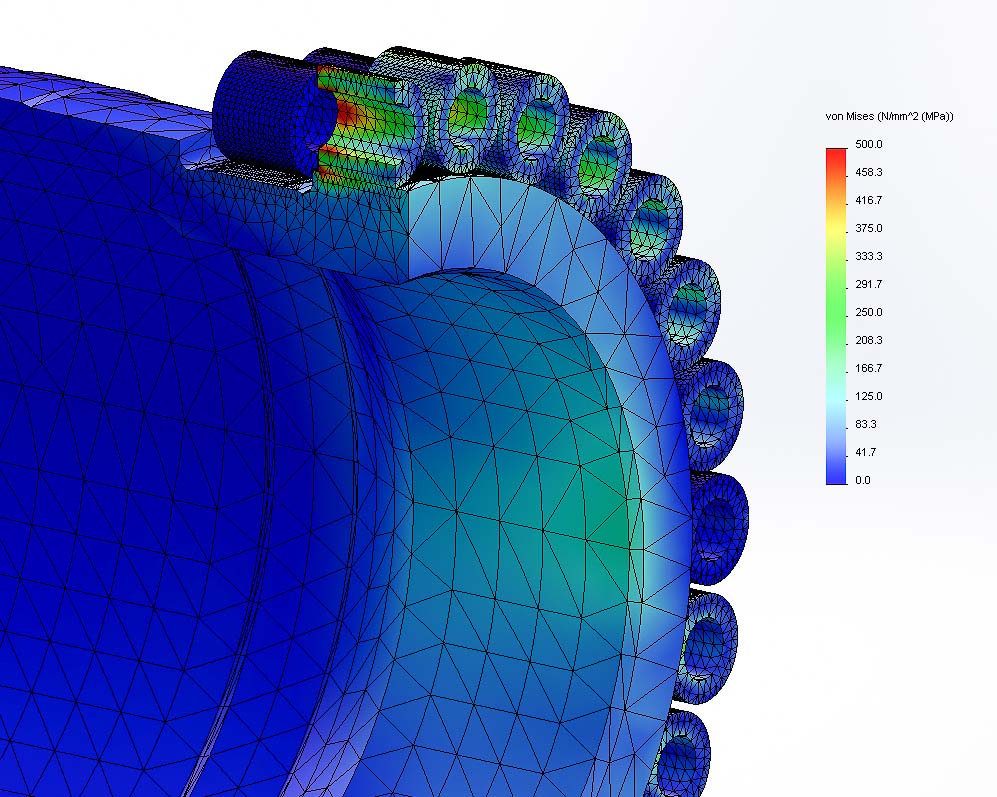
Boundary conditions interact with material models in ways that aren't always obvious. A fixed support next to a plastic material can create artificial stress concentrations that trigger premature yielding in the simulation. The physical part would distribute that load differently because of how it's actually attached. Model the connection as it exists. If a bolted joint is represented as a fixed constraint, your results near that joint are unreliable regardless of how good your material model is.
When Material Models Fail Completely
There are cases where no standard material model works well enough. Composite laminates with progressive damage require specialized formulations that most general-purpose FEA packages handle poorly out of the box. You'll need user-defined material subroutines or dedicated composite tools. Metallic foams and cellular materials have stress-strain curves with long flat plateaus that standard plasticity models don't capture without significant modification. Biological tissues exhibit nonlinear elasticity, viscoelasticity, anisotropy, and large deformation all at once. No single constitutive model covers all of that. You pick the behaviors that matter for your specific question and accept that you're ignoring the rest. Cyclic loading is another area where standard models fall short. Fatigue analysis requires either a separate fatigue module with cycle counting and S-N curves, or a cyclic plasticity model that captures hardening and softening behavior over repeated loading. Standard von Mises plasticity assumes monotonic loading. If you apply it to a cycling problem, you'll get the wrong stress-strain hysteresis loops and wrong life predictions. There's no shortcut around this. You need cyclic test data or a model specifically calibrated for cyclic behavior. Rate effects matter whenever the loading speed is high enough to cause inertial or viscous effects in the material. Automotive crashes, impact events, and ballistic problems all involve strain rates that are orders of magnitude higher than quasi-static tests. The Johnson-Cook model is widely used for this, but it requires parameters that are not always available. Using quasi-static material data for a high-rate simulation will significantly underestimate the flow stress. If your loading involves any shock or impact, make sure your material model accounts for rate dependence, or don't trust the results.
A Practical Example From My Work
I was analyzing a polymer gasket seal for a pressure vessel application. The gasket was a cross-linked nitrile rubber compressed between two flanges. The initial model used a hyperelastic Mooney-Rivlin model calibrated from uniaxial tension data provided by the gasket manufacturer. The simulation showed adequate contact pressure at the seal interface under design pressure. We ordered the parts and tested them. The gasket leaked at 60 percent of the design pressure. The problem was that the gasket experiences primarily compressive loading in service, not tension. The uniaxial tension data didn't constrain the compression behavior of the hyperelastic model. The material parameters were fitting the wrong part of the response curve. I re-calibrated the model using compression test data from the same material batch. The revised simulation predicted lower contact pressure, closer to what we measured. The discrepancy was still there, and the additional testing and recalibration took about three days, but at least the model was now pointing in the right direction. After that, we added a small margin to the initial compression load and the leaks stopped. It wasn't elegant, but it was honest about what the model could and couldn't predict. This experience changed how I approach hyperelastic material calibration. I always check what loading modes the test data covers relative to what the analysis actually applies. If they don't overlap, the model is a guess dressed up as engineering.
What to Do When You Don't Have Data
Sometimes you have to proceed without good material data. This happens more often than people admit. Start with the closest available material from a database. LS-DYNA has a materials library. Abaqus has example material definitions. These are starting points, not final answers. Run the validation test I mentioned earlier. Compare simulation output to any available physical data, even if it's from a different component made of the same material. If the comparison is wildly wrong, your material definition needs work. If it's in the ballpark, you at least know you're not off by an order of magnitude. Document every assumption. Write down where each property came from, what test it was derived from, and what the uncertainty is. Future you or whoever takes over the project will thank you. A material definition with no source information is a time bomb. It sits in the model file looking legitimate until something fails and nobody can trace back why. The bottom line is that material modeling is mostly about knowing what you don't know. Every constitutive model is an approximation. Every parameter has uncertainty. Every simulation result carries the baggage of whatever assumptions went into it. The goal isn't to eliminate that baggage. It's to understand what's in it and make sure it doesn't overwhelm your conclusions.