
Why Most People Pick the Wrong Material on Their First Try
I spent three years doing iterative redesigns because I picked 6061-T6 aluminum for a bracket that saw repeated thermal cycling between -40C and 120C. The bracket worked fine at room temperature. It lasted six weeks in the field before stress corrosion cracking showed up at the fillet radii. The problem wasn't the material's yield strength. It was the combination of residual stresses from the extrusion process and the environment. That mistake cost me about fourteen thousand dollars in shipped units and two months of lost schedule. I've made better choices since then, but only because I stopped treating material selection as a lookup exercise and started treating it as a system problem. Materials Selection In Mechanical Design isn't about finding the strongest or lightest material on a datasheet. It's about finding the material whose performance envelope contains your operating conditions with enough margin to cover manufacturing variability, environmental drift, and the things that haven't been tested yet. The Ashby method is the standard framework most engineers learn in school, but the real work happens in the gaps between the method's assumptions and the messy reality of how parts actually fail. The core process goes like this: define the functional requirements, identify the constraints, set the objective function, and then search the material property charts for candidates that satisfy all of the above. Constraints are hard limits. If your part must be electrically insulating, metals are out regardless of how good they look on a stress-strain curve. Objectives are what you're optimizing for, like minimizing mass or cost. The trade-off surfaces you get from multi-objective optimization are where most decisions actually live.
Here's what nobody tells you about the Ashby approach. It assumes materials are isotropic and homogeneous. Most aren't, especially composites and additively manufactured metals. It also assumes you can find reliable property data at your operating temperature and strain rate. Good luck getting meaningful fatigue data for Inconel 718 at 650C from a vendor database. You'll be extrapolating from room-temperature curves and calling it engineering judgment, which is another way of saying you're guessing with confidence.
How I Actually Do It Now, Not How the Textbooks Say To
The workflow I use is different from the clean academic version. I start with constraints because constraints eliminate options faster than anything else, and most junior engineers skip straight to objectives and waste three hours comparing materials that would fail on manufacturability grounds before they even get to performance. First pass, I list every constraint as a binary filter. Temperature range. Corrosion environment. Electrical requirements. Regulatory restrictions. Biocompatibility if applicable. Weldability if the part needs joining. Availability lead time if we're building prototypes next week, not next quarter. Each one is a hard no if the material doesn't pass. I write these down explicitly instead of keeping them in my head. People forget their own assumptions under time pressure and then wonder why the design failed. Second pass, I identify the objective. Usually it's mass, cost, or a combination. Sometimes it's something less obvious like thermal expansion match to an adjacent material. A few years ago I was designing a sensor mount where the primary concern wasn't stiffness or strength at all. It was coefficient of thermal expansion matching between the aluminum housing and the ceramic piezo element. Mismatched CTE caused microfractures in the bond line during thermal cycling, and the failure mode was completely invisible during static testing. The objective function there was minimizing differential strain across the interface, not maximizing specific modulus.
Get the Full Details

Third pass, I pull the property charts and do a graphical search. I plot the relevant properties against each other. Young's modulus versus density for stiffness-limited design. Yield strength versus fracture toughness when both matter. The Pareto front emerges naturally from the scatter of data points. Materials cluster into families on these charts, and the clusters are informative. Metals tend to group in the upper right of strength-density space. Polymers cluster low and left. Ceramics occupy a narrow band of high stiffness and low fracture toughness. Knowing where the clusters sit lets you skip entire categories without looking them up individually. Fourth pass, I refine with processing effects. The base alloy properties in the chart aren't the properties your part will have. Heat treatment, cold working, directional solidification, additive manufacturing build orientation, injection molding shear history, annealing cycles. These change everything. A CADP titanium bar that's been solution treated and aged has different properties than the same alloy in the as-forged condition. The difference can be thirty percent in yield strength and fifty percent in fatigue life. I always check whether the property data I'm using corresponds to the actual processing route, and if I can't verify that, I apply a derating factor of fifteen to twenty five percent as a conservative buffer.
The Edge Case That Made Me Rethink Everything
About five years ago, I was selecting material for a high-cycle vibration isolator in an automotive application. The operating environment involved exposure to brake fluid, road salts, and temperatures from -30C to 90C. The load spectrum was well characterized from dyno testing. Stiffness requirements were tight. Mass targets were aggressive. The obvious candidate was PEEK, which checks a lot of boxes on paper. PEEK has good chemical resistance, decent mechanical properties across a wide temperature range, and it's lightweight. On the property charts, it looked like a winner. I ran the analysis, selected PEEK, ran the prototypes, and the parts failed in twenty thousand cycles from fatigue cracking at the mounting bosses. The fracture surfaces showed interlamellar separation, which pointed to moisture absorption during processing weakening the polymer matrix. The datasheet values for PEEK are typically given for dry, annealed conditions. Nobody mentions that unless you ask, injection molded parts retain significant moisture and the glass transition temperature drops by roughly forty degrees Celsius when fully saturated. The effective modulus under our loading conditions was substantially lower than the handbook value, and the fatigue endurance limit shifted accordingly. The workaround was straightforward but not obvious from a properties table. I switched to a glass bead reinforced PEEK grade instead of the standard unfilled version. The reinforcement reduced moisture uptake by about sixty percent and stabilized the modulus across the humidity range. More importantly, I specified a post-mold annealing cycle at 150C for four hours followed by controlled cooling, which removed residual stresses from processing and brought the moisture content below one percent before assembly. The revised parts ran for over two million cycles without cracking. The cost per part went up by eighteen percent, but the warranty risk dropped to near zero, which mattered more than the unit price in this application.
Common Pitfalls That Keep Appearing
Engineers consistently underestimate the effect of surface finish on fatigue life. A polished specimen of 4340 steel might have an endurance limit around 450 MPa. The same alloy, shot-peened, can exceed 700 MPa. The same alloy, machined with a 32 RMS finish and then ground to 8 RMS, sits somewhere in between. The surface condition determines where crack initiation starts, and in high-cycle fatigue, initiation consumes most of the life. If your part sees more than ten thousand cycles, the surface finish specification belongs in the material selection discussion, not in the manufacturing drawing three layers downstream. Another persistent mistake is treating ultimate tensile strength as the primary design criterion for ductile materials under static loading. Yield strength is the relevant number for most mechanical designs. UTS matters for fracture scenarios and for materials that don't yield noticeably before breaking. For steel and aluminum, the ratio of UTS to yield is usually between 1.2 and 1.5. If you're designing against yielding, which you should be in ninety percent of cases, UTS is noise. Using it as a selection metric biases you toward over-designed parts or toward materials with unnecessarily high strength margins that cost more and are harder to machine. A third one that costs money is ignoring thermal conductivity when thermal management is implicit in the design. A heat sink made from a material with poor thermal conductivity will run hotter than expected even if the mechanical design is sound. I once specified an aluminum alloy for a motor mount that also served as a heat spreader. The alloy had excellent specific strength but relatively low thermal conductivity compared to other aluminum grades. The motor ran fifteen degrees Celsius hotter than the simulation predicted because the simulation assumed a generic aluminum conductivity value. The fix was switching to 6082-T6 from 6061-T6. The strength difference was negligible. The thermal conductivity difference was about thirty percent, which closed the gap completely.
When the Charts Don't Help
Material selection charts break down in several scenarios that every designer encounters eventually. They don't capture processing-dependent property variation well. They rarely include long-term aging data or creep behavior at elevated temperature. They don't reflect batch-to-batch variability from different suppliers. And they absolutely do not account for the interaction between multiple failure modes acting simultaneously. When you're working outside the charts, the practical approach is to narrow to two or three candidates through the constraint filtering process, then commit to physical testing early rather than waiting until the design review stage. Prototyping in the actual material, not a substitute, costs a fraction of what redesign does. A quick tensile test and a fatigue coupon run take one to two weeks and can prevent a month-long investigation later. I always budget testing time into the project schedule from the start, not as an afterthought. If you need actual property data for a specific material system, the most reliable sources are the material producer's technical data sheets for the exact grade and condition you plan to use, supplemented by peer-reviewed literature for edge cases. Vendor selection guides are useful for screening but often omit the conditions where performance degrades. My rule of thumb is to never select a material without at least one primary source that specifies the testing conditions, sample orientation, and heat treatment state. If the data sheet doesn't say, I assume it doesn't apply to my design.
Practical Steps for Materials Selection In Mechanical Design
Here's the sequence I follow, in order, for a typical component design project: Define the function and load case with actual numbers, not estimates. Write down the maximum expected load, the load cycle count, the temperature range, the environment, and any regulatory or interface constraints. If you can't write it down, you haven't thought it through yet. Apply constraint filters sequentially and track what remains after each one. Temperature first, then environment, then electrical, then manufacturability, then availability. Each filter eliminates a chunk of the candidate pool. By the third filter, you should have fewer than ten materials left for most common applications.
Build the objective function around what actually matters. For a cantilever beam, maximize stiffness-to-weight. For a pressure vessel, maximize pressure capacity per unit mass. For a bearing surface, maximize wear resistance within the constraints of compatibility with the mating material. Don't optimize for something that isn't the governing requirement. Check processing effects on the shortlisted materials. Apply derating factors for the actual manufacturing route. If you're casting,forging, machining, or additive manufacturing, the properties shift. Factor that in before final selection. Prototype and test in the actual material at the actual processing condition. Verify that the assumptions hold. This step catches the discrepancies between chart data and reality, and it's cheaper to do now than after production tooling is built.
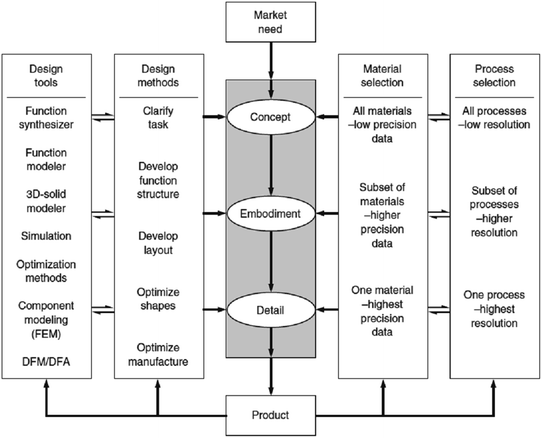
The whole process takes about forty-five minutes to two hours for a straightforward part, depending on how well the requirements are defined upfront. Most of the time variation comes from unclear constraints, not from the material search itself. If you're spending more than half a day on material selection for a single component, the problem is usually that the functional requirements haven't been pinned down clearly enough.
What I'd Tell My Earlier Self
The biggest thing I learned is that material selection is an iterative conversation between the design and the manufacturing process, not a one-time lookup. The first material you pick is almost never the final one, and that's normal. The value is in having a systematic process that catches the failure modes before they become field failures. The secondary value is in knowing which assumptions to challenge hardest, especially around processing effects, environmental interaction, and long-term property stability. Those are where the real surprises live.


