Why Your Time Studies Keep Looking Like Garbage
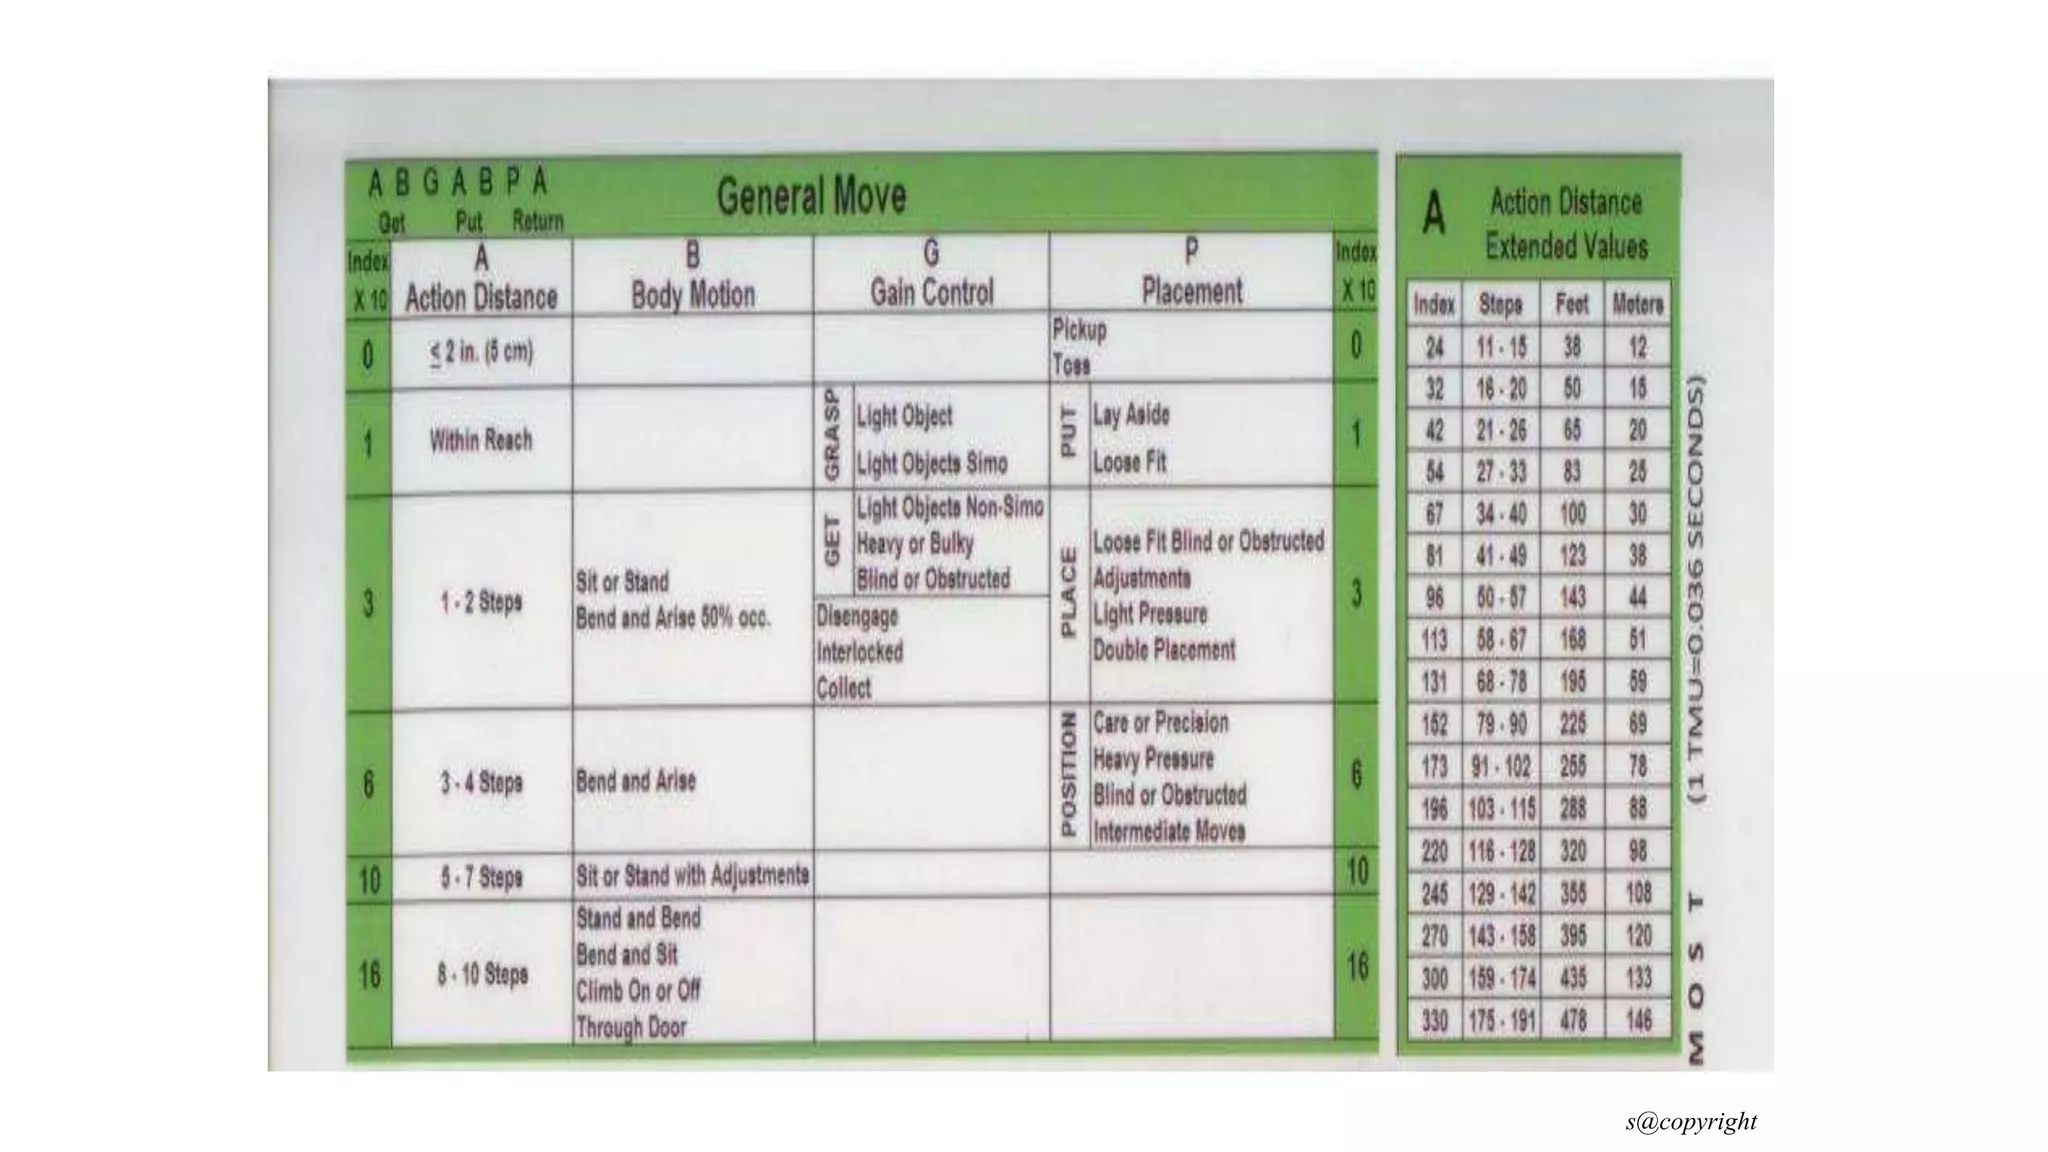
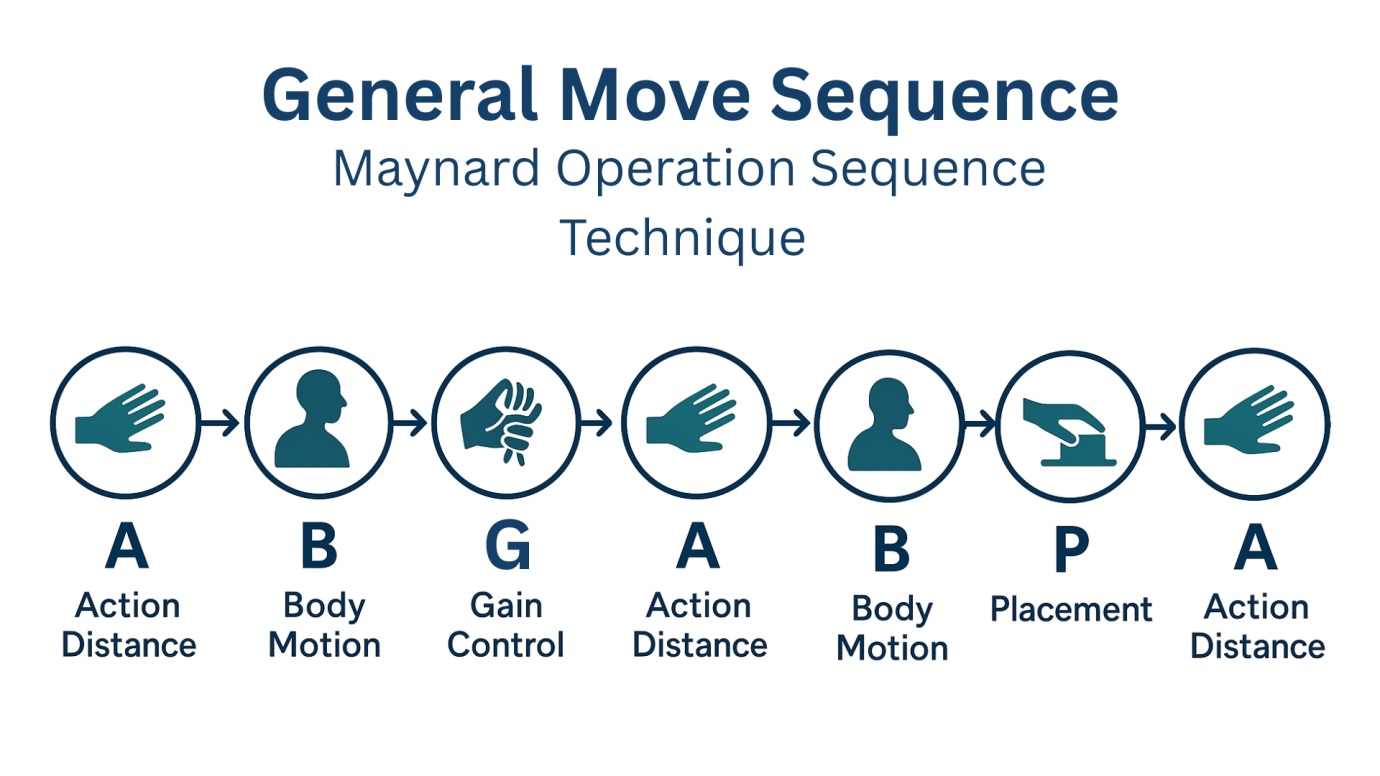
I spent about four years doing method study at a mid-sized automotive parts plant, and the single biggest source of bad data wasn't the stopwatch or the observer. It was people trying to use MOS (Maynard Operation Sequence Technique) the same way they used Basic MTM without understanding what actually changed in the methodology. The difference matters more than most training courses admit. Mos is fundamentally different from MTM-1 in how it handles the cognitive component of work. MTM-Reach or Move or Grasp are purely physical, or so the original designers claimed. Mos adds reach, position, and release as distinct categories, but here is the part nobody tells you upfront: position is where the technique either saves your study or ruins it. If you can't decide whether a movement is a position or a release-plus-reach, your times will be wrong by enough to make the whole study useless.
Getting Started with the Maynard Operation Sequence Technique
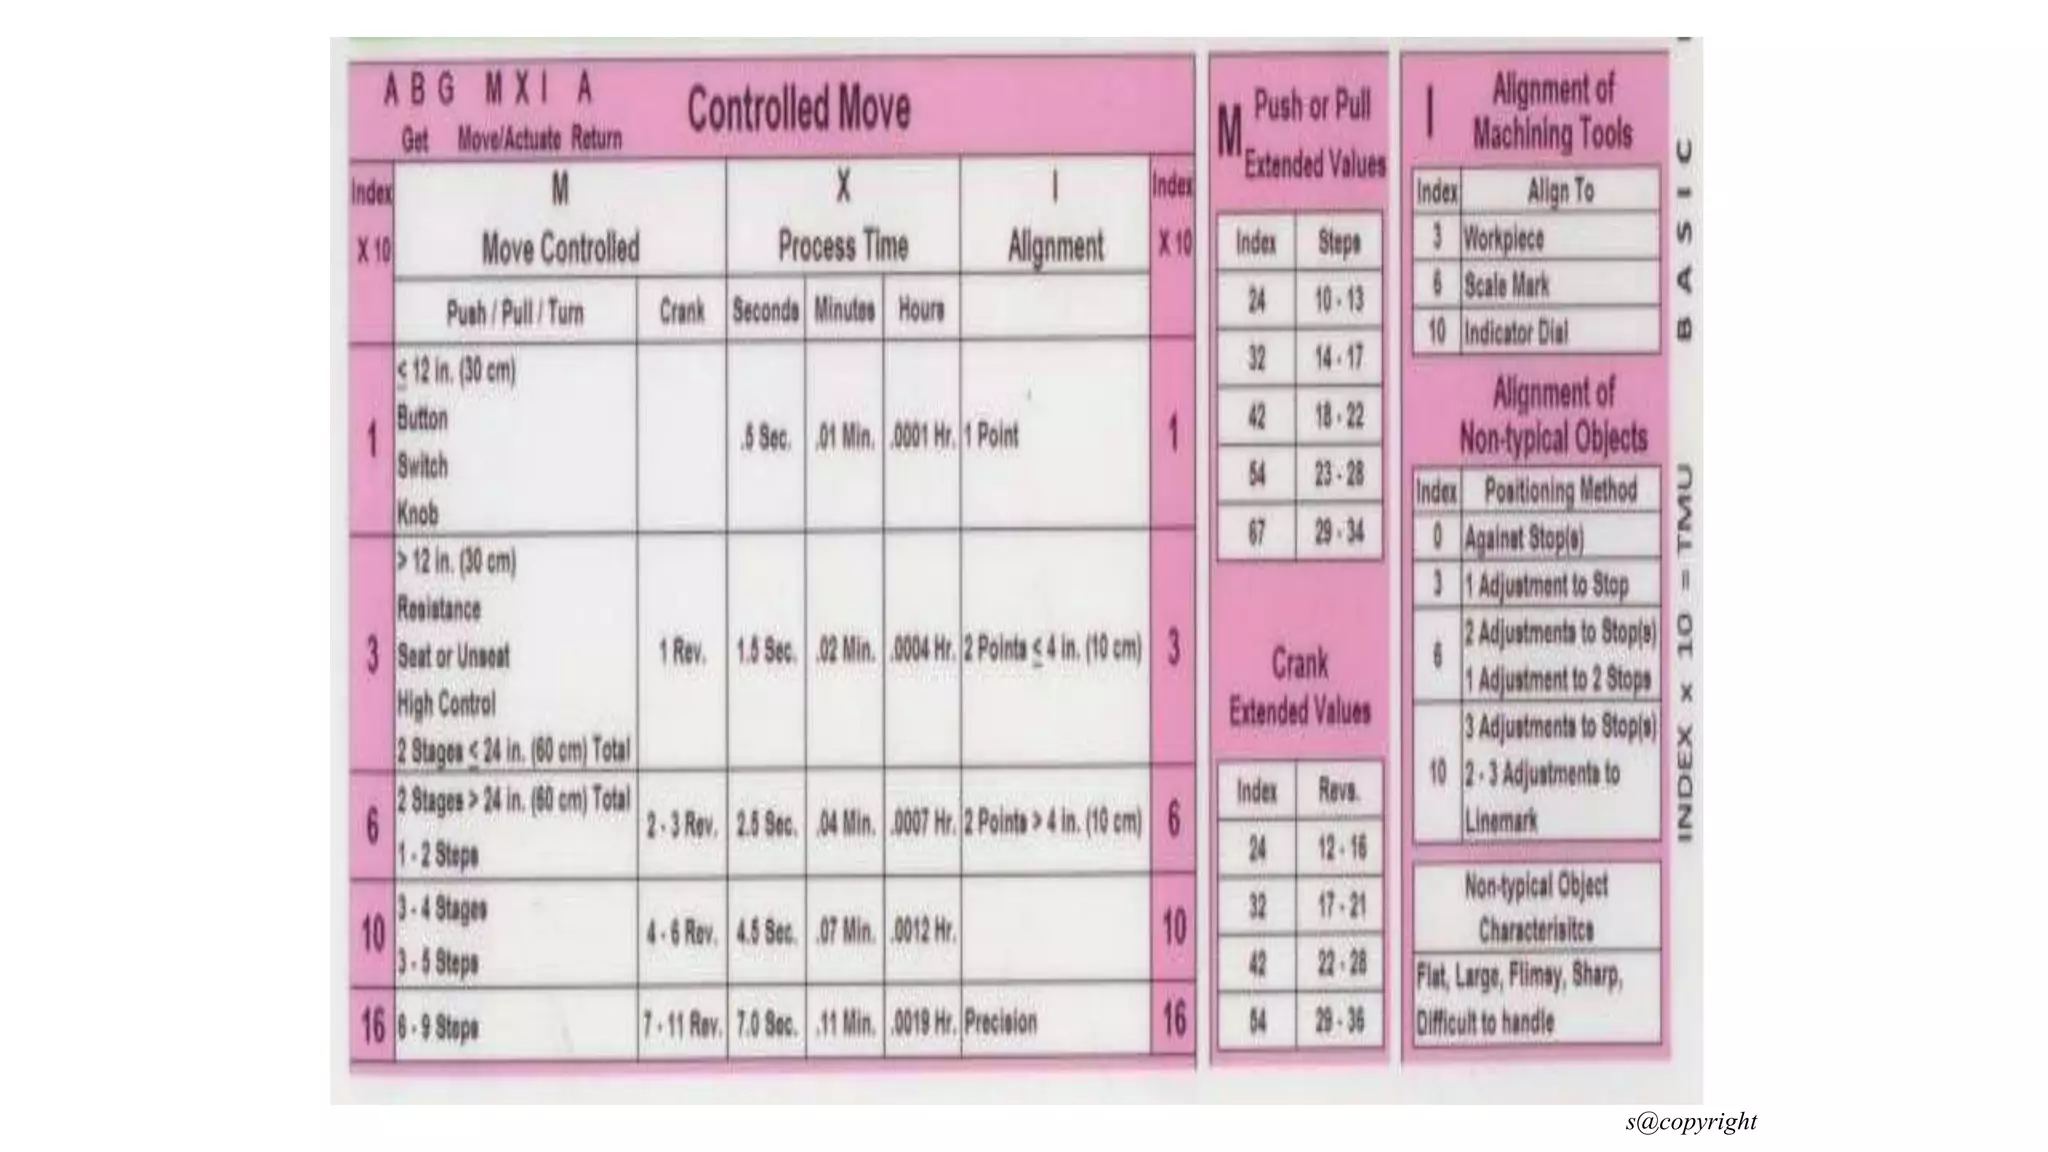
You need three things before you open the manual. A clean workstation that looks like actual production, not a demonstration rig. A stopwatch or an electronic timer that records to at least one decimal place. And a worksheet that matches the actual motion breakdown you are going to do. I used Avery Dennison's published MOS worksheets for years and they work fine if you print them at full size. The smaller versions compress the columns and make it easy to misread your own handwriting under time pressure. Here is how the actual process goes. You observe the operator do the task once at full speed without writing anything down. Just watch. This is not optional because skipping it leads people to impose a motion structure on the job that does not match reality, and then they spend twenty minutes filling out a worksheet for a task that was nothing like what they observed. After the walkthrough, you go back and break the task into its component motions. Each motion gets classified under one of the ten basic operations in Mos: get, place, hold, release, move, mental act, reach, grasp, position, and pre-position. The TMU values come from the published tables. A typical reach for a short distance is around 3.5 TMU. A position can range from 7 to over 20 TMU depending on accuracy required. Mental act is usually 4.5 TMU for a simple yes-or-no decision. Move carrying a part is generally faster than an empty reach because the operator has already located the object. These numbers are not exact predictions for any specific person on any specific day. They are normal level time values for a qualified worker operating at standard pace. Always qualify your final times with a performance rating factor if you notice the operator is consistently above or below normal speed. That is still standard practice even though the original Mos literature sometimes implies it is baked into the tables.
Where People Actually Get Stuck
The position classification is the most common source of error, and I ran into a specific case that took me three weeks to resolve properly. We were studying an assembly station where operators took a small O-ring from a tray and seated it on a metal pin on a subassembly. The first pass of the study came back with position times that made no sense when I applied them to the cycle. The O-ring was soft and deformable, and the operator was stretching it slightly with their fingers while placing it over the pin. I had initially classified this as a single position operation at the higher accuracy band. The problem was that the stretch-and-seat motion actually contains two distinct sub-motions: the initial placement onto the pin tip, which is a light position, and the final seating push, which is effectively a separate position at a tighter tolerance. When I split it that way and timed each separately, the total came out lower than my original single classification. This was counterintuitive at first, but it makes sense because the heavy position value assumes a single controlled movement to a precise final location, whereas breaking it into two lighter motions captures the actual rhythm of the task. The published tables do not cover this edge case explicitly, so you end up using judgment. That is the honest answer. Another thing that trips people up is the distinction between pre-position and reach. Pre-position means the hand is already in the path of the next motion before the current motion completes. In practice, this shows up as an overlapping motion, and Mos treats it differently than a sequential reach. I see beginners code every hand return as a reach when the operator was clearly setting up the next movement simultaneously. The difference can be five to eight TMU per cycle, which compounds fast over a multi-minute task.
Get the Full Details

Pre-positioning also shows up in two-handed operations where one hand is reaching while the other is holding or positioning. You have to watch for the overlap. If you miss it, you double-count the time for the second hand's motion. That is a very common error in MOS studies of dual-hand assembly work.
Practical Workflow for a Real Study
Start by securing the workstation exactly as the operator uses it. If there are tool holders, part bins, or fixtures that are moved around during the shift, note their positions. A bin that is two inches farther than normal adds reach time that will make your baseline look inconsistent from day to day. I once did a study where the part tray was on a pull-out shelf instead of the standard fixed position because the previous operator had modified the station layout without updating the work instruction. The reach times were 30 percent higher than the Mos table value for that distance, and it took me two additional visits to figure out why before I caught the shelf modification. Break the task into logical sub-assemblies if it is long. A full assembly cycle with twenty separate motions is manageable, but if you try to code an entire machine tending routine as one block, you will miss and the study becomes unreliable. I typically stop at the sub-assembly level and build up from there. It gives you better granularity for improvement suggestions later. Record your classifications in real time while watching the operator repeat the cycle at least three to five times. The first two cycles are just to calibrate your eye. After that, the pattern should be stable. If it is not stable, the task itself may need standardization before you even attempt a Mos study. A variable process produces variable times, and no amount of motion classification will fix that.
Once you have your classifications, calculate the total TMU by summing the standard values. Convert TMU to minutes by dividing by 1,000, then multiply by your performance rating factor if needed. A typical short assembly task that involves reaching, grasping, positioning, and releasing runs somewhere between 30 and 90 TMU, which is roughly 18 to 54 seconds of normal time. Your actual observed time might be longer or shorter depending on the operator, but the Mos standard gives you a benchmark that is independent of who is sitting at the station.

When Mos Is the Wrong Tool
Mos is not a universal solution. It works best for repetitive manual assembly tasks with clear discrete motions. It breaks down for highly variable processes where the operator makes frequent unplanned decisions, for tasks involving continuous flow like pouring or welding where motions cannot be cleanly segmented, and for cognitive-heavy work where the bottleneck is information processing rather than physical manipulation. I have seen people try to apply Mos to software documentation workflows and quality inspection routines where the operator is reading labels and making judgment calls. The results are meaningless because the time driver is the complexity of the decision, not the reach or position. If your task involves significant walking, lifting heavy objects, or working at height, consider using a different systems approach. Mos was designed for bench-level manual work with small parts. It is not built for material handling or ergonomics-heavy tasks. Using it outside that scope will give you false precision, which is worse than having no data at all. The biggest practical limitation is that Mos requires a trained observer. You cannot delegate this to a new employee after a brief orientation and expect accurate results. The classification decisions, especially around position versus release and pre-position versus reach, require experience. I typically spend a full week training someone before they can produce a study I am willing to submit. The training is not difficult, but it is substantial. Skip it and you will get numbers that look professional but are systematically wrong.
For a reference copy of the Mos tables and the official worksheet format, the original Maynard Publications materials are still available through industrial engineering suppliers. The most commonly cited version is Mos Method X, which is the updated iteration. You can also find the standard tables in most time measurement textbooks, though the exact formatting varies between publishers. The underlying values are consistent regardless of where you source them.