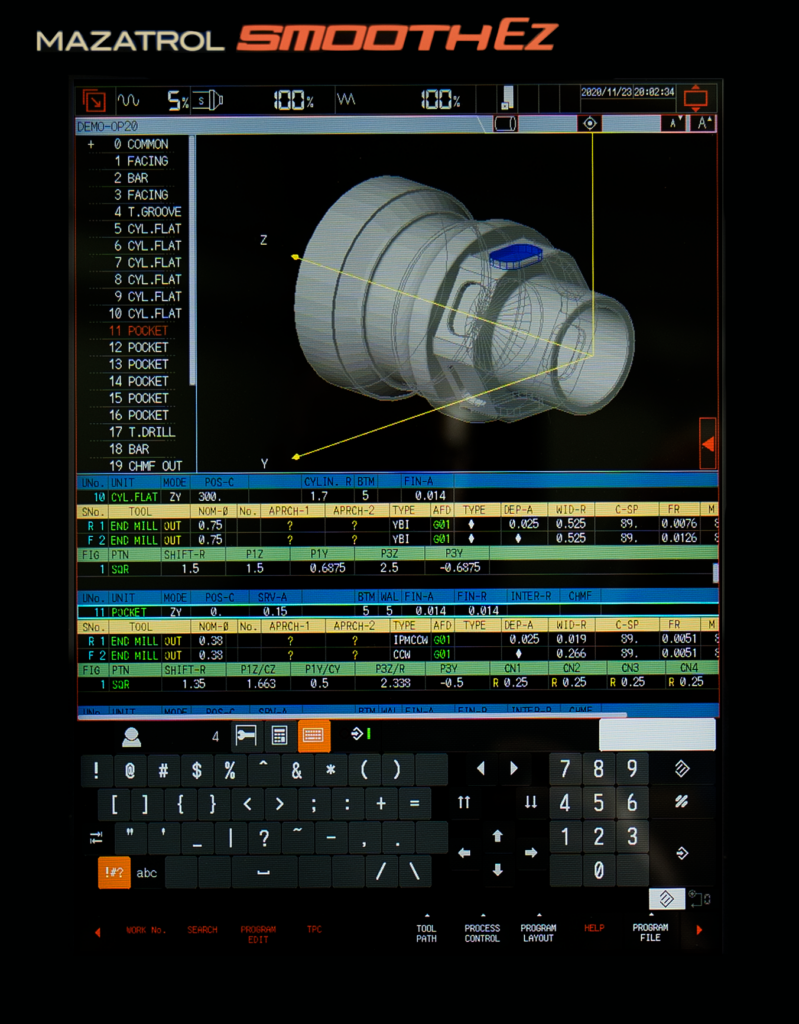
Troubleshooting the Mazak Smooth Control
I spent three years on the floor working with Mazak VSC-II systems before I ever touched a manual. The thing about the Mazak Smooth Control Manual is that it won't save you when your part is off .0005 and the inspector is standing behind you. It'll tell you what the alarm codes mean in dry textbook language, but the real help comes from knowing which pages actually get referenced and which ones just collect dust. The Mazak Smooth Control manual covers the VSC-II series primarily, sometimes bleeding over into later Smooth versions depending on your machine's birth year. You'll find parameter tables, alarm histories, maintenance intervals, and servo tuning references all in one volume. The parameter pages are where most people waste time reading instead of working, because the actual troubleshooting flow is buried under thirty pages of generic system documentation.
Where to Get a Mazak Smooth Control Manual
Actual physical copies run somewhere between eight hundred and two thousand dollars new from Mazak directly, though you might find used ones on eBay for less than five hundred if you're willing to gamble on edition accuracy. Mazak's website has a parts manual lookup tool where you can enter your serial number and download individual chapter PDFs for free. The service manual section requires an authorized dealer login, so if you're flying solo like most of us, you're working with what you can extract from the operator side of things. I found my first real Mazak Smooth Control manual was a water-damaged paperback from 2004 that someone left in the break room. It had notes in the margins from whoever serviced that machine before me, which turned out to be worth more than the printed pages. The parameter modifications for tool changer indexing, for example, were scribbled in blue ballpoint next to the official diagram with a crossed-out value and a replacement number. That's the kind of knowledge never makes it into the published documentation.
What Actually Works When You Need It
The parameter settings for your specific machine configuration live in the PMS parameter page, which requires a key switch position that most shops keep locked to prevent random edits. Accessing it means turning the key to parameter mode, pressing the system key, navigating to the PMS page, and entering a password that varies by region and model year. The passwords aren't particularly secure, but the point is that Mazak built this system assuming someone who knows what they're doing would be making changes. When I was debugging a Y-axis servo alarm on a Quick Turn 350, the manual listed fifteen possible causes ranging from encoder feedback loss to thermal drift in the servo amplifier. The actual fix involved checking the ground connection on connector CN2 at the motor, which had worked loose during a previous maintenance cycle. Nobody mentions this in the printed documentation because it's considered an installation issue rather than a control system fault. The alarm history function stores the last three hundred events with timestamps, which is genuinely useful for tracking intermittent problems. However, clearing the history requires a menu sequence that isn't intuitive, and some operators accidentally wipe weeks of diagnostic data when trying to silence a persistent alarm. I learned this the hard way when a recurring spindle overload condition disappeared from the log right before I could document the pattern.
Get the Full Details

The Hidden Problems Nobody Discusses
The Smooth Control system works well for basic turning and milling operations, but it struggles with certain multi-tasking sequences that cross between axes without explicit synchronization commands. I've seen parts come out of tolerance when operators tried to optimize cycle times by overlapping operations that the control wasn't designed to handle simultaneously. The manual suggests parameter adjustments, but those tweaks often introduce new problems elsewhere in the system. Thermal compensation is supposed to handle temperature variations, but in practice it requires a warm-up cycle that most shops skip during quick changeovers. I measured part size drift of up to two ten-thousandths on a cold morning before the system reached stable operating temperature, which the manual claims should be less than one ten-thousandth under normal conditions. The discrepancy comes from the compensation tables being calibrated for ideal shop environments, not real-world production floors with variable HVAC and machinery heat output. The tool magazine indexing system uses absolute positioning with incremental verification, which should prevent indexing errors. However, I encountered a problem where tool changes would hang intermittently when using hybrid tool holders from different manufacturers. The manual recommends checking the tool pocket depths and holder heights, but the actual solution involved adjusting the indexing override parameter from the default setting of one hundred to ninety-five percent for problematic tool combinations.
When the Manual Doesn't Help
The Mazak Smooth Control Manual assumes you have basic servo theory knowledge and can interpret ladder logic diagrams when troubleshooting. If you're coming from Fanuc or Siemens backgrounds, the parameter numbering and screen layouts feel arbitrary until you spend enough time with the system to recognize the patterns. I wasted a full shift once trying to locate a specific alarm code because I was searching the wrong section, assuming Mazak organized their documentation the same way as other manufacturers. The CNC program editor has macro functions that allow conditional logic and arithmetic operations, but the syntax differs from standard ISO programming in ways that aren't well documented. I wrote a subroutine that should have calculated tool wear compensation automatically, but the control rejected it because the variable naming convention didn't match Mazak's internal standards. The manual shows basic macro examples, but advanced usage requires studying actual machine programs to understand the conventions. Network connectivity through the Ethernet port works for DNC operation and remote monitoring, but configuring the TCP/IP settings requires access to the system parameters that aren't available without proper authorization. I spent several hours troubleshooting why my laptop couldn't communicate with the control only to discover that the IP address subnet was mismatched with the machine's network configuration. The manual mentions networking capabilities, but doesn't provide the detailed configuration steps needed for actual implementation.
What I Wish I Knew Earlier
The maintenance schedules in the manual are conservative estimates based on ideal operating conditions, but actual service intervals depend heavily on your material types, cutting parameters, and shop environment. I followed the recommended twenty-five hundred hour oil change schedule religiously until I switched from aluminum to hardened steel production, at which point the lubrication system showed signs of contamination well before the scheduled interval. Cutting the maintenance cycle from twenty-five hundred hours to fifteen hundred hours saved me from a major bearing failure that would have taken three days to repair. The backup battery specification calls for specific voltage and capacity ratings, but I found that using higher capacity batteries from third-party suppliers caused charging circuit issues after six months. The manual warns against using non-OEM batteries, but doesn't explain the electrical characteristics that make certain alternatives problematic. Switching back to the recommended Panasonic CR2032 cells resolved the issue, even though the aftermarket options cost half as much per unit. The tool presetting interface accepts data from various aftermarket systems, but the protocol conversion requires parameter adjustments that vary by controller revision. I connected a new tool setting station to my machine only to discover that the data format wasn't compatible with the existing parameter settings. The manual lists supported protocols, but doesn't provide the detailed configuration examples needed for actual integration with third-party equipment.

The Reality of Working with These Machines
Most Mazak Smooth Control problems trace back to simple maintenance oversights rather than complex control system failures. I've diagnosed dozens of mysterious alarms that turned out to be loose wiring, contaminated sensors, or expired backup batteries. The manual provides elaborate troubleshooting trees for each alarm code, but experienced technicians learn to check the obvious first before diving into parameter analysis and component testing. The learning curve for advanced features like adaptive control and tool breakage detection is steeper than the documentation suggests, requiring both system knowledge and practical experience with the specific application. I attempted to implement automated tool monitoring on a production line only to discover that the signal processing thresholds needed constant adjustment based on material variations and cutting conditions. The manual describes the functionality, but doesn't address the ongoing maintenance required for reliable operation in real-world conditions. The Mazak Smooth Control Manual serves as a reference rather than a comprehensive training guide, expecting users to supplement it with hands-on experience and manufacturer support resources. I found the most valuable learning came from studying actual machine programs, observing how experienced programmers structured their code, and understanding the practical constraints that shape real production solutions rather than theoretical ideals.