What actually happens when you run a gauge study
Most people treat Measurement System Analysis Msa like a checkbox exercise. They buy the software, throw data in, and hope the %GRR comes back under ten percent. It doesn't work that way. The numbers only mean something if the people running the gauges and the parts they're measuring are actually behaving the way the method assumes they will. I spent three years in automotive quality before moving to medical devices. The MSA framework is similar across industries but the consequences of getting it wrong scale differently. In automotive you might get a loud meeting. In medical devices, you get a regulatory finding that stops a production line for six weeks. Either way, the math is the same.
Getting started with a typical attribute gauge study
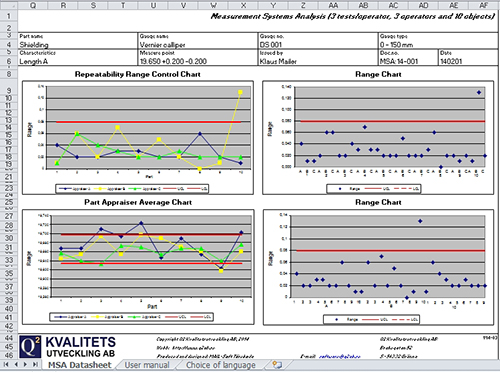
Start with the pieces of equipment you actually use on the floor, not the calibrated masters sitting in a climate controlled room. I once ran a gauge R&R on a digital caliper that read beautifully in the lab and then deviated by nearly double the tolerance when a mechanic in a cold warehouse used it at seven in the morning. The parts were from three different material lots, the operators had varying levels of training, and the ambient temperature swung twelve degrees between shifts. That single study caught a bias problem that would have blown past any X-bar chart. Here is what the basic process looks like when you are dealing with variable data: Pick your parts. Ten to twenty samples is standard. They need to cover the full expected production range, including the specification limits. If your spec is five millimeters plus or minus zero point five, your parts should span from four point six to five point four, not cluster around the nominal. Random selection matters less than range coverage. A biased sample set gives you a false sense of security.
Pick your operators. Two is acceptable for a quick check. Three is the minimum for anything you plan to defend. Five or six operators introduces repeatability issues that make the variance calculations much messier. More hands does not automatically equal better data. Each operator measures each part twice, preferably in random order. Some shops run three repetitions. That adds time and often increases fatigue error more than it improves statistical power. Two measurements per operator is usually enough if the parts are stable and the gauge is functioning correctly. The analysis then breaks down into repeatability and reproducibility. Repeatability is the variation when the same operator measures the same part multiple times. Reproducibility is the variation between different operators measuring the same part. Combined, they give you the total gauge variation relative to the process variation or the tolerance, depending on which calculation path you follow.
Get the Full Details

The result is usually expressed as a percentage. Under ten percent is acceptable. Between ten and thirty percent needs engineering review and likely some action plan. Over thirty percent means the gauge system is not fit for purpose and you should not be making production decisions based on those measurements.
Where people consistently mess this up
The first mistake is treating the %GRR threshold like a hard rule. Ten percent is a guideline from the AIAG manual, not a scientific law. In high volume processes with very tight tolerances, you might need the gauge variation to be under five percent of the tolerance. In low volume or research settings, twenty percent might be tolerable. The context determines the acceptability. The second mistake is ignoring the number of distinct categories. This is the NDFC value, and it tells you how many non-overlapping data categories the gauge can resolve within the process variation. If your NDFC is less than five, your gauge cannot reliably distinguish between good and bad parts in your actual production mix. A %GRR under ten percent with an NDFC of two is essentially useless. The gauge might look fine on paper but it cannot separate the signal from the noise. I ran into this exact situation with a hardness tester on a heat treatment line. The %GRR came back at eight point two percent, which should have been a green light. The NDFC was three. When we looked at the actual production data over two weeks, the gauge could not tell us whether a batch was drifting toward the upper spec limit. It would read a part as fine, then read it again and suggest it was borderline. We ended up scrapping product that was perfectly acceptable because the measurement system was creating false variability. Switching to a different transducer type and reducing the contact force fixed it. Cost roughly two hundred dollars and eliminated an entire category of scrap.
Attribute data is a different animal entirely
When you are dealing with pass fail gauges, go/no-go plugs, or visual inspection stations, the variable MSA approach does not apply. You need a different method. The standard here is a Kappa analysis or a reference standard comparison against a known judge. The process involves selecting parts that are clearly within spec, clearly out of spec, and several that sit near the decision boundary. Each operator classifies every part multiple times against a known reference. The agreement rates between operators and between operators and the reference are then calculated. The tricky part is that near-boundary parts are where the real problems hide. A gauge that shows ninety percent agreement overall might drop to sixty percent in the critical zone. That ninety percent number is misleading. Break down the agreement by region. If your process naturally produces parts clustered near a limit, you need near-limit agreement, not overall agreement.

I worked with a coating thickness inspection station that used a visual colorimetric method. The overall Kappa was acceptable, but the operators consistently missed under-thickness parts by ten to fifteen percent. The over-thickness parts were flagged correctly almost every time. The asymmetry in the error pattern meant we were shipping borderline parts with no one noticing. Adding a backup electronic measurement at the critical frequency point solved it without replacing the entire inspection process.
Downsides and when MSA breaks down completely
Measurement System Analysis Msa assumes that the measurement process is stable during the study period. If your environment is changing, your operators are rotating, or your parts are degrading between measurements, the variance components become unreliable. There is no statistical correction for an unstable measurement process. You have to stabilize it first and then repeat the study. The method also assumes that the parts selected for the study represent the actual production distribution. If your production has shifted significantly since you ran the MSA, the old results do not apply. Some shops run MSA once a year and treat it as perpetual documentation. That is a compliance strategy, not a quality strategy. The gauge system degrades. Operators change. Process capability shifts. The study needs to reflect current conditions. Another limitation is that MSA does not account for measurement bias drift over time. A gauge can pass a static study and then slowly drift over months. Control charts on the gauge readings themselves, monitored weekly or monthly, catch this. MSA gives you a snapshot. Process control charts give you a movie. You need both.
For dynamic measurements where the quantity being measured changes during the measurement event, traditional MSA methods are inadequate. Think of a process where part temperature affects dimension and the part is cooling while you measure it. The measurement system variation includes the process variation in this case. Separating them requires a completely different experimental design, typically involving a dedicated process control study alongside the gauge study.
Practical steps that save time and avoid rework
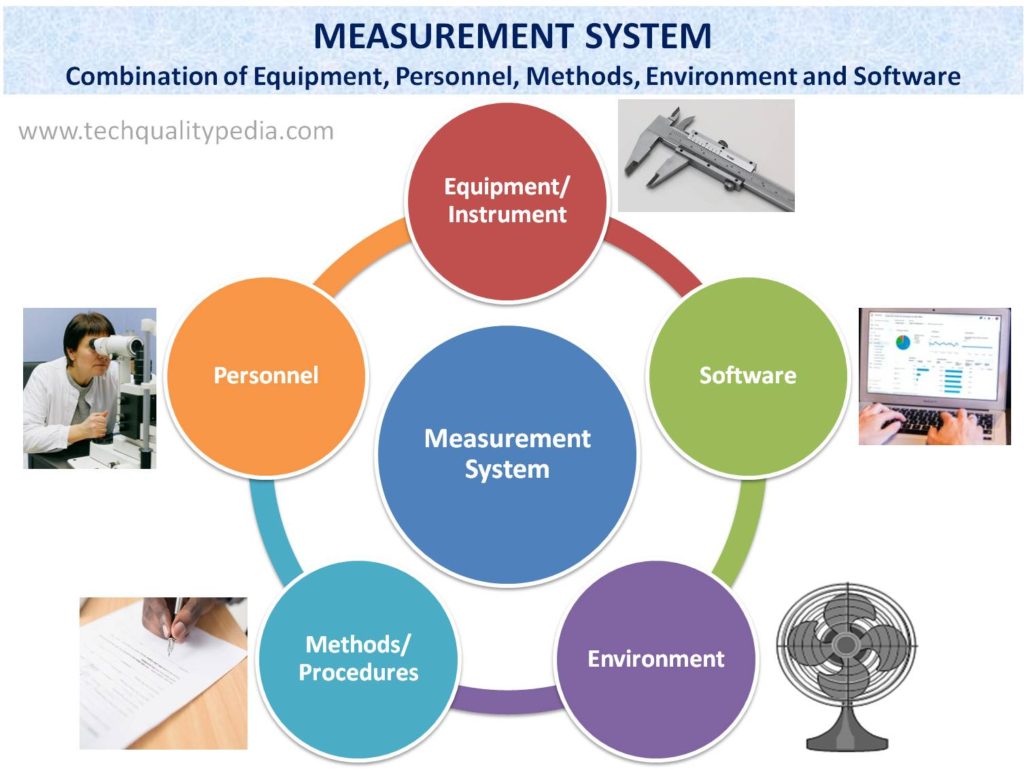
Run the gauge study in the actual measurement environment, not a lab. Temperature, lighting, vibration, and operator posture all affect results. Data collected in ideal conditions will not predict field performance. Include at least three parts near each specification limit in your sample set. The center of the distribution is easy to measure accurately. The edges are where gauge fitness actually matters. Most studies put too many parts in the middle and then wonder why the gauge fails when production drifts. Calculate both the %GRR relative to tolerance and the %GRR relative to process variation. The tolerance-based number is what auditors want to see. The process-based number tells you whether the gauge can actually detect process shifts. Both matter for different reasons.
Track the NDFC alongside every study. If it drops below five, do not accept the study as pass. Upgrade the gauge, improve the method, or narrow the study to a smaller relevant range. Do not ignore it because the percentage looks good. For attribute systems, always report the agreement rates broken down by part region. Overall agreement is a summary statistic that hides the failure modes. Region-specific agreement is what lets you fix the actual problem. The biggest thing I learned after doing dozens of these studies is that the measurement system is almost never the only problem. Usually it is a combination of operator technique, environmental factors, and gauge capability interacting in ways that a single number cannot capture. The analysis gives you direction, not a verdict. Use it to find the bottleneck, then fix the bottleneck, then retest. That loop is the whole point of doing the study in the first place.