Why I Stopped Memorizing Metric Conversions
I spent about three years in tooling design before I accepted the fact that I was going to make mistakes if I kept doing mental math. The moment I realized I'd once quoted a bearing seat diameter in inches to a supplier who only works in millimeters, costing the team two weeks of rework on a fixture plate, I stopped trying to carry everything in my head. That mistake taught me what nobody tells you about metric work: the system is supposed to be simple, but the moment you start mixing measurement systems on the same drawing, the simplicity vanishes and you're left with a spreadsheet full of rounding errors and blame. The thing that catches people is not that the metric system itself is hard. It is that modern engineering documents routinely contain both metric and imperial values in the same paragraph, and your brain does not naturally separate them the way a conversion table does. I learned this the hard way when a junior engineer on my team used a 25.4 mm pitch for a component that was actually specified as 1 inch pitch, and the part fitted perfectly during assembly until thermal expansion revealed the mismatch at operating temperature. The fix took three days and a new habit: every time I picked up a drawing, I ran the critical dimensions through a table before any comment went into the system.
Metric System Conversion Table
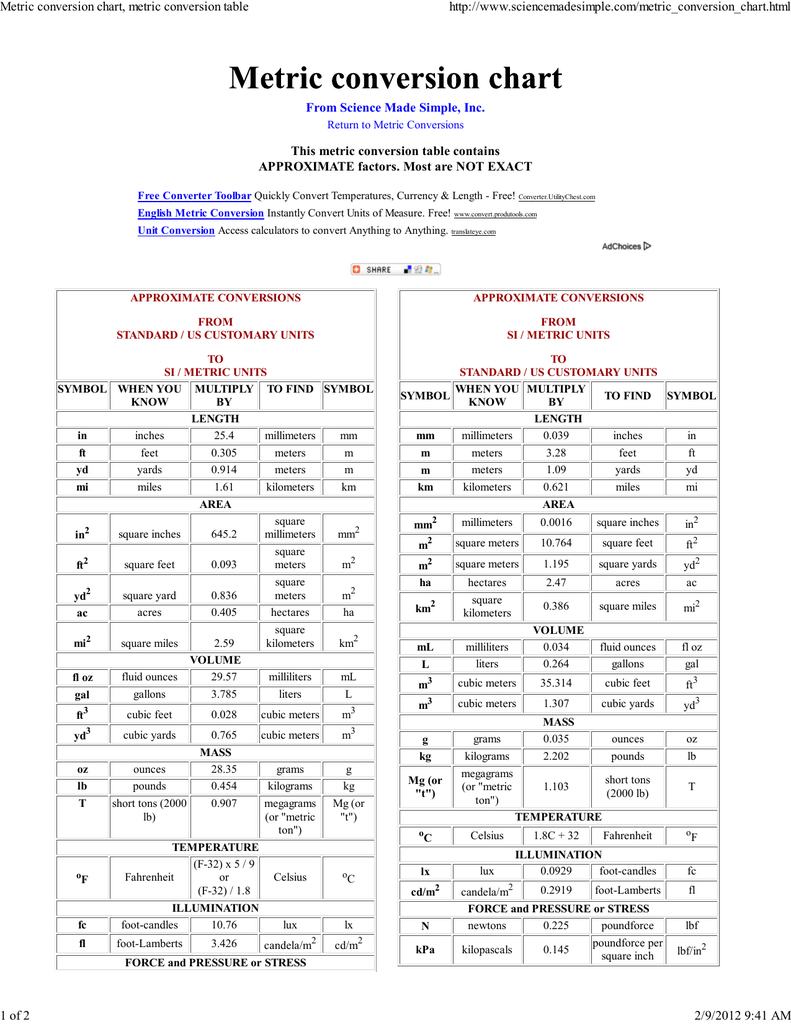
Below is the table I built and still use, though I update it whenever I run into a unit I had never needed before. It covers the conversions that actually matter on the shop floor and in the office. Most online calculators include everything from furlongs to microns, which is annoying because nobody needs furlongs and nobody wants to scroll past twenty useless rows to find the one conversion they are looking for. This table is small enough to print and tape to the wall. Length 1 inch = 25.4 millimeters exactly. This is not an approximation, it is the definition, so there is no rounding debate. 1 foot = 304.8 millimeters. 1 meter = 39.3701 inches. 1 centimeter = 10 millimeters. 1 kilometer = 0.621371 miles. 1 micron = 0.001 millimeters. 1 mil = 0.0254 millimeters. If you are working in PCB fabrication, the mil to micron conversion comes up constantly and most shops prefer microns now, but old documentation still uses mils.
Area 1 square inch = 645.16 square millimeters. 1 square foot = 929.03 square centimeters. 1 hectare = 2.47105 acres. 1 square meter = 10.7639 square feet. These come up mainly when you are calculating material yield or coating coverage, and the rounding here matters more than in length because area compounds the error. Volume
Get the Full Details

1 liter = 0.264172 US gallons. 1 US gallon = 3.78541 liters. 1 cubic meter = 264.172 US gallons. 1 milliliter = 0.0610237 cubic inches. 1 US fluid ounce = 29.5735 milliliters. 1 imperial gallon = 4.54609 liters. The imperial gallon confusion has cost me at least two orders of coolant before, so I always check which gallon the drawing specifies. Mass and Weight 1 pound = 0.453592 kilograms. 1 kilogram = 2.20462 pounds. 1 ounce = 28.3495 grams. 1 tonne = 2204.62 pounds. 1 carat = 0.2 grams. These seem obvious but the ounce to gram boundary is where people slip when they switch between avoirdupois and troy systems in jewelry or precious metals work. I stopped trusting my gut on this one after a supplier sent 150 troy ounces when we ordered 150 avoirdupois, and the difference was just enough to throw off a gold alloy batch.
Temperature Fahrenheit to Celsius: subtract 32, multiply by 5, divide by 9. Celsius to Fahrenheit: multiply by 9, divide by 5, add 32. 0°C = 32°F. 100°C = 212°F. 37°C = 98.6°F. 200°C 392°F. 400°F 204.4°C. Temperature conversions are the only ones on this page where the formula matters more than memorization because the offset breaks any simple ratio you might try to use in your head. Force and Pressure
1 pound-force = 4.44822 newtons. 1 kilonewton = 224.809 pounds-force. 1 psi = 6.89476 kilopascals. 1 bar = 14.5038 psi. 1 atmosphere = 101.325 kilopascals. 1 torr = 133.322 pascals. These show up in hydraulic and pneumatic work, and the bar to psi conversion is the one I look up most often because European component datasheets use bar and American fittings use psi, and they do not always label which one they mean. Torque 1 pound-foot = 1.35582 newton-meters. 1 newton-meter = 0.737562 pound-feet. 1 pound-inch = 0.112985 newton-meters. Torque conversions are deceptively dangerous because a 10% rounding error in bolt preload can lead to joint failure under vibration, and I once missed this on a gearbox cover because I multiplied by 1.35 instead of 1.35582. The difference sounds small but at 45 newton-meters it amounts to about 2 newton-meters of error, which is enough to strip a thread in aluminum.
How I Actually Use the Table
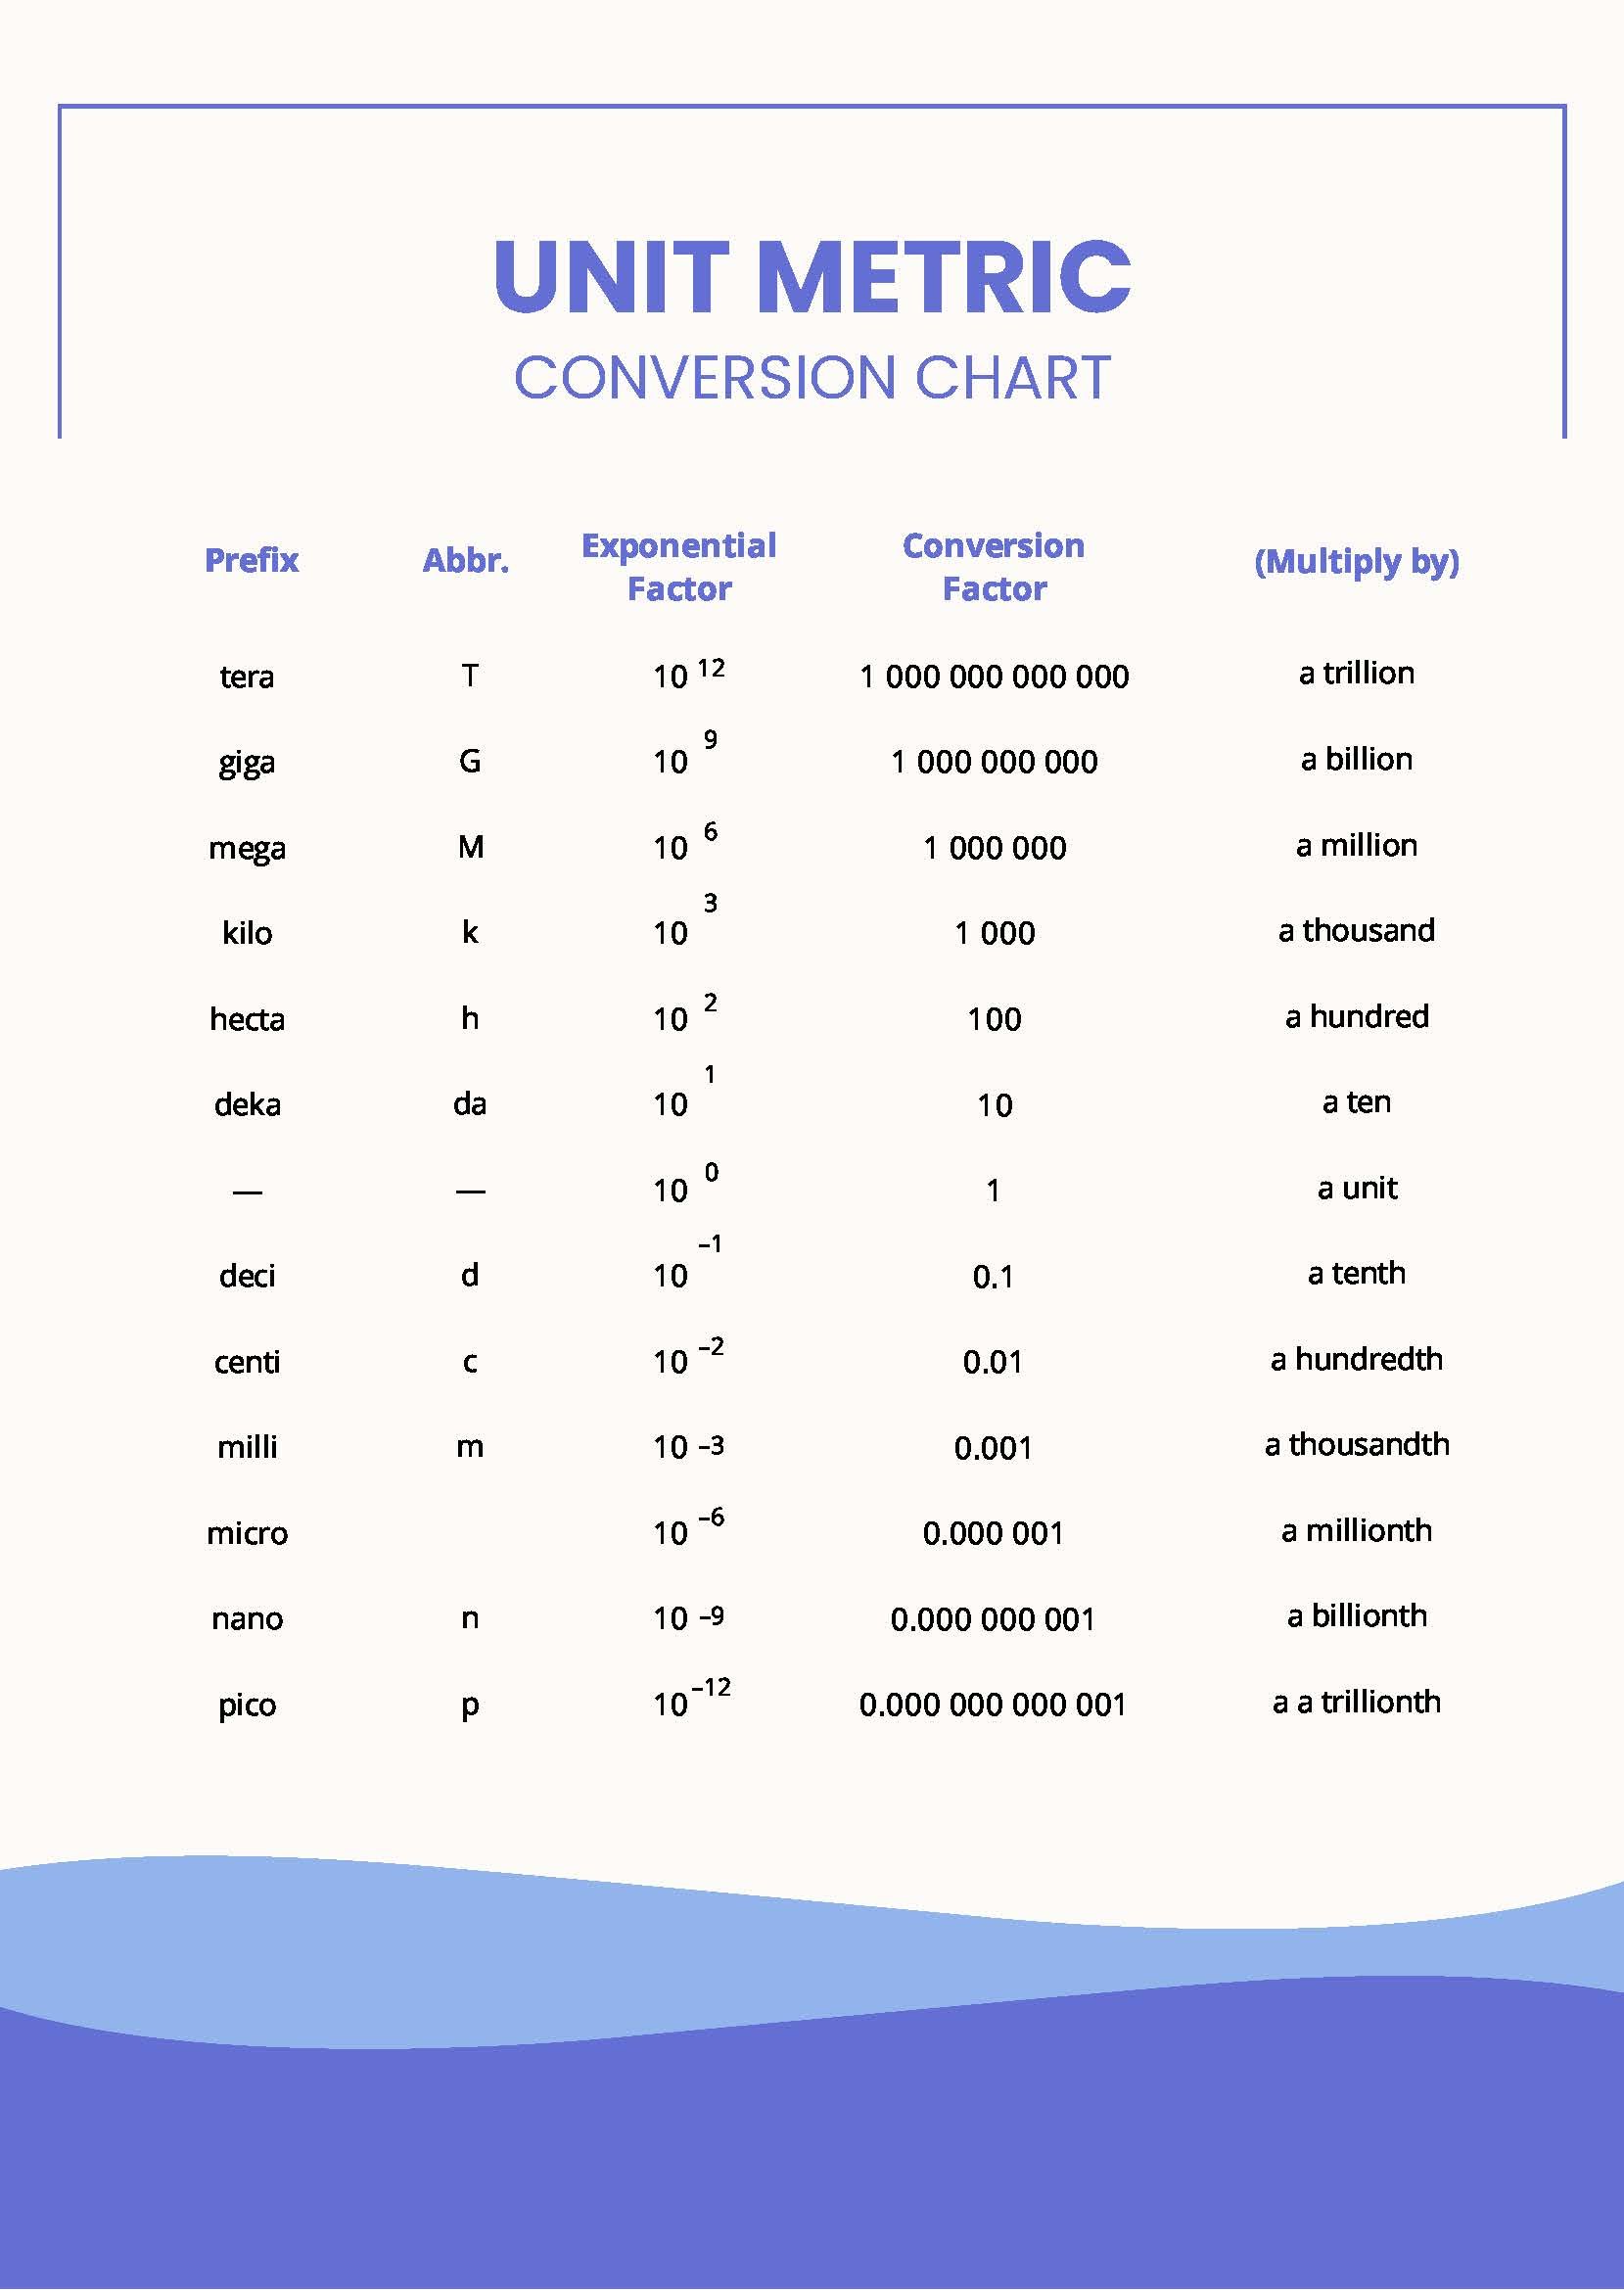
I keep a local spreadsheet with the same numbers, but the printed table on the wall is for quick checks. When a drawing comes in, I highlight every dimension that has a unit tag and verify it against the original spec source. If the spec says 0.5 inch and the drawing shows 12.7 millimeters, I flag it because 0.5 inch is exactly 12.7 millimeters and any deviation means someone rounded prematurely and then the fit might be off by a tolerance stack you cannot see on a single dimension. The edge case that still surprises me is the micron level. When I moved from general machining to optics mounting work, I encountered a situation where a specification called for a surface flatness of 2 microns over a 50 millimeter span. The drawing listed the flatness in microinches as 80 microinches, and 80 microinches is 2.032 microns, not 2 microns. The part was rejected on the first inspection because the optical shop measured in microns and the procurement spec was written in microinches, and nobody had caught the 0.032 micron gap. We ended up using a third-party calibration lab to resolve it, and that experience made me add a rule: at the micron scale, always write the unit and never assume equivalence between microinch and micron without checking. Another thing people get wrong is the assumption that metric and imperial can be freely interchanged in fastener specifications. A M10 bolt is not the same as a 3/8 inch bolt, even though 3/8 inch is 9.525 millimeters and that looks close to 10. The thread pitch alone makes them incompatible, and I have seen at least one incident where someone tried to force a 3/8 inch-16 UNF bolt into an M10 tapped hole and cross-threaded the component. The workaround is to keep fastener references in their native system and only convert when you are calculating clearance or engagement length, never when you are selecting the fastener itself.
When the Table Fails You
No conversion table can save you when the source document is ambiguous about which system it is using. I have seen drawings where a dimension was written as just a number with no unit tag, and the CAD model was in millimeters while theGD&T frame referenced inches. The model would render correctly but the tolerance analysis would be off by a factor of 25.4, and the only person who caught it was the inspector who noticed that the theoretical exact dimension did not match the manufactured feature within any reasonable tolerance band. The table cannot fix ambiguous documentation, it can only help you catch the ambiguity faster. Rounding is the second failure mode. The metric system was designed to avoid arbitrary fractions, but every time you convert back and forth you introduce a rounding decision. 1 inch is exactly 25.4 millimeters, but 1 millimeter is 0.3937007874 inches, and nobody writes that many digits on a drawing. The convention is to round to the appropriate number of significant figures for the tolerance, but if the tolerance is tight enough that the rounded value changes the fit, you need to carry an extra digit through the calculation and round only at the end. I learned this when a gear reduction ratio specified as 3.175 to 1 was being converted to a metric module, and rounding the pitch diameter to 3.18 instead of keeping it at 3.175 shifted the center distance by 0.015 millimeters, which was within the drawing tolerance but outside the backlash specification. The third failure is cultural. In some organizations, the drafting standard explicitly forbids dual dimensioning, and in others it is required. If you work across teams that follow different standards, the conversion table is the least of your problems because you will spend more time arguing about whether a dimension should be marked as 25.4 mm or 1.000 inch or both. The practical solution is to ask the receiving engineer what their standard requires before you send anything, rather than assuming they will accept your format.
What I Would Add to the Table
If I were extending this to cover more specialized conversions, I would add electrical units because that is where I see the most confusion between regions. 1 horsepower = 745.7 watts. 1 kilowatt = 1.34102 horsepower. 1 volt-ampere = 1 watt in DC, but in AC with reactive power the distinction between VA and W matters and the conversion depends on the power factor. I also wish there was a reliable section on viscosity conversions because lubricant specs routinely mix centistokes and SUS, and the relationship is not linear below 100 centistokes. For most daily work, the table above covers about 95 percent of what I encounter. The remaining 5 percent is usually something obscure enough that a quick search is faster than maintaining a reference for it. I stopped trying to build a complete table and started building a reliable one instead. Completeness is a trap because you will never finish it and the ones you leave out are the ones you need most often.