Working with millimeter to inch conversions is something everyone does at some point, but most people skip it because they think they can just divide by 25.4 in their head. That works fine until it doesn't, and then you are stuck with parts that do not fit.
I ended up wasting an entire afternoon on a custom fabrication project because I used a rounded conversion table instead of doing the math properly. The bracket I ordered had holes specified in millimeters, but the drawing was stamped out assuming approximate inch equivalents. Nothing lined up. I should have just kept a calculator open the whole time. The relationship between millimeters and inches is defined internationally. One inch equals exactly 25.4 millimeters. That number does not change. You take whatever measurement you have in millimeters and divide it by 25.4 to get inches. If you are working backwards from inches to millimeters, multiply by 25.4. That is the full method. There is nothing hidden in it. When I started dealing with more demanding tolerances, I stopped relying on printed reference tables entirely. They are usually rounded to three or four decimal places, which is fine for general construction work but completely inadequate when you are assembling precision mechanical components. A difference of 0.0001 inches might look small, but over a series of mating parts, it adds up fast.
Mm To Inch Chart
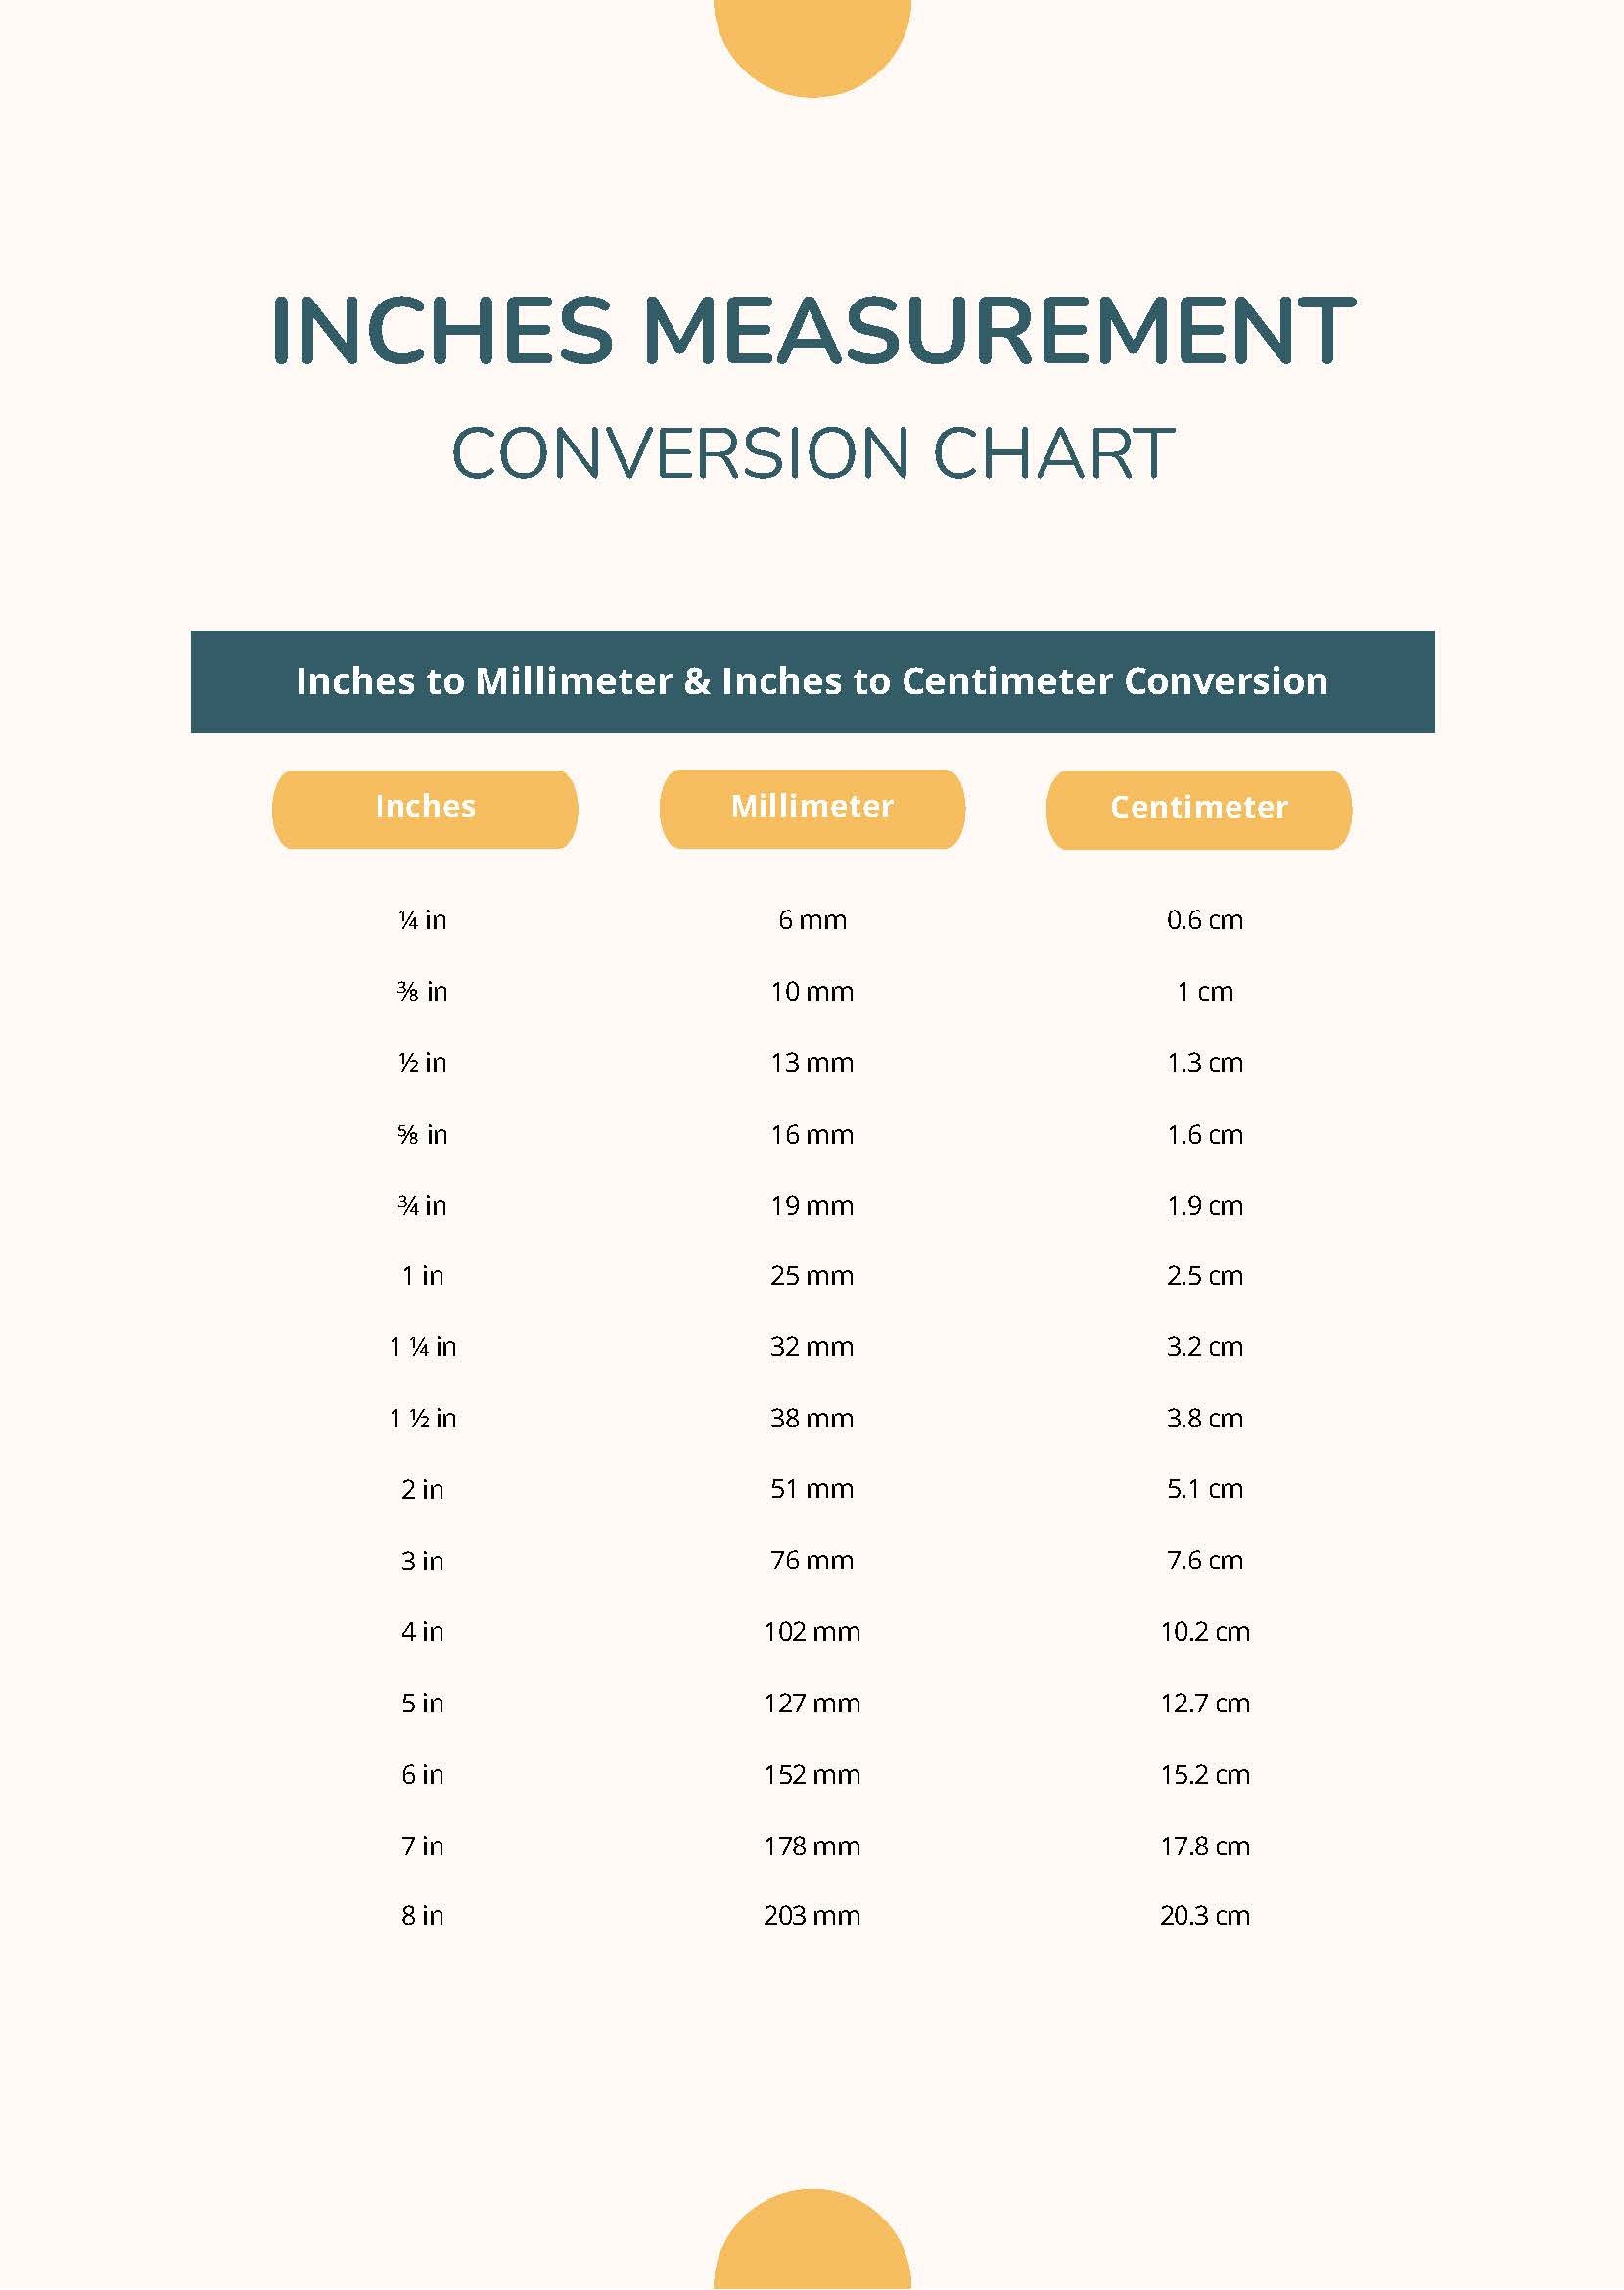
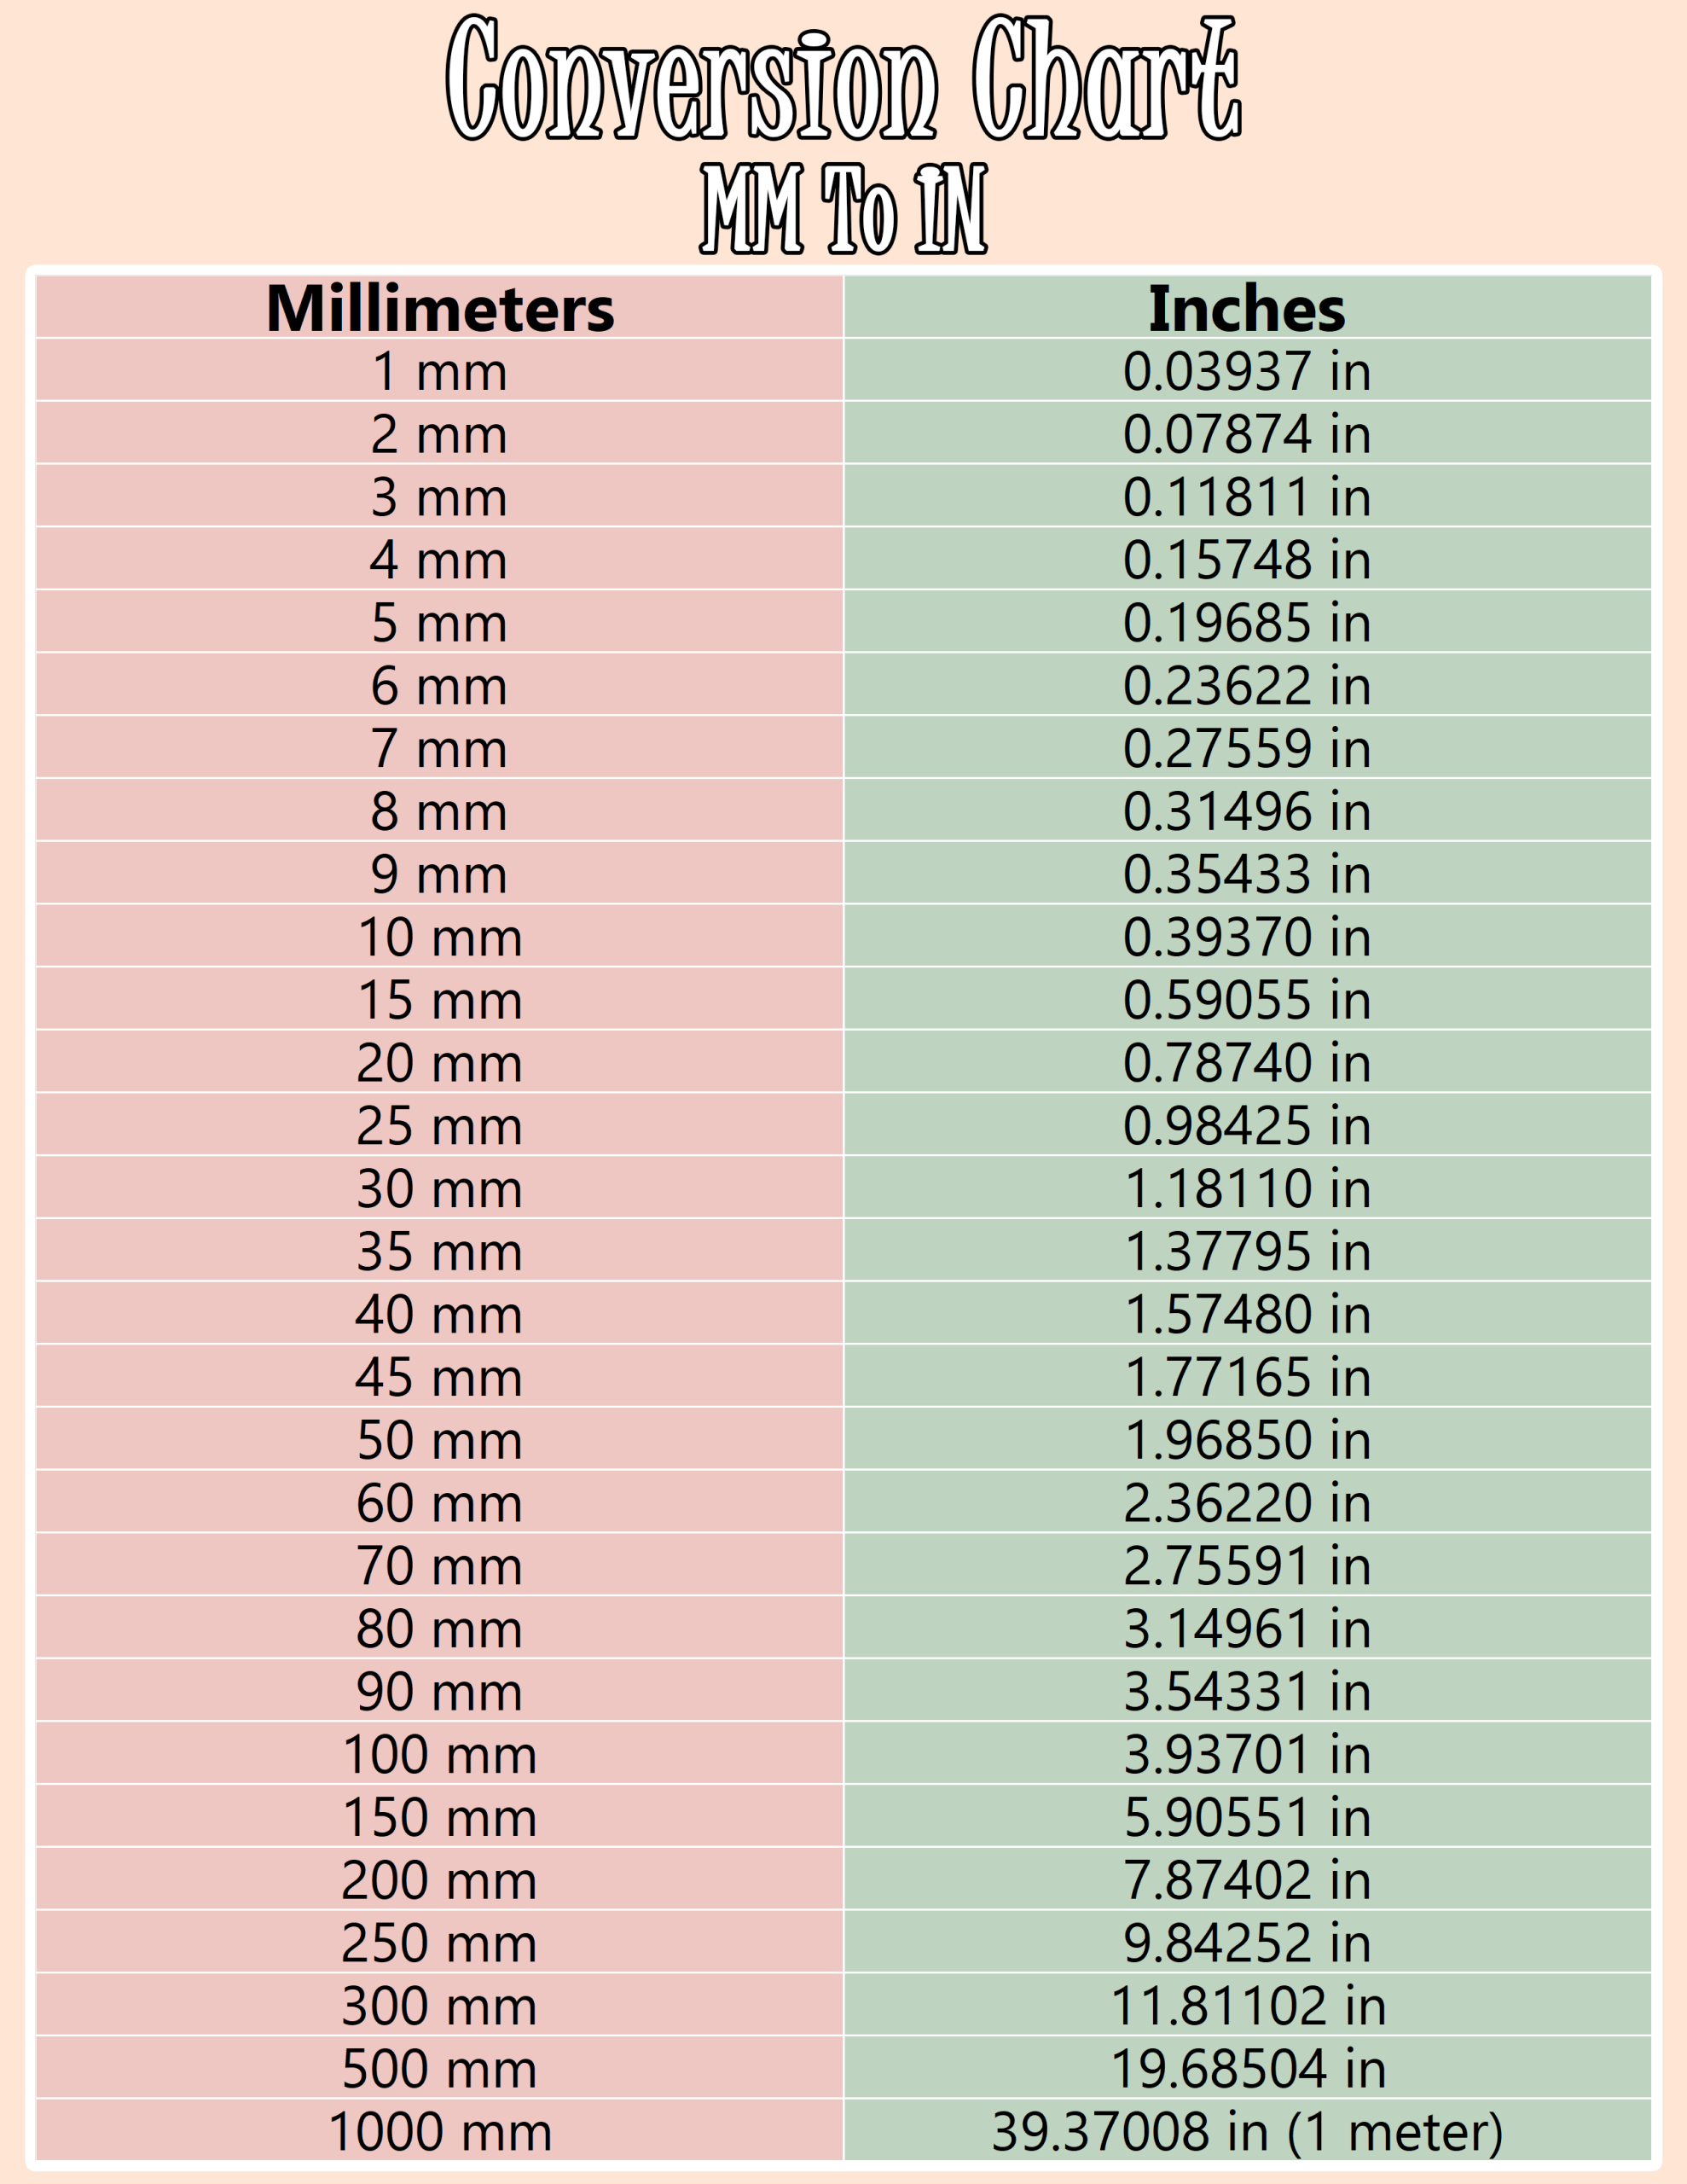
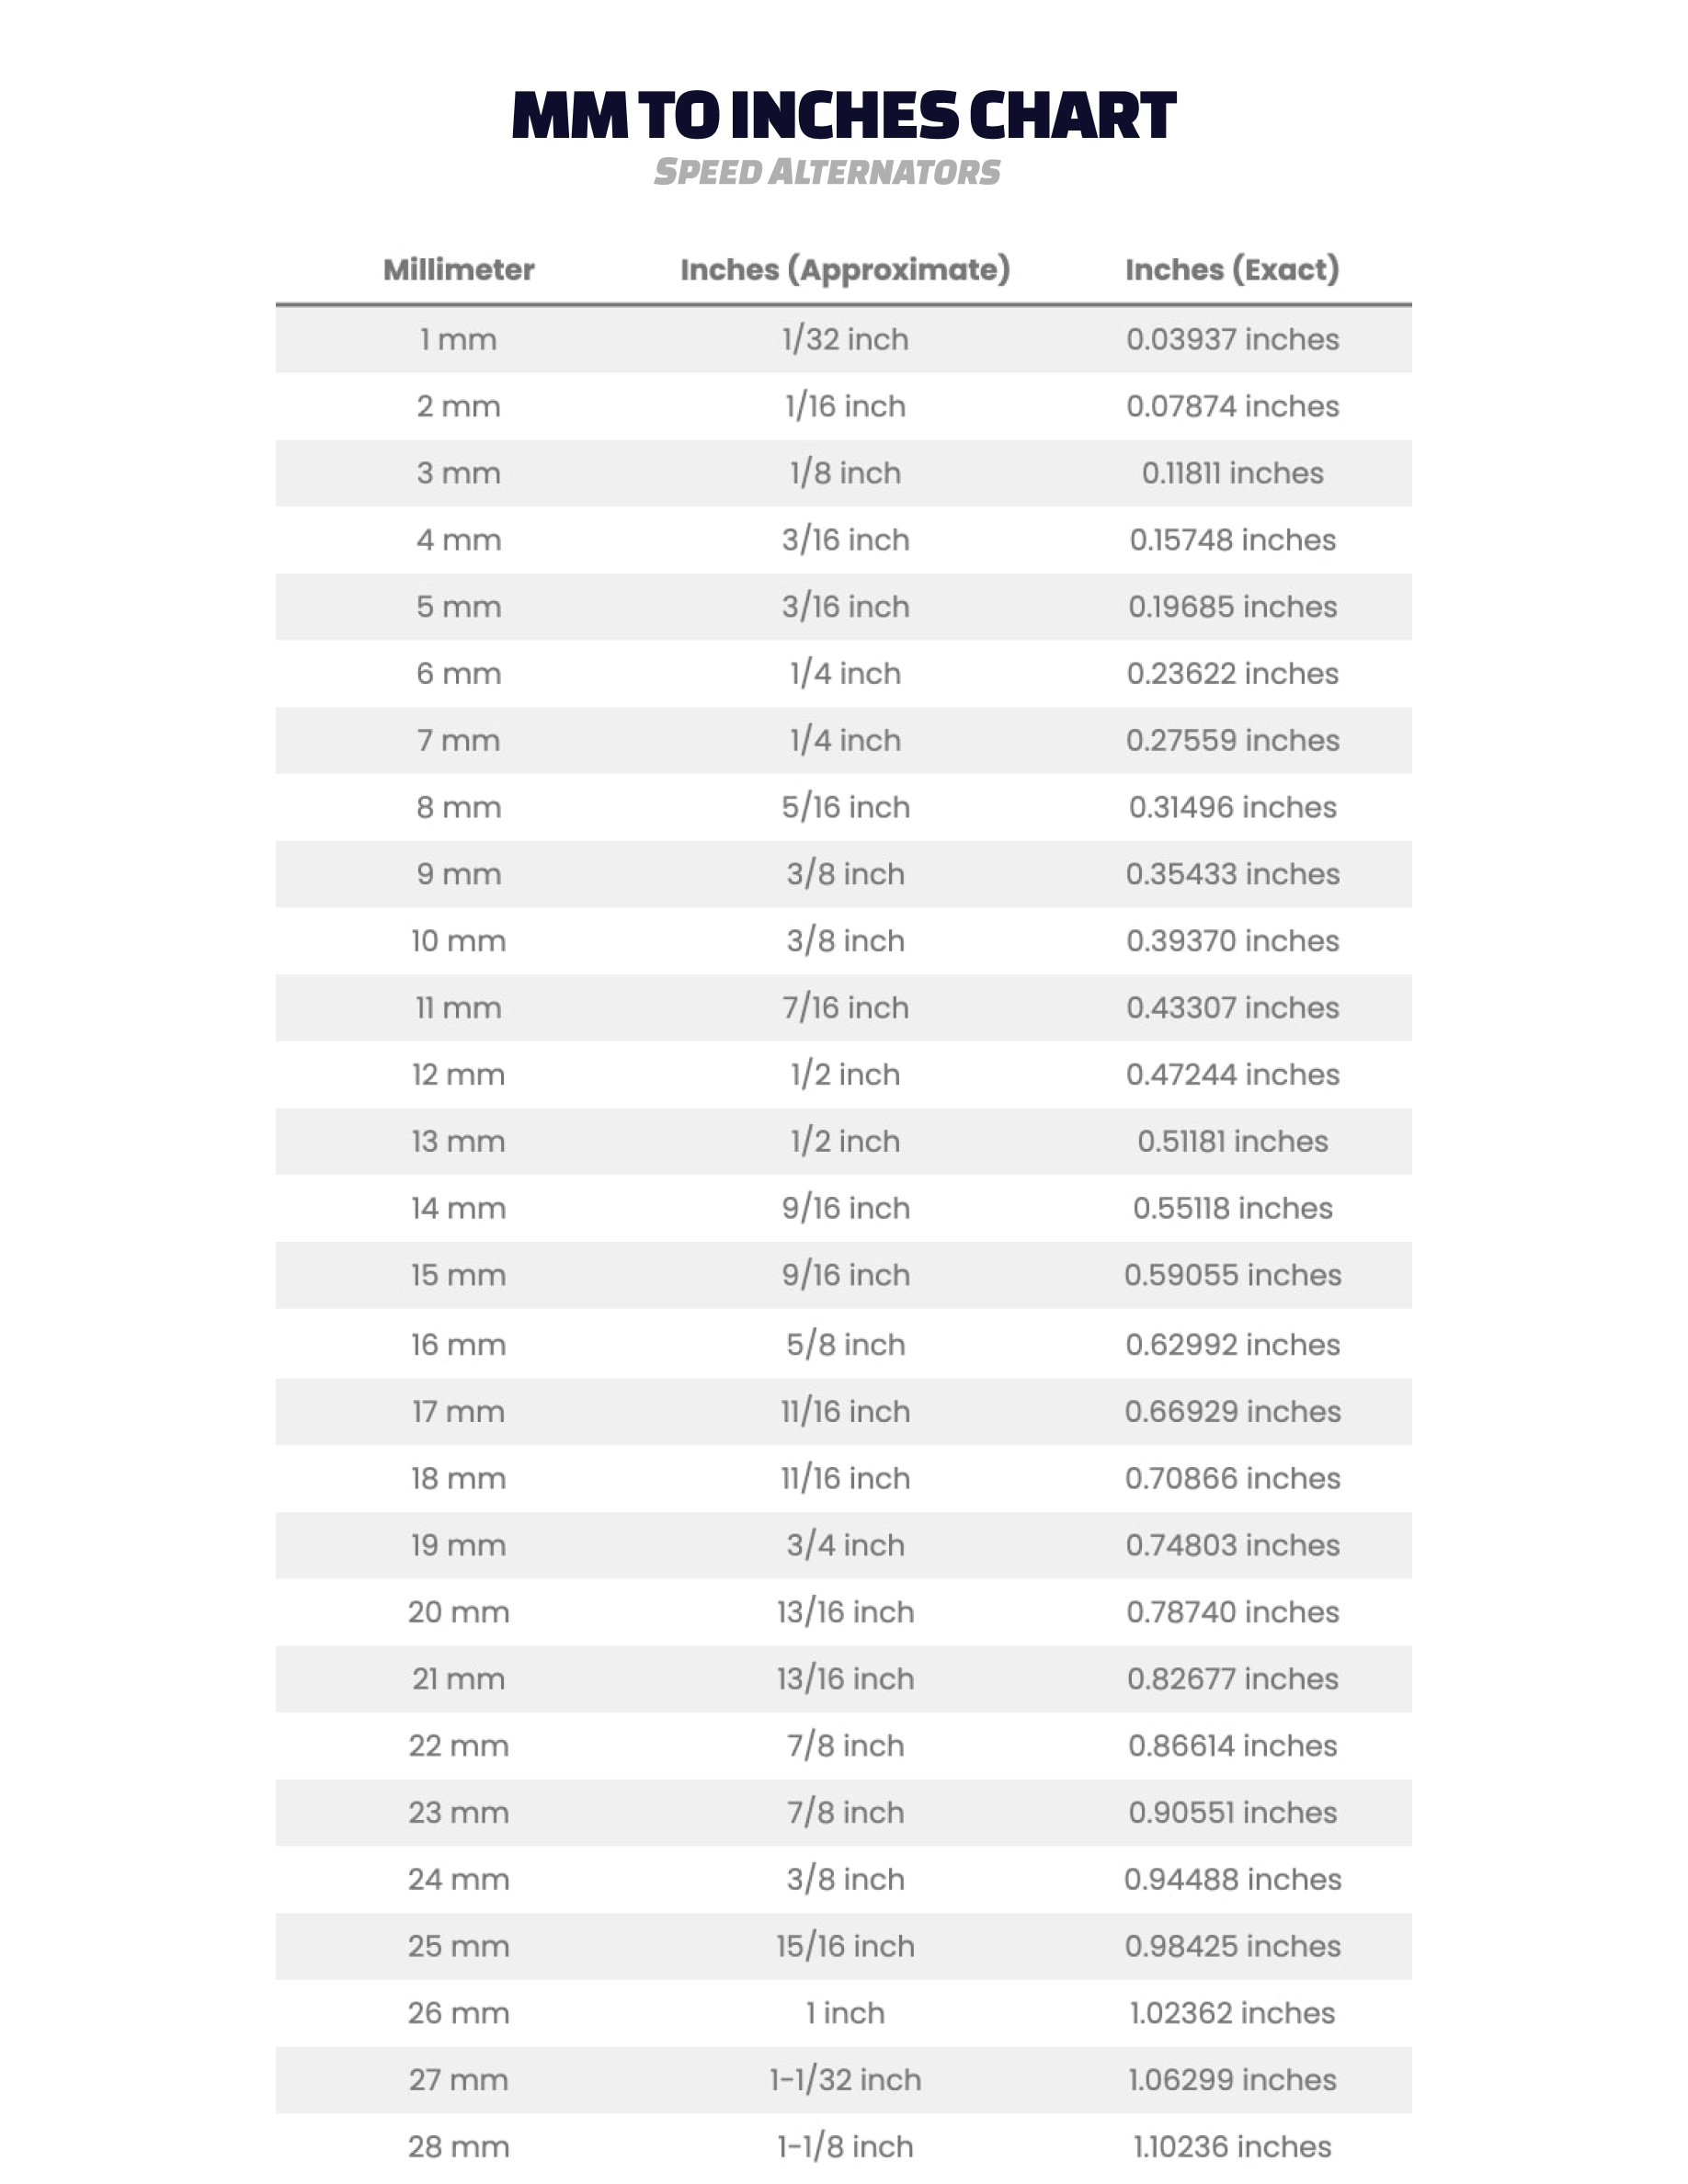
Below is a straightforward reference for the most commonly needed conversions. These values are calculated using the exact 25.4 factor and rounded to four decimal places for practical use. 0.5 mm = 0.0197 in 1 mm = 0.0394 in
2 mm = 0.0787 in 3 mm = 0.1181 in 5 mm = 0.1969 in
Get the Full Details

6 mm = 0.2362 in 8 mm = 0.3150 in 10 mm = 0.3937 in
12 mm = 0.4724 in 15 mm = 0.5906 in 20 mm = 0.7874 in
25 mm = 0.9843 in 30 mm = 1.1811 in 40 mm = 1.5748 in

50 mm = 1.9685 in 60 mm = 2.3622 in 75 mm = 2.9528 in
100 mm = 3.9370 in This chart covers the range you will encounter in most hardware and machining work. Anything outside these common sizes, like 1.5 mm or 22 mm, requires actual division rather than lookup, and the chart gets less useful past about 200 mm unless you build one tailored to your specific project.
Where these charts break down
Converted values in any chart are never exact. The result of dividing by 25.4 is often an infinite decimal, so every entry in a printed chart is rounded somewhere. Rounding to four decimal places introduces an error of roughly 0.00005 inches per conversion. That is negligible for cutting lumber or measuring a room. It is not negligible when you are working with bearing fits, shim stacks, or anything that requires a tolerance tighter than 0.001 inches. I learned this the hard way when converting drill bit sizes for a CNC project. The chart I was using rounded 4.5 mm to 0.1772 inches, but the actual value is 0.1771653543... The difference is tiny, but when the toolpath was already cut and the part was already on the table, I spent an hour recalibrating rather than debugging. Now I just type the division into a calculator or spreadsheet before committing to anything on paper. Another limitation is that standard charts do not account for temperature-dependent material expansion. If you are working with aluminum or steel in a shop where the ambient temperature swings by more than ten degrees Fahrenheit across the workday, your converted dimensions shift with the material. No chart corrects for that. You need to factor in the coefficient of thermal expansion separately if your application demands it. For most weekend projects, this is irrelevant. For production runs, it is a problem you only discover after the parts fail inspection.
What to do instead of printing a chart
The single most reliable approach is keeping a spreadsheet with a formula. Put your millimeter values in one column, use the formula =A1/25.4 in the next column, and set the formatting to display as many decimal places as your tolerance requires. This eliminates rounding errors at the source, takes about two minutes to set up, and scales to any range without buying a new reference document. If you need physical references in the field, a dual-scale ruler marked in both millimeters and inches is worth far more than any paper chart. The markings on a good quality steel rule are calibrated to within 0.001 inches across the full length, which is better than what you will find in almost any downloaded conversion table. For quick mental approximations, multiplying by 0.04 and then subtracting about 1 percent gives you a result close enough for rough layout work. The conversion factor 0.04 is easy to calculate, and the 1 percent correction brings it closer to the true value of 0.03937. It is not precise, but it is fast, and speed matters when you are standing at a workbench with the cutting already started.
A note on online converters
Most online converters produce correct results, but they are not consistently reliable. I have seen at least two popular conversion sites return slightly different values for the same input due to how each handles floating-point precision internally. If you are double-checking a critical dimension, cross-reference the result on at least two sources or verify it manually with the 25.4 formula. It takes ten seconds and prevents the kind of error that costs hours of rework. The method is straightforward. The edge cases are what cause problems, and knowing where the method falls apart is usually more valuable than memorizing a list of conversions. Keep the exact factor in mind, use a calculator for anything beyond rough estimates, and move on.