What Nd Yag Laser Technology Actually Is
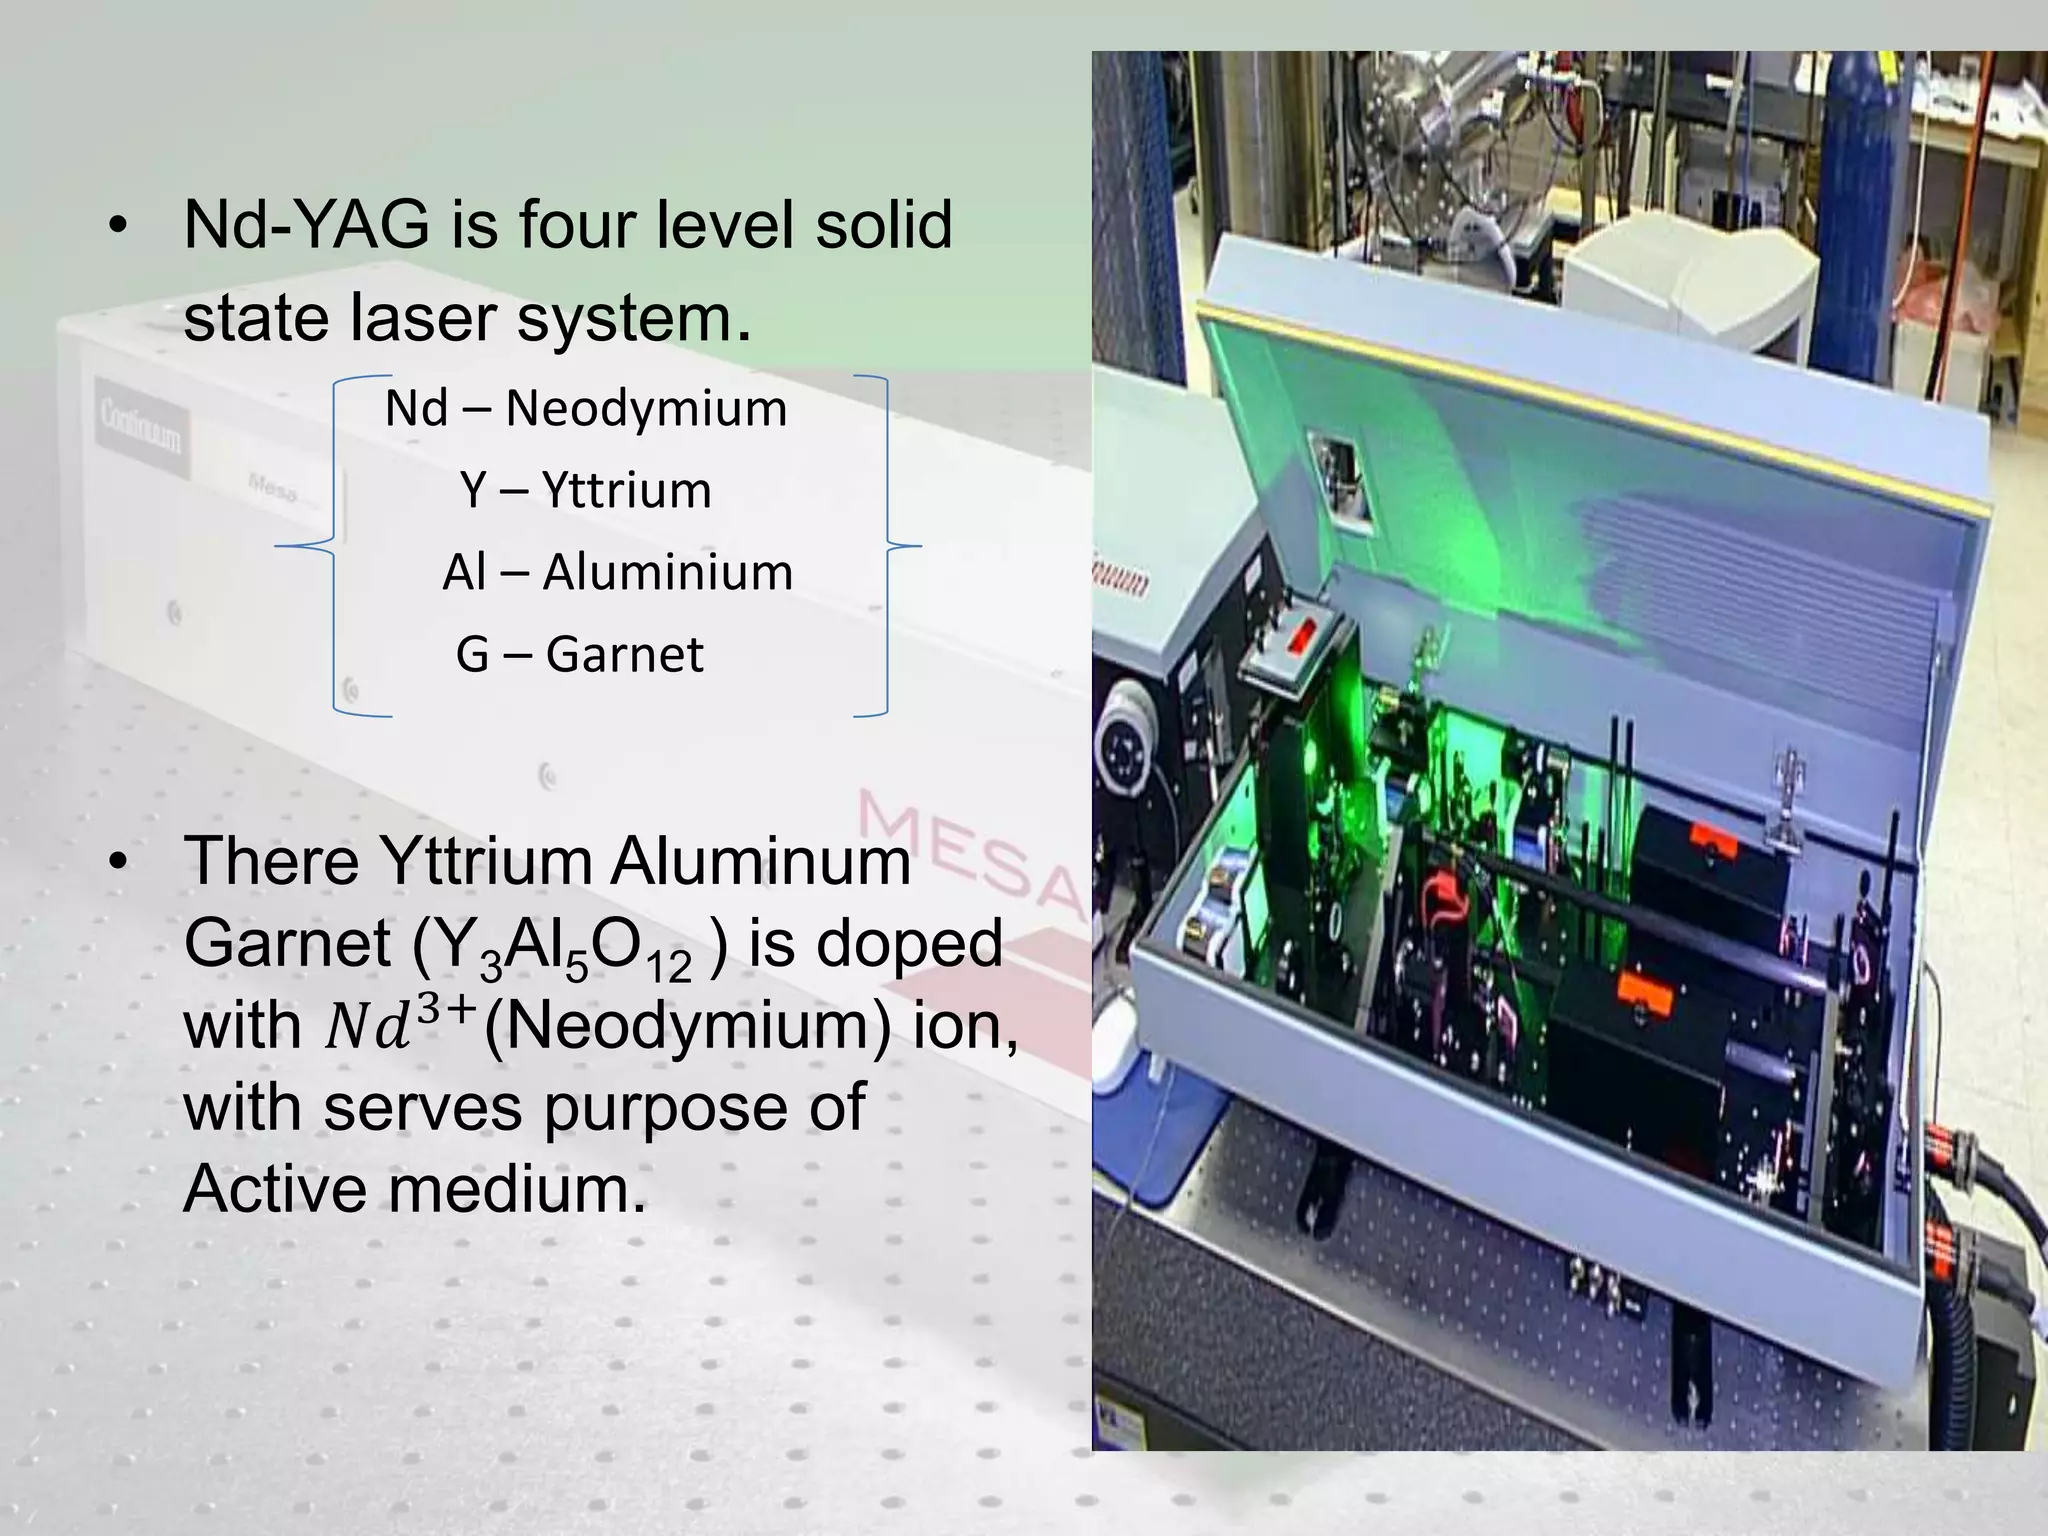
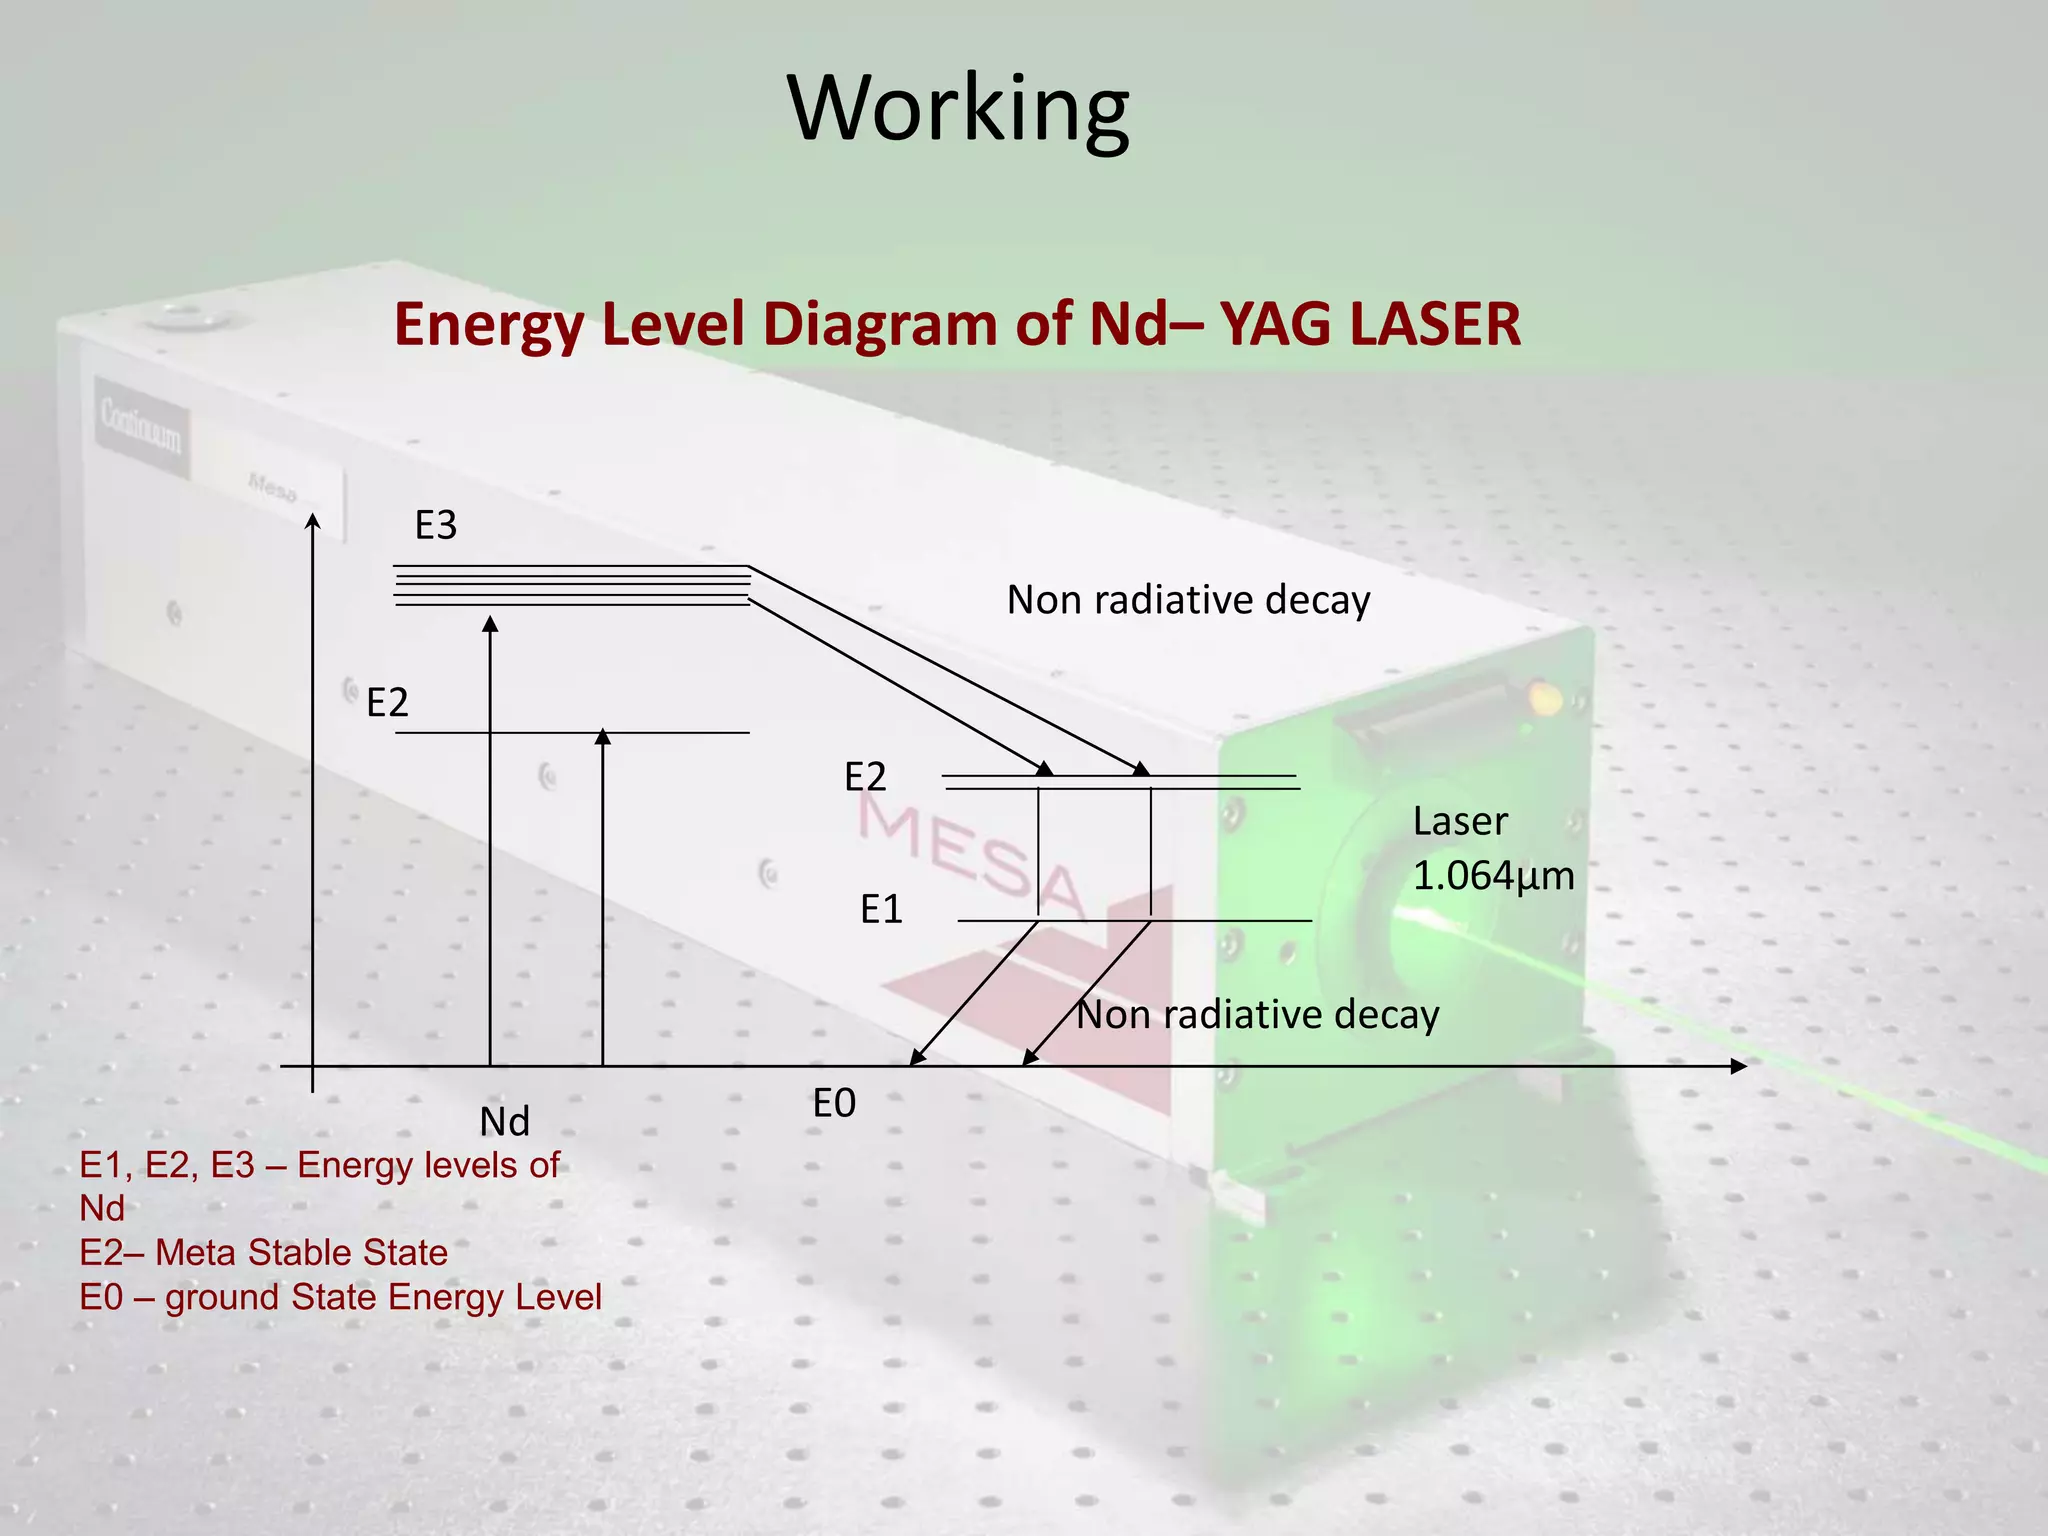
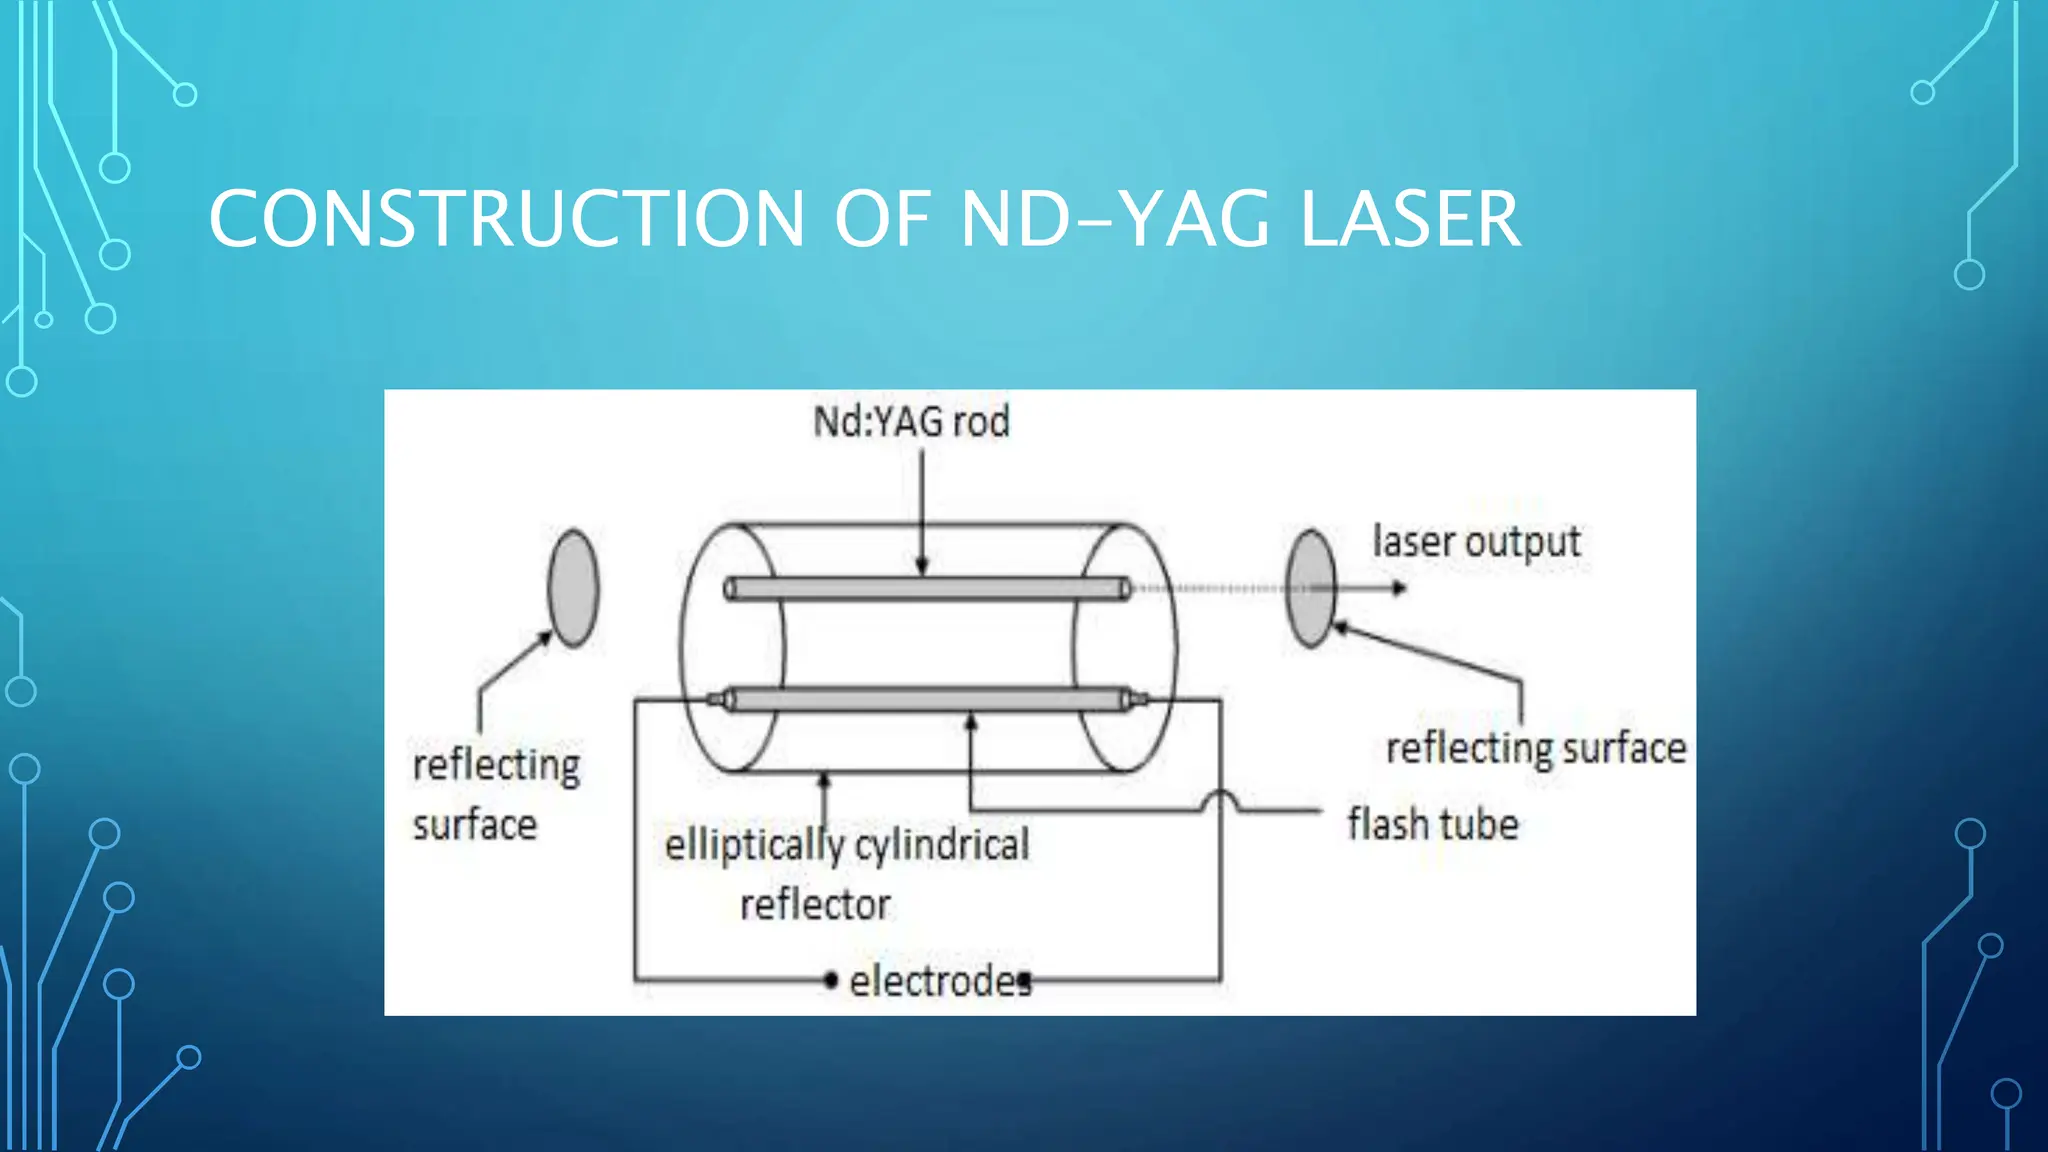
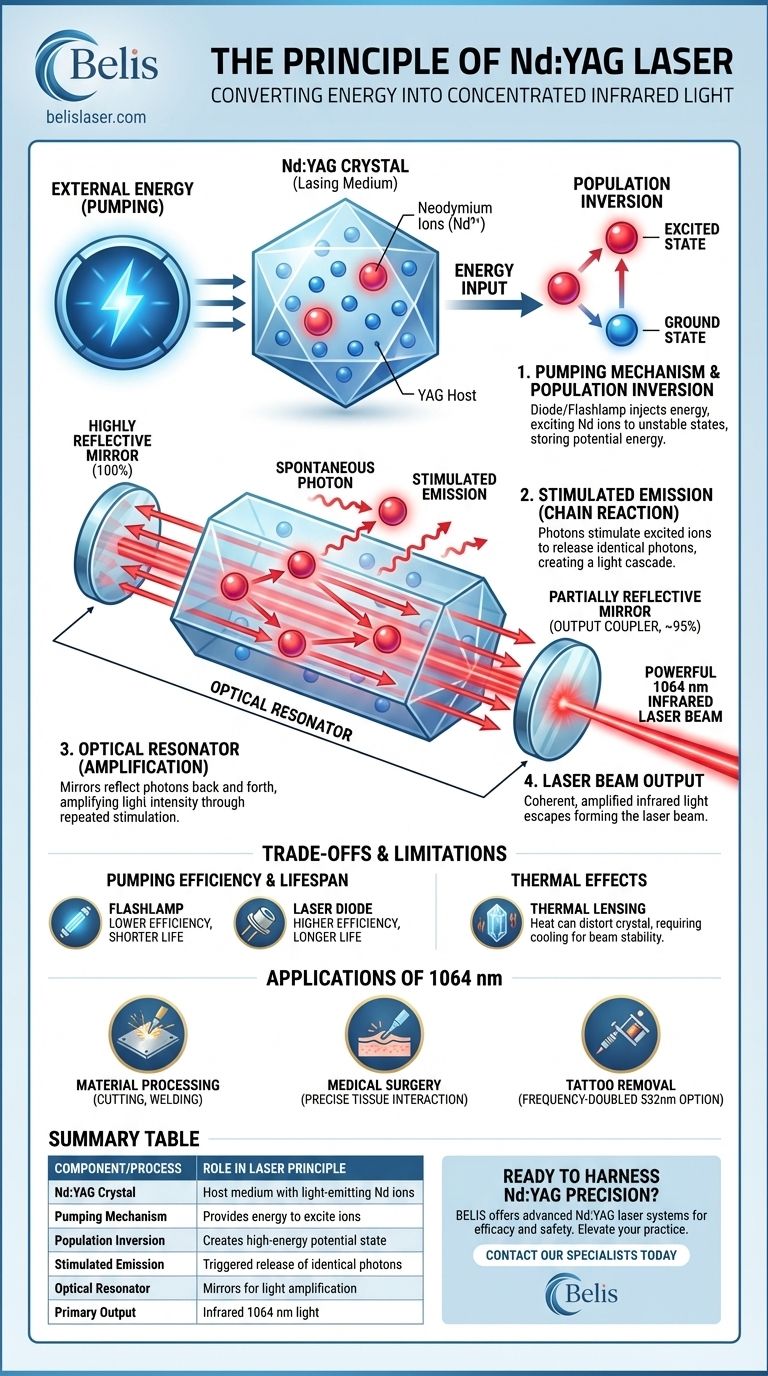
Most people hear "Nd Yag laser" and picture something from a sci-fi movie. The reality is less glamorous and more practical. Nd Yag stands for neodymium-doped yttrium aluminum garnet. It is a solid-state laser medium. The active ion is neodymium, sitting inside a crystal lattice. When you pump it with light, usually from flashlamps or diodes, it emits at 1064 nanometers. That wavelength is near-infrared. You cannot see it with your naked eye. It punches through tissue, paint, metal, whatever the job requires. The first thing to understand is that Nd Yag lasers are not a single tool. They come in Q-switched, mode-locked, and continuous-wave configurations. Each behaves completely differently. Q-switched gives you short, high-power pulses. Mode-locked throws even shorter bursts. Continuous wave just delivers steady energy. Pick the wrong one for your application and you will waste time and material, then wonder why the results look sloppy.
How Nd Yag Laser Technology Works in Practice
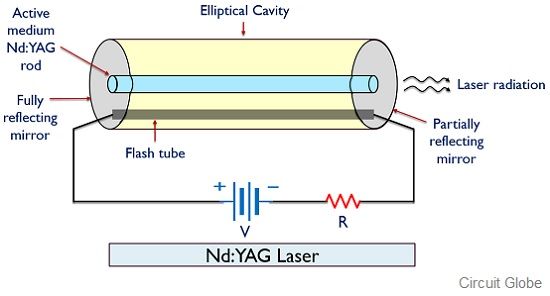
Here is how I approach a typical Nd Yag Laser Technology setup. Start with the pump source. Diode-pumped versions are everywhere now because they are efficient and stable. Old-school flashlamp-pumped units still exist, but they run hot, they consume power like a small appliance, and the beam quality degrades as the lamp ages. If you are buying today, go diode-pumped unless your budget forces otherwise. Next, the resonator. Nd Yag needs two mirrors. One fully reflective, one partially transmissive. The distance between them determines the mode structure. A short resonator gives you a better beam. Long resonators are cheaper but the output is messier. For most industrial marking and engraving, a compact cavity with intracavity optics works fine. Just make sure the gain crystal is properly aligned to the pump source. Misalignment here causes power droop and inconsistent cuts. Then there is the beam delivery. Nd Yag at 1064 nm travels through standard optical fiber with minimal loss. Galvo scanners handle the positioning. F-theta lenses focus the beam onto the workpiece. A typical setup covers a 100 by 100 millimeter field with good focus uniformity. Larger fields need more expensive lenses or a different scanning strategy. This is where budget decisions get painful.
Applications That Actually Make Sense
Marking and engraving is the bread and butter. Anodized aluminum, titanium, certain plastics, coated metals. The laser interacts with the surface layer, modifying color or removing material. Speeds of 500 to 2000 millimeters per second are common on decent machines. A part that used to take a rotary drum or chemical etching now does in seconds. Cutting thin sheet metal works too. Stainless steel up to about two millimeters, aluminum similar. Beyond that, the energy density drops and you get ragged edges or incomplete cuts. Fiber lasers have eaten into this space significantly. Nd Yag still holds ground on specific alloys where fiber wavelengths interact poorly. The 1064 nm line is absorbed better by copper and brass than 10700 nm fiber outputs. If you are working with high-conductivity metals, Nd Yag remains relevant. Laser cleaning is another solid use case. Oxide removal, rust stripping, paint ablation. The short pulse evaporates contaminants without heating the substrate. I have seen operators clean engine blocks in under ten minutes where sandblasting would take an hour and create hazardous waste. The tradeoff is throughput. Nd Yag cleaning is slower than abrasive methods on large surfaces. It excels on precision parts where abrasives would damage geometry.
Get the Full Details

A Problem I Actually Encountered
Last year I was running a Nd Yag system for serial number engraving on stainless steel medical instruments. The spec called for consistent contrast across a batch of three hundred pieces. The first fifty looked perfect. Then the output started fading incrementally. Same power setting. Same speed. Same focus. Nothing had changed on the machine. I ruled out the obvious: crystal aging, lamp degradation, water chiller failure. None of it. The issue was the galvo scanner thermal drift. Nd Yag pulses heat the scanner mirrors slightly with each shot. Over a couple hundred cycles, the thermal expansion shifted the beam path by fractions of a degree. The focus landed slightly off the surface on later parts. Less absorption. Fainter marks. The fix was adding a thermal compensation routine to the control software. It measured mirror temperature every cycle and adjusted the galvanometer offset in real time. Took about an afternoon to implement and a week to validate. Now the first part and the three-hundredth look identical. This is the kind of problem nobody writes about in brochures. Thermal effects in scanning systems are real and cumulative. If your application runs high throughput, build compensation in from the start.
Counter-Intuitive Things Beginners Miss
People assume higher pulse energy always means better results. That is wrong. On many materials, excessive energy causes cratering, recast layers, and thermal damage around the mark. The goal is minimum energy for the desired effect. For marking anodized aluminum, you often need less than one millijoule per pulse. Dial in the lowest setting that still produces readable contrast. It gives cleaner edges and longer component life. Another misconception is that 1064 nm works on everything black. Dark materials absorb well at that wavelength, yes. But transparent materials like glass or clear polycarbonate are nearly invisible to Nd Yag unless you add a coupling agent or operate in a regime that triggers nonlinear absorption. For those substrates, frequency-tripled Nd Yag at 355 nm or a UV fiber laser makes more sense. Don't force a tool to do what it cannot. There is also the myth that pulsed Nd Yag is always superior to continuous wave. CW is cheaper, simpler, and faster for deep engraving or welding applications. Pulsed operation shines when you need thermal control. Choose based on the physics of your material interaction, not marketing claims.
Limitations and When to Walk Away
Nd Yag technology has clear weaknesses. Beam quality degrades over time. Diode-pumped units are more stable than flashlamp versions, but the crystal still experiences photodarkening. After tens of thousands of hours, output power drops and beam profile broadens. Budget for crystal replacement or system recalibration on a five-year horizon. Capital cost remains higher than CO2 lasers for equivalent average power. If your primary work is cutting wood, acrylic, or leather, a CO2 system at 10600 nm is more efficient and cheaper. Nd Yag simply does not compete there. The 1064 nm wavelength is absorbed by metals and some polymers. It transmits through many organics. Match the wavelength to the material absorption spectrum before buying equipment. Safety is another constraint. Invisible 1064 nm radiation means you cannot see the beam. Interlocks, enclosed workspaces, and appropriate laser safety glasses are non-negotiable. Nd Yag systems typically require Class 4 enclosures. Opener exposure risks retinal damage instantly. This is not a hobbyist toy even at low power levels.
For thick section cutting beyond three millimeters of steel, fiber lasers dominate. Higher wall plug efficiency, better beam quality, lower operating cost per part. Nd Yag does not make economic sense at those depths. Keep it in the thin-sheet, marking, and precision cleaning lanes where it still has advantages.
Practical Setup Guidelines
Water cooling is essential. Even diode-pumped Nd Yag units generate significant heat at the crystal. Maintain chiller setpoint between 20 and 22 degrees Celsius. Fluctuations above that cause wavelength drift and power instability. Monitor return water temperature. A rising delta between inlet and outlet indicates pump wear or heat exchanger fouling. Optical cleaning schedule matters more than people realize. Dust on the output coupler or scanner windows absorbs 1064 nm energy and creates hot spots. Wipe weekly with optical-grade tissue and pure isopropanol. Replace windows when you see persistent burn marks that cleaning cannot remove. One degraded window can ruin a entire batch of parts. Beam profiling should be done quarterly at minimum. A knife-edge scanner or camera-based profiler will show you whether your M-squared value is staying within spec. If it drifts above 1.5, the crystal or alignment needs attention. Catching this early prevents downstream quality issues that are far more expensive to fix.
Software configuration deserves equal attention. Pulse frequency, pulse width, and duty cycle interact in ways that are not always intuitive. For fine marking, shorter pulse widths around 20 to 50 nanoseconds give cleaner results. Higher repetition rates improve throughput but can cause thermal accumulation on sensitive materials. Find the sweet spot through systematic parameter sweeps. Document everything. Different materials respond differently to the same nominal settings.
What to Look for When Buying
Pick a manufacturer that provides beam profiling data, not just average power specifications. Two systems rated at 50 watts can perform very differently depending on spatial mode quality. Ask for M-squared measurements and beam waist specifications at the workpiece plane. Galvo scanner quality is a frequent bottleneck. Cheap scanners drift with temperature and wear out faster. Brand-name components from Raytools or Junyi last longer and hold calibration better. Factor this into your total cost of ownership calculation. Replacement scanner heads run several thousand dollars. Service accessibility matters. Nd Yag lasers contain high-voltage pump supplies, precision optics, and moving parts. When something breaks, you need technical support that actually understands solid-state laser physics, not just general equipment repair. Check warranty terms and response time guarantees before committing.
Integration capability should be verified upfront. Most modern systems support standard industrial protocols like Ethernet IP, Profinet, or simple trigger I/O. If your production line requires synchronization with conveyors or robots, confirm this is available in the base configuration. Retrofitting communication interfaces later is costly and risky.