Understanding Fluid Behavior When It Matters
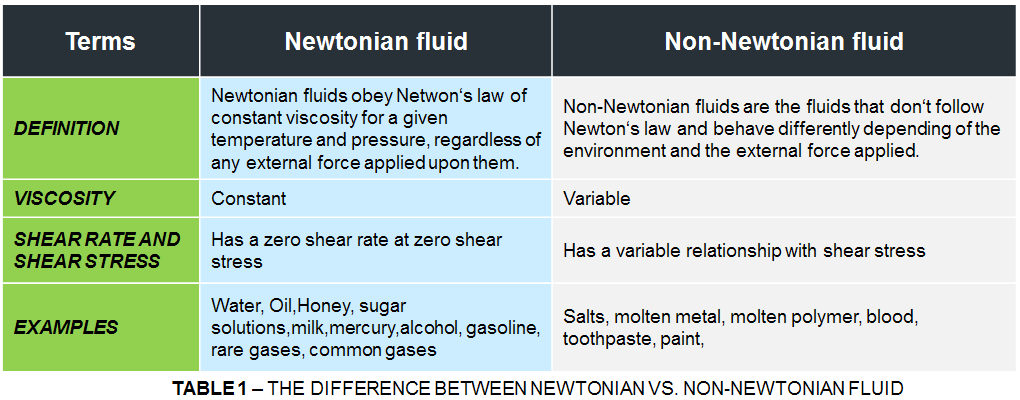
You're probably familiar with water and how it just flows. Pour it, it pours. Shake it, it shakes. That's a Newtonian fluid. Now imagine paint that thickens when you stir it hard or a mixture that refuses to move at all until you push it past a certain point. Those are Non-Newtonian fluids, and they exist everywhere in industrial processes if you know where to look. The basic difference between Newtonian And Non Newtonian fluids comes down to whether viscosity changes when you apply force. A Newtonian fluid maintains a constant viscosity regardless of how much shear stress you put on it. Water stays water whether you're stirring it gently or blasting it through a pipe at high velocity. A Non-Newtonian fluid's viscosity shifts based on the shear rate, the duration of force application, or sometimes both.
Reading Rheology Data Without Losing Your Mind
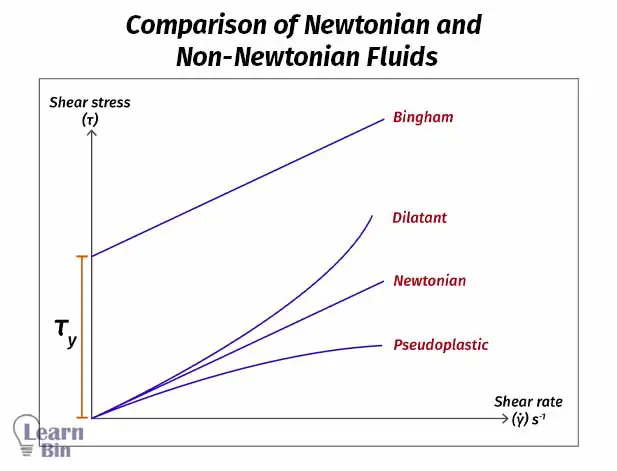
When you're actually working with these materials, the first thing you need is a rheometer or at minimum a viscometer with variable speed settings. I spent about three weeks last year trying to get a ceramic slurry to flow consistently through a 3D printing extruder, and the data I gathered there changed how I approach every non-Newtonian material since. The slurry was shear-thinning, which sounds like it should make extrusion easy, but it also had a significant yield stress. My nozzle would sit there and refuse to push anything out until I hit a threshold pressure, then suddenly it'd flood. The prints came out terrible every single time. The workaround was straightforward once I understood what was happening. I pre-sheared the material by running the extruder motor in reverse briefly before each print cycle, which broke the yield structure. Then I printed at a consistent mid-range shear rate instead of trying to push it through the nozzle at maximum speed. The yield stress itself wasn't the problem—excessively high shear rates during extrusion were causing the viscosity to drop too far, leading to structural collapse right after deposition. Once I controlled the shear profile rather than just cranking pressure, the prints were acceptable for post-processing. This is where most people get tripped up. They see shear-thinning on a viscosity curve and assume the material will flow easily. They don't account for the yield stress or the fact that the material might be thixotropic, meaning its viscosity continues to change over time even at a constant shear rate. A material that reads 500 centipoise at low shear and 50 centipoise at high shear on a quick snapshot test might behave completely differently if you're holding it at that high shear for five minutes straight.
Common Pitfalls That Cost Real Money
Pipe flow calculations are where non-Newtonian behavior causes the most damage. If you size a pump using a single viscosity number, you're already making a mistake. The power-law model and the Herschel-Bulkley model are the two most commonly used frameworks. The power-law model handles simple shear-thinning and shear-thickening fluids but ignores yield stress entirely. The Herschel-Bulkley model accounts for yield stress plus shear-thinning behavior and is more accurate for materials like drilling muds, food pastes, and wastewater sludge. I once saw a pharmaceutical company estimate a batching process using a Newtonian approximation for a polymer solution that was strongly shear-thinning. They designed the mixing impeller based on a viscosity measured at a single high shear rate. When the tank was nearly full and the actual shear rates dropped significantly, the apparent viscosity was ten times higher than what they'd used in the calculation. The impeller stalled. They ended up replacing the motor and redesigning the tank geometry. The whole thing took six weeks and probably cost them around forty thousand dollars in lost production time. Another thing that comes up constantly is temperature compounding. Viscosity drops as temperature rises for almost every fluid, Newtonian or not. But non-Newtonian fluids don't follow the same temperature-viscosity relationship linearly. A polymer solution might thin predictably with heat at low shear rates but show erratic behavior at high shear rates as the temperature changes. If you're processing a non-Newtonian material and your facility has seasonal temperature swings without climate control, you should expect batch-to-batch variability unless you're actively controlling the material temperature during processing.
Get the Full Details
Shear-Thickening Fluids Are Their Own Problem
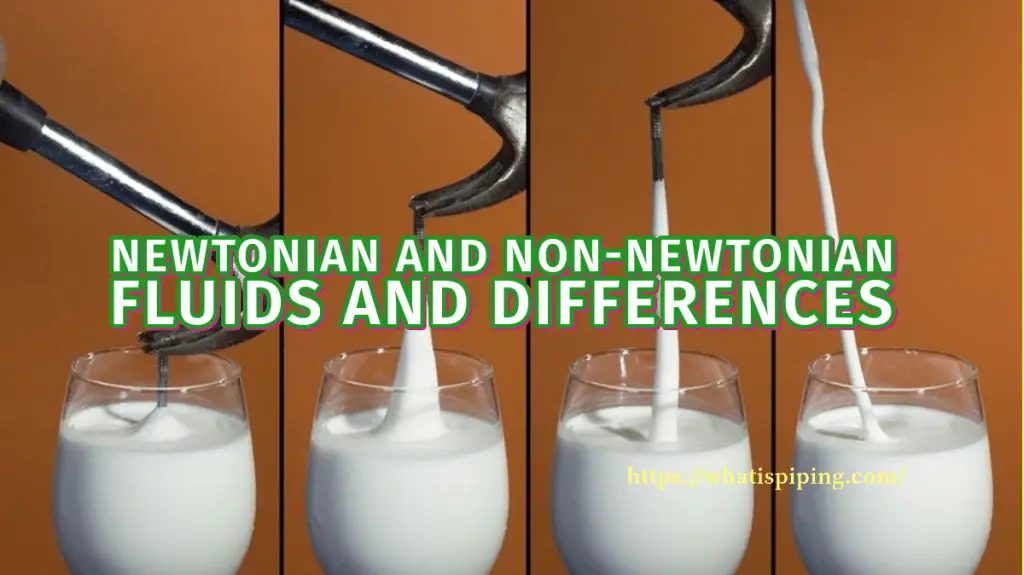
Most discussions focus on shear-thinning materials because they're more common in manufacturing. Oobleck, which is basically cornstarch and water, is the classic shear-thickening example. It liquefies when you poke it gently and turns solid when you strike it. In an industrial context, shear-thickening fluids show up in things like certain suspension pumps and slurry transport systems where particles settle and then suddenly jam when the flow accelerates. These are harder to work with because the viscosity increase happens unpredictably once you cross a critical shear rate threshold, and that threshold shifts with particle concentration and size distribution. If you're dealing with a shear-thickening system, the practical approach is to stay below the critical shear rate entirely. Running the system faster to clear a potential blockage often makes it worse. I've seen operators accidentally accelerate a slurry pump past the critical point and watch the pipe pressure spike dramatically within seconds. The fix isn't to push harder. It's to reduce flow rate and let the material restructure itself, then restart slowly.
Practical Testing That Actually Works
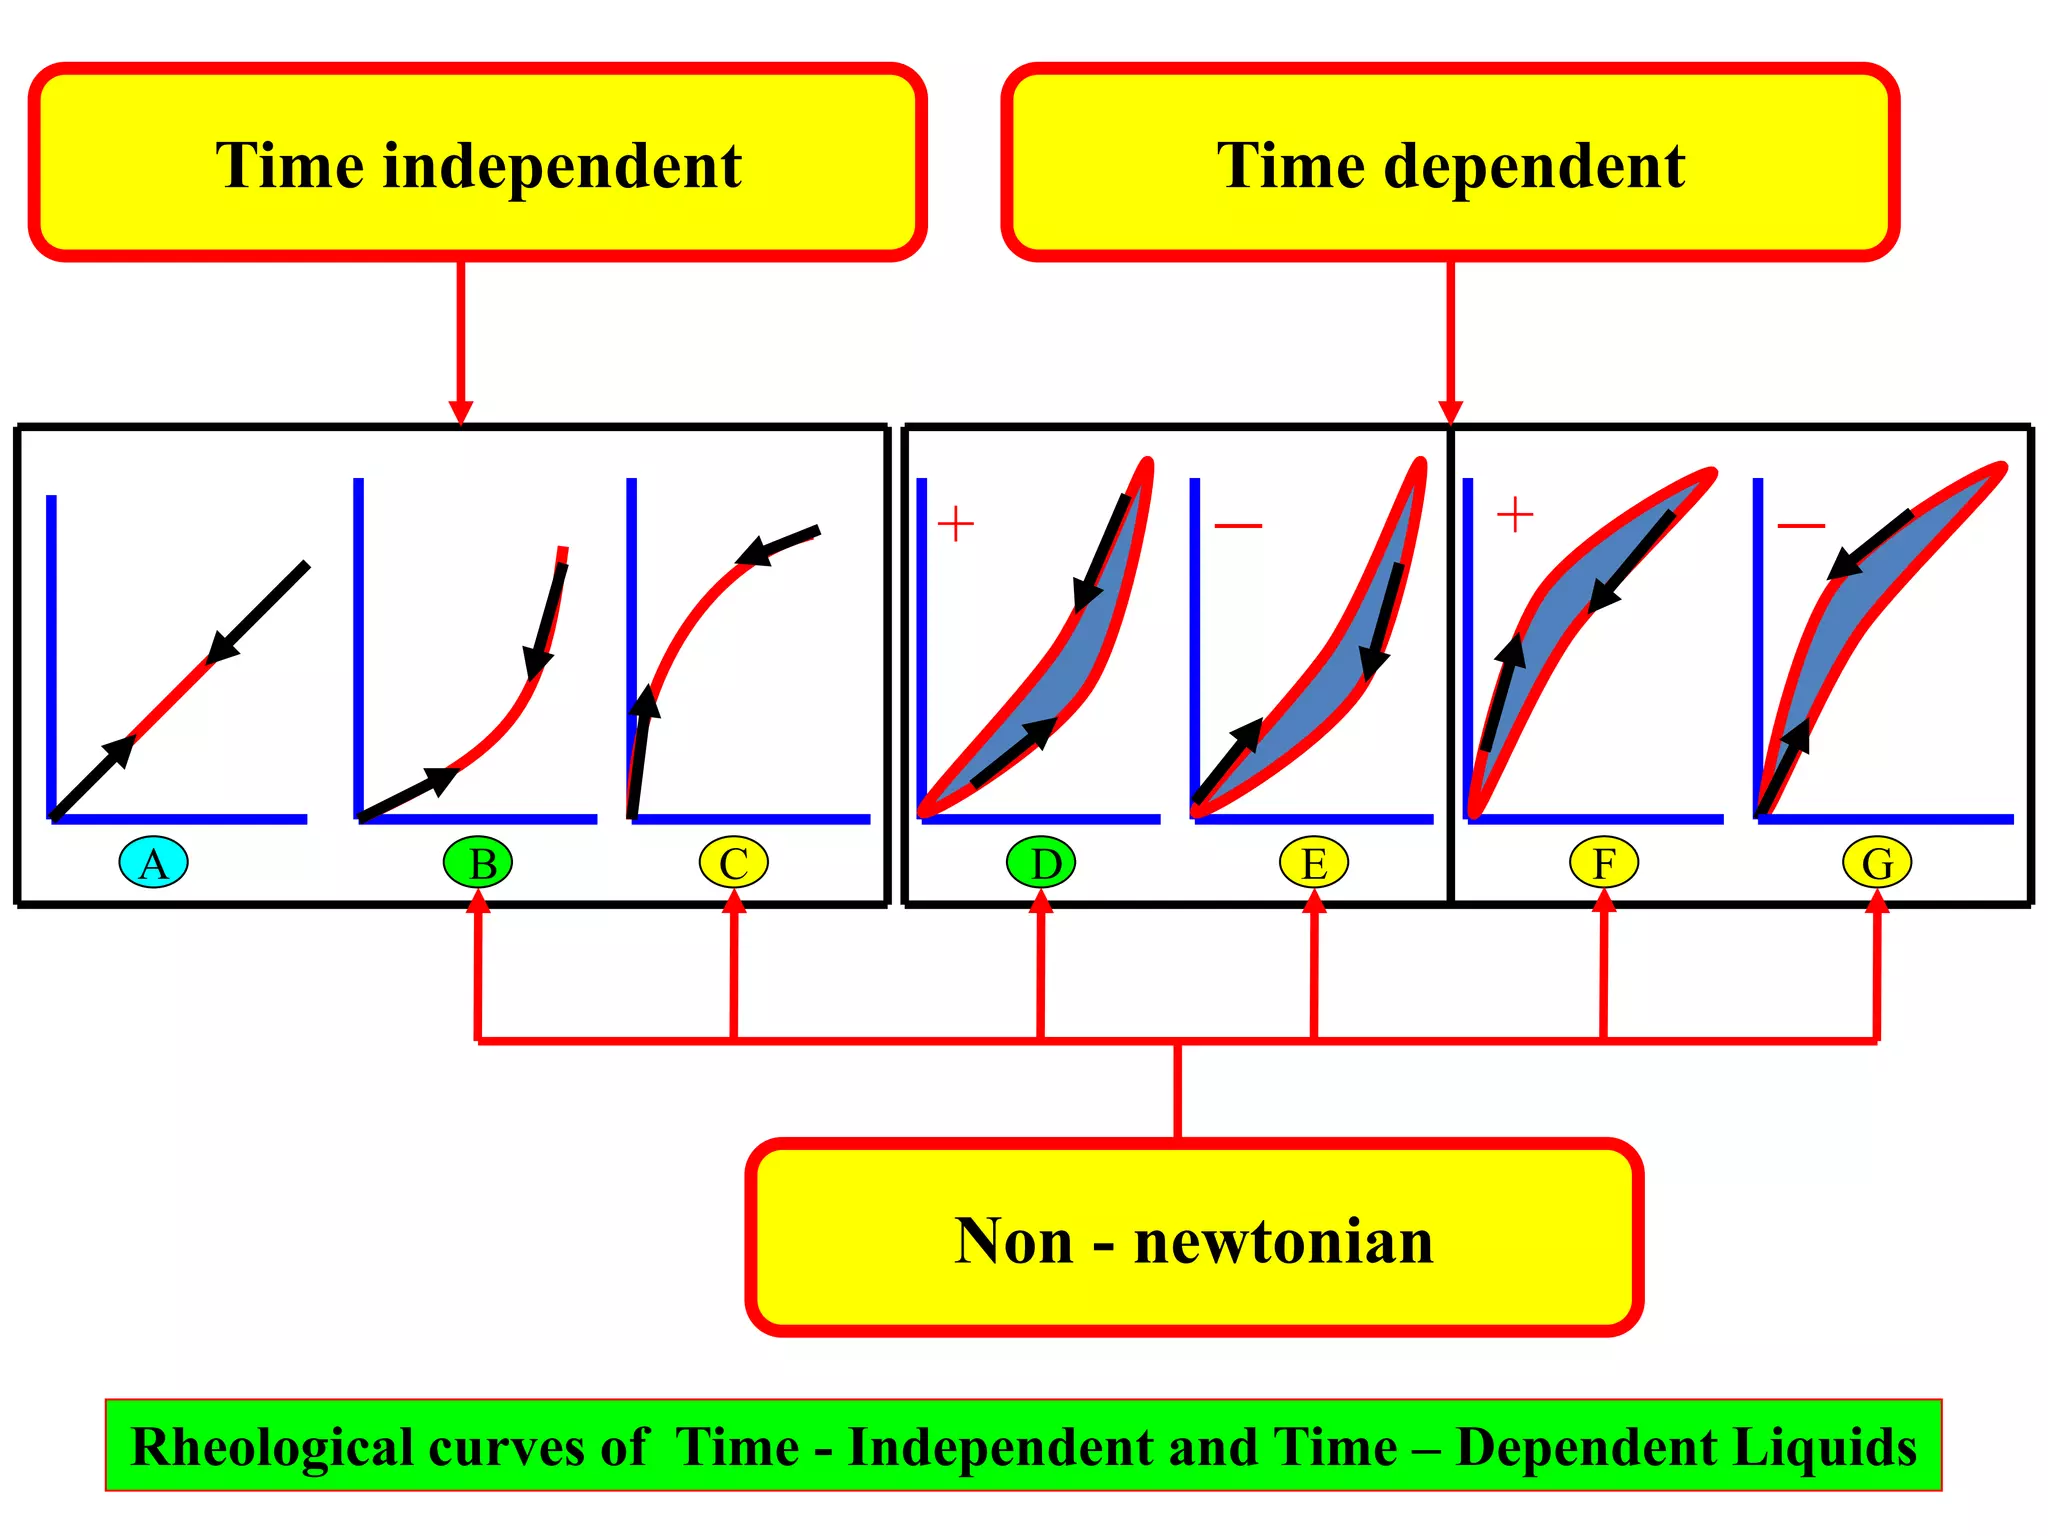
Don't skip the preliminary testing phase. Before you design any equipment or set operating parameters, run a full flow curve across the relevant shear rate range for your application. A single viscosity reading at one speed tells you almost nothing useful about a non-Newtonian fluid. I usually recommend sweeping from the lowest shear rate your process will encounter up to the highest, holding each point long enough for the reading to stabilize, and recording the temperature at every step. For thixotropic materials, do a hysteresis loop test. Shear up through your range, then shear back down while measuring viscosity at each point. If the upward and downward curves don't overlap, your material has time-dependent behavior that will affect repeatability. The area between those two curves gives you a quantitative measure of thixotropy that you can track over time and across batches. There are also free and low-cost rheology simulation tools available online if you're working with known fluid models and need to predict pipe pressure drops or mixing power requirements before building anything physical. They won't replace actual measurement, but they save time during the early design phase when you're evaluating multiple process configurations. I typically use these tools to narrow down reasonable parameter ranges, then verify with bench-scale testing before committing to full-scale equipment.
The bottom line is that non-Newtonian behavior is not theoretical overhead. It's a daily operational variable that will determine whether your process runs smoothly or fails in ways that are difficult to diagnose because the underlying fluid mechanics don't match the assumptions built into your equipment design. Measure the fluid under conditions that match your actual process, not idealized lab conditions. The difference between a working system and a broken one is usually a detail someone skipped because it felt like extra work.