Getting to Grips with the Centricut AM387 Nozzle
Most people buy replacement nozzles on auto-pilot. They check the part number against their existing one, order a box, and swap them out when the old ones start dragging through the plate. That works fine until it doesn't. I ran into a real issue last month with a batch of these Centricut nozzles on a Mark 5 that kept producing inconsistent kerf widths on 6mm mild steel. The cut quality was decent at first pass, but after about forty cuts the edge quality degraded noticeably, and I was burning through nozzles at nearly double the expected rate. Turned out the issue wasn't the nozzle itself — it was how I was seating them during installation. The Centricut AM387 is a standard pilot arc / cutting nozzle used across a range of their plasma systems. It has a 1.0mm orifice, a radius tip design, and notably no groove. That absence of a groove matters more than you'd think if you're used to working with grooved nozzles on other brands. The radius profile is meant to concentrate the arc at the tip and reduce spatter accumulation around the orifice entrance. In theory. In practice, it means you need to keep a tighter eye on stand-off distance because any variation translates directly into a wider or more ragged kerf.
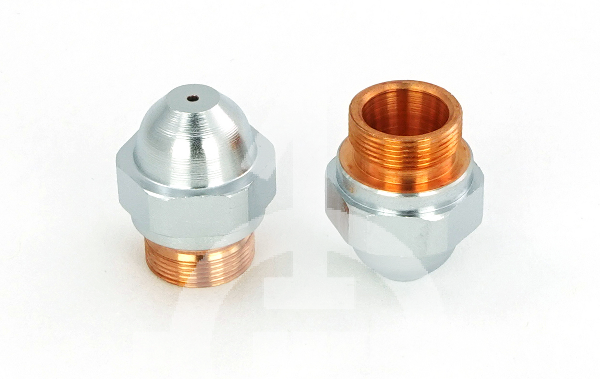
Nozzle Am387 0001 W Radius No Groove 1 0mm Centricut Original
I'll be blunt about the one scenario where this nozzle simply won't give you acceptable results: when you're cutting material thicker than about 12mm on a 45-amp system without adjusting your amperage down. The 1.0mm orifice is not designed for high amperage on thick plate. You'll get a cone-shaped cut instead of a square one, and the nozzle life drops to maybe a quarter of what it should be. For thicker work I'd switch to a larger orifice nozzle or drop to a lower amperage setting and accept the slower cut speed. There's no workaround for physics here. Here's the practical installation process. Remove the retaining cap from the torch body, take out the old nozzle, and clean the torch body seat with a brass brush. Don't skip this step — I learned that the hard way when spatter buildup inside the seat caused my new nozzles to sit at a slight angle, which ruined every cut I made for about two hours before I figured out what was going on. Wipe the seat with a lint-free cloth and a little acetone afterward. Slide the new Centricut nozzle in and make sure it sits flush. It should go in with light hand pressure. If you're forcing it, something is wrong — either the seat is dirty, or you've got the wrong part number. After installing, set your stand-off to 1.5mm to 2mm depending on whether you're running a contact tip that sits proud or flush. I use a piece of 2mm shim stock for setup and just tap the torch down onto it before engaging the arc. It takes about ten seconds and saves you from wrecking the first few cuts while you eyeball the distance. Tighten the retaining cap by hand plus a quarter turn with pliers. Not more. Over-tightening deforms the nozzle seat over time and creates the exact angle variation I mentioned earlier.
A couple of things that aren't obvious from the spec sheet. The radius on this nozzle wears faster than a straight-profile nozzle because the arc is concentrated at a single point. You'll know it's wearing when your pierce time starts increasing — that's the radius flattening out and the arc spreading instead of staying pinpointed. When that happens, replace it. Trying to run it past that point just burns up your consumables faster overall. The second thing: these nozzles are not interchangeable with grooved versions on the same torch body. Some people try to mix them, thinking the groove is just a minor detail. It isn't. The groove provides a seating surface and alignment feature. Without it, the nozzle can rotate slightly under vibration, which causes uneven wear and poor cut quality within minutes. I also want to mention the cost aspect. A single Centricut AM387 nozzle runs somewhere in the £8 to £12 range depending on supplier and quantity. That's not cheap for a consumable, but it's also not the most expensive option on the market. The real cost driver is how quickly you're destroying them through improper setup. I've seen people go through a box in a week on a machine that should easily get three weeks out of the same box when run correctly. The difference almost always comes down to one of three things: dirty torch seats, incorrect stand-off distance, or using the wrong amperage for the material thickness. If you're running high-volume production work on mild steel under 10mm, this nozzle will serve you well. For aluminum or stainless, the same rules apply but expect roughly 20 to 30 percent shorter nozzle life due to the different thermal properties. And if you need something for thicker plate, look at the larger orifice options in the Centricut range instead of trying to push this one beyond its design parameters.
Get the Full Details