Working With Press Brake Manuals: What Actually Helps
The Pacific Press Brake Manual covers everything from basic bending sequences to offset calculation adjustments and ram parallelism checks. Most operators never read past the first few pages, then spend three hours on the floor trying to figure out why their bend angle is drifting two degrees off program every seventh part. I've seen it happen. The manual has those answers, but they're buried under layers of generic warnings and diagrams that assume you already know the difference between a back gauge finger and a crown adjustment. I remember one job where we were running 14-gauge cold-rolled steel at 90-degree angles across a full-width bend. The setup felt fine. First ten parts looked good. Then the angles started opening up on the right side only. I pulled the Pacific Press Brake Manual from the binder clipped to the machine, flipped to the section on tooling deflection compensation, and cross-referenced it with the cumulative tonnage chart. The problem wasn't the machine. It was that we'd switched to a different die without updating the V-die width parameter in the control system, which threw off the whole springback curve. Took about twelve minutes once I knew where to look.
Pacific Press Brake Manual Navigation
Here's how to actually use this thing instead of treating it like doorstop. Start at section 4.2 on initial calibration before touching anything else. Most shops skip straight to the bending tables because they're in a hurry, and that's where things fall apart within the first shift. The calibration routine takes about forty-five minutes. Doing it right means the subsequent tables actually mean something when you reference them later. The tonnage charts in chapter 6 are useful but come with a caveat most people miss. They assume ambient temperature stability and clean, undamaged tooling. If your lower die V-opening has nicks or your upper tooling isn't seated flush, those numbers become suggestions rather than constraints. I measured my die V-edges with a go/no-go gauge once and found wear on two out of three dies. The manual mentions this in passing around page 89 but doesn't emphasize it enough. Tooling wear changes your required force by roughly eight to fifteen percent depending on severity, and the tonnage tables don't account for that automatically. When you get to the bending sequence section, pay attention to the part ordering guidelines before committing to a program. There's a subsection about sequencing bends to avoid tooling collisions that I see people ignore constantly. I had a part where we tried to do the second bend before the third was fully clear of the upper tool, and the CNC didn't catch it because the step sequence wasn't flagged properly in the program. Destroyed a $400 punch tip in about three seconds. The fix was going back through the manual's collision geometry diagrams and reordering the bend sequence to give clearance. Added maybe five minutes to programming but saved us a full day of downtime.
The troubleshooting section at the back is the least polished part of the manual. It reads like someone compiled a list of complaints from the field without much editing. The entry on inconsistent bend angles covers six different root causes but buries the most common one — back gauge repeatability drift — behind less likely culprits like hydraulic temperature fluctuation. Check your back gauge positioning first. Run the same part twenty times and measure the variation. If it's beyond .005 inches, before you start adjusting pressure settings or die selection, fix the gauge. One thing the manual doesn't address directly but you should know: the bend allowance tables are calculated for mild steel at room temperature. When you move to stainless or harden aluminum, you're looking at different springback characteristics that the standard tables won't cover accurately. I keep a separate reference sheet taped near the control panel with adjustment multipliers for the common alloys we run. Stainless usually needs about four degrees of overbend compared to mild steel at the same material thickness. The Pacific Press Brake Manual will tell you to use the tables as a starting point, but starting point doesn't mean close. You'll still need to dial in each material batch individually because temper variations between lots affect results more than the manual acknowledges. If your manual is missing pages or has handwritten notes all over it from three different operators with different pen colors, that's a real problem. Incomplete documentation leads to inconsistent practices across shifts. I'd recommend scanning whatever version you have and keeping a clean digital copy alongside the physical one. Takes twenty minutes and saves an afternoon of argument when shift B claims the setup was done correctly according to the binder version they can barely read.
Get the Full Details
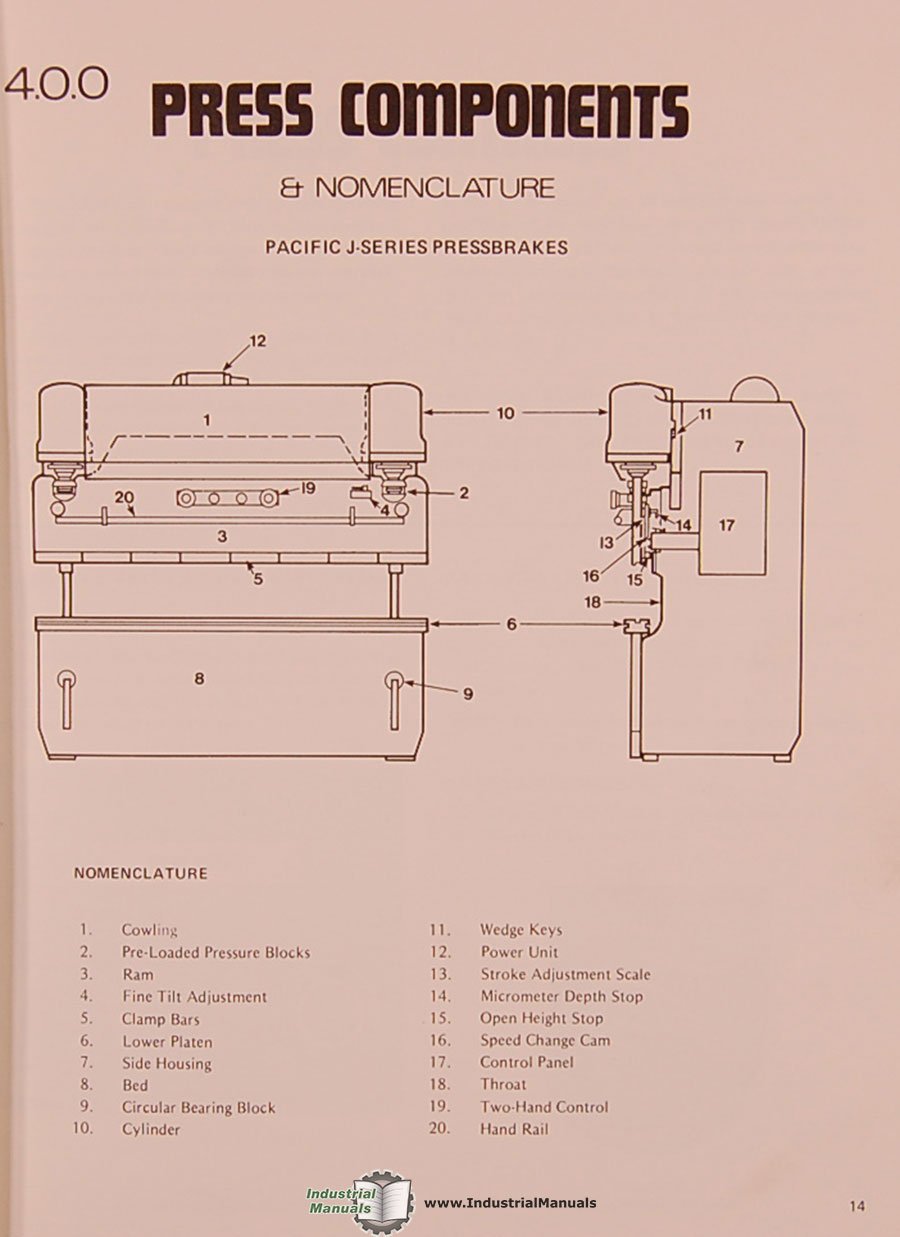
The maintenance schedule in appendix C is where people cut corners. Skipping the biweekly ram parallelism check seems harmless until you're running tight-tolerance work and wondering why the left side is consistently half a degree off from the right. That check takes about six minutes with a dial indicator. Do it on a Monday morning before the shop gets busy and you won't have surprises by Wednesday afternoon. There are also cases where the manual simply won't help you. If you're working with unusual material combinations, non-standard tooling configurations, or bending sequences that require custom tool paths outside normal parameters, you're going to need to rely more on experience and trial than on the published tables. The manual covers standard operations well. Outside those boundaries it becomes a reference rather than a complete guide. That's honest to say because I've seen people try to force the manual to cover situations it wasn't designed for and end up with scrapped parts and frustrated operators. Keep a logbook next to the machine. Record material lot numbers, tooling used, tonnage applied, and actual versus programmed angles for the first five parts of every setup. After a week you'll have data that's more useful than any static table in the manual. The patterns show up quickly when you actually track them instead of just hoping the book tells you the right settings.