Breaking Down What Actually Makes A Needle
You pick up a needle and look at it. Most people see a thin metal spike. That's not enough if you're trying to pick the right one for a job or troubleshoot why your stitching keeps failing. The anatomy is specific and each part has a function that matters. I spent years dealing with needle-related failures in technical sewing — everything from aerospace composites to medical device assembly. The difference between a clean job and a ruined batch often comes down to understanding these components rather than just grabbing whatever fits in the machine. Here's what you're actually looking at when you inspect one.
Parts Of A Needle Explained
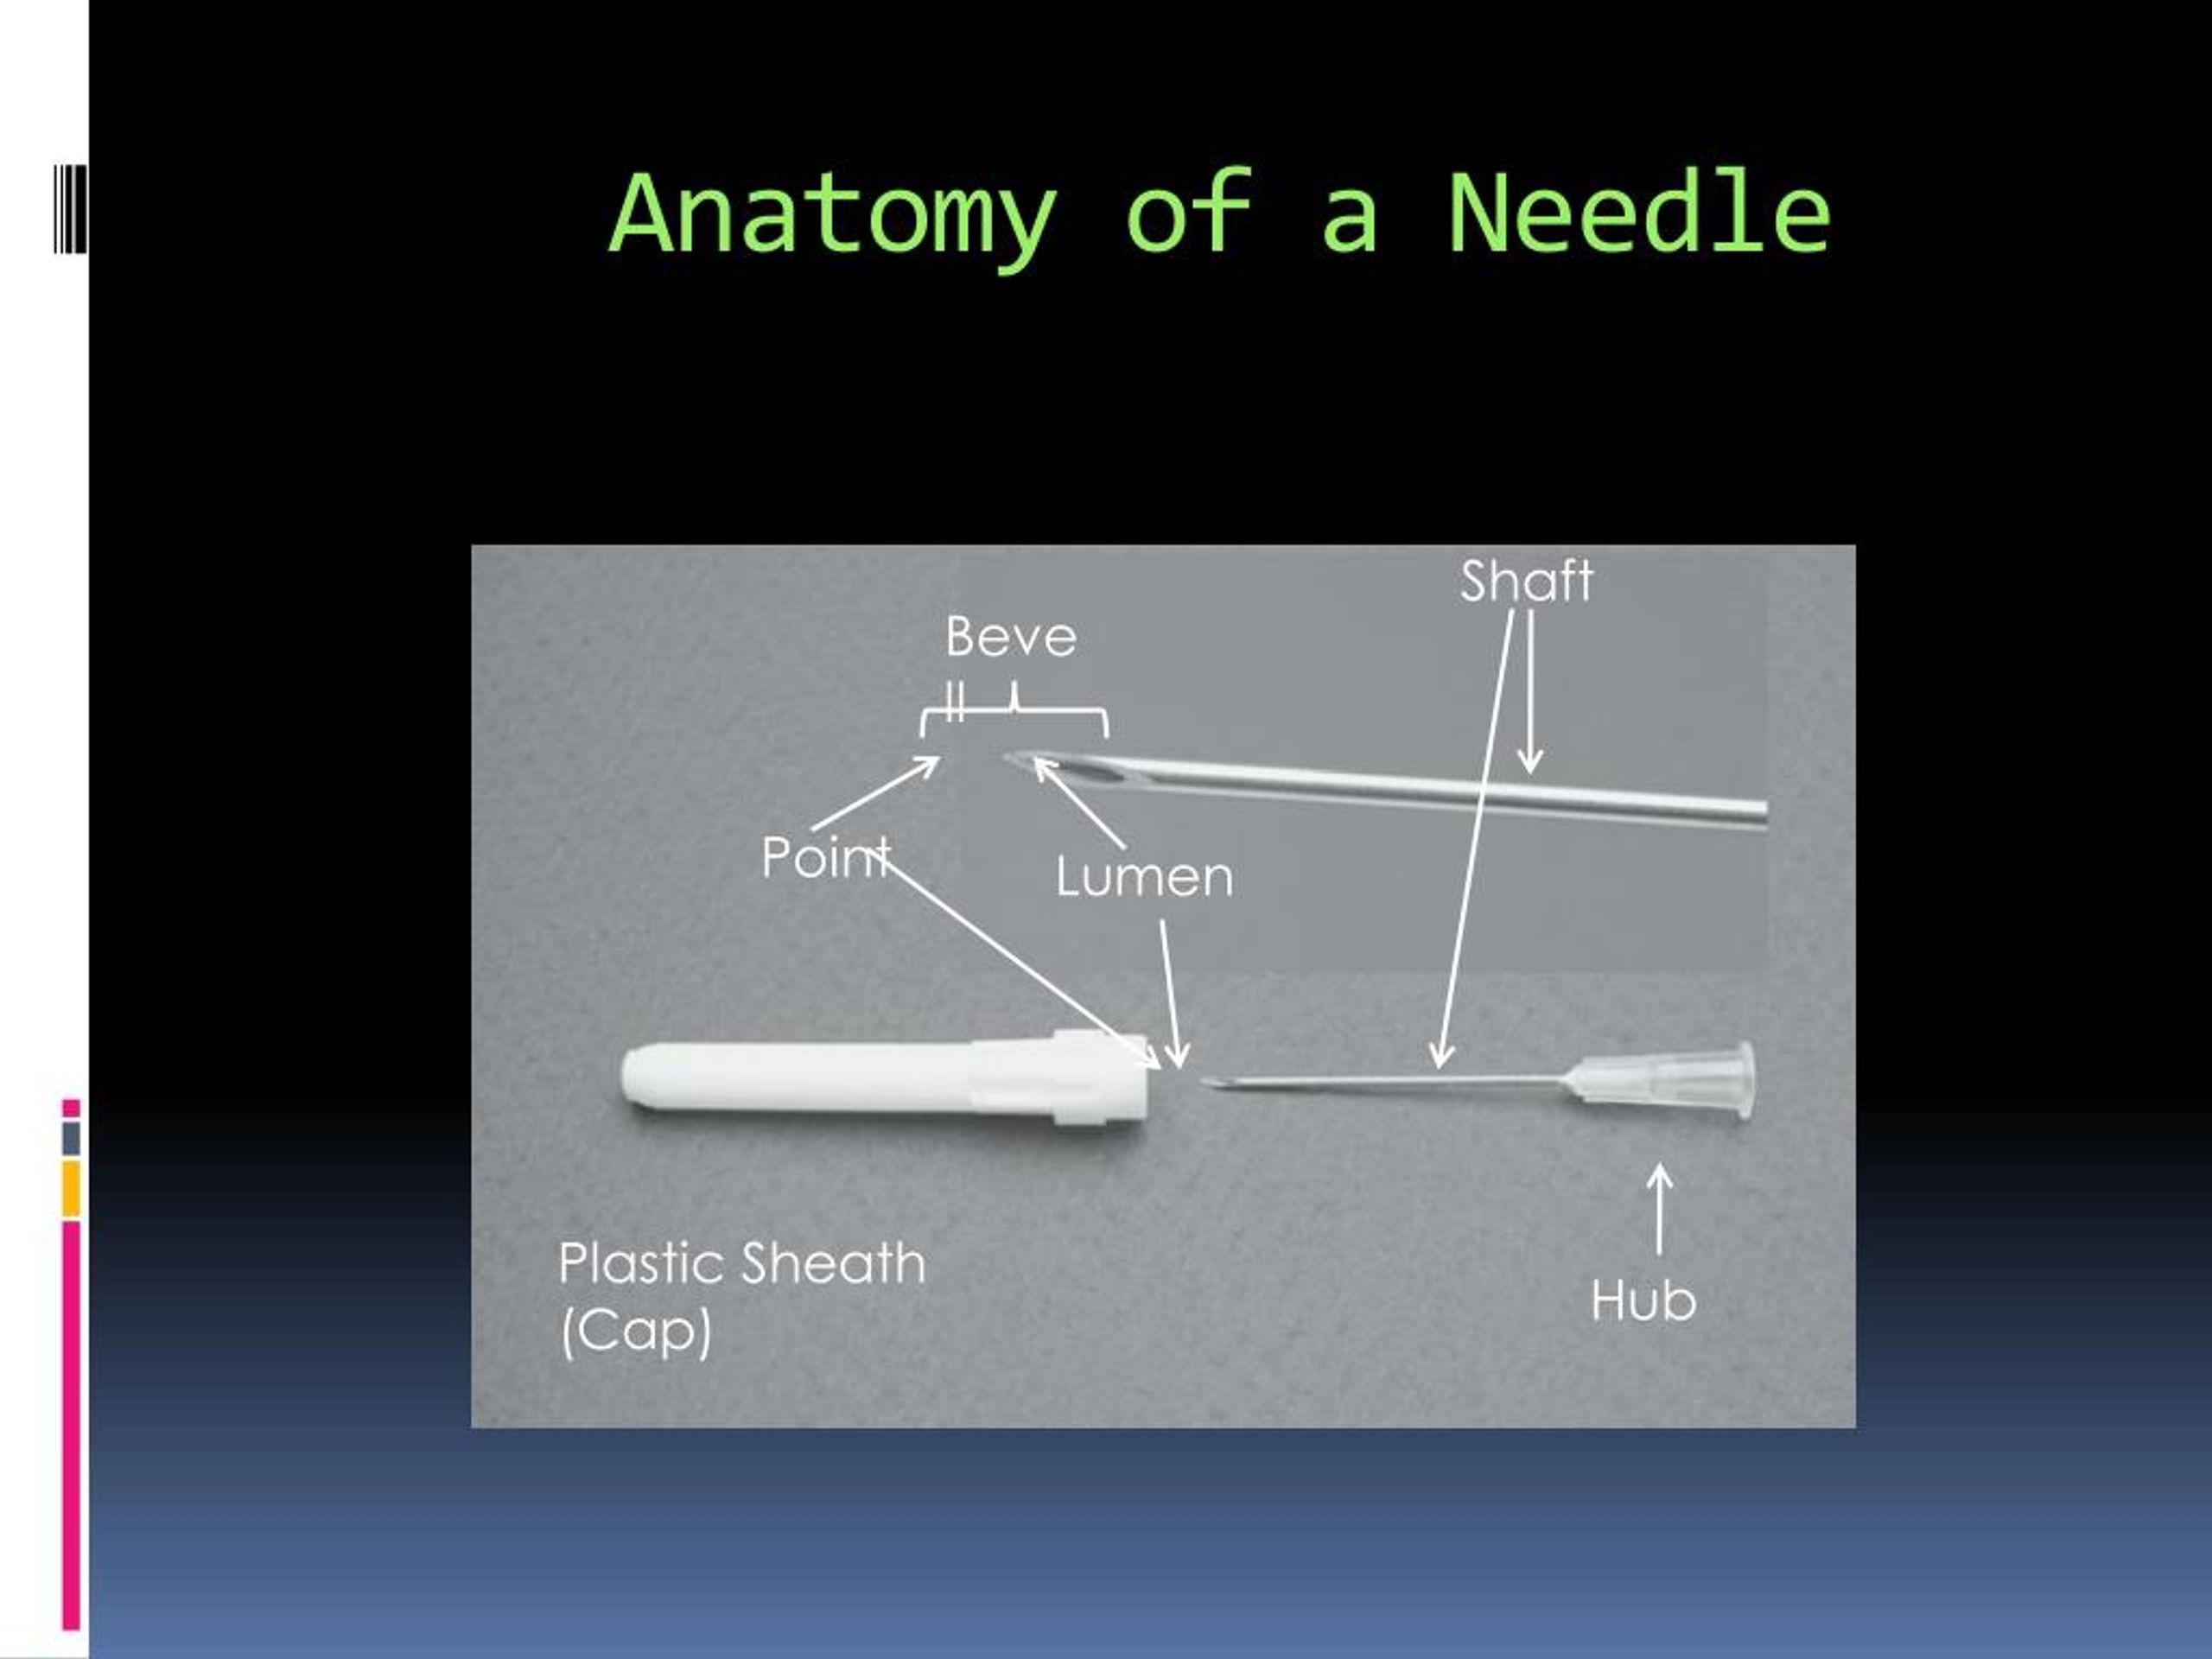
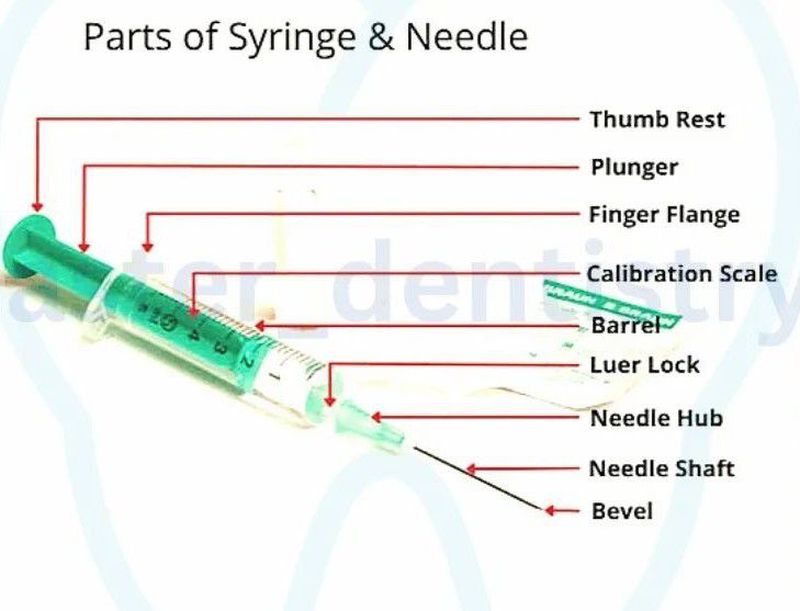
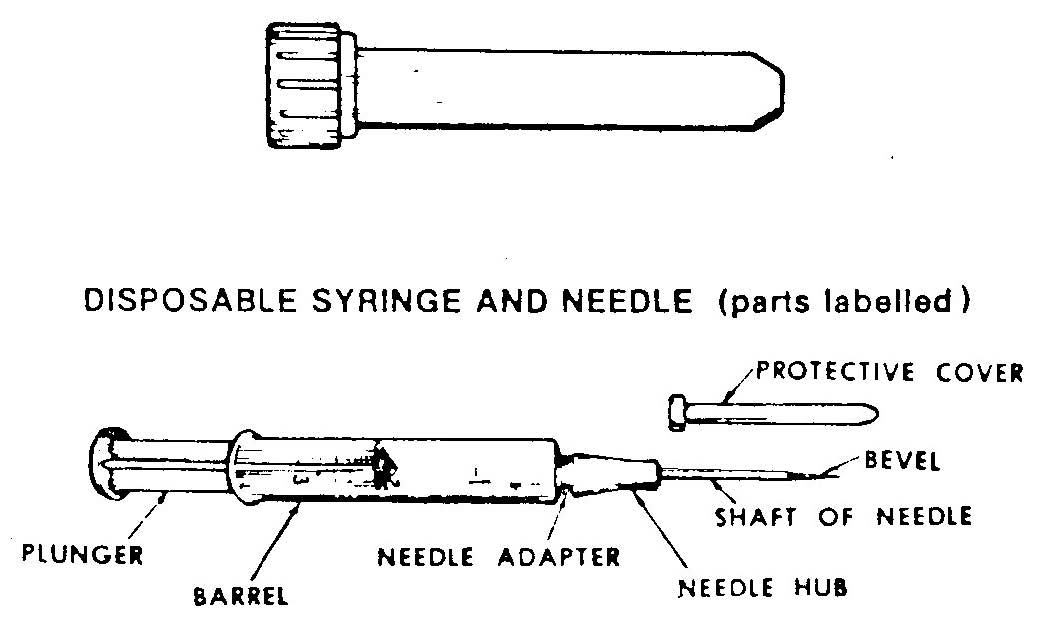
The point is the business end. It determines how the needle enters your material. There's a reason a needle for leather looks completely different from one meant for silk, and it all starts at the tip. A cutting point slices through dense fibers. A ballpoint pushes them aside instead. Wedge points exist for specialty applications like neoprene and certain synthetic fabrics. Using the wrong point type on a material is one of the fastest ways to get skipped stitches or material damage, and people don't always catch it because they're focused on thread or tension instead of what's actually piercing the fabric. Just behind the point is the shank, which is the thicker unground portion that sits inside your sewing machine or holding fixture. The shank's job is simple — secure the needle in place. But the geometry matters. Standard industrial machines use a specific shank profile. Domestic machines use another. Mixing them up obviously won't work, but even within those categories there are variations. I once spent three hours chasing a timing issue on a Juki before realizing the replacement needle had a slightly different shank dimension than the original. The needle was the same length and fit visually, but the shank was off by fractions of a millimeter. It threw the entire hook timing off. The scarf is the indented area on the backside of the needle just above the shank. This one gets overlooked constantly. The scarf creates a gap that allows the hook or looper to pass close enough to catch the thread loop. Without a properly sized scarf, the hook can't form a stitch. In high-speed industrial operations, an insufficient scarf is a leading cause of broken thread and missed stitches. You won't know it's wrong until your machine is running and failing repeatedly. Inspecting the scarf against a known-good needle under magnification will usually confirm it quickly enough.
Beneath the point you have the eye. The eye's dimensions — its length, width, and shape — determine what thread size you can run through it. A needle with an oversized eye reduces friction on the thread but weakens the needle shaft. A needle with a tight eye protects the shaft but can shred delicate threads at high speeds. There's a tradeoff built into every design choice here. I've seen production lines running polyester topstitch thread through needles that were too narrow, resulting in consistent thread breakage that everyone blamed on the thread quality. It wasn't. The needle eye was undersized for the thread diameter. The shaft runs from the eye down to the point and its diameter tapers depending on the needle type. Some needles maintain a consistent diameter through most of their length. Others taper significantly. The taper affects rigidity and flexibility. A stiffer shaft resists deflection but can bend or break under lateral load. A more flexible shaft absorbs some of that force but may wander slightly during penetration, affecting stitch placement accuracy. This becomes critical when you're working with layered materials or thick stacks where the needle experiences side loading as it pushes through. Then there's the groove, the channel cut along one or both sides of the needle between the eye and the point. The groove guides the thread and reduces friction as the needle retracts. A deeper groove handles heavier threads better. Shallow grooves are fine for fine threads but become a bottleneck with anything substantial. In my experience with heavy upholstery work, switching to needles with deeper longitudinal grooves eliminated about seventy percent of our thread friction issues without changing anything else on the machine.
Get the Full Details
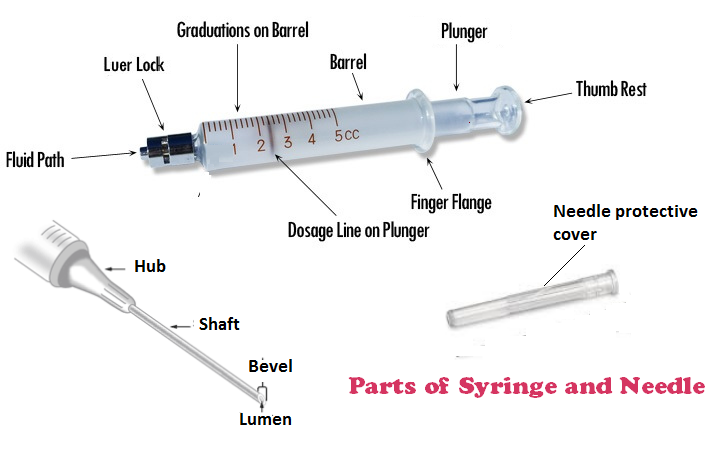
The flat side of the shank is another detail that matters more than people give it credit for. Most industrial needles have a flattened section on the shank. This flat serves as a key — it ensures the needle installs in the correct rotational orientation. Get the orientation wrong and the scarf won't align with the hook path. The needle might physically fit into the clamp, but it won't form stitches. I've found that the quickest way to identify whether a needle is seated correctly is to verify the flat aligns with the corresponding ridge in the needle clamp before tightening. Some needles include a heel, a slightly widened section between the shank and the shaft. Not all needles have one, but when they do, it adds marginal strength at a stress-concentration point. In high-vibration environments or when running at extreme speeds, the heel can make the difference between a needle that lasts a full shift and one that fatigue fractures partway through. When you're selecting or troubleshooting needles, start with the point type and work your way up through the other features. Most failures trace back to one of these components being mismatched to the application. The needle is a precision tool, not a generic fastener. Treating it like one is why people constantly blame their thread, their tension settings, or their machine timing when the real problem is sitting in their needle case.