Understanding the Pb Sn Phase Diagram
The Pb Sn Phase Diagram is one of those things every soldering engineer and materials scientist learned but few actually understand deeply. It shows how lead and tin behave when mixed together, and it is deceptively simple at first glance. The diagram plots temperature against composition, revealing solid, liquid, and mushy zones that determine everything from solder joint quality to casting defects. I spent three years debugging inconsistent solder joints on prototype boards before I actually sat down and read the phase diagram properly instead of relying on trial and error. The problem was not with my technique or equipment. It was that I did not understand what was happening microstructurally during cooling. Once I mapped my process against the actual phase relationships, most issues vanished within a week.
Reading a Pb Sn Phase Diagram Correctly
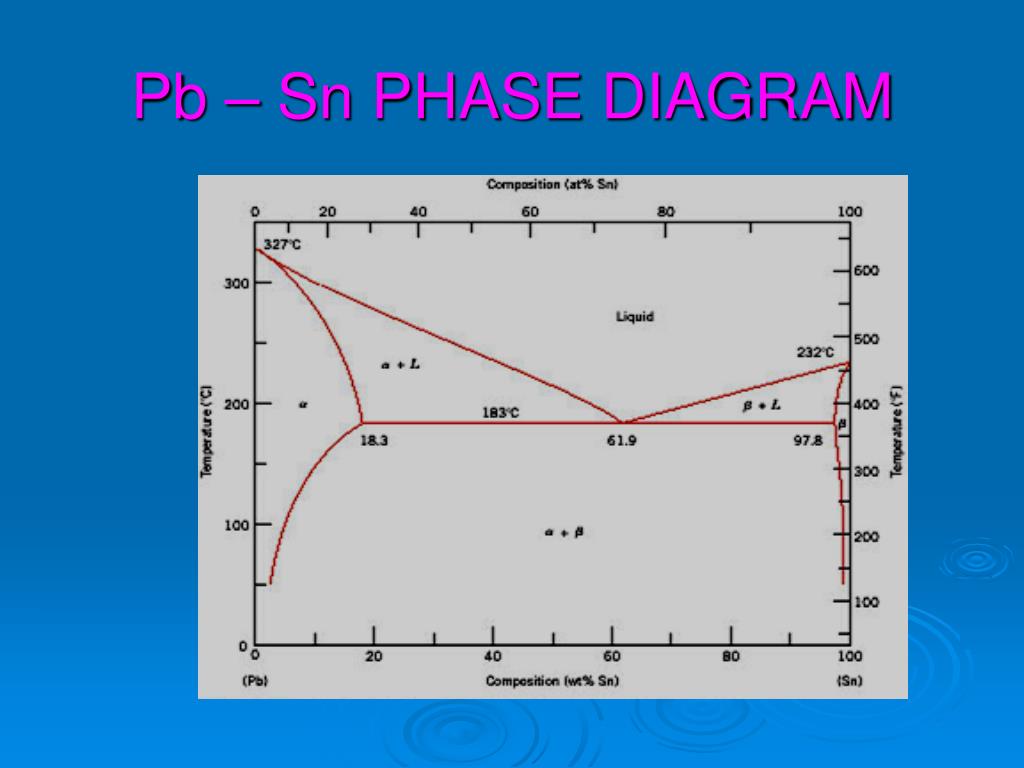
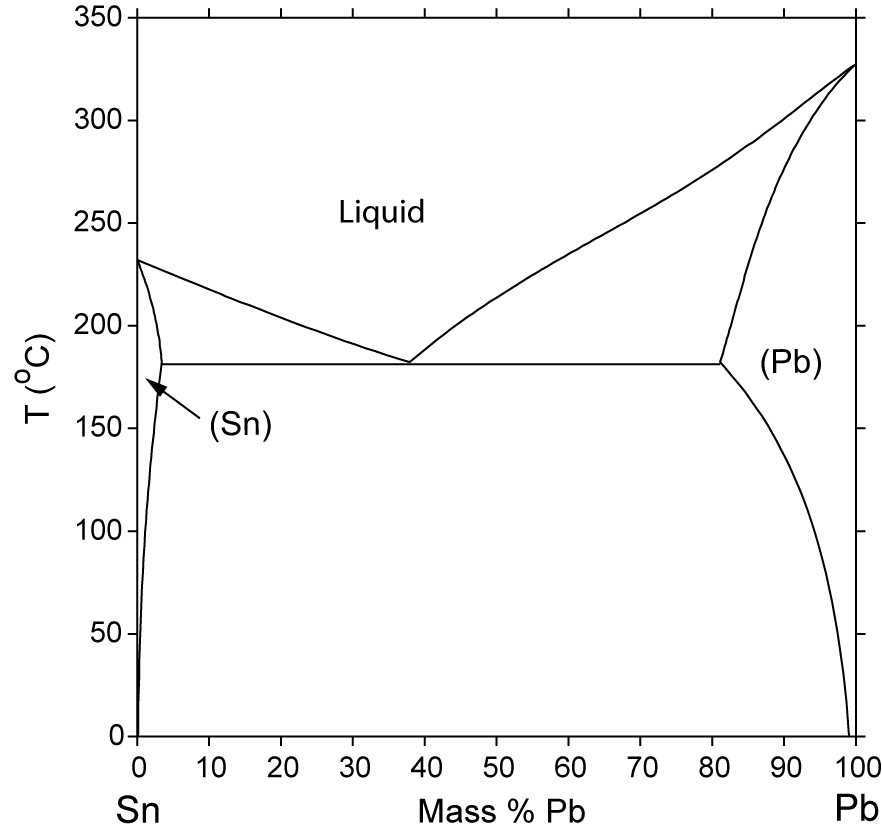
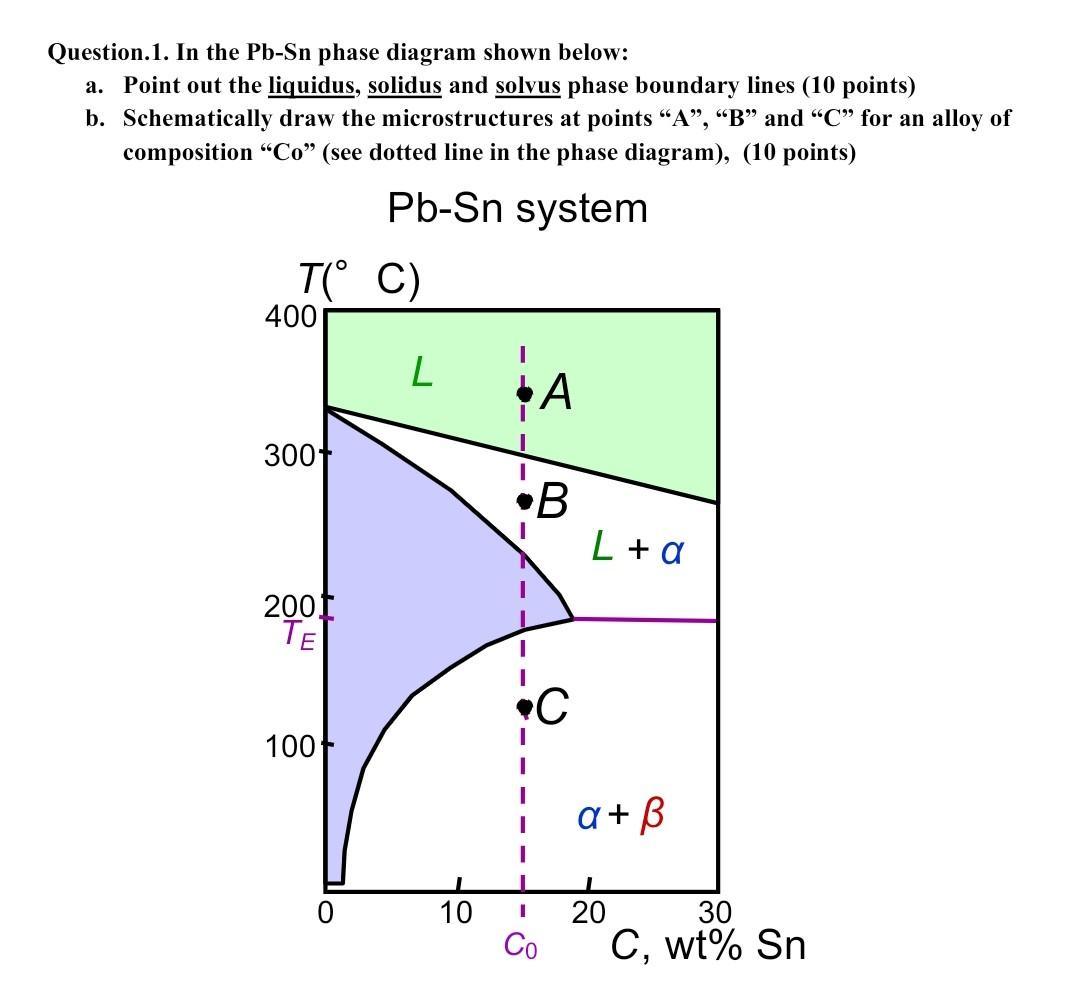
The diagram has two liquidus lines meeting at a eutectic point around 183°C with a composition of roughly 61.9% tin and 38.1% lead by weight. Below that line you enter the solid solution region where alpha lead-rich and beta tin-rich phases coexist. Between the liquidus and solidus lines lies the notorious mushy zone where partial melting occurs. This is where most soldering problems originate. The eutectic composition is critical because it melts and solidifies at a single temperature rather than over a range. When you use 60/40 solder, you are not at the eutectic point. You will see dendritic solidification as the alloy cools through the mushy zone. This creates weak joints prone to cracking under thermal cycling. I learned this the hard way when a batch of assembled boards failed vibration testing after just two thermal cycles between -40°C and +85°C. The solid solubility limits are often overlooked. At room temperature, lead can only dissolve about two percent tin, and tin can dissolve roughly five percent lead. This means even supposedly homogeneous solder joints actually contain separate lead-rich and tin-rich regions after solidification. These regions have different thermal expansion coefficients, which generates internal stresses during temperature changes. That is why old leaded solder joints sometimes develop cracks decades later even without mechanical stress.
Practical Implications for Soldering
When you heat a solder joint above the liquidus temperature, the entire mixture becomes liquid. During cooling, the first solid to form depends on the composition. For hypoeutectic alloys like 60/40 tin-lead, pure tin-rich dendrites nucleate first along the solidus line. These dendrites grow as temperature drops, consuming tin from the remaining liquid. The liquid composition shifts toward the eutectic point until the remaining material solidifies at 183°C as a fine lamellar structure. The cooling rate dramatically affects microstructure. Fast cooling produces finer dendrites and a finer eutectic structure. This generally improves joint strength and fatigue resistance. Slow cooling allows larger dendrites to form, which can reduce mechanical properties. In practice, typical PCB reflow profiles cool at around 2-4°C per second, which gives a reasonable balance between joint strength and production throughput. One counter-intuitive point that beginners miss is that overheating solder does not necessarily improve wetting. Once the solder is liquid, holding it at high temperature can actually promote intermetallic compound formation at the interface with copper pads. This consumes copper from the substrate and creates brittle Cu6Sn5 and Cu3Sn layers. I once spent two days investigating poor bond strength on gold-plated connectors only to discover that my rework iron was sitting at 400°C for extended periods, growing excessive intermetallics that cracked under minimal stress.
Get the Full Details

Common Pitfalls When Working With Pb Sn Alloys
Tin whisker growth is rarely an issue with leaded solder because lead inhibits whisker formation. This is one reason the industry is reluctantly returning to lead despite environmental concerns. The European Union mandated lead-free solder under RoHS, but many aerospace and medical applications still qualify for exemptions. Lead-free alternatives like SAC305 require higher processing temperatures around 217-220°C and do not wet as reliably. Composition control matters more than most people realize. Commercial solder wire often has a tolerance of ±0.5% on the tin content. If you are making custom solder batches, measuring composition by melting point determination can verify the alloy. The eutectic composition melts sharply at 183°C, while off-eutectic alloys show a distinct pasty range during heating. There are scenarios where the Pb Sn system simply does not work. Aluminum substrates cannot be soldered directly with tin-lead alloys because aluminum forms a refractory oxide that prevents wetting. You would need a specialized flux with strong reducing agents or a nickel barrier layer. Silver-bearing solders like Sn62Pb36Ag2 improve wetting on difficult substrates but increase cost without significant benefit for standard PCB work.
The diagram also reveals why lead contamination in lead-free systems is problematic. Even trace amounts of lead below one percent can form low melting eutectics that weaken joints at elevated temperatures. I have seen circuits fail unexpectedly when lead-contaminated solder paste from previous processes created liquid films at just 150°C during normal operation. This is why dedicated production lines for lead-free solder require thorough cleaning between material changeovers. Understanding the Pb Sn Phase Diagram fundamentally changes how you approach soldering problems. Instead of adjusting temperature and time arbitrarily, you can predict what microstructure will form and whether it will survive your application conditions. The diagram does not solve every soldering issue, but it eliminates guesswork for most common alloys and processes.
Resources and Further Reading
ASM International publishes comprehensive phase diagram databases that include the tin-lead system. The Binary Alloy Phase Diagrams book by Massalski remains the standard reference despite being published decades ago. Many universities offer interactive phase diagram simulators that allow you to trace cooling paths and predict microstructures in real time. For practical soldering guidance, IPC standards like J-STD-001 provide qualification requirements based on phase diagram principles. The Society for Soldering Technology offers workshops that cover both theory and hands-on practice. Online forums like EEVblog have extensive discussions about real-world soldering problems and solutions from experienced practitioners.