Understanding the Phase Diagram Of Iron Carbon
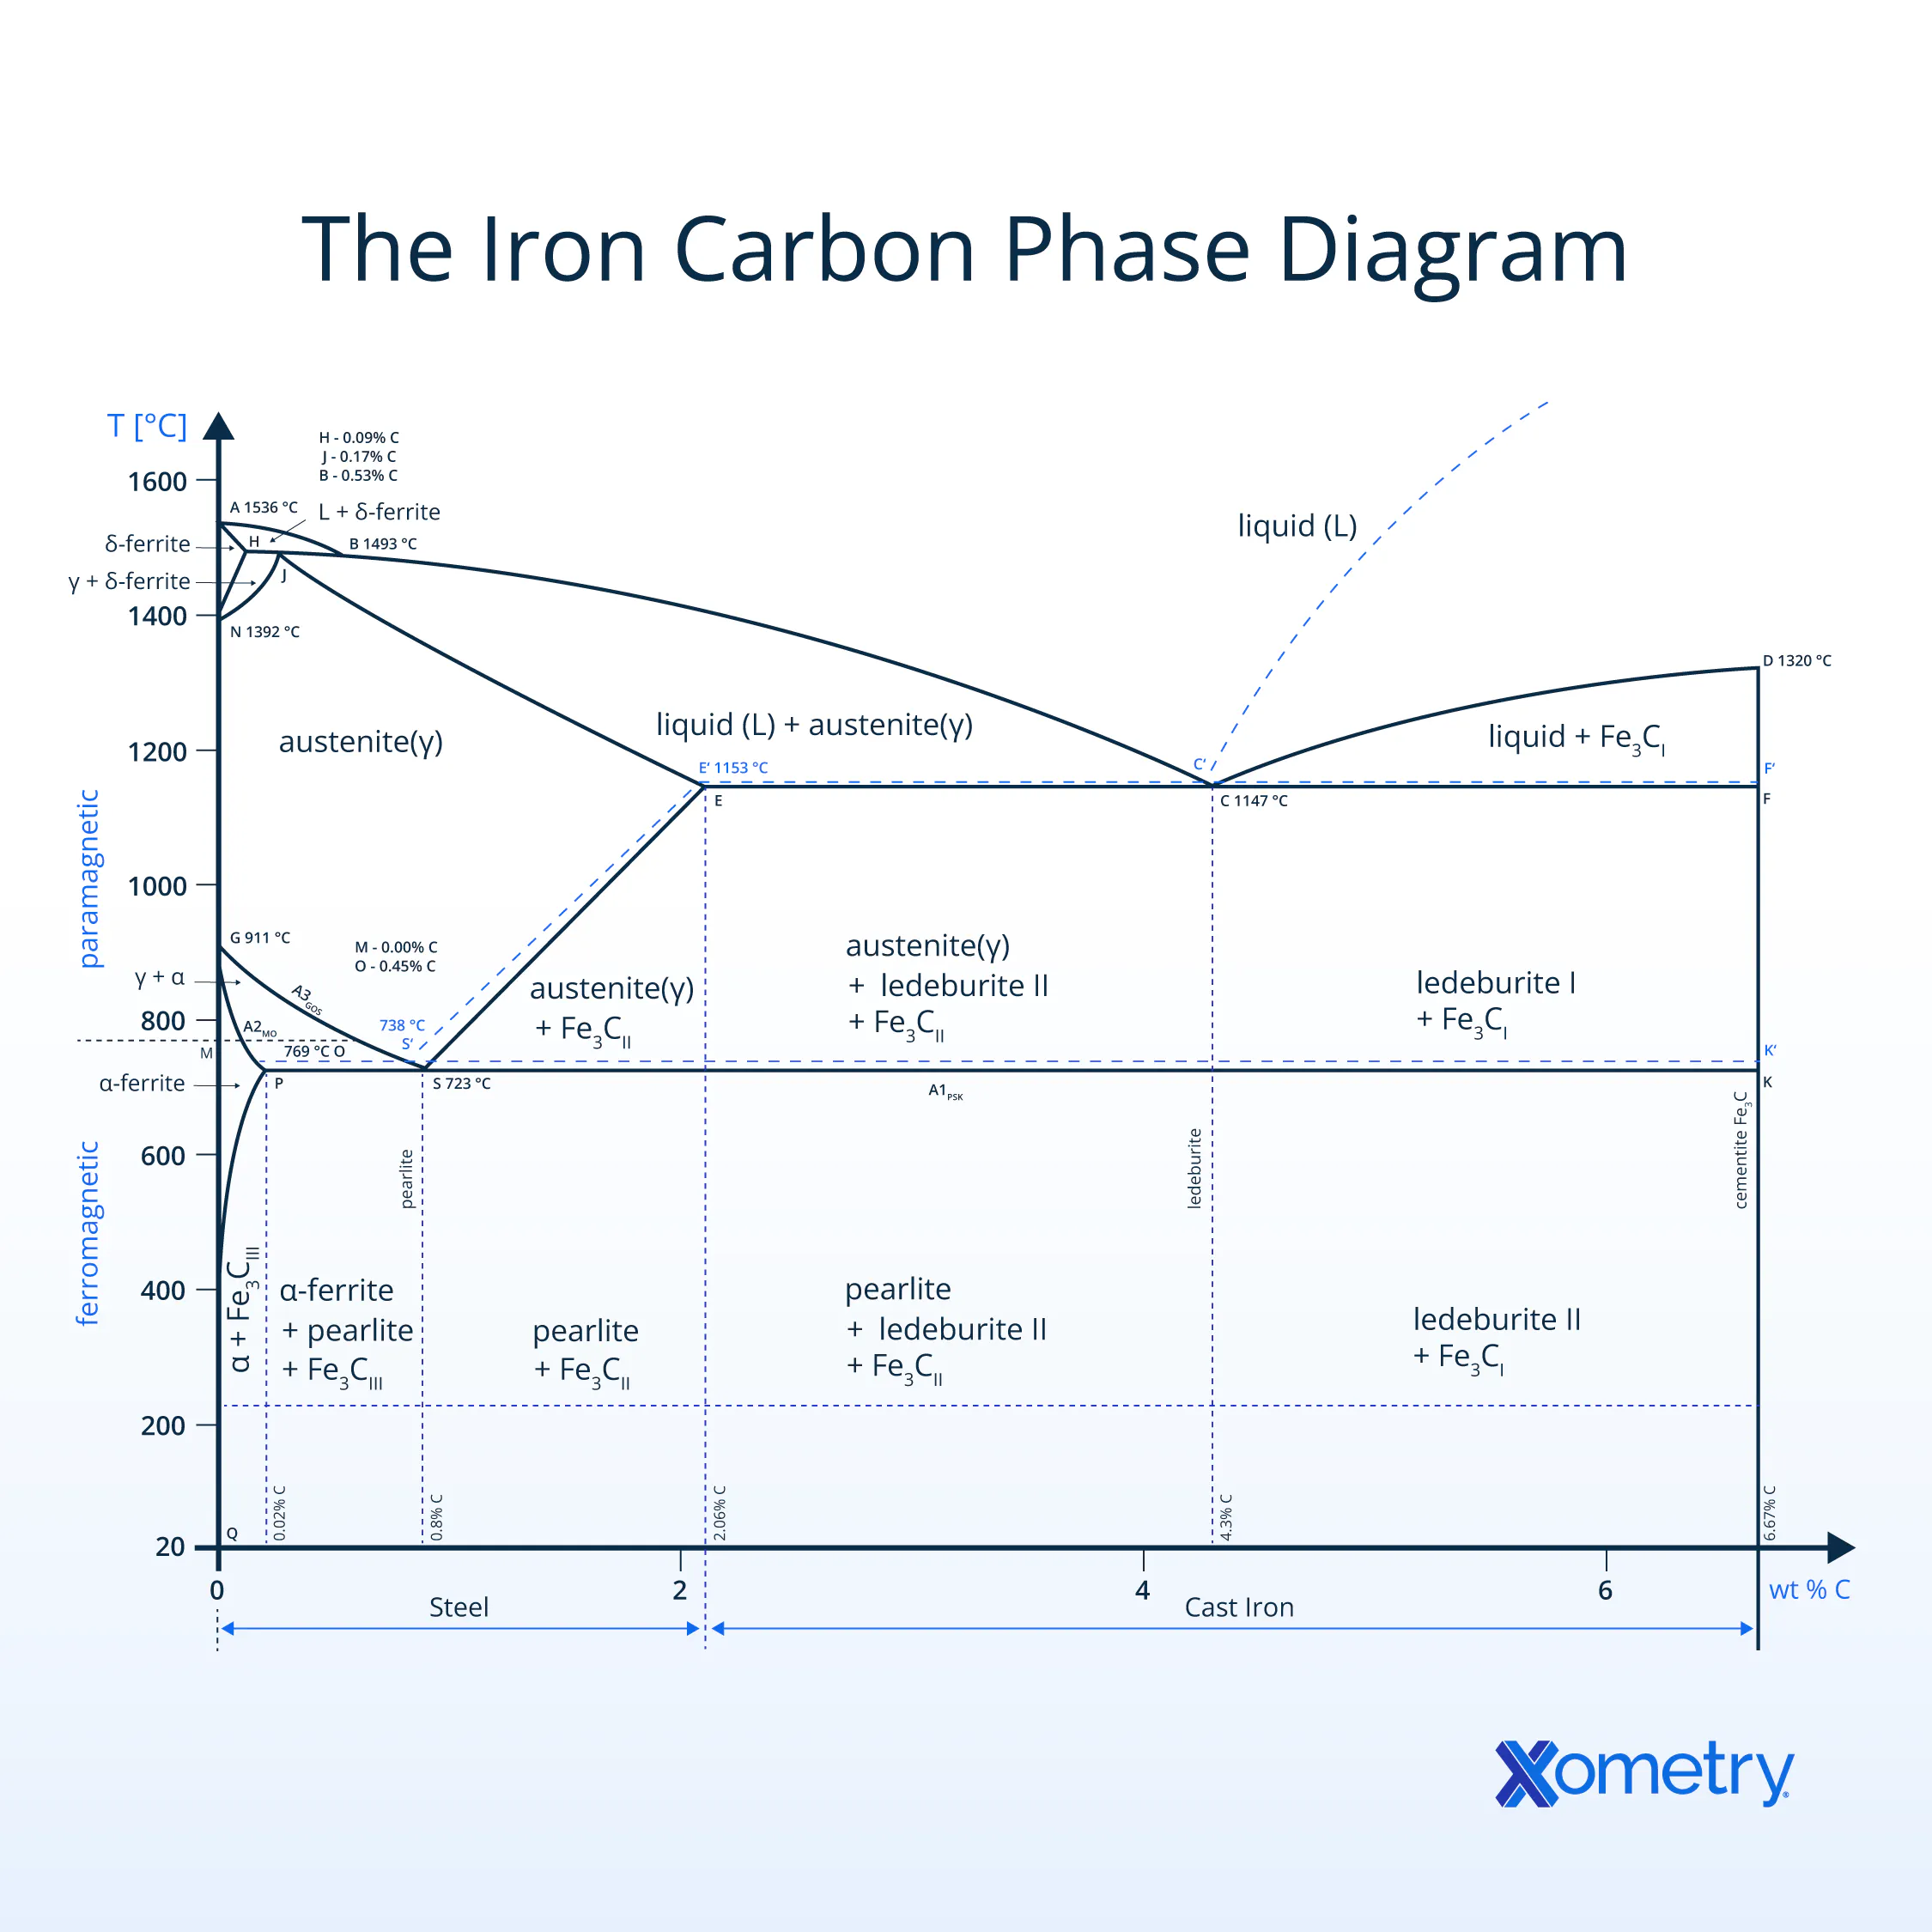
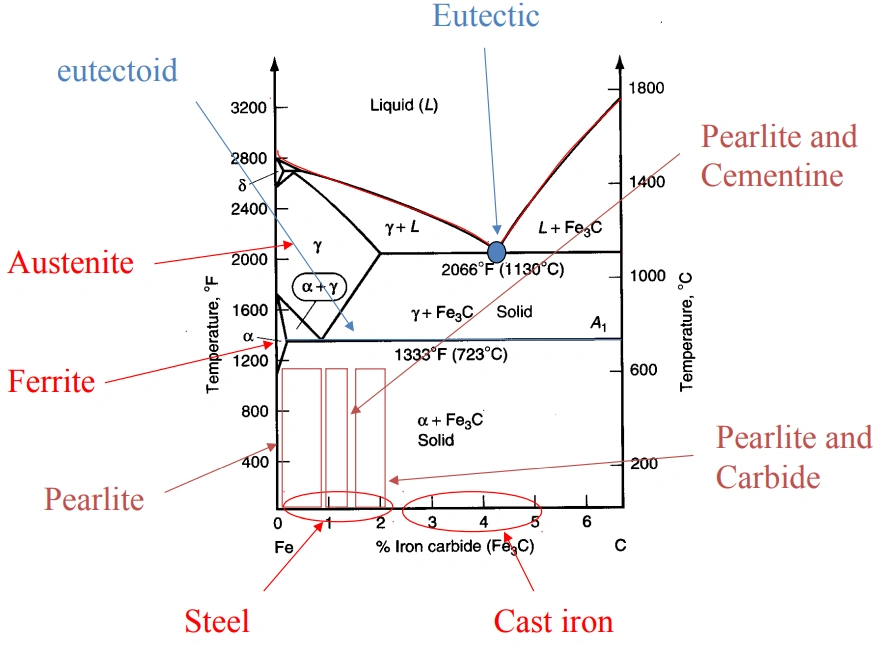
The iron-carbon phase diagram is one of those foundational tools that looks straightforward until you actually need to use it for something real. It maps out what phases exist in an Fe-C alloy at different temperatures and carbon concentrations, typically shown from 0 to about 6.67% carbon, which is the stoichiometric ratio for Fe3C, cementite. Most textbooks stop there, but the practical world doesn't always cooperate with textbook boundaries. At room temperature, a plain carbon steel with less than 0.022% carbon is almost entirely ferrite, a BCC structure that's soft and ductile. As carbon increases toward 0.77%, you start getting pearlite, which is a lamellar mixture of ferrite and cementite that forms during eutectoid transformation. Past 0.77%, proeutectoid cementite begins appearing along the grain boundaries of prior austenite grains. The eutectic point sits at 4.3% carbon and 1147 degrees Celsius, where liquid transforms directly into austenite and cementite simultaneously, forming ledeburite. Cast irons live in that region and behave completely differently from steels. I once spent three days trying to figure out why a batch of 1045 steel parts developed unexpected brittle fracture surfaces after normalizing. The material was supposed to be fine-grained ferrite and pearlite. I pulled the actual TTT curve and realized the furnace was cycling temperature in a way that held the steel right in the nose of the transformation curve for austenite-to-pearlite conversion, producing unusually coarse pearlite with a higher fraction of cementite networks at grain boundaries than the equilibrium diagram would suggest. The equilibrium diagram didn't warn me about that because it assumes infinite cooling time. Practical heat treatment never gives you infinite time.
Reading the Diagram for Real-World Decisions
The key lines you need to track are the A1 line at 727 degrees Celsius, which marks the eutectoid transformation temperature, the A3 line for hypoeutectoid steels showing where austenite fully forms on heating, and the Acm line for hyper-eutectoid steels showing complete cementite dissolution. When you're cooling from the austenite region, the diagram tells you where phase boundaries sit under equilibrium conditions. But equilibrium cooling means furnace cooling, roughly 10 to 20 degrees Celsius per hour. Quenching changes everything. Here's something that trips people up regularly: the diagram shows austenite as a single-phase region between roughly 727 and 1493 degrees Celsius for low-carbon compositions, but that doesn't mean you can hold steel at any temperature in that range and get the same grain structure. Grain growth accelerates dramatically above 900 degrees Celsius for most carbon steels. I learned this the hard way when a client complained about poor impact toughness in forged gears made from 8620 steel. The forging operation held the billet at 1250 degrees Celsius for extended periods, producing austenite grains several millimeters across. After hot working, those giant grains transformed to coarse prior-austenite structures that showed up as brittle fracture paths even after proper hardening. Normalizing at 880 degrees Celsius with controlled cooling fixed it, but the damage was already done on the first run. The phase diagram itself doesn't tell you about grain size, but anyone who's dealt with actual production knows grain size matters as much as phase composition.
Common Pitfalls When Using the Diagram
One major issue is assuming the diagram applies directly to all alloy steels. Add elements like chromium, molybdenum, nickel, and manganese shift every critical temperature and change the shape of the phase fields. A 4140 steel doesn't transform at 727 degrees Celsius the way 1045 does. The A1 temperature drops with most alloying elements except nickel and copper. This is why alloy steel heat treaters rely on modified diagrams or computational tools rather than the plain Fe-C diagram. Another frequent mistake is ignoring the difference between heating and cooling transformations. The A3 and A1 temperatures shift to higher values on heating due to hysteresis. If you're calculating austenitizing temperatures for hardening, using the cooling-side values will leave you under-austenitized, resulting in incomplete transformation and retained ferrite in your final microstructure. For 1045 steel, the A3 on cooling is about 780 degrees Celsius, but on heating it sits closer to 810 degrees Celsius. Hardening at 790 degrees Celsius based on the cooling diagram might seem correct but leaves you with unmixed ferrite islands that soften the surface during quenching. The diagram also breaks down for rapid solidification scenarios. Additive manufacturing and laser cladding of iron-carbon alloys produce microstructures that exist nowhere on the equilibrium diagram. I've seen martensite form in what should be a fully pearlitic composition because the cooling rates exceeded 1000 degrees Celsius per second. The diagram is still useful as a reference frame, but it doesn't predict those outcomes directly.
Get the Full Details

Where the Phase Diagram Of Iron Carbon Falls Short
The equilibrium diagram assumes slow, diffusion-controlled transformations. It cannot account for kinetic effects like bainite formation, martensitic transformation, or the effects of prior deformation on transformation temperatures. If you're working with quenching and tempering cycles, the diagram tells you approximately what austenite composition to expect before quenching, but nothing about what happens after. Martensite doesn't appear on the equilibrium diagram at all because it's a diffusionless product. For practical heat treatment planning, the Fe-C diagram is a starting point, not a complete answer. Pair it with TTT or CCT diagrams for time-dependent predictions. Use software like Thermo-Calc or JMatPro when alloying elements complicate the picture. And if you're dealing with something outside the standard 0 to 2% carbon range for steels, remember that the cast iron region introduces its own set of complications around graphite versus cementite stability that the basic diagram doesn't address without modification.