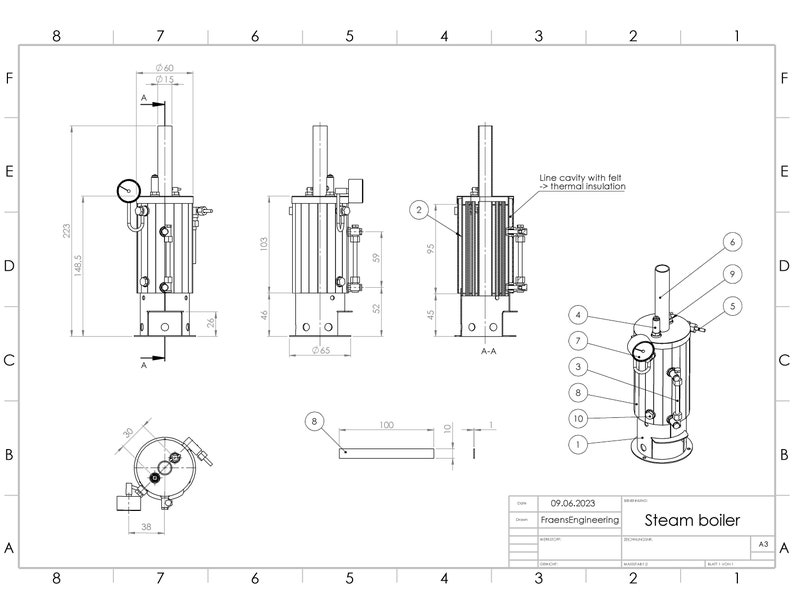
Building a model steam boiler and engine from scratch
Most people who get into model steam don't actually start with plans. They buy a kit, fiddle with it, realize it's not good enough, and then finally look at what it would take to make one from raw materials. That shift is where the real learning happens. Plans For Model Steam Boiler And Engine projects are a different animal entirely from kit builds, and they demand a level of precision that most hobbyists don't expect until they're already standing over a milling machine wishing they'd paid more attention to the drawings. I spent about three months on my first actual homemade model steam engine. The boiler part took longer than the engine itself. Here's how I approached it, and where things went wrong so you don't have to redo the work.
Where to find Plans For Model Steam Boiler And Engine
The good plans come from a few reliable sources. The Model Engineering website archives have decades of articles by people like David Williams and John Emms, and those are generally accurate because multiple builders have followed them. The Yahoo Groups for steam modeling — specifically the "class1" and "modeleng" lists — have threads going back to the late 90s with scaled plans shared by members. David Williams' book "The Amateur Steam Engine Builder" contains full-scale drawings you can reproduce at any ratio. There's also the British Model Engineer Magazine website, which has a subscription archive but free sample plans occasionally. Avoid random PDF sites. I've seen plans circulating that had the scale wrong on the cylinder bore, which means your piston doesn't fit, or the water jacket is dimensioned in inches when the rest of the drawing is in millimeters. Always cross-check the scale by measuring one known dimension before you commit material to the project.
The boiler: what actually matters
The boiler is the dangerous part. It's also the part that determines whether your engine runs for five minutes or fifty. A model steam boiler is small, but small pressure vessels fail catastrophically — there's no gradual like you'd get with a car tire. I learned that after a 1/4" tube leak turned into a blown end plate during a test firing. The repair cost was less than the embarrassment. Here's the basic construction path for a simple horizontal return-flue boiler: Step one: design the furnace tube. This is the 3/4" or 1" copper or brass tube that runs through the center of the cylindrical shell. It's where the flame travels, and it's what heats the surrounding water. The critical dimension here is the clearance between the tube and the end plates. You need at least 1/8" all around for water circulation. Too tight and you get scale buildup, which insulates the metal and creates hot spots. I once ran a boiler with only 3/32" clearance because I was working from a plan that had a typo in the drawing. It worked for six firings before the water passage restricted enough to cause a localized overheating event. The copper around the firebox end discolored dark purple — that's oxidation from temperatures above 400°F, which means the water wasn't cooling that section. I reamed out the holes and increased clearance to 3/16", and the discoloration stopped completely.
Get the Full Details

Step two: form the shell. Sheet copper or brass, rolled on a pipe bender or a homemade slug former. The joint runs along the length of the boiler and needs to be silver-soldered or braze-welded, not brazed with high-temperature rod. I used Easy-Flo 65 (silver brazing alloy with a lower melting point) and a propane/MAPP setup. The key is clean metal. Wire brush every surface, flux generously, and don't rush the heat application. Heat the joint area evenly, not the filler metal directly. The filler should melt and be wicked into the joint by capillary action, which requires the base metals to be hotter than the filler's melting point. Step three: the end plates. These are usually 1/4" to 3/8" phosphor bronze or mild steel. Bronze is easier to work but more expensive. Steel holds up better under repeated thermal cycling. Drill the tube holes first, then fit the tubes. The tubes should slide in with a light push fit — no hammering. If they're tight, ream them slightly. Then silver-solder the tubes to the end plates. I use a tiny bit of flux in the tube-to-plate joint and apply the flame just outside the joint so heat conducts through the plate into the seam. Step four: assemble and hydrostatic test. This is non-negotiable. Never fire a boiler without first pressurizing it with water to 1.5 times the intended working pressure. A hand pump works fine. Hold the pressure for at least ten minutes. Check every joint, every tube connection, every fitting. If you see weeping, depressurize, drain, dry, and repair. Water testing reveals problems that air testing won't — water doesn't compress, so any leak is immediate and visible. Air will simply bleed through a hairline crack invisibly until you apply heat.
The engine: keeping it simple
Once the boiler is done, the engine is straightforward. A basic two-cylinder horizontal slide-valve engine will run on 20-30 psi comfortably. The plan I used — adapted from a David Williams design scaled to about 1:3 — called for 1-1/4" stroke, 5/8" bore cylinders, and a 4" flywheel. The crankcase was machined from 6061 aluminum, and the cylinders from brass bar stock. The common mistake beginners make is overcomplicating the valve gear. A simple oscillating cylinder engine is actually harder to seal properly than a fixed-cylinder with slide valves. Stick with slide valves and an eccentric drive. It's proven, it's tolerant of minor machining errors, and you can adjust the valve timing by moving the eccentric on the crankshaft. One thing plans rarely mention: the importance of steam passage sizing. I found that the passages in my first engine were undersized by about 30% compared to what the plan showed. The result was sluggish operation at low RPM and excessive condensation in the passages. I opened them up with a files and a small end mill, and the engine came alive. Rule of thumb: the total cross-sectional area of all steam passages should be at least 60% of the piston area. For a 5/8" bore cylinder, that means roughly 0.3 square inches of passage area minimum.
Fuel and firing considerations
Most model steam boilers run on denatured alcohol, methyls, or a small oil burner. Denatured alcohol is clean and easy to control but produces low BTU output. A typical alcohol burner might deliver 5,000-8,000 BTU/hr, which is enough to bring a small boiler up to operating pressure in 15-20 minutes but struggles to maintain pressure under heavy load. I switched to a Wicks-style oil burner (about $40) and could run the engine continuously for an hour without dropping below 25 psi. The trade-off is soot and the need for a wick trimmer. Plans alone won't save you from bad material choices. I've seen builders try to make boilers from aluminum because it's easier to machine. Aluminum has a melting point around 1,200°F and loses strength rapidly above 400°F. Copper carries heat efficiently and maintains strength at boiler temperatures. Brass is acceptable but has a higher melting point than copper and is harder to solder. Mild steel is strong but difficult to work without proper equipment. These material choices directly affect safety margins, and no amount of planning changes the metallurgy. Another thing plans don't cover well: thermal expansion. Copper and steel expand at different rates. If your boiler has steel stays or fittings pressed into a copper shell, you need to account for that differential. I didn't on my first attempt, and after three heat cycles, a 1/4" NPT pressure gauge fitting wept. Tightening it made things worse because the copper had expanded differently than the steel threads. I replaced it with a brass fitting, which matched the copper's expansion coefficient much more closely, and the problem disappeared.

If you're serious about this, invest in a good reference book before you buy any stock material. "Steam Mobile Models" by John Emms and the "Model Engineer" building logs are both practical. The theoretical texts like Royle's "Model Steam Engineering" are useful for calculations but won't tell you how to actually hold a tube in place while you solder it. That comes from doing it, and doing it wrong a couple of times.