Getting the Plasmid Process Right
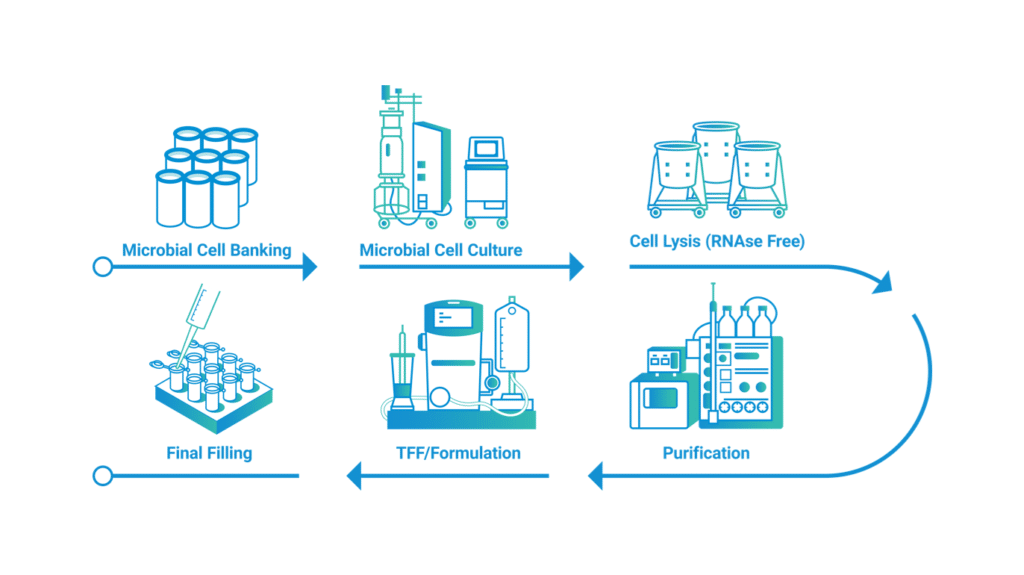
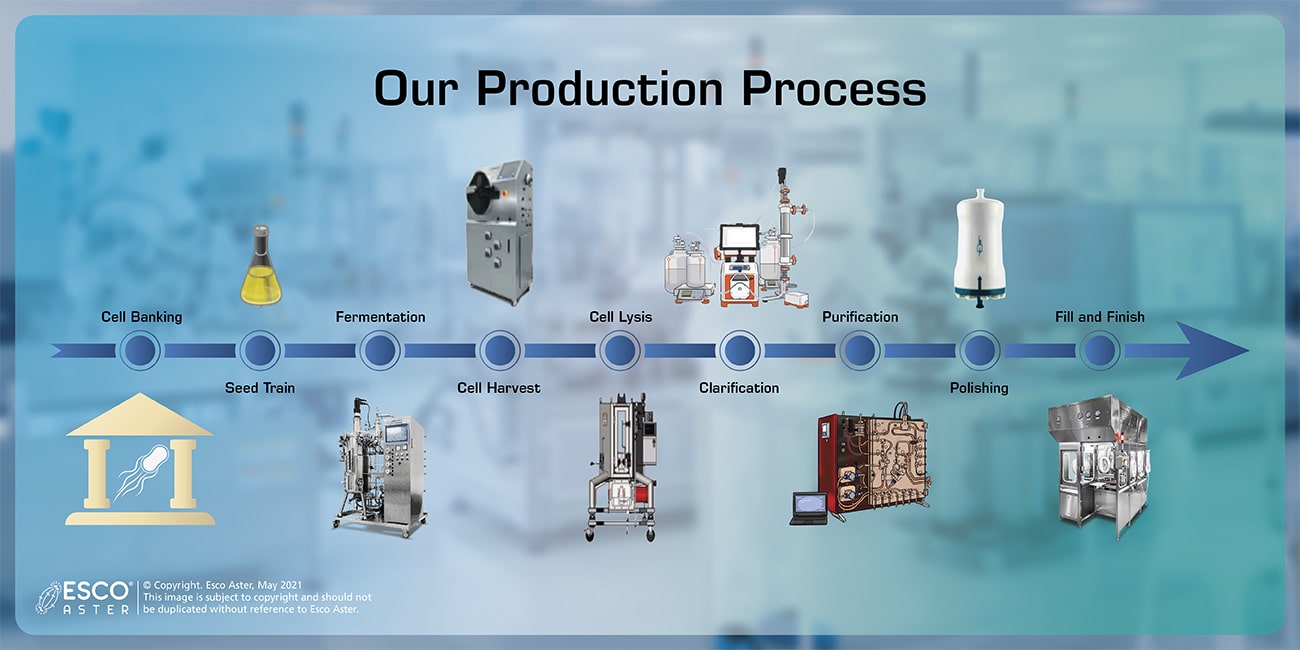
Most people think plasmid manufacturing is just growing bacteria and spinning it in a centrifuge. That is not wrong, exactly, but it leaves out half the work. The actual flow involves cloning, fermentation, lysis, purification, endotoxin removal, formulation, and QC. Each step has failure modes that will quietly kill your yield if you ignore them. I spent three years running pilot-scale plasmid prep for gene therapy vectors. We had one batch where the endotoxin levels spiked after purification even though the A260/A280 ratios looked fine. Turned out the silica column was leaching trace amounts of diethylpyrocarbonate at high pH. Switched to a resin-based alternative and the problem vanished. You do not notice these things until a regulatory auditor asks for your chromatography elution profiles.Plasmid Manufacturing Process Flow Diagram
The basic flow starts with a glycerol stock of competent cells. You streak on an antibiotic plate and pick a single colony into liquid culture overnight. This seed train step matters more than people admit because the growth phase directly influences plasmid supercoiling efficiency. A 1:100 inoculum into TB medium at 37C with 250 rpm shaking gives you about 6-8 hours to OD600 of 8-10. Go too hot or shake too hard and you get more relaxed circle forms instead of the supercoiled monomers your downstream work needs.After the overnight, you transfer into the main bioreactor. Most facilities run 2-10 liter scales for GMP work. The fermentation itself takes 4-6 hours with controlled pH at 6.8-7.2 and dissolved oxygen above 20 percent. Antibiotic concentration stays at 100 micrograms per milliliter of ampicillin or 50 for kanamycin. The key metric here is cell density measured as dry cell weight. You want 30-50 grams per liter for reasonable plasmid yields. Harvest happens by continuous flow centrifugation. The pellet gets resuspended in a TRITON X-100 lysis buffer with sodium hydroxide at 0.2 M. This alkaline lysis step denatures proteins and releases the plasmid DNA while chromosomal DNA precipitates out. You neutralize with potassium acetate at 3 M pH 5.5 and spin again. The supernatant contains your plasmid along with RNA contaminants and residual proteins. Purification typically uses affinity chromatography on a q Sepharose column. Most protocols use anion exchange at pH 8.0 loaded directly onto the resin. Plasmid binds while contaminants flow through. You elute with a sodium chloride gradient from 0 to 1 M over about 20 column volumes. This step usually cuts the process down from crude lysate to greater than 95 percent purity measured by agarose gel electrophoresis.
Endotoxin removal is the step most people underestimate. Polymyxin B affinity resin removes lipopolysaccharide down to less than 0.1 EU per milligram of plasmid. You have to validate this step carefully because endotoxin levels can vary by plasmid sequence and preparation method. I once saw a 10-fold difference in endotoxin carryover between two plasmids with identical backbone sequences but different insert sizes. The larger insert seemed to trap more lipopolysaccharide during lysis. Formulation involves buffer exchange into a saline or histidine solution at pH 7.4. Most final products concentrate plasmid to 0.5-2 milligrams per milliliter. You filter sterilize through a 0.22 micrometer PES membrane and fill into type I glass vials. The formulation buffer affects plasmid stability significantly. I found that adding 0.05 percent polysorbate 80 reduced aggregation during freeze-thaw cycling compared to plain saline. QC testing runs parallel to formulation. You need identity confirmation by restriction digest mapping and sequencing. Purity analysis uses capillary gel electrophoresis or agarose gel with ethidium bromide. Concentration measures as nanograms per microliter by A260. Endotoxin quantifies by chromogenic LAL assay. Sterility tests take 14 days by direct inoculation. Mycoplasma detection runs by PCR for about 24 hours.
Bottlenecks usually appear at the purification step. Anion exchange capacity limits how much plasmid you can load per run. A 5 mL column handles about 50-100 milligrams of plasmid before breakthrough occurs. You can scale up by using larger columns or implementing batch bind-elute mode. Most facilities optimize for throughput over resolution because plasmid QC tolerances are relatively wide compared to protein therapeutics. The main downside of this workflow is endotoxin variability. Even with Polymyxin B treatment, some plasmid preparations show inconsistent endotoxin removal depending on the bacterial strain and growth conditions. I recommend running a spike-recovery test with your specific plasmid sequence before committing to a purification protocol. This usually takes about 2 hours of method development but prevents months of regulatory headaches later. For large-scale production greater than 100 grams of plasmid per batch, most manufacturers switch to continuous chromatography mode. This cuts downstream processing time from 8 hours to about 3 hours per batch. The capital equipment costs around 500 thousand dollars for a complete platform but pays for itself within 6 months at high throughput.
Get the Full Details

If you need plasmid for research use only, a miniprep workflow with the QIAprep kit works fine for microgram quantities. The 15-minute spin column protocol gives you about 5-20 micrograms of plasmid with greater than 90 percent supercoiled form. Not suitable for therapeutic applications but adequate for transfection studies. For GMP manufacturing, you must follow the current good manufacturing practice guidelines from your regulatory authority. The FDA expects documentation of every process step including in-process controls and release criteria. Most sponsor develop a master cell bank and a master seed lot for plasmid production with extensive characterization data. Common pitfalls include ignoring the effect of plasmid size on purification. Larger plasmids greater than 15 kilobases behave differently during chromatography and require modified gradient conditions. I found that reducing the sodium chloride gradient slope by 50 percent improved separation of supercoiled from linear forms for our 18 kilobase vector.
The field is moving toward plug-and-play bioprocessing systems for plasmid manufacturing. These closed systems reduce contamination risk and cut cleaning validation time from days to hours. Most vendors offer 2-10 liter disposable bioreactors with integrated harvest and lysis modules. The per-batch costs run about 2-5 thousand dollars but the operational savings often justify the expense.
References and Further Reading
Current guidelines on plasmid DNA manufacturing come from the FDA, EMA, and PIC/S. Most reference the ICH Q5A and Q5D documents for viral safety and cell substrate characterization. The pharmacopeial chapters monograph plasmid DNA products with specific acceptance criteria for identity, purity, potency, and safety. Technical details on alkaline lysis and anion exchange chromatography appear in numerous peer-reviewed journals. The Biotechnology and Bioengineering journal has several papers on plasmid purification scale-up. The Journal of Chromatography A publishes method development workflows for endotoxin removal.