The Basics Nobody Really Gets Right
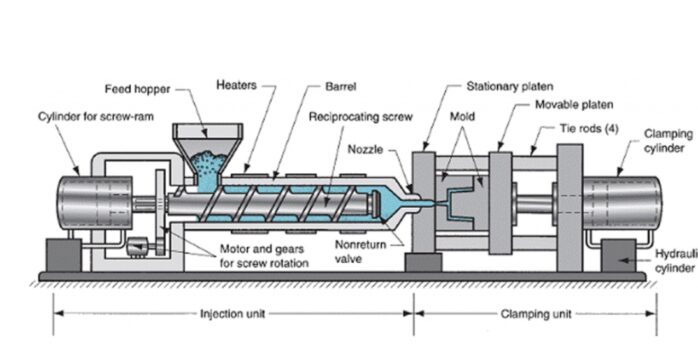
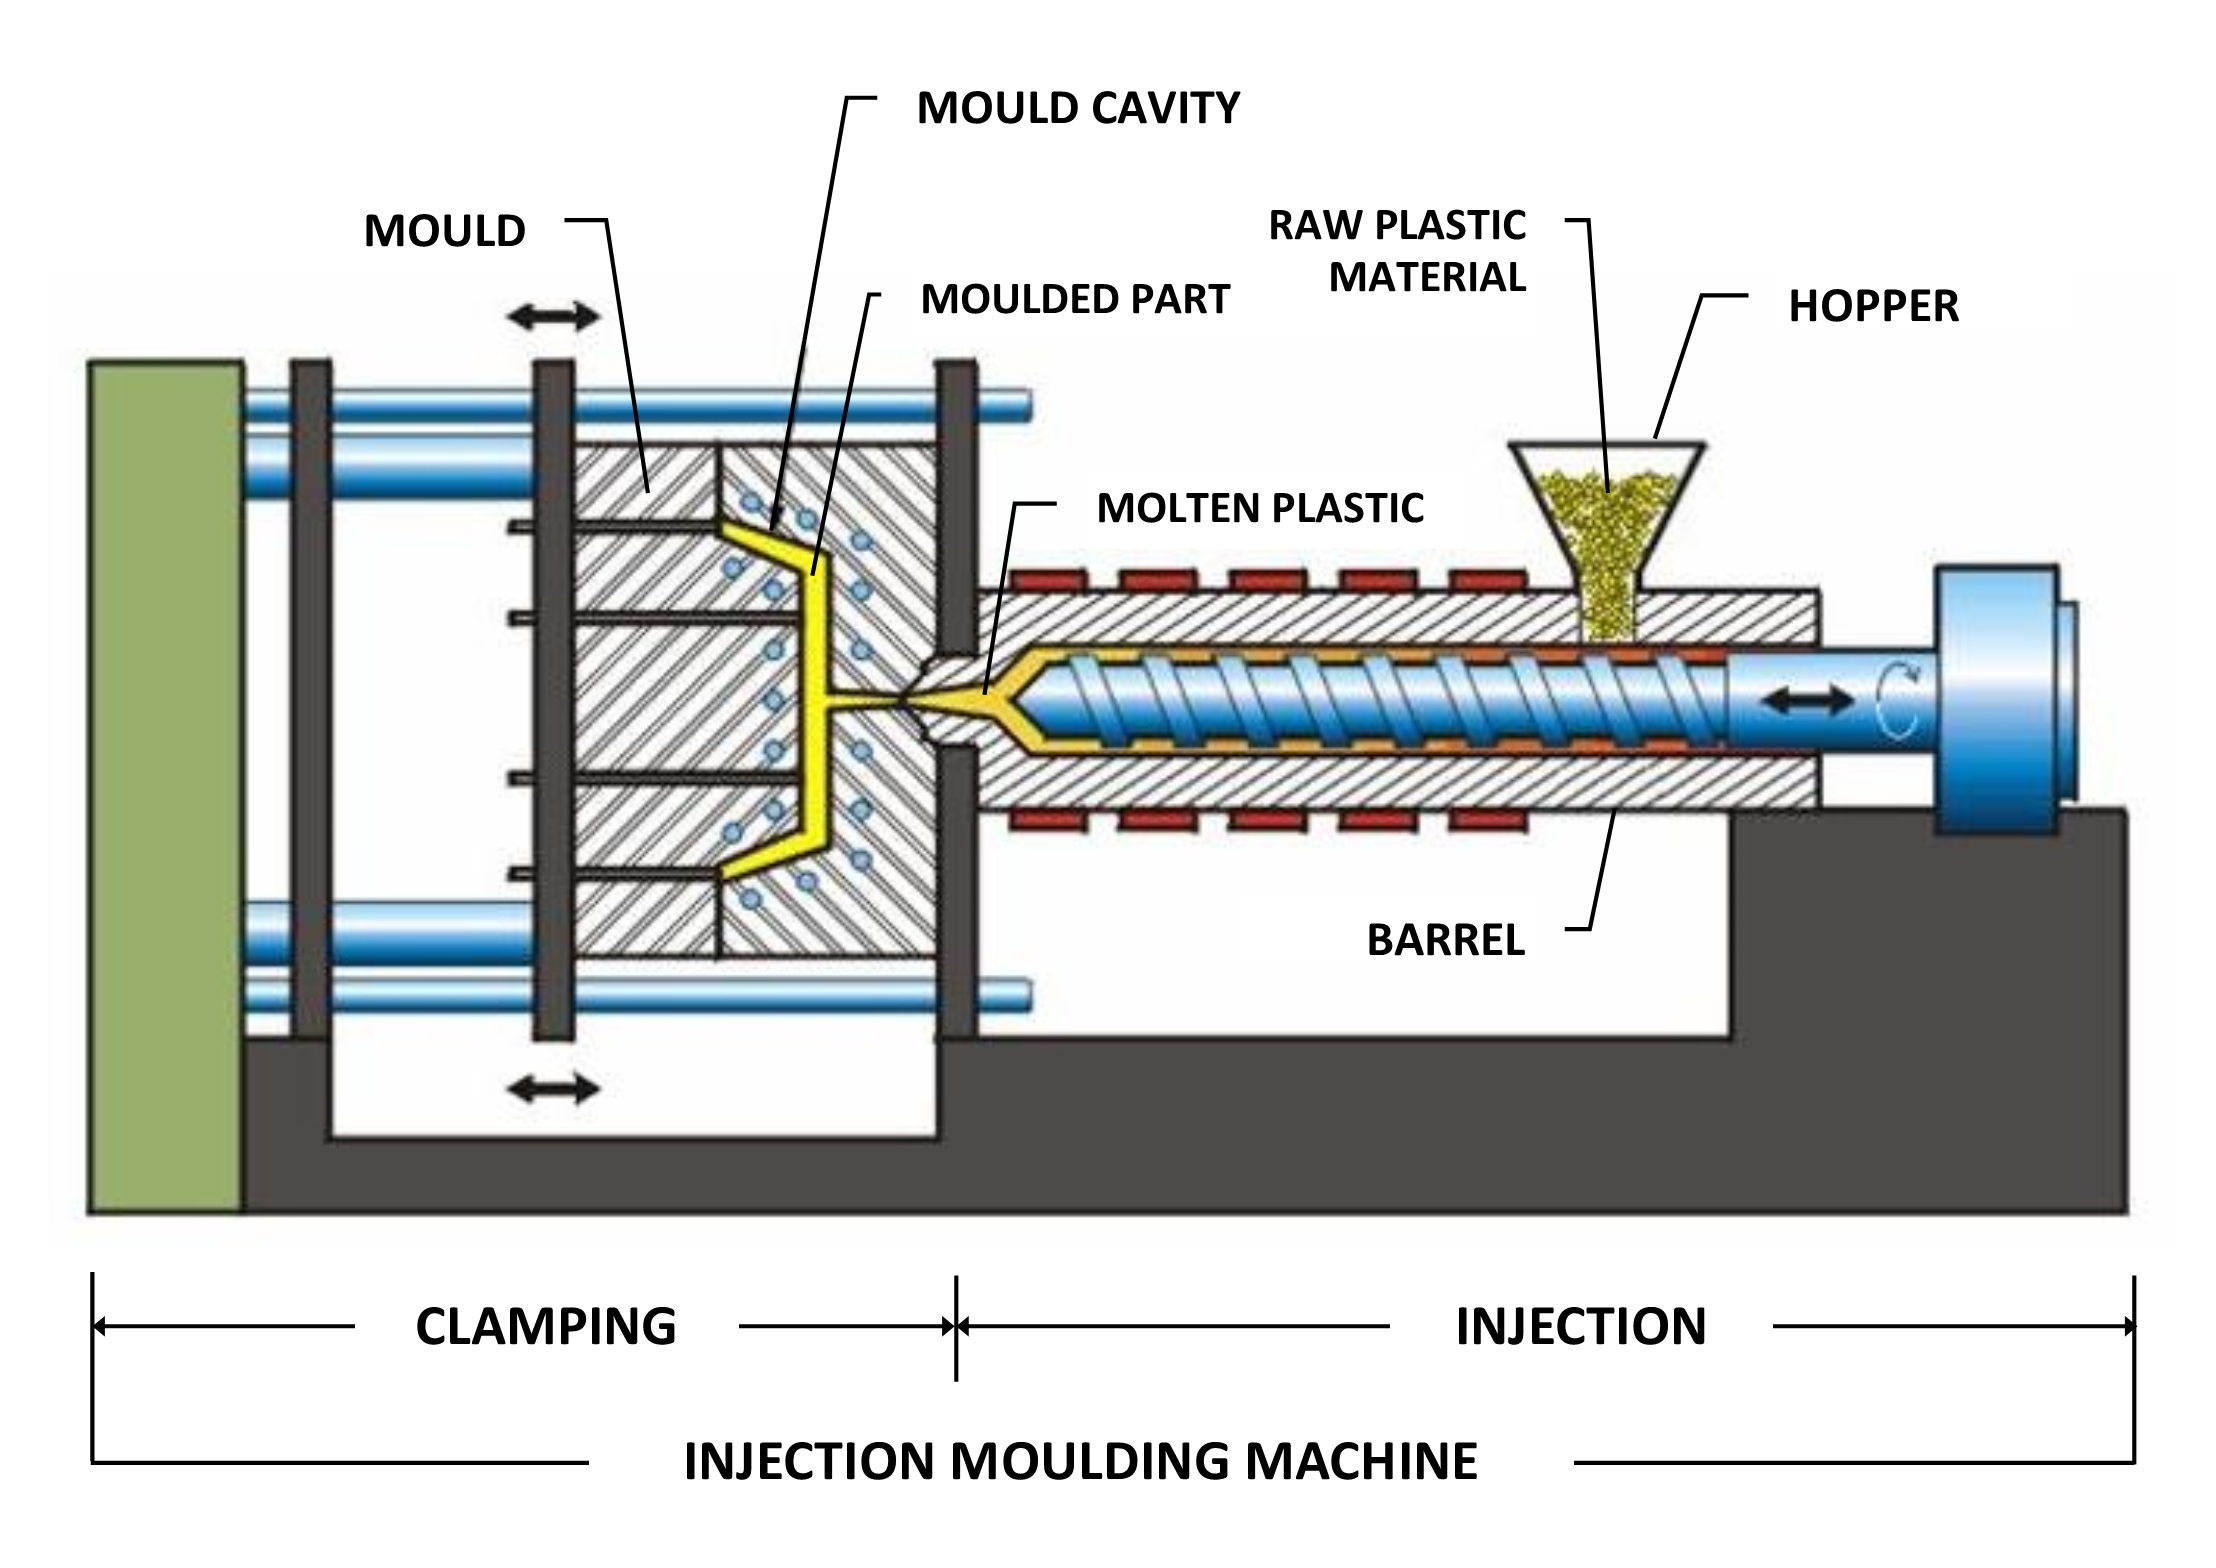
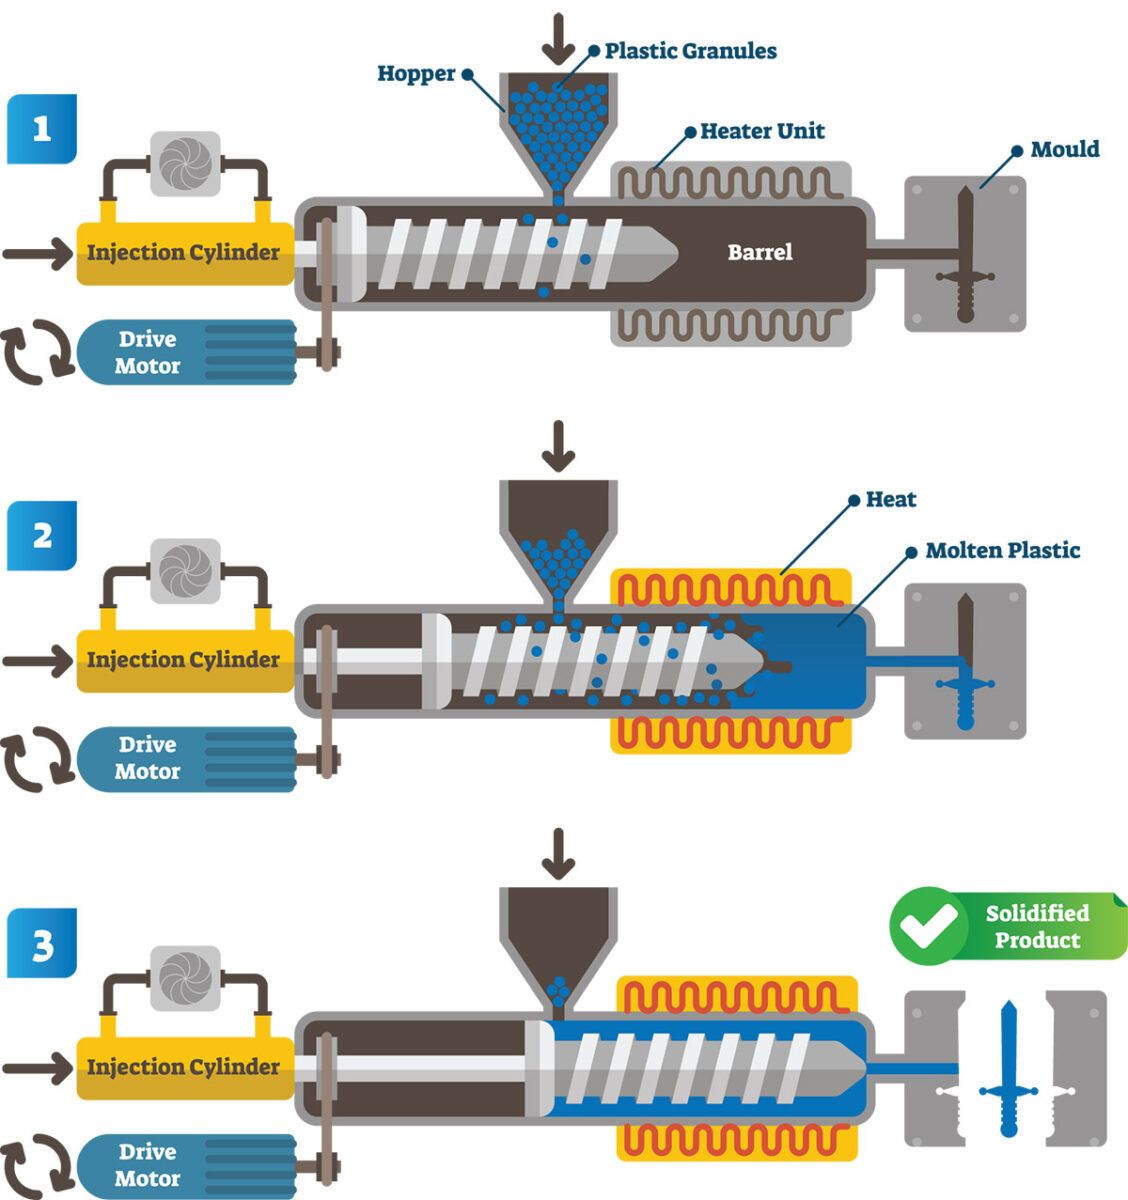
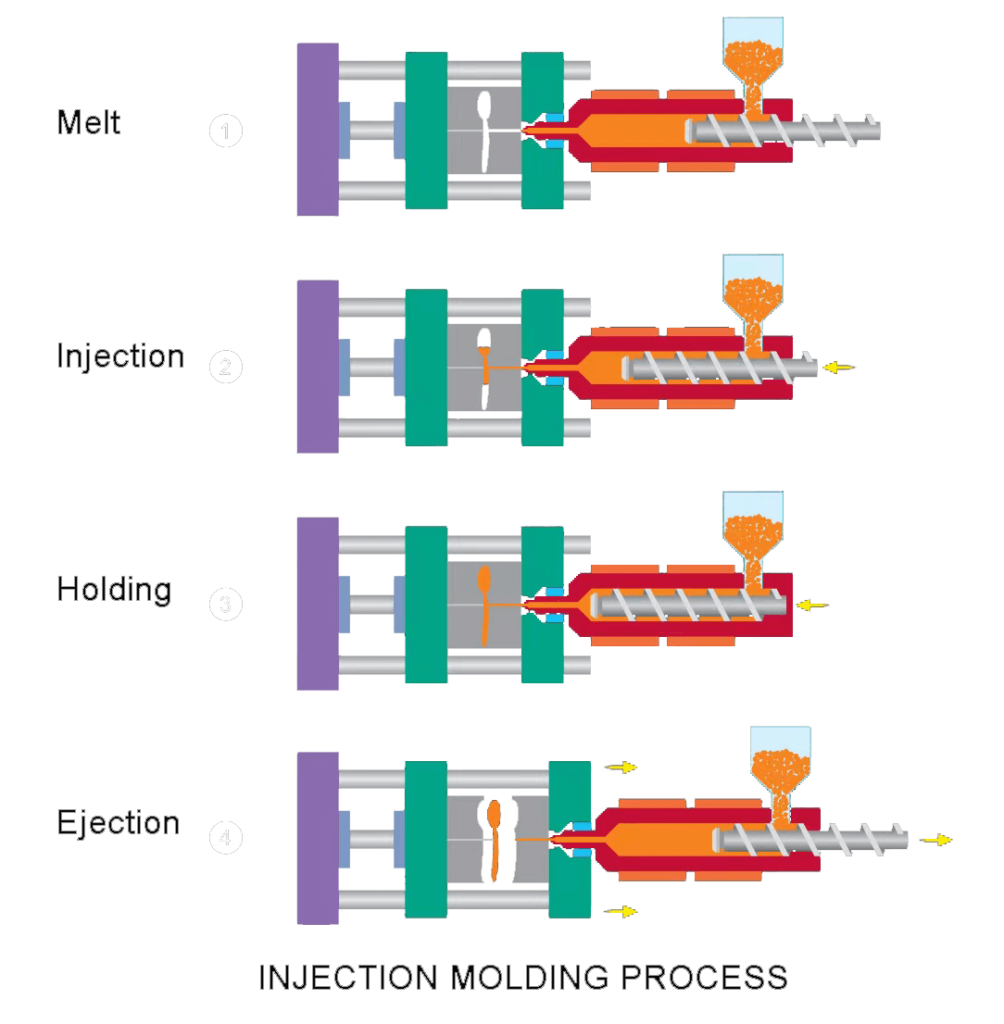
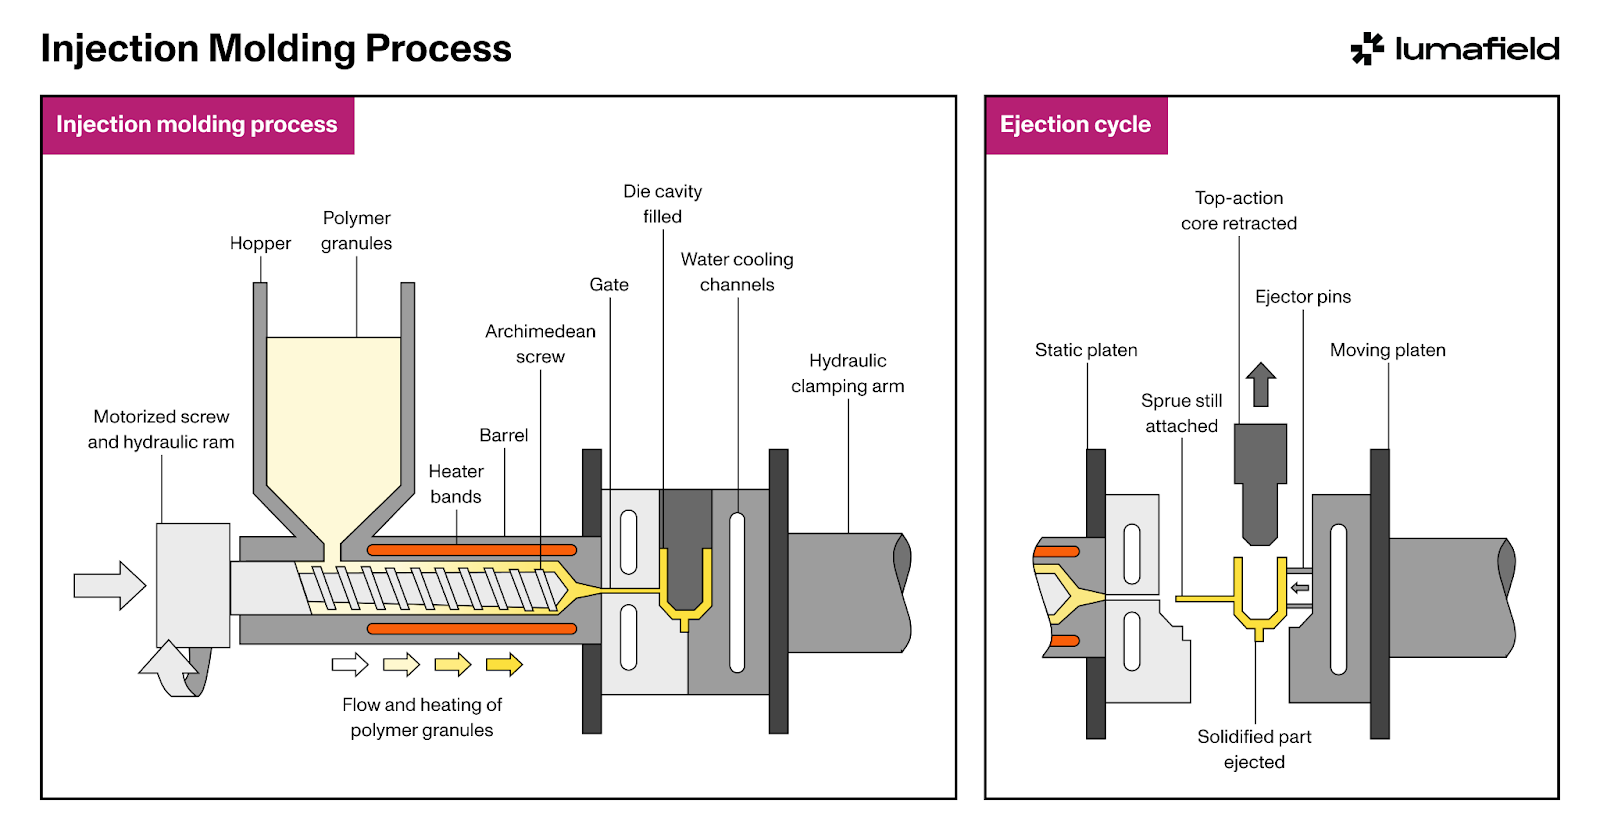
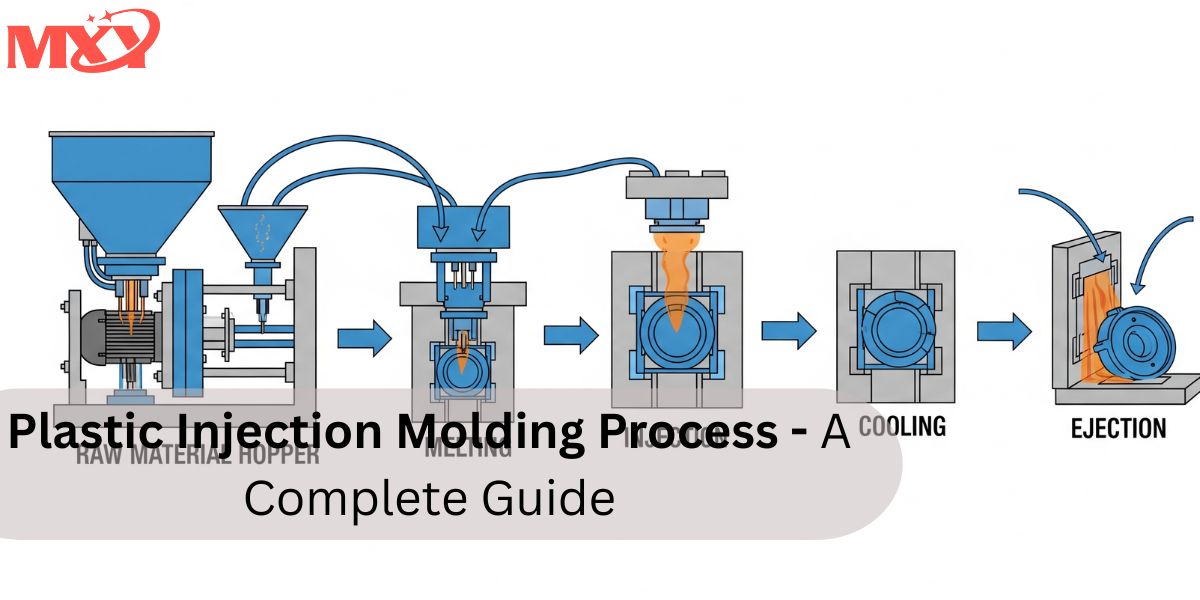
Plastic injection molding is one of those processes that sounds simple until you're the one responsible for turning out 10,000 identical parts and every single one has a visible sink mark on the backside. The general idea is straightforward enough: you melt polymer pellets, force the molten material into a closed mold cavity under high pressure, let it cool, and open the mold to eject the part. That's the textbook version. The actual day-to-day reality involves a lot more moving variables than most beginners expect. The process breaks down into a handful of core stages, but the order and timing of each one matters more than people realize. First, the mold closes. This isn't just about shutting two steel plates together — the clamping unit needs to apply enough force to keep the mold sealed against the injection pressure, which can easily reach 15,000 to 30,000 psi depending on the material and part geometry. I learned this the hard way early in my career when we were running short shots on a simple bracket and spent three days chasing the problem before someone finally noticed the machine's tonnage rating was borderline for the part's projected projected area at the selected material pressure. Upgrading the clamp wasn't an option, so we recalculated the flow path, split the gate into two locations, and cut the required injection pressure roughly in half. The parts came out clean after that. After the mold is locked, the screw rotates inside the heated barrel to convey and melt the pellets. The melt temperature needs to be set carefully — too hot and you degrade the polymer, too cold and you risk high shear forces damaging the material or overloading the machine. A typical polypropylene part might run at a melt temperature around 230 to 260 degrees Celsius. Nylon 6/6 runs considerably hotter, often 280 to 310 degrees. The exact setting depends on the grade, the machine's history, and what the part design demands.
The injection phase then pushes the molten plastic into the cavity. This is where most people think the process happens, but it's actually the cooling phase that dominates the cycle time. Cooling can account for anywhere from 50 to 80 percent of the total cycle depending on part thickness and material. That's why mold cooling channel design and placement is arguably the most impactful factor in production efficiency, yet it's also the most overlooked by teams that don't have a dedicated moldflow specialist on staff.
Material Selection Is Where Things Go Wrong Fast
Different polymers behave completely differently inside the same mold. Taking a part designed for ABS and switching to polycarbonate without adjusting the process parameters will likely result in a cascade of defects. ABS flows readily at relatively low temperatures and doesn't absorb much moisture, so it's forgiving for newcomers. Polycarbonate needs higher melt and mold temperatures and will yellow or splay if it picks up any moisture before processing. The material datasheet from the supplier should be your starting point, but actual machine conditions often require fine-tuning beyond what the recommendation sheet suggests. I ran into a situation once where a client switched from a virgin polypropylene to a 30 percent glass-filled variant without telling us. The part had the right dimensions on paper, but the filled material dramatically increased the viscosity and reduced flow length. We got short shots and excessive packing pressure requirements that we couldn't resolve without modifying the runner system. The moral here is straightforward: always verify the exact material grade being fed into the hopper. Material substitutions are one of the most common sources of problems in production runs, and they're almost always preventable with basic communication. Moisture control is another area that deserves attention. Materials like PET, PC, and nylon are hygroscopic, meaning they absorb water from the air. Processing wet material causes hydrolytic degradation, which reduces molecular weight and severely impacts the mechanical properties of the final part. A desiccant dryer running at the correct temperature and dew point is non-negotiable for these materials. I've seen shops skip dryers entirely to save space and energy on small runs, and the parts come out brittle and discolored every time. The cost of a proper drying system pays for itself quickly when you stop scrapping failed batches.
Get the Full Details
Mold Design Decisions That Matter
Gate location determines where the melt enters the cavity and has a direct impact on weld lines, cosmetic appearance, and packing efficiency. A poorly placed gate can create a visible weld line on the exterior surface of a part that will never pass quality inspection. I once spent a full week troubleshooting a cosmetic rejection issue on a white housing before realizing the gate was positioned at the center of a large flat surface. Moving the gate to an edge location eliminated the visible weld line entirely. Sometimes the solution is that simple, but finding it requires understanding how the material flows through the cavity during injection. Vent placement is equally critical. Trapped air in the cavity causes burns, short shots, and poor surface finish. Vents are typically machined as narrow slots along the parting line or at the end of the flow path. The depth of a vent depends on the material — thinner for high-viscosity materials, slightly deeper for low-viscosity ones. A common vent depth for most thermoplastics falls between 0.01 and 0.03 millimeters. If the vent is too deep, you'll get flash as the material forces its way out of the gap. If it's too shallow, the air won't escape fast enough and you'll have trapping issues. Ejection system design is another area where beginners make costly mistakes. The part needs to stay on the correct side of the mold during opening — usually the moving side — so the ejection pins can push it out cleanly. If the part sticks to the stationary side instead, you'll get ejection failure and potential damage to both the part and the mold. Shrinkage characteristics of the material determine which side the part will cling to. Most materials shrink as they cool, creating a grip on the core side of the mold. Adding draft angle, properly polishing the cavity surfaces, and using the right ejection pin layout resolves most sticking issues.
Process Parameters and What Actually Controls Quality
Injection speed, packing pressure, holding time, and cooling time are the four parameters that most directly affect part quality. They're interdependent, which means adjusting one affects the others. Increasing injection speed reduces shear heating in some cases but can cause jetting if the gate is too open. Reducing packing pressure saves cycle time but risks sink marks and dimensional instability. There's no universal setting — every part-material-mold combination requires its own optimized parameter set. One counter-intuitive insight that saves people a lot of trouble is the relationship between injection speed and part strength. Running faster doesn't always mean weaker parts. In many cases, a faster fill allows the material to reach the far corners of the cavity before it starts cooling and thickening, which reduces the need for excessive packing pressure downstream. The tradeoff is that high speeds can increase shear stress and potentially degrade heat-sensitive materials. It's a balancing act that requires testing, not guessing. Another common mistake is overpacking. More packing pressure doesn't always mean a denser, better part. Excessive packing can cause internal stresses that lead to warpage, cracking, or dimensional shrinkage after the part ejects and continues to cool. I've seen parts measured perfectly on the machine but then shrink out of tolerance by several hundredths of an inch once they reached room temperature. The solution is usually to optimize the packing curve rather than simply maximizing pressure. Using a calibrated scale to measure part weight and correlating that with dimensional data helps identify the sweet spot.
Defect Diagnosis and Practical Troubleshooting
Short shots happen when the cavity doesn't fill completely. The cause could be insufficient injection pressure, low melt temperature, inadequate venting, or a flow path that's too long for the material being used. The fix depends on identifying the root cause, not just throwing more pressure at the problem. I had a case where increasing injection pressure made the short shot worse because the added heat from higher shear was causing the material to gel near the gate, blocking flow to the far end of the cavity. Lowering the melt temperature slightly and increasing the injection speed resolved it. Flash is another common defect that stems from multiple possible causes. Mold wear, insufficient clamping force, contaminated parting surfaces, or excessive injection pressure can all contribute. If flash appears consistently in the same location across hundreds of parts, it's usually a mold issue. If it appears intermittently, it's more likely a process or material variable. Checking the mold for wear or damage on the parting surface and verifying that the clamping unit is actually delivering the rated tonnage at the operating temperature are good starting points. Sink marks appear on the surface opposite thick sections where material contracts during cooling. They're essentially surface depressions caused by inadequate packing during the solidification phase. Reducing wall thickness in those areas is the most effective fix, but that's often a design decision that can't be easily changed after tooling is cut. Process-wise, increasing holding pressure and extending holding time can reduce sink, but there's a limit before you start creating other defects like overpacking or ejection damage.
Quality Control and Realistic Expectations
Injection molding can produce parts with tight tolerances, but "tight" is relative. Most standard thermoplastic parts hold within plus or minus 0.1 to 0.3 millimeters depending on size and material. Going tighter than that requires special molds, controlled environment conditions, and often post-processing like machining or trimming. Some materials, like PEEK or PTFE, have higher shrinkage rates and are inherently harder to hold to tight tolerances. If your drawing calls for sub-0.05 millimeter tolerances over a large surface area, injection molding might not be the most cost-effective manufacturing method, and you should consider machining or a different forming process instead. Statistical process control is valuable for production runs but shouldn't be overdone for low-volume work. Monitoring critical dimensions at regular intervals, tracking material batch numbers, and maintaining a record of process parameter changes are reasonable practices for any run above prototype quantity. For volumes below a few thousand parts, the overhead of formal SPC documentation usually isn't justified. The focus should be on consistent process execution and clear communication between the design team and the molder. Tool life is another factor that affects cost and schedule. A well-maintained aluminum mold might last for a few thousand cycles before showing significant wear. Steel molds can last tens or even hundreds of thousands of cycles depending on the material being processed and the maintenance schedule. Hardened steel with proper surface treatment like nitriding or chrome plating extends life significantly when processing abrasive filled materials. Factor tooling cost and expected lifespan into your per-part pricing from the beginning rather than treating it as a separate line item that surprises you later.
When Injection Molding Isn't the Right Choice
There are scenarios where injection molding is the wrong answer, and acknowledging that upfront saves time and money. Low-volume production, typically under 500 to 1,000 parts, is often more economical using 3D printing, CNC machining, or vacuum casting. The upfront tooling cost for an injection mold ranges from a few thousand dollars for simple aluminum prototypes to over $100,000 for complex multi-cavity steel tools. That investment only makes sense when you're spreading it across enough parts to justify it. Certain materials that require extremely high processing temperatures or have problematic flow characteristics may be better suited to compression molding or extrusion depending on the part geometry. Complex internal features that would require extensive side-actions and lifters increase mold complexity and cost significantly. Sometimes a simpler design that eliminates internal undercuts or reduces the number of cavities needed can cut tooling cost by half without compromising the final part function. The fundamentals of plastic injection molding are accessible, but the nuances separate functional parts from failed ones. Understanding how material properties interact with mold design and process parameters is what turns a routine production run into a consistent, defect-free output. Pay attention to the details that others overlook — vent placement, gate location, drying conditions, and the actual material grade on the reel — and the process becomes much more predictable than it appears at first glance.