Working with PLCs without asking the right questions first is how projects fall apart
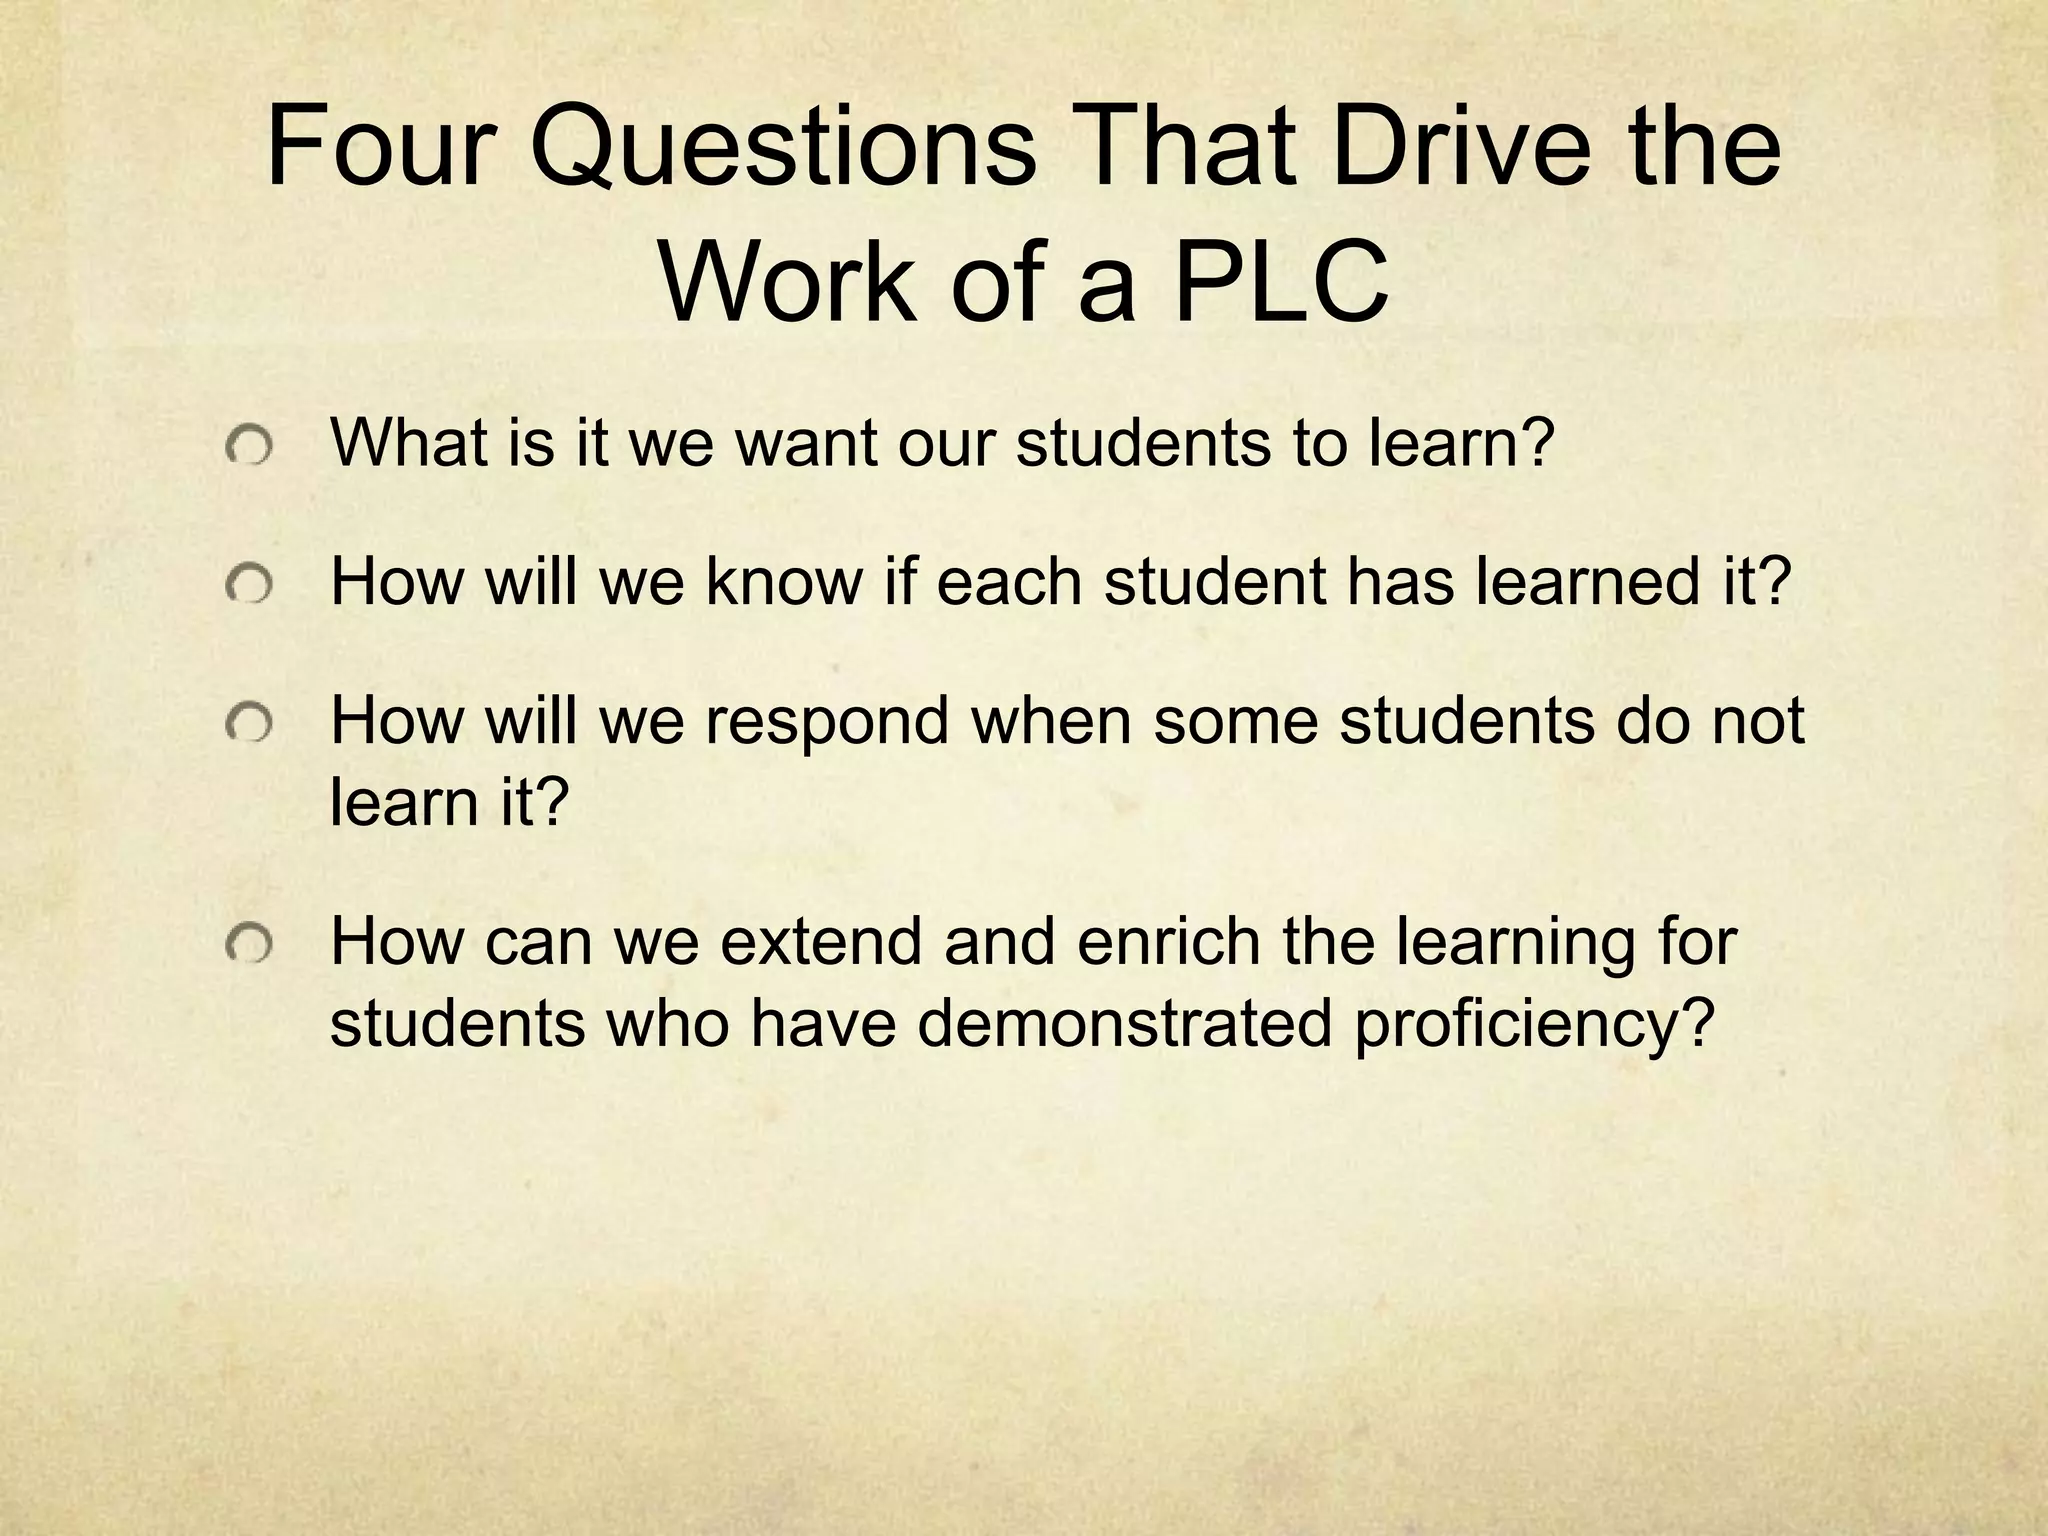
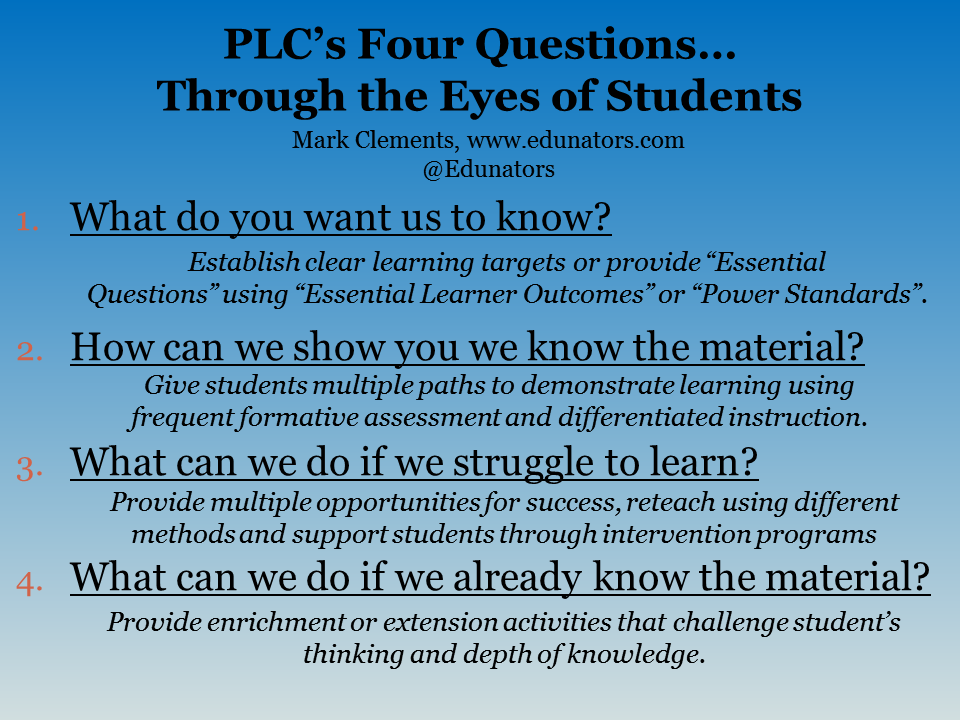
I've seen more shutdowns caused by unclear requirements than by bad code. The whole "Plc 4 Essential Questions" framework isn't some polished academic exercise. It's basically what separates the people who ship working systems from the ones who spend three weeks debugging something that was never properly scoped in the first place. Here's how it actually works when you're standing in front of a rack that needs to do something. Before you touch any ladder logic or function blocks, write down exactly what the process is supposed to do in plain language. Not what you think the operator wants. What the process actually does. I spent two days last year chasing a false alarm on a packaging line because the "what" wasn't clearly defined. The operator told me the machine would jam. Turns out the jam happened only when ambient temperature dropped below 15°C, which nobody had mentioned in the requirement phase. If you had asked the right version of question one upfront, you wouldn't be rewiring thermocouples at 2 AM. This section of your documentation should read like a story someone who has never seen the machine could follow. Subject, action, condition, expected result. One sentence per behavior. Nothing more. When you come back to this six months later after a change order, this is the only thing that will save you from rebuilding the entire logic from scratch.
Where does the data come from
Inputs. Sensors, switches, encoder counts, analog reads, remote I/O channels, whatever feeds into your system. Map every single one before you write a single rung. Not the ones you think matter. Every one. I ran into this on a water treatment upgrade where the BOM listed a pressure transmitter that turned out to be a different model with a 4-20mA range mapped inversely to what the PLC was programmed to expect. The tank was overfilling by about eight percent. The PLC logic was correct. The signal was backwards. Get the tag list. Confirm the physical address against the cabinet wiring diagram. Cross-reference with the instrument index if one exists. Then go look at the actual device and confirm the model number matches the paperwork. This takes thirty minutes and prevents weeks of troubleshooting later. There is no shortcut that doesn't involve physically verifying something.
What should the system do with that information
This is the logic portion. State machines, timers, counters, interlocks, sequencing. Write it out on paper or in a flowchart before you open the programming software. I used to skip this step because I figured I could think it through as I coded. That changed when I was working on a boiler control system and realized midway through programming the startup sequence that two safety interlocks were checking the same pressure point but with conflicting logic paths. One would allow ignition while the other would trip the flame failure alarm under identical conditions. The system would oscillate between safe and unsafe states every four seconds. The fix wasn't in the code. It was in the architecture. I ended up rewriting the entire sequence controller from the ground up. A simple flow diagram drawn on a napkin during the design phase would have shown me the conflict before any code existed. Use standard state-transition notation. Name each state clearly. Document the transition conditions in plain language next to each arrow. When someone later asks why the system behaves a certain way during a fault condition, you should be able to trace it back to a specific transition rule.
Get the Full Details
What happens when things go wrong
This is the question most people skip. Fault handling. Emergency stops. Safe shutdown states. Recovery procedures. A PLC program that only handles the normal case is a liability. I learned this the hard way on a material handling system where the conveyor would restart automatically after any fault without requiring a manual reset acknowledgment. The maintenance crew would clear a jam, hit the reset button, and the conveyor would start moving while someone was still clearing debris. That incident resulted in a lost finger and a three-month engineering review. Every fault condition needs a defined response. What does the system do when a sensor fails open. What happens when communication to a remote I/O module drops. What state does the process enter when power is restored after an unplanned outage. Write these down. Implement them. Test them. I keep a fault matrix spreadsheet that lists every possible failure mode for a given project along with the programmed response and the test procedure used to verify it. This document doubles as commissioning checklist and later becomes the first thing anyone asks for when troubleshooting down the line.
How to apply this in practice
Start a new project by filling out a one-page template covering all four questions. Keep it in the project folder alongside the wiring diagrams and BOM. Update it whenever scope changes. When you're writing the actual program, reference it constantly. If you find yourself adding logic that isn't covered by one of those four sections, stop and ask whether something is missing from the documentation rather than patching it into the code. The framework doesn't catch everything. It won't help you when the vendor changes their protocol mid-project. It won't protect you against a rushed commissioning schedule that skips the fault testing phase. And it certainly won't compensate for a hardware selection that was wrong from the start. But it will make those problems visible much earlier than they otherwise would be. That's the actual value. Not elegance. Just visibility.
When this approach breaks down
Complex motion control systems often outgrow a simple four-question structure. When you're dealing with synchronized axes, cam tables, or closed-loop servo loops, the questions need to be subdivided further. Each axis becomes its own subsystem with its own input validation, logic flow, and fault handling. You still use the same framework, but each answer to each question gets its own section. Trying to cram a multi-axis packaging machine into a single four-question document produces a mess that no one will actually read. Legacy systems are another edge case. Retrofitting an existing installation means the original documentation often doesn't exist or describes a completely different intent than what the machine actually does today. In those cases, reverse engineering the four questions becomes necessary before you can trust anything you write down. I spent a week on a retrocommissioning job just mapping inputs to actual field devices because the as-built drawings matched nothing I found in the control panel. The PLC program had been modified repeatedly over twelve years without any record of those changes. The four questions helped me reconstruct the original intent by elimination.

What you get out of it
Cleaner code. Fewer debug cycles. Documentation that doesn't require a translation step. The people who adopt this consistently report that their first-pass acceptance rate on new projects improves significantly, usually cutting rework time by roughly forty to sixty percent compared to projects where they skipped the upfront questioning. That's not a guarantee. It depends on how honestly you answer each question and whether you're willing to update the answers when reality proves them wrong. Nothing about PLC programming is simple. The four essential questions just make sure you're solving the right problem before you start building the solution.