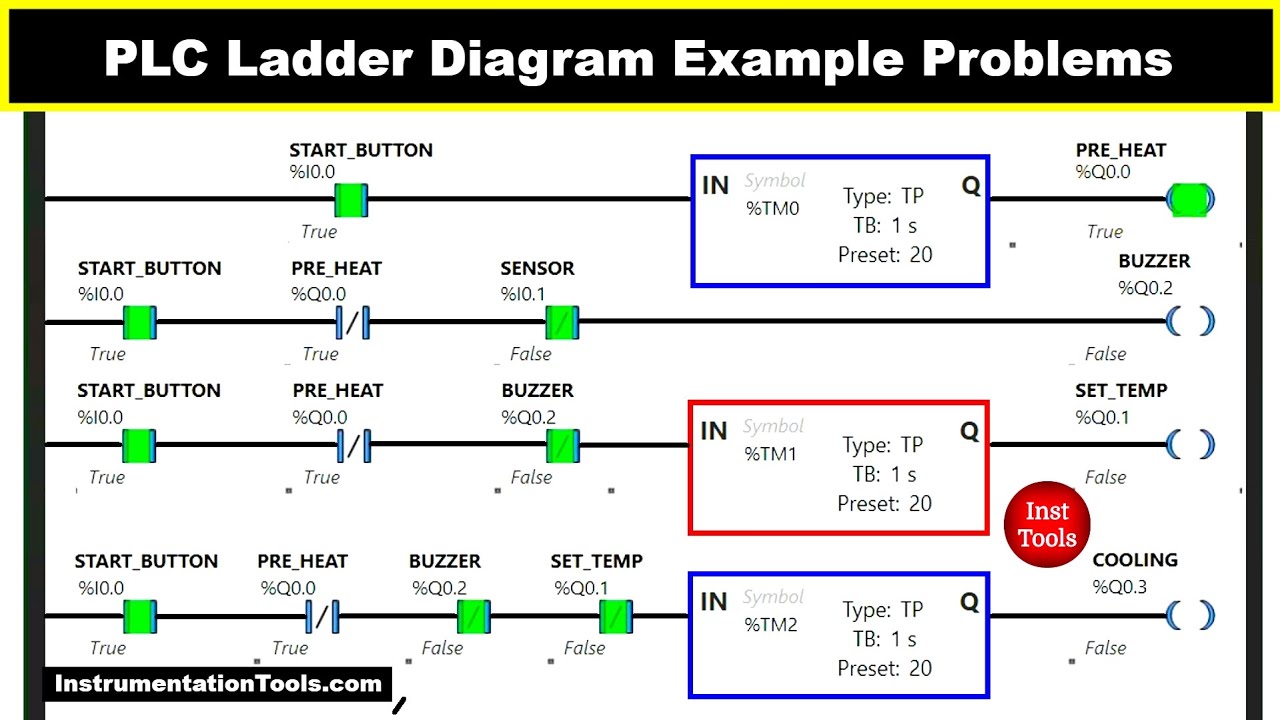
Where Most People Go Wrong With Ladder Logic
Most ladder logic practice problems you'll find online are useless. They teach you the syntax but skip the stuff that actually matters when a machine won't start at 2 AM on a Saturday. I've seen technicians who can build perfect training circuits but freeze when faced with a real panel. The gap is usually in how practice problems are designed, not in your understanding of the basics. Here is a blunt assessment of what works, what doesn't, and why you should be selective about what you practice.
What Quality Plc Ladder Logic Practice Problems Actually Look Like
A good practice problem has constraints, not just a blank canvas. Something like: design a motor control circuit with forward-reverse interlocking, three-wire start-stop control, overload protection, and a timer delay for jogging mode. Each constraint forces a decision point. If the problem just says "create a ladder diagram for a conveyor," you are not learning anything you will use on the job. I once ran across a practice set that had a problem asking you to create a sequence for a hydraulic press with a 10-second cycle and an emergency stop that must immediately break the circuit. The solution presented used a single timer coil (TON) for the entire cycle and an emergency stop that simply broke the rung leading to the timer. When I traced through it on paper, the E-stop would cut power to the coil, yes, but the output that was latched would de-energize and the timer would reset, which meant pressing start after an E-stop would jump straight to the press down position instead of going through the safety home sequence first. That problem exposed a real design flaw in the training material itself. I flagged it and built a workaround where the E-stop feeds into a separate safety latch rung that holds a status bit regardless of the main cycle, then forces a reset routine before any normal operation can restart.
Core Concepts You Actually Need to Drill
Latch circuits. Every beginner needs to burn into muscle memory the difference between a latching seal-in and a momentary pulse. The standard three-wire control circuit with start, stop, and seal is not optional. I still see people writing latches inside conditional branches where they should not be, creating race conditions that cause unpredictable behavior during scan cycles. Timers. On-delay, off-delay, and pulse timers. The common mistake is assuming all PLCs treat timer resets the same way. Some platforms clear accumulated time on rung false, others only clear when explicitly rung-disabled. This detail destroys your timing logic if you move a program from one brand to another without auditing every TON block. Counters. Up counters, down counters, and up-down counters. A lot of practice problems ignore the reset input entirely, which means once your counter reaches its preset, you are stuck until a full PLC restart. Real systems need a controlled reset path tied to a process condition, not just a manual reboot.
Get the Full Details

One-shot instructions. Falling edge and rising edge detection are essential for debouncing inputs and ensuring actions happen exactly once per trigger event. Skip this and your practice problems will work in simulation but produce double-triggered outputs on real hardware where contact bounce is a fact of life.
Plc Ladder Logic Practice Problems You Should Avoid
Anything that uses hypothetical sensor names without specifying signal type. A problem that says "sensor A turns on when object detected" gives you no information about whether it is NPN or PNP, sink or source, digital or analog. This is not a trivial detail. Wiring a NPN sensor to a source-type input terminal will result in the PLC never seeing the signal, no matter how correct your logic is. Any practice problem worth your time will specify the input type and expected behavior under fault conditions. Also avoid problems where the answer key presents a single correct solution. There is always more than one way to wire a logic circuit, and the best choice depends on the PLC platform, the I/O module type, and the maintenance requirements of the end user. If a tutorial insists your only option is to ladder-logic a state machine with dozens of rungs when a single structured text block would do, that is bad teaching.
How to Build Your Own Practice Problems
The most effective approach is to take a real piece of equipment you have access to and reverse-engineer its control logic into a problem set. A bottling line, a small packaging machine, a water treatment skid. Start with the I/O list. Number every input and output. Write the operational sequence in plain language first, then translate it rung by rung. Here is a specific exercise that actually builds skill: write a program for a traffic light intersection with two phases, pedestrian crossings on both sides, a flashing amber mode triggered by a fault input, and a timer-controlled emergency vehicle override. The fault input should disable the normal sequence and force the flashing amber state. The override should immediately switch to green for the vehicle direction while holding the cross street on red. Add a manual test mode where each output can be toggled independently. This single problem touches eight different concepts: basic sequencing, interlocking, fault handling, timer coordination, manual override, status indication, I/O mapping, and diagnostics. If you can build it cleanly on the first try, you have a solid foundation. If not, you now know exactly where your gaps are.

Tools and Resources That Are Actually Worth Using
Free PLC simulators exist for major brands. DeltaSoft, OpenPLC, and CODESYS evaluation versions can run ladder logic programs locally. The limitation is that simulation does not replicate timing jitter, electrical noise, or the physical behavior of relays and contactors. Your logic might run perfectly in software and still fail in the field because a solenoid valve draws enough current to cause a voltage sag that bounces a nearby input. For pure logic verification, these tools are fine. For anything approaching production readiness, you need to test with actual hardware, even if it is just a small control panel with momentary switches and indicator lights wired to a used PLC. The cost of a basic PLC plus I/O modules is nowhere near the cost of a site visit to fix a bug that simulation never caught. If you want downloadable practice problem sets with answer keys, search for documentation from industrial training organizations rather than random blogs. Textbooks like "Programmable Controllers" by Stephen L. Herman or manufacturer-specific application manuals from Mitsubishi, Siemens, and Allen-Bradley contain properly vetted exercises. The DIY forum compilations you find through general search are often filled with errors and untested solutions.
Common Mistakes That Ruin Practice Sessions
Not writing out the I/O table before starting. This is the single most common error. You jump straight into ladder logic, forget what address corresponds to which physical device, and end up rewriting half the program because you mixed up an input assignment. Spend ten minutes on the I/O list and you save an hour of debugging later. Testing only the happy path. If your practice problem only checks that the machine works when everything goes right, you have not tested the program. Intentionally break inputs. Simulate sensor failures. Check what happens when power drops and returns. Most beginner programs behave unpredictably during recovery sequences because the programmer never considered the state of every timer and counter when power is restored. Using internal bits freely without tracking them. Every latching bit, every status flag, every intermediate calculation needs to be documented in a comment or a separate address map. I have spent hours tracing a malfunction back to an internal bit that was being overwritten by a different section of the program because the original programmer used M001, M002, M003 without any naming convention and with no documentation.
Progression Path That Actually Works
Start with basic motor control: start-stop-latch, forward-reverse, star-delta. Move to sequential operations: a three-stage process with timers between each stage. Then tackle data handling: moving values between registers, comparison operations, and simple math. Finally, address structured logic: state machines using retentive timers and step-based transitions rather than a single rungs-of-logic monolith. Each stage should include a deliberately flawed practice problem where you are shown incorrect ladder logic and asked to identify and fix the issues. This builds the diagnostic skill that is more valuable than simply writing correct programs from scratch. On the job, you will spend more time reading and modifying someone else's logic than writing new code. The hardest transition is moving from relay-based thinking to PLC scan-cycle thinking. Relay logic is parallel and instantaneous. PLC logic is sequential and scanned top to bottom, left to right, every cycle. If you write logic that depends on an output changing mid-scan, you will get unexpected results. This is not a bug, it is the fundamental architecture, and every practice problem you do should reinforce understanding of how the scan cycle governs execution order.
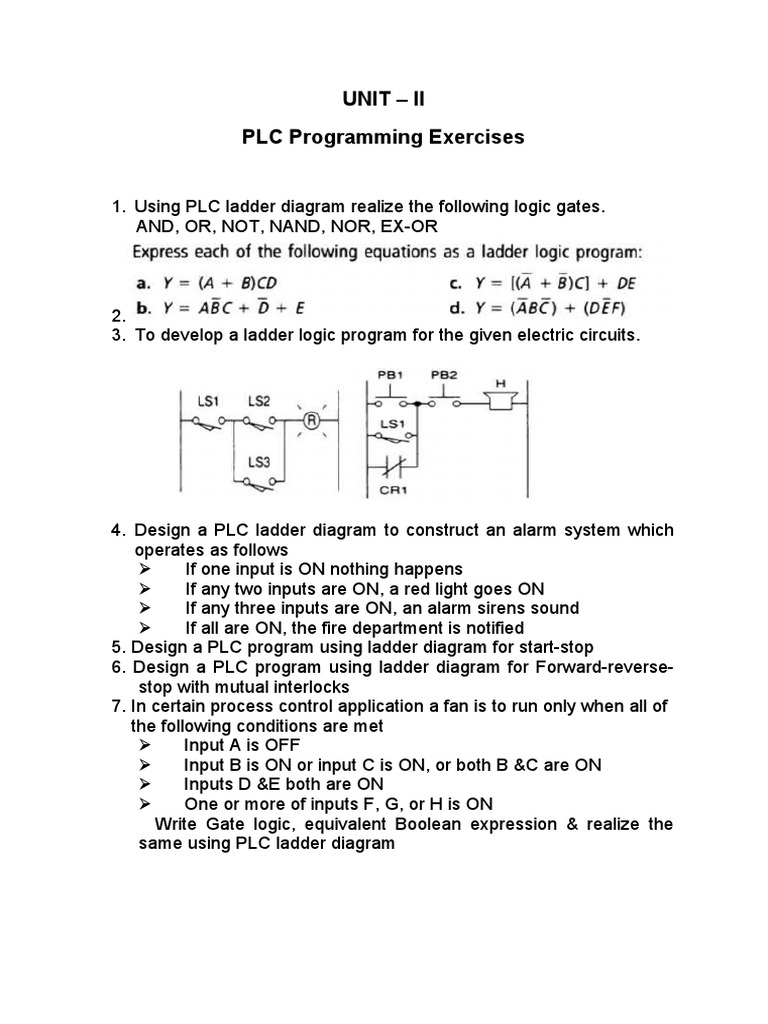
If your goal is to land a job working with PLCs, practice problems alone will not get you there. You need hands-on time, familiarity with at least one major brand's programming environment, and the ability to read an electrical schematic. But solid practice problems, chosen carefully and worked through methodically, will compress years of trial and error into weeks of deliberate skill building.