
Processing Polycarbonate on the Machine
Polycarbonate is one of those materials that will punish you if you treat it like ABS. It demands precision, and it doesn't forgive lazy setups. The main challenges come from its high melt viscosity, sensitivity to moisture, and the enormous shear heating it generates inside the barrel and through the gate. Get those three under control and the rest of the process stabilizes quickly. Miss any of them and you are chasing problems down the line — cloudiness, silver streaks, cracked parts, or just miserable cycle times. I ran into a specific issue a while back that illustrates exactly where people go wrong. We were molding a 3mm wall polycarbonate enclosure for an outdoor sensor housing. The first shots came out crystal clear, looked fine, and measured within tolerance. Then, six hours after demolding, the parts started warping. Not dramatically — maybe 0.3mm over a 120mm span — but enough to fail assembly. The root cause was hidden residual stress from a narrow gate that was shearing the material excessively during injection. The part felt good when it was hot and fresh off the mold. Once it cooled and relaxed, the stored energy in the polymer chains released and the geometry shifted. The fix wasn't to change the part design or the machine. It was to widen the gate from a 1.5mm pin gate to a 3mm fan gate, drop the injection speed by about 30%, and run a full anneal cycle at 130°C for two hours after molding. The warpage went away completely and the parts held their dimensions indefinitely. This is the kind of thing that doesn't show up in a data sheet. The resin supplier will give you a recommended processing window, and it's usually broad enough to be useful but narrow enough that if you ignore it, your parts will fail. The real work is understanding what happens between the numbers.
Drying is the first thing you get wrong, and it is also the easiest thing to fix. Polycarbonate is hygroscopic. It absorbs water from the air, and that water decomposes the polymer chains at melt temperature through hydrolysis. The result is a drop in molecular weight, which hits your tensile strength and impact resistance directly. You need to dry the resin at 120–130°C for at least four hours before it ever touches the hopper. A desiccant dryer with -40°F dew point is the standard setup. If you are running a gravimetric blender, make sure the drying section is integral or that the feed line is short enough to prevent rehumidification. I have seen people dry the material properly and then let it sit in an open hopper for an hour before the run starts. The material reabsorbs moisture fast. That single mistake turned a batch of good parts into a batch of cloudy, brittle ones. Melt temperature for polycarbonate typically runs between 280°C and 320°C. The material has a relatively narrow processing window compared to something like polypropylene. Below 280°C and you are pushing high injection pressures that create shear stress and potentially degrade the resin at the gate. Above 320°C and you start seeing yellowing and chain scission. The sweet spot for most general-purpose grades is around 290–305°C. Crystal-clear grades used in optical applications often run on the hotter end of that range because the lower viscosity helps reduce flow marks and weld lines. But running hot means you are closer to degradation, so you need to keep residence time short. If your cycle time is long and your barrel is large relative to the shot size, the material sits in the barrel longer and degrades more. A good rule of thumb is to keep your shot size at no less than 20–30% of the barrel capacity. This minimizes the amount of material sitting in the barrel between cycles. Barrel temperature profiles should be set with the rear zone cooler and the front zone hotter. Start at 270°C in the feed zone, ramp up through the compression zone, and finish at 290–310°C near the nozzle. The reason the feed zone runs cooler is simple: you want the pellets to start melting in the compression zone, not glue together and pack into a solid plug in the feed throat. If the feed zone is too hot, you get bridging and starvation. If it is too cold, the material won't plasticize properly and you get high back pressure and uneven melt. Most machines handle this well with a gradient profile. Just don't set all zones to the same temperature and expect it to work.
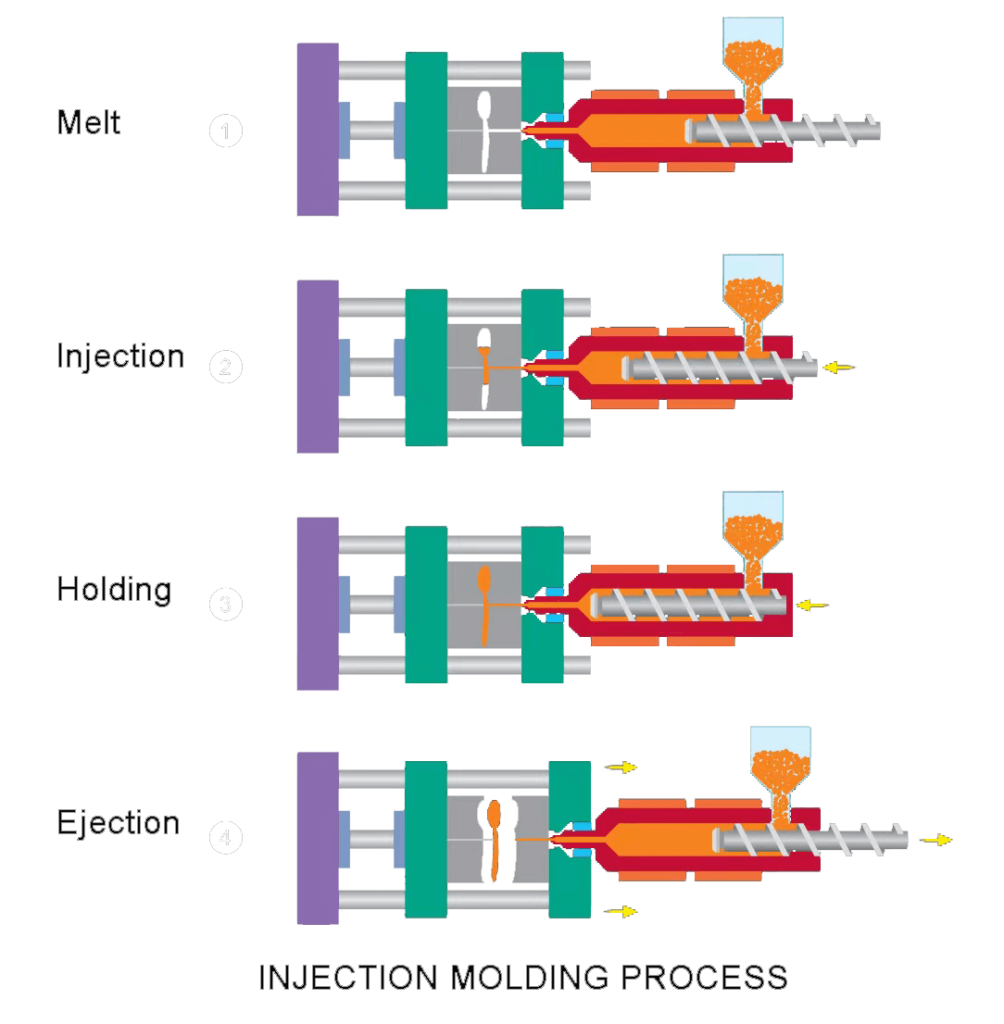
Injection pressure and speed require a different way of thinking with polycarbonate. This material is pseudoplastic, meaning its viscosity drops dramatically as shear rate increases. That is actually useful because it allows you to fill the cavity quickly without needing absurdly high pressures. The trick is finding the right balance. If you inject too slowly, the melt cools prematurely and you get short shots or poor surface fusion. If you inject too fast, you generate excessive shear heating and potentially burn the material at the gate or in thin sections. A typical starting point is an injection speed that fills the cavity in 1–3 seconds, depending on part geometry. Then watch the cavity pressure trace. If you see a sharp spike at fill completion, you are overpacking and creating internal stress. Back off the speed or reduce the hold pressure. Hold pressure is where a lot of people lose dimensional accuracy. Polycarbonate shrinks about 0.5–0.7% linearly, which is moderate for engineering thermoplastics but significant when you are holding tight tolerances. Hold pressure needs to be high enough to compensate for shrinkage as the material cools, but not so high that you are fighting the part into the mold and creating ejection problems. A common mistake is running hold pressure at 80–100% of injection pressure. For polycarbonate, that is usually excessive. Start at 40–60% of injection pressure and adjust based on part weight and dimensions. If the part is still shrinking and pulling into the cavity, increase hold pressure in 5% increments. If you are getting flash or having trouble ejecting the part, decrease it. Cooling time is where cycle efficiency lives or dies. Polycarbonate has a relatively high glass transition temperature — around 147°C — which means the part needs to cool well below that before it can be safely ejected without distortion. A typical cooling time for a 2–3mm wall part is 20–40 seconds, but this depends heavily on your mold temperature and the coolant flow in the mold. Mold temperature should be set between 80°C and 120°C. Higher mold temperatures improve surface finish and reduce residual stress, which is why optical and exterior-appearance parts often run at 100–120°C. Lower mold temperatures speed up the cycle but increase the risk of warpage and higher residual stress. I have found that running the mold at 90°C with a slightly longer cycle gives better dimensional stability than running at 60°C with a shorter cycle, even though the total cycle time is longer. The part comes out of the mold closer to its final shape.
Get the Full Details
One detail that nobody mentions enough is the effect of recycled material. Polycarbonate can handle some regrind, but it degrades with each thermal cycle. The molecular weight drops, the melt flow rate increases, and mechanical properties decline. A safe starting point is 10–15% regrind mixed with virgin material. If you need to run higher percentages, consider a solid-state polymerization post-treatment or switch to a grade that is specifically designed for high regrind content. Some suppliers offer PC grades rated for up to 30% regrind without significant property loss. But mixing your own regrind from different part colors or grades is a recipe for inconsistency. Keep the regrind source uniform. Gating and runner design matter more with polycarbonate than with many other materials because of the shear sensitivity. Hot runner systems work well with PC, but you need to be careful about dead spots and material stagnation in the manifold. A cold runner system is simpler to manage but generates more waste. Gate type is critical. A standard edge gate works for many applications, but for thick sections or high-visibility parts, a wide fan gate or a diaphragm gate around a cylindrical part will reduce shear stress at the gate entrance. The gate should be thick enough to allow material to flow without excessive shear, but thin enough to break clean. A good starting thickness is 60–70% of the part wall thickness at the gate location. If the gate is too thin, you get high shear heating and potential degradation. If it is too thick, you get slow freeze-off and longer cycle times, plus more cosmetic required after ejection. Venting is another area where polycarbonate can be unforgiving. The material flows easily and fills the cavity quickly, but if the air cannot escape, you get burns, short shots, or poor surface quality. Ensure your mold has adequate venting at the end-of-fill locations and along parting lines. Vent depth for polycarbonate should be around 0.01–0.02mm. Deeper vents risk flash because PC has low viscosity at processing temperatures. Shallower vents may not be effective. The standard parting line vent of 0.015mm is usually a good compromise.
When things go wrong, the first place to look is always moisture. Silver streaks, haze, or a reduction in impact strength almost always traces back to inadequate drying. If the parts are cloudy rather than just streaked, that is typically hydrolytic degradation — the polymer chains have broken down. If you see dark streaks or black specks, that is thermal degradation from too-high melt temperature or excessive residence time. Yellowing is a clear sign of overheating. If the parts are brittle and crack easily, check the molecular weight by measuring the melt flow rate of the processed material versus the incoming resin. If the MFR has increased significantly, the material has degraded. If the MFR hasn't changed and the parts are still brittle, the issue may be residual stress from poor gate design or excessive injection pressure. The biggest limitation of polycarbonate injection molding is that it is not a forgiving material for rapid prototyping or quick setup changes. You cannot just load the resin and start running. The drying requirement alone adds at least four hours to any startup. Mold temperature stabilization takes additional time. And because of the sensitivity to process variations, you need to monitor the process closely during the first shots to catch issues early. This makes it less ideal for short production runs where setup time eats into profitability. For high-volume production, the material performs exceptionally well and offers properties that are hard to beat — high impact resistance, good heat deflection, and excellent clarity. But if you are doing a run of 500 parts and your mold takes two hours to stabilize, you need to plan around that reality. If you need something easier to process and don't require the impact strength or clarity of polycarbonate, polystyrene or polypropylene will run faster and with fewer headaches. If you need heat resistance and clarity but want better processability, consider a polycarbonate-acrylonitrile butadiene styrene blend. These blend materials retain much of the PC performance profile while being more tolerant of process variations and allowing higher regrind content. The trade-off is slightly lower impact strength and lower heat resistance compared to pure polycarbonate. For most structural applications, the difference is negligible. For optical or extreme-temperature applications, stick with pure PC.
The material data sheets from suppliers like Covestro, SABIC, and Teijin will give you baseline processing recommendations. Use them as a starting point, not a final answer. The actual optimal settings depend on your specific mold design, machine condition, ambient environment, and the exact grade you are running. Keep records of what works for each material-lot and mold combination. Process stability with polycarbonate is not something you achieve once and forget. It is something you maintain through consistent drying, consistent mold temperatures, and careful monitoring of every shift.


